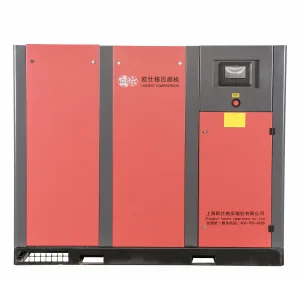
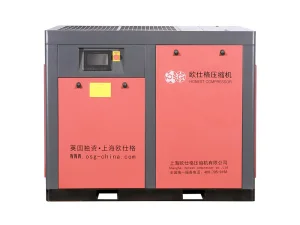
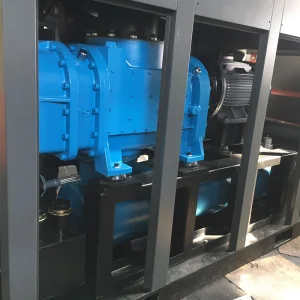
Featured Export Vacuum & Compression Systems
Engineered in Shanghai under British technical governance. Precision air-cooled, oil-free, and permanent magnet VFD industrial solutions certified for heavy continuous duty.

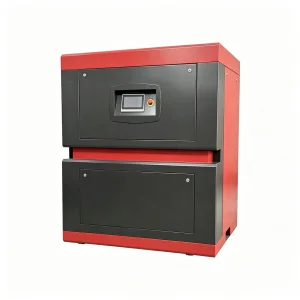
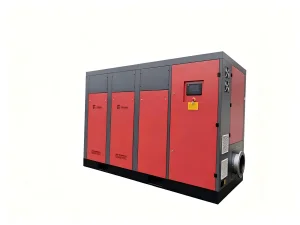

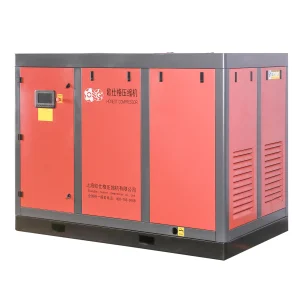



Global Commercial & Industrial Status of Air-Cooled Vacuum Systems
A Whitepaper on Energy Transition, Decarbonization, and Process Optimization by China’s Leading Screw Vacuum Machinery Exporters
The global industrial vacuum ecosystem is undergoing a fundamental paradigm shift. Historically dominated by liquid-ring, oil-sealed rotary vane, and steam-ejector mechanisms, modern manufacturing facilities are rapidly transitioning toward dry air-cooled screw vacuum pump architectures. As a premier China air cooled vacuum pump exporter, Shanghai Honest Compressor Co., Ltd. (operating under British engineering standards since 2004) stands at the forefront of this industrial transition.
The global vacuum market—projected to exceed USD 8.5 Billion by 2030—is driven by stringent environmental regulations, escalating energy tariffs, and the imperative for absolute process purity. In regions across Europe, North America, and the Asia-Pacific, industrial facilities face rigorous mandates regarding industrial wastewater discharge (Zero Liquid Discharge - ZLD initiatives) and carbon intensity metrics. Traditional water-ring vacuum pumps, which consume hundreds of thousands of liters of process water annually while creating toxic effluent streams, are increasingly being decommissioned. Simultaneously, oil-sealed systems present recurring contamination risks, hazardous oil waste disposal liabilities, and high maintenance overheads.
Air-cooled dry screw vacuum pumps resolve these systemic challenges by eliminating water usage entirely and operating without oil in the compression chamber. By combining variable-pitch screw profile engineering with high-efficiency forced-air cooling systems, modern Chinese export models deliver ultimate vacuum levels down to $10^{-2} \text{ mbar}$ while reducing total cost of ownership (TCO) by up to 35% compared to legacy liquid ring configurations.
Key Market Drivers Accelerating Global Adoption
- Eradication of Process Water Consumption: Air-cooled designs eliminate water chillers, cooling towers, fluid piping, and water treatment costs, achieving true zero-water vacuum creation.
- ISO 8573-1 Class 0 Purity: Dry screw chambers run without liquid sealing lubricants, guaranteeing zero hydrocarbons carry-over into sensitive processes such as semiconductor chemical vapor deposition (CVD) or pharmaceutical freeze-drying.
- Integration of Smart VFD Electronics: Advanced Permanent Magnet Variable Frequency Drives (PM VFD) dynamically adjust rotor RPM to match real-time process gas loads, preventing unnecessary energy draw during baseline idling.
- High Thermal Tolerance & Gas Handling: Optimized rotor cooling geometries allow air-cooled units to reliably handle corrosive, condensation-heavy, and vapor-rich industrial exhausts without thermal lockup.
Engineering Architecture & Technical Roadmap
Thermodynamic Mechanics, Variable Pitch Geometry, and Advanced Air Cooling Heat Dissipation
Variable-Pitch Rotor Physics
Unlike conventional fixed-pitch screws that compress gas uniformly along the shaft length, our advanced variable-pitch rotors compress process gas progressively toward the discharge port. This reduces gas exhaust temperatures by 20–30°C and minimizes mechanical power loss ($W_{comp}$), yielding unmatched isothermal efficiency.
Dual-Channel Forced Air Cooling
Achieving robust thermal equilibrium in an air-cooled pump requires sophisticated heat-exchange dynamics. Integrated high-static pressure fans drive ambient air through dual-ducted internal heat sinks, cooling both the oil-lubricated gear cavities and the dry pump casing without liquid cooling loops.
IE4/IE5 PM VFD Motor Integration
Direct-coupled permanent magnet synchronous motors deliver constant full-load torque across wide speed ranges (500 to 4500 RPM). Integrated inverter control automatically ramps down pump velocity during holding vacuum phases, cutting parasitic power loss.
Rotor Metallurgy & Anti-Corrosion Surface Engineering
In harsh industrial processes—such as chemical degassing, organic solvent recovery, or semiconductor etching—the internal surfaces of the vacuum pump are subjected to highly reactive process media. To prevent premature chemical degradation and mechanical abrasive wear, China export vacuum pumps utilize state-of-the-art metallurgy and protective thin-film coatings:
- Nitinol & Nickel-Alloy Plating: Multi-layer electroless nickel-plating (ENP) providing uniform thickness across complex screw profiles, resisting acidic vapor attack ($HCl, H_2SO_4$).
- PFA / PTFE Fluoropolymer Coatings: Applied to internal compression chambers to minimize condensate adhesion, prevent polymer scaling, and lower surface friction coefficients.
- Ductile Iron (FCD 600) & Stainless Steel Rotors: Precision-machined on five-axis CNC centers to maintain clearance tolerances under 0.03mm, preventing internal back-leakage without physical metal-to-metal contact.
Localized Industrial Application Scenarios
Deploying Tailored Vacuum Solutions Across Diversified Global Manufacturing Ecosystems
Lithium-Ion Battery Manufacturing
Essential for high-vacuum electrolyte filling, pouch-cell degassing, and slurry drying. Air-cooled dry pumps prevent moisture contamination, maintaining cell dew points below -50°C for maximum energy density.
Semiconductor & Photovoltaics
Used in solar ingot pulling, PECVD, and load-lock chamber evacuation. Dry operation eliminates oil vapor back-streaming, ensuring high wafer yield rates in Class 10 cleanroom environments.
Chemical & Pharmaceutical Distillation
Facilitates low-temperature vacuum distillation, solvent recovery, and active pharmaceutical ingredient (API) crystallization. Air-cooled designs reliably exhaust flammable solvent vapors without explosive risk.
Comparative Performance Matrix: Vacuum Technology Technologies
When selecting industrial vacuum machinery, procurement engineers must weigh capital expenditure against lifetime operating costs, environmental impacts, and maintenance complexity. Below is a comparative engineering benchmark compiled from field operational data:
| Performance Criterion | Air-Cooled Dry Screw Pump | Oil-Sealed Rotary Vane | Liquid-Ring Vacuum Pump |
|---|---|---|---|
| Operating Vacuum Range | $10^{-2} \text{ mbar}$ to $10^{3} \text{ mbar}$ | $10^{-1} \text{ mbar}$ to $10^{2} \text{ mbar}$ | $33 \text{ mbar}$ to $10^{3} \text{ mbar}$ |
| Process Water Consumption | Zero (0 L/hr) | Zero (0 L/hr) | High (Up to 5,000 L/hr) |
| Oil Contamination Risk | Absolute Zero (ISO Class 0) | High (Oil carry-over backstreaming) | Low (Water medium contamination) |
| Energy Efficiency (Specific Power) | Superior (VFD dynamic tuning) | Moderate (Fixed friction loss) | Low (Viscous liquid drag) |
| Routine Maintenance Interval | 16,000 – 24,000 Hours | 2,000 – 4,000 Hours | 8,000 – 12,000 Hours |
| Waste Stream Generation | None | Hazardous Waste Oil | Contaminated Effluent Water |
Turnkey Industry Solutions & System Integration
From Single Utility Units to Centralized Smart Factory Vacuum Networks
Modern mega-factories require more than standalone machinery; they demand intelligent, interconnected utility networks. As a sophisticated OEM/ODM manufacturer in Shanghai, Honest Compressor provides complete macro-industry solutions designed to seamlessly interface with modern Plant Distributed Control Systems (DCS) via IoT and Industrial Ethernet protocols (Modbus RTU, Profinet, EtherCAT).
Centralized Vacuum Automation
By networking multiple air-cooled screw vacuum pumps through a master PLC controller, air flow capacity dynamically scales from 10% to 100% depending on real-time line utilization, reducing energy footprint across multi-line facilities.
Explosion-Proof (ATEX / IECEx) Packages
For chemical and hazardous petrochemical environments (Zones 1, 2, 21, and 22), our customized vacuum packages feature flameproof enclosures (Ex d IIB/IIC T4), intrinsically safe sensor circuits, and spark-free static grounding.
Digital Twin & Predictive Maintenance
Integrated vibration telemetry, bearing temperature monitoring, and oil quality sensors feed machine-learning algorithms. System diagnostics predict component wear up to 1,500 operating hours prior to failure, avoiding unplanned production line shutdowns.
Frequently Asked Questions (FAQ)
Technical Insights & Sizing Guidance Direct from Vacuum Engineering Specialists
Complete Screw Machinery & Air Systems Portfolio
Explore our full line of rotary screw compressors, oil-free blowers, two-stage high-pressure units, and dry vacuum pumps manufactured for export.