Engineered Oil-Free Solutions for Global Procurement
Precision-machined rotary screw compressors, vacuum extractors, and dual-speed units configured for continuous heavy-duty service across international voltage and environmental standards.




The Macro Paradigm Shift: Why Clean Air Purity Dictates Modern Industrial Yields
In high-tech industrial plants, compressed air is the fourth utility. For decades, traditional manufacturing relied heavily on oil-flooded rotary screw air compressors outfitted with multi-stage coalescing filters and carbon adsorption towers. However, mechanical coalescing fails to prevent sub-micron vaporized oil aerosols from breaking through under ambient thermal spikes or filter degradation.
As advanced fabrication tolerances tighten across biotechnology, semiconductor photolithography, and electric vehicle battery gigafactories, oil contamination can ruin entire production runs. A single hydrocarbon droplet can blind analytical sensors, ruin sterile biopharma fermentation broths, or cause catastrophic coating delamination in lithium battery separator foils.
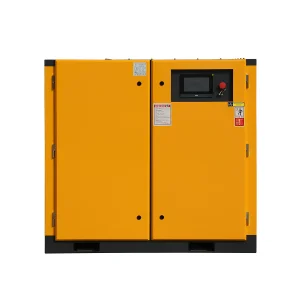
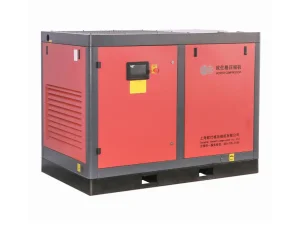
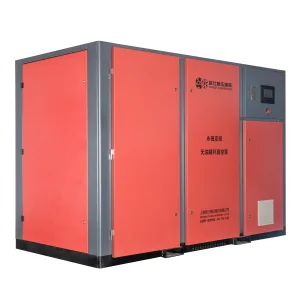
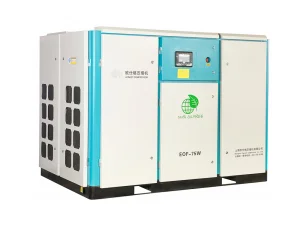
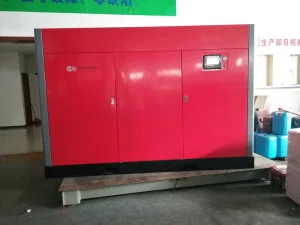
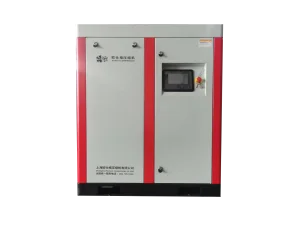
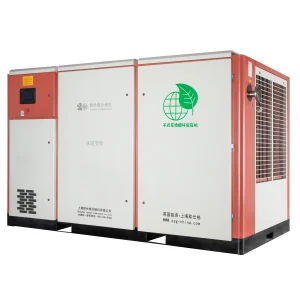
Leading global manufacturers are retiring legacy oil-flooded machinery in favor of direct oil free screw air compressor units. Certified to ISO 8573-1 Class 0, these machines physically separate compression cavities from lubrication circuits, eliminating contamination risks, downstream filter disposal costs, and pressure-drop energy penalties.
Total Cost of Ownership (TCO): Demasking the Real Costs of Compressed Air
A frequent misconception during procurement is that equipment capital expenditure (CAPEX) dominates the purchase. A holistic lifecycle calculation reveals a different reality over a 10-year operating horizon:
Because electricity accounts for up to 80% of a compressor's lifetime cost, purchasing inefficient machines based on low initial price leads to higher total expenses within 24 months. Shanghai Honest Compressor integrates IE4/IE5 permanent magnet motors and precision rotor machining to ensure continuous volumetric efficiency and stable power savings.
Technological Paradigms: Dry-Type Twin-Screw vs. Water-Lubricated Systems
Choosing the right engineering configuration requires evaluating thermodynamic principles, duty cycles, operating pressures, and rotor cooling dynamics.
Dry-Type Two-Stage Rotary Screw Architecture
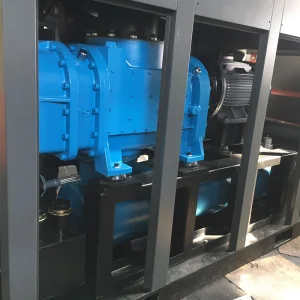
Dry-type oil-free screw compressors utilize high-precision synchronized timing gears to drive male and female rotors without physical contact. Because no lubricating liquid enters the compression chamber, the compression process is near-adiabatic and generates substantial heat.
- Two-Stage Staged Compression: Pressure ratios are divided across low-pressure and high-pressure stages with an intermediate intercooler, lowering thermal strain and saving up to 15% specific energy.
- Advanced Barrier Coatings: Rotors receive specialized food-grade polymer, MoS2, or PTFE surface coatings to protect clearances during high-heat operation.
- Carbon Ring Mechanical Seals: Multi-labyrinth venting seals backed by stainless steel atmospheric chambers prevent bearing lubricants from entering the air stream.
Optimal Fit: Large industrial base-loads (55 kW to 315 kW+), 24/7 continuous duty, petrochemical processing, and environments where water quality management is difficult.
Single-Stage Water-Lubricated Screw Architecture
Water-lubricated oil-free compressors inject purified reverse-osmosis (RO) water directly into the compression cavity. Water seals rotor clearances, absorbs thermal energy, and lubricates sliding contact points.
- Isothermal Compression Thermodynamics: Water absorbs heat directly during compression, keeping discharge temperatures below 50°C and matching the ideal Carnot cycle.
- Zero Hydrocarbons On-Site: The entire machine uses zero hydrocarbon oil, eliminating oil filters, oil-gas separation elements, and disposal costs.
- Corrosion-Resistant Metallurgy: Rotors and housing are precision-machined from stainless steel and advanced ceramic composites to prevent oxidation.
Optimal Fit: Light to medium manufacturing (7.5 kW to 75 kW), medical labs, hospital surgical lines, cleanroom automation, and sites with fluctuating load profiles.
| Evaluation Parameter | Dry-Type Two-Stage Screw | Water-Lubricated Single-Stage | Legacy Oil-Flooded + Carbon Filters |
|---|---|---|---|
| ISO 8573-1 Air Quality | Class 0 Certified (100% Dry) | Class 0 Certified (Pure Water) | Class 1 or 2 (Vapor Risk Remains) |
| Thermodynamic State | Staged Adiabatic with Intercooler | Near-Isothermal (<50°C Discharge) | Polytropic with Oil Quenching |
| Compression Efficiency | High across 55 kW - 315 kW sizes | High across 7.5 kW - 75 kW sizes | Moderate (Degrades as filters saturate) |
| Maintenance Overhead | Gearbox oil & air filter replacements | Water filtration & periodic seal checks | High (Oil filters, oil drums, separators) |
| Condensate Treatment | Standard clean water disposal | Clean water recycling loop | Hazardous chemical waste handling |
Mission-Critical Industrial Applications & Deployment
Where zero hydrocarbon presence is required to protect processes, products, and operational safety.
Semiconductor & Electronics
Wafer fabrication, PCB surface mounting, and photolithography require ISO 8573-1 Class 0 air. Hydrocarbon particulates cause wafer hazing, disrupt copper deposition, and reduce microchip yield rates. Clean air is also critical for optical lens cleaning and precision pneumatic indexing.
Pharmaceutical & Biotechnology
In sterile fermentation, tablet coating, and aseptic vial filling, air comes into direct contact with the active product. Oil traces can kill microbial cultures, ruin active pharmaceutical ingredients (APIs), and cause regulatory non-compliance during FDA or EMA quality audits.
Food, Beverage & Dairy Processing
Direct air contact occurs during PET blow molding, dry food conveying, sorting, and sterile packaging. Oil-free screw compressors eliminate product recalls, discoloration, and taste alterations, helping facilities maintain strict HACCP, BRCGS, and ISO 22000 hygiene certifications.
Lithium-Ion Battery Gigafactories
Battery cell manufacturing demands ultra-dry, oil-free conditions (dew points down to -40°C or -70°C). Any oil residue on aluminum and copper current collectors impairs electrolyte wetting, causing internal resistance anomalies and long-term thermal runaway hazards in electric vehicles.
Automotive Robotic Paint Application
In modern automotive paint shops, compressed air atomizes high-solid and waterborne clearcoats. Even minuscule hydrocarbon particles (0.1 ppm) can cause surface defects like cratering and fisheyes, requiring expensive panel repaints and disrupting assembly schedules.
Chemical, LNG & Industrial Gases
For catalyst fluidization, control valve actuation in explosive atmospheres, and cryogenics, compressors must run continuously without oil-induced gumming. Explosion-proof ATEX/IECEx packages operate safely in hazardous Zone 1 and Zone 2 environments.
Engineering for Cross-Border Integration & Global Compliance
Exporting industrial machinery requires adapting electrical, structural, and thermodynamic configurations to local regional standards.
Multi-Voltage & Frequency Support:
Custom motor windings and control inverters built for 380V/50Hz, 400V/50Hz (Europe/Asia), 415V/50Hz (UK/Oceania), and 460V/480V/60Hz (Americas). Machines start smoothly and maintain full torque under local grid variations.
Pressure Vessel & Safety Accreditations:
Intercoolers, moisture separators, and internal buffer vessels are certified to CE-PED (Europe), ASME Section VIII Div 1 (Americas), DOSH (Malaysia), and MOM (Singapore) for prompt customs and site inspection sign-off.
Tropicalization & Harsh Environments:
Heavy-duty cooling systems, IP55/IP65 electrical enclosures, anti-corrosive radiator coatings, and pre-filtration panels maintain continuous operation in ambient temperatures up to +50°C and humid coastal environments.
Factory Infrastructure: Jiading District, Shanghai
Operating from a 50,000 m² facility with British engineering heritage dating back to 2004, Shanghai Honest Compressor Co., Ltd. (OSG Compressor) pairs precision European rotor designs with automated modern manufacturing.
Every compressor undergoes multi-hour continuous run-in tests before crating. Computerized test benches measure free air delivery (FAD) per ISO 1217 Annex C/E, thermal stability, rotor vibration levels, and electrical harmonics.
Technology Roadmap: Intelligent Compression & Decarbonization
How ongoing developments in digital telemetry, materials science, and heat recovery are shaping modern compressed air systems.
IIoT Cloud & Predictive Maintenance
Next-gen controllers feature native 4G/5G and Ethernet telemetry. Edge-computing microchips continuously track high-frequency bearing vibration, pressure dew points, and inter-stage temperatures. Cloud-based predictive models alert plant technicians to rotor wear or filter loading before unscheduled downtime occurs.
Waste Heat Recovery (Recuperators)
Up to 90% of electrical energy consumed by screw compressors converts directly into thermal heat. Integrated liquid-to-liquid heat recovery exchangers tap into oil-free cooling loops, returning clean process hot water (65°C to 80°C) for boiler preheating, sanitation, or space heating—helping plants reach Scope 1 and Scope 2 carbon reduction goals.
Ultra-High Efficiency Rotor Profiles
Using computational fluid dynamics (CFD) and finite element analysis (FEA), our R&D engineering center continues to refine asymmetric 5:6 lobe geometries. Reduced internal backflow and tighter running tolerances allow air ends to deliver greater free air delivery per kilowatt (kW/(m³/min)).
Frequently Asked Technical Questions
Engineering, installation, and sizing considerations addressed by our compressor application specialists.
What differentiates ISO 8573-1 Class 0 from "Technically Oil-Free" compressed air?
How does a Permanent Magnet Variable Speed Drive (PM VFD) lower electricity consumption?
What water supply quality is required for water-lubricated screw air compressors?
Why choose a two-stage dry screw compressor over a single-stage dry screw?
Can your factory accommodate international electrical voltages and custom OEM/ODM packaging?
What routine maintenance is required for a dry-type oil-free screw compressor?
How do you maintain reliable cooling during continuous 24/7 industrial duty?
Explore Specialized Screw Machinery & Industrial Blowers
From explosion-proof integrated skids to high-vacuum dry screw pumps and energy-saving blowers, browse our full industrial equipment selection.