


1. Executive Summary & Global Market Dynamics of Portable Diesel Air Compressors
In the contemporary industrial ecosystem, portable diesel air compressors represent the backbone of off-grid mechanical power generation across mining, heavy civil engineering, oil and gas exploration, deep geothermal drilling, and municipal trenchless utility restoration. Unlike stationary electric motor-driven compressor packages anchored inside factory utility rooms, portable diesel-driven rotary screw units operate under severe environmental constraints—enduring ambient temperatures ranging from -25°C in arctic sub-grades to +52°C in hyper-arid desert terrains, while operating continuously under heavy particulate contamination.
The global demand for portable diesel air compressors engineered in China has experienced a paradigm shift over the past decade. Historically regarded primarily as cost-effective alternatives to European and North American legacy OEMs, leading Chinese compressor manufacturers and specialized supplier factories have evolved into global technology pioneers. By integrating high-efficiency SAP/GHH rotor profiles, Tier 4 Final / EU Stage V compliant diesel powertrains (including Cummins, Weichai, Yuchai, and Deutz platforms), intelligent micro-processor telematics, and multi-stage oil-air separation systems, top-tier Chinese suppliers now deliver unmatched specific power consumption rates (kW per m³/min of Free Air Delivery) and lifetime operating durability.
2. Industry Ecosystem & China’s Manufacturing Supply Chain Advantage
China's dominance as a premier exporter of portable diesel air compressors is grounded in a highly consolidated, vertically integrated manufacturing matrix concentrated in industrial hubs like Shanghai, Zhejiang, and Shandong. This localized ecosystem enables rapid R&D iteration, precise quality control, and streamlined component sourcing. Key structural drivers behind China's competitive leadership include:
Precision Rotor Milling
Advanced 5-axis CNC thread grinders (such as KAPP and Klingelnberg) manufacture asymmetric male-female rotor pairs with micron-level tolerances, minimizing internal blow-by leakage.
Tier-1 Diesel Integration
Direct factory partnerships with world-class diesel engine providers enable seamlessly tuned electronic engine control units (ECUs) synchronized with compressor intake valves.
Heavy-Duty Chassis Fabrication
Robotic welding of high-tensile steel frames with hot-dip galvanizing or electrostatic powder coating prevents structural oxidation in marine and high-salinity offshore environments.
3. Core Technical Architecture & Thermodynamics of Diesel Screw Units
Understanding the thermodynamic mechanics of portable diesel rotary screw air compressors requires examining the relationship between engine speed modulation, air-end displacement, and system discharge pressure. A portable diesel compressor system functions through a closed-loop mechanical interaction:
3.1 Asymmetric Rotor Profile Geometry
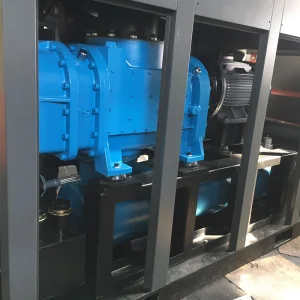
The heart of any diesel air compressor is the rotary screw air-end. Modern Chinese factories employ a 5:6 tooth ratio (5 male lobes driving 6 female grooves). This specific configuration ensures continuous contact along the sealing line, reducing internal backflow gas slippage while maintaining lower pitch-line speeds. Lower rotational speeds mean decreased friction losses, reduced heat generation, and prolonged SKF/TIMKEN tapered roller bearing life (target design life exceeding 100,000 continuous operation hours).
3.2 Stepless Automatic Capacity Control (0–100% Load Regulating System)
To match variable pneumatic tool consumption on job sites, Chinese manufacturers equip units with proportional stepless control systems. When air demand drops, the system simultaneously adjusts two variables:
- Intake Throttle Modulation: The butterfly or poppet intake valve throttles back to restrict incoming atmospheric air volume.
- Engine Speed De-acceleration: The diesel engine ECU receives a pneumatic or Electronic CAN-bus signal, dropping engine RPM from maximum rated power (e.g., 2,200 RPM) down to idle speed (e.g., 1,300 RPM).
This dual-action regulation prevents unnecessary relief valve blow-offs, conserving fuel during non-productive intervals.
3.3 Multi-Stage Air-Oil Separation & Filtration Mechanics
Air discharge from the screw rotor is saturated with atomized cooling oil used for sealing, lubrication, and thermal dissipation. Chinese export-grade portable units utilize a multi-stage centrifugal and coalescing separation canopy:
- Primary Centrifugal Separation: The high-velocity mixture strikes the inner tank wall, dropping 95% of bulk oil droplets into the sump through gravitational vortex action.
- Secondary Coalescing Filtration: The air passes through deep-bed synthetic microfiber filter elements, capturing sub-micron oil mists and reducing carry-over oil content to below 2 ppm (parts per million).
| Technical Parameter | Low/Medium Pressure Series | High Pressure Deep Well Series | Ultra-High Pressure Geothermal Series |
|---|---|---|---|
| Discharge Pressure (Bar / PSI) | 7.0 – 12.0 Bar (100 – 175 PSI) | 17.0 – 25.0 Bar (246 – 362 PSI) | 30.0 – 35.0 Bar (435 – 507 PSI) |
| Free Air Delivery (FAD - m³/min) | 5.0 – 18.5 m³/min | 21.0 – 34.0 m³/min | 35.0 – 42.0 m³/min |
| Compression Stages | Single-Stage Oil-Injected Screw | Two-Stage Intercooled Screw | Two-Stage High-Pressure Screw |
| Diesel Engine Power (kW / HP) | 37 kW – 132 kW (50 – 180 HP) | 194 kW – 390 kW (260 – 525 HP) | 410 kW – 560 kW (550 – 750 HP) |
| Typical Site Applications | Sandblasting, Jackhammers, Cable Blowing | DTH Water Well Drilling, Anchoring | Deep Oil/Gas Drilling, Piling, Geothermal |
4. Localized Application Scenarios & Real-World Field Implementations
The operational versatility of portable diesel air compressors allows them to function in diverse sectors. China suppliers custom-engineer package configurations to fulfill localized operational mandates:
Deep Water Well & Geothermal Drilling
Requirement: Extremely high pressure (25–35 Bar) combined with large volumetric delivery (30+ m³/min) to power Down-The-Hole (DTH) hammers and clear heavy rock cuttings out of 300+ meter boreholes.
Solution: Two-stage portable diesel units equipped with dual air filters, heavy-duty oil coolers, and fast blow-down valves to accelerate drilling cycles in granite bedrock.
Open-Pit Mining & Stone Quarrying
Requirement: Continuous 24/7 blast-hole penetration in severe ambient dust environments.
Solution: Heavy-duty skid-mounted or four-wheel towed diesel compressors with multi-stage heavy dust pre-cleaners (Donaldson TopSpin systems) and reinforced undercarriages.
Pipeline Pressure Testing & Purging
Requirement: High FAD output with ultra-dry, oil-free or low-oil air stream to verify long-distance cross-country oil/gas pipeline integrity.
Solution: Trailer-mounted diesel screw units integrated with built-in aftercoolers, water separators, and cold-weather start kits for high-altitude mountain pipelines.
Municipal Tunnelling & Concrete Shotcreting
Requirement: Sound-attenuated acoustic canopy (low noise level <75 dB(A) at 7 meters) for urban construction work compliance.
Solution: Whisper-quiet portable diesel units featuring fire-retardant sound-absorbing foam lining, compact chassis dimensions for tight shaft maneuvering, and central drain ports.
5. Technology Roadmap & Future Outlook (2025–2030)
The mobile air compression industry is undergoing rapid technological transformation. Forward-looking China diesel air compressor factories are investing heavily in next-generation R&D pathways:
5.1 Diesel-Electric Dual-Drive (Hybrid Powertrains)
Recognizing the transition toward green site electrification, cutting-edge Chinese OEMs offer dual-drive portable compressors. On job sites with available grid power, the machine runs on a high-efficiency electric motor. When operating in remote locations off-grid, the diesel engine automatically engages. This hybrid capability cuts operating costs by up to 60% on grid-connected sites while retaining 100% field mobility.
5.2 IoT Telematics & 5G Predictive Maintenance Fleet Management
Modern Chinese portable diesel compressors come equipped with cloud-connected IoT controller modules. Fleet managers can monitor critical parameters in real-time via smartphone apps or web dashboards: GPS position, engine oil pressure, coolant temperature, compressor discharge temperature, real-time FAD output, fuel consumption rates, and filter clog alerts. Machine-learning algorithms analyze vibration data to forecast bearing wear before catastrophic field failure occurs.
5.3 Ultra-Low Emission Engine Integration (EU Stage V & EPA Tier 4 Final)
To meet stringent environmental regulations in North American and European markets, top China factories incorporate advanced exhaust aftertreatment systems—including Selective Catalytic Reduction (SCR), Diesel Particulate Filters (DPF), and Diesel Oxidation Catalysts (DOC)—ensuring compliance with global zero-smog standards.
6. Macro Industry Solutions & Custom Sizing Matrix
Selecting the optimal portable diesel air compressor requires balancing air volume (FAD) with working pressure to prevent equipment under-performance or unnecessary capital expenditure. Below is an engineering recommendation matrix established by lead OEMs:
Note: Operating at altitudes above 1,500 meters requires a de-rating factor of approximately 3% per 300 meters for naturally aspirated diesel engines, or 1% per 300 meters for turbocharged engines.
For rental companies and large EPC contract operators, standardization of chassis components, filters, and operational controllers across horsepower classes significantly reduces spare parts inventory overhead and simplifies operator field training.
7. Enterprise Sourcing & Factory Selection Guidelines (E-E-A-T Framework)
When vetting China portable diesel air compressor suppliers and manufacturing facilities, international procurement buyers should evaluate candidates against four critical criteria:
- Quality Management System & Pressure Vessel Compliance: Verify ISO9001 certification alongside specialized pressure vessel approvals such as CE (PED 2014/68/EU), ASME Code Stamp certification, or local national registration for air-oil separator tanks.
- Factory Testing Infrastructure (ISO 1217 Annex C Standards): Ensure the manufacturer operates a certified nozzle test bench capable of measuring actual Free Air Delivery (FAD) under full thermal load, rather than relying on theoretical rotor displacement calculations.
- Global After-Sales Parts Support: Confirm that engine components (filters, belts, injectors) are cross-compatible with global engine dealer networks (Cummins/Deutz), and that the compressor factory maintains a 48-hour dispatch guarantee for core screw airend spares.
- Custom OEM/ODM Engineering Flexibility: Review factory capabilities for custom voltage controller mapping, tropicalized cooling radiator packages, skid versus trailer towing hitches (ball vs. pintle eye), and custom brand livery.