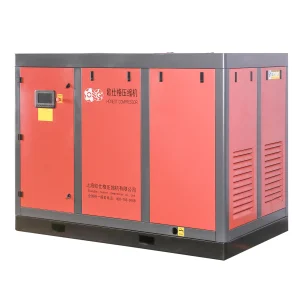
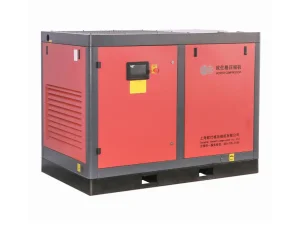
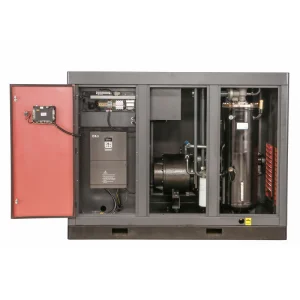
Featured Industrial Screw Compressors & Vacuum Systems
Explore our top-tier OEM engineering lineup engineered for maximum specific power efficiency, extreme durability, and continuous 24/7 heavy industrial reliability.


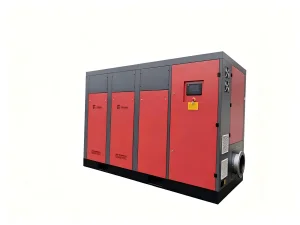




OEM Belt Drive Air Compressor Engineering Architecture & Design Principles
A comprehensive technical analysis of belt-driven rotary screw compressor mechanics, torque dynamics, and thermal management for industrial original equipment manufacturing.
1. Belt Drive vs. Direct Drive: Mechanical Mechanics & OEM Modularity
In modern industrial compressed air system design, selecting the optimal power transmission architecture between the prime mover (electric motor) and the rotary screw air end represents a critical decision for OEM machinery builders. While direct-drive setups link the motor shaft directly to the male rotor via a flexible coupling or gear drive, belt drive air compressors provide unparalleled modular flexibility, economical repairability, and operational tuning agility across small-to-medium power outputs (7.5 kW to 45 kW).
From an OEM manufacturing perspective, belt drive systems utilize heavy-duty Poly-V (ribbed) or wedge belt profiles that allow exact pitch-diameter tuning of drive pulleys. This engineering parameter enables factories to match specific air-end rotative speeds (RPM) to various operating pressure targets (e.g., 7 bar, 8 bar, 10 bar, 13 bar) without altering motor pole counts or redesigning internal gearbox castings.
Information Gain Insight: Advanced poly-V belt transmission systems achieve up to 98.5% torque efficiency when correctly tensioned with automatic spring-loaded motor baseplates. They act as mechanical shock absorbers during high-load startup cycles, isolating the air-end bearings from motor shaft harmonics and voltage spikes.
2. Poly-V Belt Power Transmission & Pulley Ratio Engineering
The core advantage of high-spec belt drive screw compressors lies in friction dynamics and contact area optimization. Unlike older V-belt configurations prone to wedging friction losses and thermal degradation, micro-ribbed Poly-V belts offer multiple longitudinal grooves that mesh precisely with machined pulley sheaves.
- Reduced Linear Velocity Loss: Poly-V belts maintain high flexural stress endurance and lower centrifugal tension, permitting peripheral belt speeds up to 40 m/s without belt slippage.
- Custom Speed Ratios for Variable Discharge Pressures: OEMs can fine-tune Free Air Delivery (FAD) per ISO 1217 Annex C simply by changing pulley pitch diameters ($D_1/D_2 = n_2/n_1$), ensuring maximum thermodynamic output per kW consumed.
- Extended Bearing Wear Life: Shock loads generated during sudden unloads or rapid cyclic pressure drops are dampended mechanically by elastomeric belt deflection, preventing micro-pitting on roller bearing races.
| Drive Parameter | High-Torque Belt Drive System | Direct Gear Drive System | Direct Coupling Drive System |
|---|---|---|---|
| Pressure Flexibility | Extreme (Simple Pulley Change) | Low (Requires Gear Set Change) | Fixed (Tied to Motor RPM) |
| Vibration Damping | Superior (Elastomeric Isolation) | Moderate (Metal Mesh Transmission) | Dependent on Flexible Element |
| Field Maintenance Cost | Low (Rapid Belt Replacement) | High (Requires Gear Alignment) | Moderate (Coupling Insert Check) |
| CAPEX for OEM Assembly | Highly Cost-Effective | Capital Intensive | Moderate-High |
| Transmission Efficiency | 97.5% - 98.5% | 98.0% - 99.0% | 99.2% - 99.5% |
3. Automatic Belt Tensioning Mechanisms & Structural Shock Isolation
A frequent challenge historically associated with belt-driven machinery was premature belt elongation and manual tension drift, which led to slippage, heat generation, and volumetric efficiency decay. Modern OEM factories solve this issue through dynamic, self-adjusting motor mounting bases.
Using a heavy-duty pivot point and adjustable spring tension bolt or gas-strut assembly, the electric motor's weight and reaction torque continuously maintain ideal belt tension regardless of ambient thermal expansion or belt wear. This eliminates routine manual retensioning shutdowns and ensures stable specific power consumption ($kW / (m^3/min)$) across thousands of hours of uninterrupted operation.
Localized Application Scenarios & Global Industry Deployment
Field-proven performance across harsh ambient conditions, regional manufacturing hubs, and specialized commercial operations.
Southeast Asia & Tropical Manufacturing
Operates continuously in high-ambient humidity (>90% RH) and hot environments up to 45°C. Heavy-duty air intake filtration and high-viscosity synthetic lubricant circuits protect internal rotors against moisture condensation and thermal degradation in textile mills, furniture plants, and rubber processing workshops across Vietnam, Indonesia, and Thailand.
Automotive Repair & Spray Booths
Delivers clean, pulse-free compressed air for robotic paint spraying, pneumatic wrenches, and body shop sanding in North American and European automotive facilities. Integrated air treatment systems (coalescing filtration + refrigerated air dryers) eliminate moisture and oil droplets down to 0.01 micron.
Mining, Quarrying & Construction
Enclosed in IP54 / IP55 powder-coated heavy-gauge steel cabinets, belt drive units handle high ambient dust concentrations in stone quarries, cement facilities, and regional mining operations. Mechanical belt drive isolates sensitive motor components from intense shock vibrations caused by heavy rock crushers.
Technology Roadmap & Future Engineering Innovations (2025–2030)
Pioneering smart diagnostics, next-gen materials, and hybrid variable-speed powertrains to drive next-decade energy efficiency.
1. AI-Driven IoT Belt Health & Tension Diagnostics
Future iterations of OEM screw compressors incorporate optical laser reflection sensors and acoustic frequency analyzers mounted inside the belt canopy. Connected directly to the main PLC logic controller via Modbus RS485 or IoT cloud gateway, these systems monitor belt frequency vibration profiles in real-time.
Any loss of belt tension, surface micro-cracking, or pulley misalignment triggers automated predictive maintenance alerts to shop floor technicians long before catastrophic mechanical failure occurs.
2. Carbon Fiber Reinforced Elastomer Belts
By replacing traditional polyester cord tensile members with embedded carbon fiber cords, next-generation industrial Poly-V belts offer zero stretch over their operating life span. This innovation allows belt service intervals to jump from 4,000 hours to over 12,000 hours, matching the routine oil filter and oil separator change intervals of premium direct-drive systems while retaining all modular OEM cost benefits.
China Supply Chain Resilience & Shanghai Manufacturing Advantage
Leveraging deep industrial clusters, precision machining, and agile OEM factory customization to deliver global competitive superiority.
Precision Machining Ecosystem
Situated in Jiading District, Shanghai, our plant leverages a complete supply chain cluster within a 50 km radius—from high-grade grey iron foundry foundries for air-end casings to premium German rotor grinding machines (Kapp/Holroyd) ensuring sub-micron profile accuracy on 5:6 asymmetrical rotor profiles.
Comprehensive Turnkey Customization
We empower international brand owners, engineering contractors, and private-label distributors with custom skid sizes, dual voltage/frequency motors (220V/380V/400V/415V/440V/460V at 50Hz or 60Hz), tailored PLC software languages, custom color powder coating, and localized OEM branding packages.
Unmatched Production Throughput
With 4 automated assembly lines and dedicated dynamic load testing bays, our plant maintains a monthly production capacity exceeding 1,500 units. Rapid component staging cuts standard OEM delivery lead times from 8 weeks down to 14 business days.
Global Market Status & Total Cost of Ownership (TCO) Economics
Optimizing lifetime expenditure through intelligent CAPEX/OPEX balance and high specific energy performance.
Over a standard 10-year operating life of an industrial rotary screw air compressor, energy consumption (electricity cost) accounts for approximately 75% to 80% of Total Cost of Ownership (TCO), while initial equipment capital expenditure (CAPEX) represents merely 10% to 15%, with routine maintenance making up the rest. Belt drive screw compressors offer an exceptional economic compromise for small-to-midsize industrial facilities.
Strategic Financial takeaway: For factories running 1-2 shifts daily (2,000 to 4,000 operational hours per year), an OEM belt-driven screw air compressor delivers the lowest upfront CAPEX while maintaining 98%+ specific energy efficiency, offering payback periods under 8 months compared to premium geared drive alternatives.
Localized Support, Quality Certification & International Compliance
Ensuring complete regulatory approval and seamless field integration across North America, Europe, Latin America, and Asia-Pacific.
Safety & Electrical Approvals
All factory units hold official CE certification (MD 2006/42/EC & LVD 2014/35/EU), ISO 9001:2015 quality control compliance, and optional ASME / CRN pressure vessel approvals for North American export requirements.
Dual-Voltage Control Flexibility
Equipped with intelligent PLC microprocessors featuring multi-language user interfaces (English, Spanish, French, Russian, Arabic), phase sequence protection, overload auto-shutdown, and remote RS485 telemetry.
Rapid Spare Parts Fulfillment
Standardized belt sizes (Gates, Optibelt, Continental) and universal spin-on oil filter cartridges ensure off-the-shelf component availability anywhere in the world, minimizing potential production downtime.
Frequently Asked Questions (FAQ) – Technical & OEM Sizing Guide
Detailed engineering answers to assist technical buyers, OEMs, and plant managers in making informed machinery decisions.
1. What is the typical service lifespan of a Poly-V belt in an OEM industrial screw compressor?
2. How does a belt drive compressor handle frequent load/unload cycling compared to VFD drives?
3. Can we customize the discharge pressure of an OEM belt drive compressor post-purchase?
4. How does belt alignment impact bearing life and energy efficiency?
5. What customization options are available for private-label OEM buyers?
6. Are belt drive screw air compressors suitable for 24/7 continuous duty?
7. What is the difference between single-stage belt drive and two-stage pressure screw compressors?
8. How do I request a formal technical proposal or factory audit?
Additional OEM Industrial Air & Vacuum Equipment Lineup
Complete your compressed air station with high-precision micro-oil pumps, two-stage heavy chemical compressors, and energy-saving VFD screw blowers.