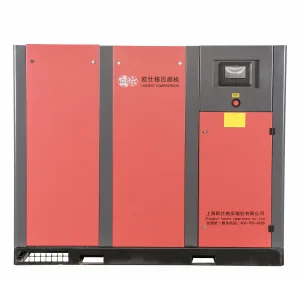
Featured Industrial Rotary Compressors & Vacuums
Engineered for low specific power consumption, extreme thermal stability, and low lifecycle operating expenses.
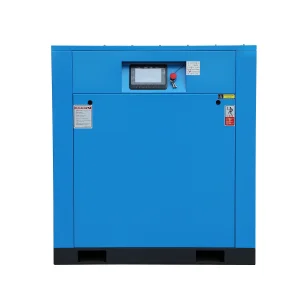
OEM VFD screw air compressor 0.7-1.25mpa Energy Saving up to 30% Manufacturers, Exporter
Explore Model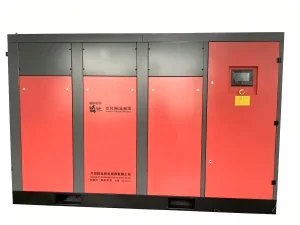
China EGV-132A-140 Oil-Free Permanent Magnet VFD Screw Blower Manufacturers, Exporters
Explore Model
OEM 4-in-1 Explosion-Proof Air Compressor | 7.5-22kW Permanent Magnet Integrated Unit Factory, Exporters
Explore Model
China Smart energy saving water lubricating 100% oil free screw air compressor with fixed speed or VSDPM Manufacturers, Exporter
Explore Model
ODM Industrial Screw Vacuum Pump Oil Free High Efficiency Vacuum Pump for Semiconductor & Chemical Industry Manufacturer, Factories
Explore Model
OEM Industrial Screw Vacuum Pumps – Oil-Injected (0.35 mbar) & Oil-Free (20–80 kPa) Series, 5.5–110 kW Supplier, Exporter
Explore Model
China 30kw Industrial Oil Free Vsd Screw Air Blower Vacuum Pump With Plc Inverter Pm Motor oil free screw blower Supplier, Suppliers
Explore Model
ODM IP55/54 55KW 75HP Factory Price Two Stage Industrial Screw Type Air Compressor Machine Factories, Exporters
Explore ModelThe Strategic Role of Oil-Flooded Rotary Screw Compressors in Modern Industry
Oil-injected rotary screw air compressors generate over 80% of all utility-grade compressed air consumed across heavy fabrication, chemical processing, automotive assembly, and mineral extraction worldwide.
In modern industrial facilities, compressed air is universally recognized as the fourth industrial utility, alongside water, electricity, and natural gas. Among positive displacement machinery, the oil-flooded rotary screw air compressor (also termed oil-injected screw compressor) maintains an uncontested dominance in baseline pneumatic power delivery. Unlike dynamic compressors or reciprocating pistons, twin-screw mechanisms deliver continuous, pulsation-free air discharge characterized by exceptional volumetric efficiency, mechanical longevity, and predictable operational uptime.
The global commercial landscape is witnessing an accelerated technological transition driven by global net-zero mandates, escalating grid electricity tariffs, and rigorous energy management protocols under ISO 50001. Industrial plants can no longer tolerate legacy fixed-speed units operating on inefficient load/unload cycles—which waste up to 30% to 40% of their total power during unloaded idling. Instead, engineering procurement teams in North America, Europe, Southeast Asia, and the Middle East increasingly specify Permanent Magnet Variable Frequency Drive (PM VFD) and two-stage compression architectures designed to minimize free air delivery (FAD) specific power (measured in kW/(m³/min)).
Thermodynamic Sealing & Isothermal Approach
Injected synthetic lubricant forms a hydrodynamic film along rotor meshing lines and radial clearances, eliminating internal back-leakage while absorbing heat directly at generation. This achieves near-isothermal compression with significantly reduced specific power.
Uninterrupted 24/7 Heavy Industrial Duty
Engineered for 100% continuous duty cycles without thermal throttling. Precision tapered roller bearings and hydrodynamic fluid damping cushion dynamic radial and axial thrust loads across high-pressure differential regimes.
ISO 8573-1 Residual Purity Standards
Through advanced three-stage air-oil separation featuring cyclonic pre-separation, gravity settling, and deep-bed borosilicate coalescing elements, oil carry-over is consistently suppressed below 1 to 3 ppm for downstream instrument air compatibility.
Rotor Dynamics, Lubrication Physics & Electromechanical Integration
A granular technical examination of twin-screw thermodynamic engineering, precision CNC profile grinding, and variable-speed synchronous permanent magnet motor systems.
The core operating efficiency of an oil-flooded rotary screw air compressor hinges on the geometrical profile of its twin helical rotors. Honest Compressor employs an optimized 5:6 asymmetric tooth profile (5 male driving lobes to 6 female driven flutes). Compared with obsolete 4:6 symmetrical profiles, the 5:6 configuration drastically reduces the transverse blowhole area, minimizes internal slippage paths, and optimizes rotor tooth root rigidity. In our Jiading, Shanghai manufacturing center, rotors are milled on ultra-precision German rotor grinding centers, holding micrometric manufacturing tolerances below 5 microns.
During the compression phase, oil is injected directly into the compression chamber without an auxiliary oil pump, relying purely on the internal pressure gradient established between the air-oil separator tank and the airend suction inlet. This injected lubricant performs three indispensable functions:
1. Hydrodynamic Sealing: Closes the clearance gap between the intermeshing male/female rotors and the housing bore, suppressing high-pressure back-leakage to suction.
2. Isothermal Heat Quenching: Compressing atmospheric air from 0.1 MPa to 0.8–1.3 MPa generates extreme polytropic heat. Injected oil absorbs over 80% of this heat instantaneously, maintaining discharge air below 90°C and averting thermal rotor degradation.
3. Mechanical Rotor Film Lubrication: Directly drives the female rotor via a fluid cushion, eliminating metallic contact between helical flanks, dampening acoustic vibration, and protecting precision bearings.
| Performance Parameter | Legacy Fixed-Speed Single Stage | Honest OEM PM VFD Single Stage | Honest OEM Dual-Stage PM VFD |
|---|---|---|---|
| Drive Mechanism | Induction Motor (IE2/IE3) + Belt/Gear | Direct-Coupled PM Motor (IE4/IE5) | Twin Direct-Coupled PM Motors |
| Turndown Ratio (Capacity Mod.) | 100% or 0% (Unloaded Idling) | 25% – 100% Linear Speed Mod. | 20% – 100% Inter-Stage Speed Mod. |
| Average Specific Power (0.8 MPa) | 7.2 – 8.1 kW / (m³/min) | 6.1 – 6.6 kW / (m³/min) | 5.4 – 5.9 kW / (m³/min) |
| Air Pressure Stability Band | ±0.15 to ±0.2 MPa (Wide Delta) | ±0.01 MPa (Constant Pressure) | ±0.01 MPa (Constant Pressure) |
| Unloaded Energy Wastage | Up to 35% of Nominal Motor Rating | 0% (Instant Soft Start / Stop) | 0% (Intelligent Sleep / Wake) |
| Bearing Service Life (L10h) | 40,000 – 50,000 Operating Hours | 60,000 – 80,000 Operating Hours | 100,000+ Operating Hours |
Why Global Air System Exporters Partner with Our Shanghai Factory
Integrating British engineering standards established in 2004 with the unmatched industrial scale, supply chain density, and cost efficiencies of our Shanghai production plant.
Operating from our 50,000 m² modern manufacturing headquarters in Jiading District, Shanghai, Shanghai Honest Compressor Co., Ltd. offers a unique value proposition to global compressor distributors, engineering, procurement, and construction (EPC) contractors, and private-label OEMs. China’s Yangtze River Delta industrial belt provides the world’s most dense cluster of precision mechanical machining, electrical insulation, pressure vessel fabrication, and power electronics manufacturing. By fully internalizing core airend machining, structural casing fabrication, robotic wiring, and automated run-in testing, we reduce manufacturing lead times to 15–25 business days while delivering capital expenditure savings of 30% to 45% compared to Western European machinery of identical technical output.
British Engineering Pedigree
Founded as a British-owned manufacturer in 2004, our production and quality management systems combine UK thermodynamic design tolerances with rigorous ISO 9001 certified execution.
Global Electrical Compliance
Turnkey OEM electrical integration supporting international grid configurations: 220V, 380V, 400V, 415V, 460V, and 575V at 50Hz/60Hz, compliant with CE-MD, CE-LVD, and UL 508A safety codes.
Complete Pressure Vessel Approvals
Air-oil separators and integrated receiver tanks fully certified according to European CE-PED (2014/68/EU), ASME Section VIII Div. 1, and national pressure safety standards.
White-Label Customization
Bespoke sheet-metal canopy styling, industrial powder coating in RAL custom palettes, client firmware branding, and localized multilingual PLC touchscreens (English, Spanish, Arabic, Russian).
Sector-Specific Deployments: Demanding Field Scenarios
How our heavy-duty oil-flooded rotary systems excel in harsh ambient conditions, fluctuating pneumatic demands, and hazardous operating environments.
Automotive Stamping & Robotic Assembly
Automotive assembly facilities endure dramatic air consumption swings as automated pneumatic clamps, paint-shop robots, and mechanical presses cycle rapidly. Our PM VFD systems respond in milliseconds to pressure dips, stabilizing ring-main line pressure at ±0.01 MPa and eliminating stamping downtime.
Petrochemical & Heavy Chemical Refining
Chemical processing plants feature volatile ambient atmospheres containing trace airborne hydrocarbons. Honest’s integrated explosion-proof series (certified Ex d IIB T4 / IIC) provides sealed flameproof enclosures, heavy-duty antistatic drive linkages, and sparkless intake safety for Zone 1 and Zone 2 environments.
Textile Weaving & High-Speed Air-Jet Looms
Air-jet weaving consumes vast volumes of continuous medium-pressure air (0.5 to 0.7 MPa). With textile plants operating 8,400 hours annually, our dual-stage oil-flooded compressors reduce specific energy by up to 15%, slashing hundreds of thousands of dollars in facility utility expenses.
Cement, Aggregates & Open-Pit Mining
Pneumatic conveying of bulk powdery cement or pulverised ores demands robust air units resilient against heavy airborne dust. Equipped with heavy-duty two-stage centrifugal pre-filtration and nanofiber media filters, our compressors keep intake particulates well under 1 micron.
High-Pressure Laser Cutting & Sheet Metal
Modern fiber laser cutting systems utilize high-pressure air (1.6 to 2.5 MPa) as an affordable alternative to nitrogen assist gas. Our booster-integrated oil-flooded packages deliver high-pressure, ultra-dry, particle-free compressed air that produces mirror-finish stainless steel cut edges.
Centralized Vacuum & Degassing Systems
Leveraging screw compression mechanics in reverse, our oil-injected and dry screw vacuum pumps replace inefficient liquid ring and rotary vane units across pharmaceutical vacuum drying, electronics degasification, and automated packaging pick-and-place lines.
Technological Horizons: Smart IIoT, Two-Stage Compression & Waste Heat Recovery
The modern air compressor is transitioning from an isolated mechanical utility into an intelligent, digitized cyber-physical asset integrated directly into factory automation.
Three primary technological frontiers are reshaping the global oil-flooded rotary screw air compressor landscape:
Two-Stage Isobaric Compression
Splitting total compression across two independent airends reduces the compression ratio per stage from ~8:1 down to ~2.8:1. Incorporating intermediate oil-mist intercooling brings thermodynamic behavior remarkably close to ideal isothermal compression, slashing overall input energy by 12% to 18%.
Intelligent Cloud Telemetry & IIoT
Our integrated edge microcontrollers stream real-time operational data via 4G/5G and Modbus TCP/IP. Predictive analytics detect early bearing micro-vibrations, differential oil filter clogging, and cooling degradation before unplanned mechanical trips occur.
Thermally Coupled Heat Recovery
Over 94% of electrical energy fed into an air compressor converts into thermal dissipation. Honest Compressor integrates secondary plate-fin heat exchangers that recover up to 75% to 80% of heat into boiler feedwater or sanitary industrial hot water at 70°C without consuming additional fuel.
Total Cost of Ownership (TCO) & Sizing Selection Matrix
A transparent economic and thermodynamic evaluation framework to guide B2B plant engineers, facility directors, and procurement specialists.
A frequent error in industrial air system procurement is evaluating equipment predominantly by initial purchase cost. Over a standard 10-year operating horizon (operating 6,000 hours per year), the financial breakdown of an oil-flooded rotary screw air compressor reveals that electricity represents between 72% and 78% of the Total Cost of Ownership. Initial capital expenditure accounts for only 10% to 15%, while routine scheduled maintenance accounts for 10% to 12%. Specifying a compressor with inferior specific power (kW/(m³/min)) to save 20% on upfront capital typically inflicts six-figure electricity penalties over its lifecycle.
Volumetric Flow & Pressure Sizing
Determine total peak pneumatic demand in m³/min or CFM and add a 15% safety buffer for piping leakage. Operating at 0.1 MPa higher pressure than required increases energy consumption by approximately 7%. Correct pressure matching directly preserves utility budgets.
Demand Profile Analysis
For steady continuous baseload air demand, a fixed-speed single-stage or two-stage compressor offers peak efficiency at its sweet spot. For cyclical, multi-shift, or fluctuating pneumatic loads, a PM VFD compressor eliminates off-load idling and optimizes utility costs.
Downstream Quality Engineering
Pair the oil-flooded compressor with matched moisture separators, refrigerated air dryers (dew point +3°C), adsorption desiccant dryers (dew point -40°C), and activated carbon filtration towers to meet ISO 8573-1:2010 purity classes.
Frequently Asked Technical & Procurement Questions
In-depth answers curated by our senior application engineering team on oil-flooded screw air compressor design, operation, and international export.
Why is an oil-flooded screw air compressor often more energy-efficient than a dry oil-free compressor for general industrial applications?
In a dry oil-free screw compressor, no liquid lubricant enters the compression chamber. As a result, the compression process follows a steep polytropic/adiabatic curve, generating extreme temperatures (often exceeding 200°C) and demanding substantial mechanical shaft work. Furthermore, because dry rotors cannot touch, clearances are wider, permitting significant high-pressure slip-back to suction unless operated at very high rotational speeds.
In contrast, an oil-flooded compressor injects specially formulated synthetic oil directly into the compression pocket. The oil creates an impermeable fluid seal across clearances and directly absorbs the heat of compression. This brings the process close to an ideal isothermal compression curve, where the thermodynamic work required to compress air is minimized. For general industrial utilities where trace residual oil (<1–3 ppm) is easily removed by coalescing filtration, oil-flooded compressors deliver 15% to 25% superior specific power efficiency and substantially longer component lifespan.
How does Permanent Magnet Variable Frequency Drive (PM VFD) technology eliminate off-load idling power losses?
Standard fixed-speed compressors operate on a crude load/unload mechanism: when line pressure reaches its upper setpoint, the inlet suction valve chokes closed, but the large AC induction motor continues running at full RPM. During this unloaded idling phase, the machine consumes 30% to 45% of its rated electrical power without generating a single cubic meter of usable compressed air.
Honest’s PM VFD systems replace fixed-speed induction motors with synchronous Permanent Magnet motors driven by advanced vector inverters. The controller continuously monitors discharge line pressure with high-precision pressure transducers. As pneumatic demand decreases, the inverter reduces motor RPM in linear proportion to air consumption. If air consumption stops entirely, the motor safely shuts down into an intelligent standby sleep mode, drawing virtually zero wattage and re-accelerating smoothly upon demand without high inrush current spikes.
What causes oil carry-over in an oil-injected compressor, and how does Honest Compressor keep residual oil below 3 ppm?
Excessive oil carry-over in compressed air typically stems from poor mechanical separation geometry, torn or saturated separator filter elements, failed scavenger line check valves, or operating at excessively high discharge temperatures that vaporize lubricant.
Honest Compressor resolves this through a proven three-stage mechanical and coalescing separation architecture. First, the air-oil mixture exits the discharge port tangentially into a vertical separator vessel, utilizing centrifugal cyclonic action to remove 95% of bulk oil droplets. Second, the air passes through a gravity settling chamber. Third, it flows through a dual-wrapped, deep-bed borosilicate microfiber separator cartridge. The coalesced oil drains into a sump and is drawn back to the airend suction via a visible optical scavenger return tube equipped with an internal check valve. This guarantees residual downstream oil content below 1 to 3 ppm across all operating regimes.
How does a two-stage oil-flooded rotary screw air compressor achieve higher specific power efficiency than single-stage units?
Compressing atmospheric air (0.1 MPa) directly to an industrial operating pressure of 0.8 MPa in a single stage requires a steep pressure ratio of 8:1. This large differential pressure across rotor flanks increases internal air leakage back to suction and subjects the rotor bearings to high axial thrust loads.
A two-stage rotary screw compressor divides this pressure rise across two distinct airends arranged in series. The first stage compresses atmospheric air up to an intermediate pressure (~0.28 MPa, ratio ~2.8:1). An atomized oil-curtain intercooler injects cooled synthetic lubricant between stages, reducing the air temperature before it enters the second stage airend, which completes compression to 0.8 MPa. By reducing stage pressure ratios, internal volumetric slip is virtually eradicated, and mechanical compression work is reduced by 12% to 18%, making two-stage systems the preferred choice for continuous baseload facilities exceeding 75 kW.
What OEM and ODM customization services does Honest Compressor offer international distributors and brand owners?
As a specialized OEM/ODM manufacturer in Shanghai, Honest Compressor provides extensive private-label manufacturing programs for overseas distributors and equipment brands. Customization capabilities include:
- Electrical & Grid Adaptation: Native builds for 208V/220V/380V/400V/415V/460V/575V at 50Hz or 60Hz.
- Industrial PLC Firmware: White-label touchscreen programming displaying distributor logos, custom contact details, and multi-language support (English, Spanish, French, Russian, Arabic, German).
- Enclosure & Sheet Metal Design: Custom industrial styling, soundproofing insulation grades, and powder coating matched to client brand RAL color codes.
- Turnkey Modular Packaging: 4-in-1 integrated skid systems combining rotary compressor, air receiver tank, refrigerated dryer, and multi-stage coalescing filters onto a compact baseframe.
- International Certification Packs: CE (Machinery & Low Voltage Directives), ASME pressure vessel stamps, ISO 9001 quality documentation, and comprehensive factory test logs.
What are the recommended preventative maintenance intervals for maintaining peak operational efficiency?
To preserve low specific power consumption and protect twin-screw rotor profiles over a 100,000-hour design life, Honest Compressor recommends the following scheduled maintenance intervals under standard industrial operating conditions:
- Every 500 Operating Hours: Initial break-in lubricant change, scavenger return line inspection, and electrical terminal torque check.
- Every 2,000 to 3,000 Hours: Replacement of intake air filter cartridges, secondary lubricant spin-on filter elements, and synthetic coolant analysis.
- Every 4,000 to 6,000 Hours: Complete charge replacement of synthetic rotary screw lubricant (such as PAO or synthetic esters), precision air-oil separator element replacement, and intake unloader valve seal kit refurbishment.
- Every 20,000 Hours: Minimum pressure valve (MPV) and thermostatic bypass valve rebuilding, motor bearing regreasing/inspection, and laser rotor clearance verification.
Explore Complete Industrial Compressor & Pump Series
Direct manufacturer export pricing, robust factory testing, and tailored OEM delivery for global plant installations.
China 110Kw/150Hp Two-Stage Rotary Screw Air Compressor Permanent Magnetic Variable Frequency 380V Air Cooled Exporter, Exporters
Explore Model
China Oil-Free Water Lubricated Screw Air Compressor EOWV-45A/W Suppliers, Exporter
Explore Model
OEM Hot Sale China Factory High Quality Screw Vacuum Pump Permanent Magnet Frequency Conversion Progressive Pump Manufacturers, Factories
Explore Model
China Oil Cooled Screw Air Compressor 55kw 75hp Industrial Air Compressor Rotary Air Compressor Supplier, Exporter
Explore Model
ODM PM VFD Dry Oil-Free Screw Vacuum Pump for Industrial Clean Vacuum Manufacturer, Suppliers
Explore Model
OEM 18.5kW 25HP Industrial VFD PM Screw Air Compressor Factory, Exporter
Explore Model
OEM 30kW 40HP Permanent Magnet VFD Air Compressor Manufacturers, Factories
Explore Model