
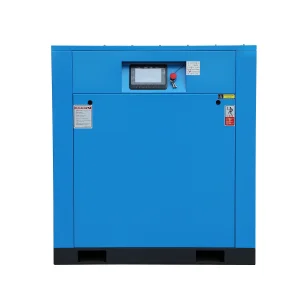
Featured Heavy-Duty Vacuum & Compressor Solutions
Field-tested continuous duty equipment configured for North American industrial specifications and clean power standards.


The Greater Los Angeles Industrial Vacuum Landscape: Dynamics, Demands & Transition
Spacecraft Propulsion Testing, Composites & Electron Beam Welding
Southern California's aerospace corridor requires rough and high vacuum regimes engineered for autoclave vacuum bagging of carbon-fiber composites, environmental thermal vacuum chambers (TVAC), and electron-beam titanium welding. Dry screw vacuum pumps have superseded historical liquid ring and oil-sealed pumps due to their complete elimination of oil hydrocarbon backstreaming, critical for preventing optic lens degradation and propulsion thruster contamination during altitude simulation cycles.
Freeze Drying (Lyophilization), Vacuum Evaporation & MAP Packaging
Processing thousands of tons of high-grade food, nutriceuticals, and pharmaceuticals daily, plants across Vernon and Irwindale demand continuous pumping capacity capable of handling saturated water vapor and corrosive cleaning vapors without emulsifying mechanical lubricating oil. Dry screw vacuum technology isolates process gas entirely within contact-free screw passages, preventing batch contamination and eliminating hazardous oil waste disposal.
Thin-Film Physical Vapor Deposition (PVD) & Semiconductor Tooling
Silicon and compound semiconductor wafer manufacturing, lithium-ion battery drying, and thin-film optical coating facilities depend on clean ultimate vacuum pressures down to 0.01 to 0.005 mbar. Our variable-frequency dry screw pump platforms deliver stable backing performance for magnetic levitation turbomolecular pumps, guaranteeing continuous 24/7 uptime without harmonic resonance or particulates.
Bulk Material Vacuum Pneumatic Conveying & Marine Offloading
The twin ports of Los Angeles and Long Beach move massive dry bulk plastics, resins, grain, and mineral chemicals. Modernization initiatives prioritize heavy-duty industrial vacuum blowers and rotary systems that slash electrical power consumption during pneumatic ship-to-silo transfer, operating cleanly under stringent harbor district clean-air tariffs.
Compliance Engineered for SCAQMD, Title 24 & OSHA Mandates
SCAQMD Rule 219 & VOC Emission Elimination
The South Coast Air Quality Management District (SCAQMD) strictly enforces VOC emission thresholds. Traditional rotary vane pumps exhaust oil mist particulates into plant environments, risking fines under permit-to-operate reviews. Our dry screw vacuum units use non-contact dry compression rotors requiring zero internal sealing fluid, eliminating oil aerosols at source.
- 100% hydrocarbon-free exhaust
- Zero hazardous used oil manifest filings
California Title 24 & LADWP Peak Efficiency
With California commercial electricity rates frequently surpassing $0.22 - $0.34 per kWh, energy compliance under California Title 24 Energy Efficiency Standards is essential to operating margins. Integrated Permanent Magnet synchronous motors (IE4 / IE5 equivalent) controlled by vector VFD dynamically ramp speed to match actual vacuum demand, slashing idling draw by 35% to 50%.
- SCE & LADWP energy efficiency rebate eligible
- Soft start eliminates utility peak kVA demand charges
UL 508A Electrical Standards & Cal/OSHA Acoustics
Our custom control cabinets are engineered for 460V/480V 3-phase 60Hz North American power architectures utilizing UL-recognized electrical contactors, breakers, and PLC logic. Dual-enclosure sound insulation dampens rotor pulsations down to <68 dB(A), keeping facilities fully compliant with Cal/OSHA 8-hour permissible noise exposure limitations without exterior sound baffles.
- NEMA 4 / IP54 dust and moisture control cabinets
- Certified acoustic dampening eliminates hearing PPE zones
Direct-From-Factory Supply Chain Competitiveness: Engineering Excellence from Shanghai
Proprietary Asymmetrical Rotor Geometry
Our variable-pitch screw profiles are ground on German-engineered Klingelnberg CNC rotor grinding centers. The progressive pitch reduces gas temperature during the continuous internal compression process, minimizing thermal expansion and permitting tight micron-level inter-rotor clearances without dynamic interference.
- Reduced internal leakage / slip loss
- Lower operating temperatures and bearing stress
Advanced Chemical Barrier Coatings
For aggressive process gases containing halogens, acids, organic solvents, or condensation moisture, our rotors and pump chambers receive specialized multi-layer PTFE, Nickel-Phosphorus, or PEEK coating treatments to withstand aggressive corrosion and abrasion in harsh chemical and battery slurry processes.
- Anti-corrosive chemical shielding
- Extreme resistance to solvent carryover
Rare-Earth Magnet Supply Integration
China commands over 70% of the world's high-grade NdFeB (Neodymium Iron Boron) rare-earth magnet refinement. Direct upstream integration allows our PM VFD motors to utilize ultra-high-coercivity Grade-SH and UH magnets that remain demagnetization-free up to 180°C under severe duty cycles.
- Up to 96.5% motor drive electrical efficiency
- Zero slip losses compared to induction drives
Comparative Engineering Analysis: Dry Screw vs. Rotary Vane vs. Liquid Ring
| Evaluation Parameter | Oil-Free Dry Screw Vacuum Pump | Oil-Sealed Rotary Vane Pump | Liquid Ring Vacuum Pump |
|---|---|---|---|
| Operating Medium Purity | 100% Oil-Free (Class 0 Dry Cavity) | Oil Misted (Requires Exhaust Coalescers) | Water/Liquid Contaminated Effluent |
| Ultimate Pressure (Rough/Deep) | 0.005 mbar to 0.05 mbar | 0.1 mbar to 0.5 mbar | 33 mbar (Vapor Pressure Dependent) |
| Condensable Vapor Tolerance | Exceptional (Gas Ballast + Purge Cycle) | Poor (Oil Emulsification Risk) | High (Acts as Direct Contact Condenser) |
| Energy Consumption Index | Lowest (PM VFD Matches Gas Flow Curve) | Medium (Fixed Rotor Friction Losses) | High (Liquid Drag Resistance Losses) |
| Preventive Maintenance Cycle | 16,000–24,000 Operating Hours | 1,500–3,000 Hours (Oil / Filter Swap) | Continuous Water Conditioning Needed |
| SCAQMD Permitting Burden | Minimal (Zero VOC Emissions) | Strict Exhaust Filtration Review | Wastewater Disposal Permitting Required |
| 10-Year Total Cost of Ownership (TCO) | Optimal (Power & Maintenance Savings) | High (Ongoing Oil & Filter Disposals) | High (Water Treatment & High kWh Usage) |
Real-World Case Profiles: Deployments Across Greater Los Angeles
Retrofit of Four Oil-Sealed Systems with Dry Screw PM VFD Packages
Challenge: An aerospace structural supplier in Hawthorne faced oil backstreaming that compromised the ultrasonic inspection integrity of resin-infused carbon wing spars. Frequent oil separator failures led to repeated inspection shutdowns.
Engineering Solution: Deployed two ODM 45 kW Dry Screw Vacuum Pumps paired with PLC-controlled Roots vacuum blowers. System delivers 2,400 m³/h volumetric flow down to 0.01 mbar.
Outcome: Achieved 100% hydrocarbon-free vacuum chambers, reduced pump room ambient noise from 84 dB(A) to 66 dB(A), and saved $38,400 annually in avoided hazardous oil disposal and electricity tariffs.
Continuous Vacuum Distillation & Solvent Extraction System
Challenge: Excessive ethanol and water vapor carryover in a food flavor extraction process was emulsifying pump lubricants within 120 hours of operation, causing premature bearing seizures and excessive maintenance downtime.
Engineering Solution: Installed an OEM Industrial Screw Vacuum Pump with Nickel-Phosphorus anti-corrosive rotor plating, automatic thermal jacket temperature regulation, and high-volume nitrogen gas ballast purging.
Outcome: The system runs at a sustained 115°C internal temperature to keep volatile vapors in gas phase until exhaust condensing, boosting extraction batch yields by 14% with zero bearing failure over 18 continuous months.
Frequently Asked Questions by Industrial Vacuum Engineers & US Buyers
How do China-manufactured vacuum pumps comply with Southern California 460V/480V 60Hz industrial grids?
All vacuum pumps, blowers, and screw compressors configured for the North American market are engineered from factory floor level with dual-wound or dedicated 460V/480V 3-phase 60Hz motors. Control circuits are stepped down to 24V DC / 120V AC with UL-listed circuit breakers, Siemens or Schneider contactors, and Phase Monitor Relays to protect sensitive electronics against utility brownout and phase imbalance conditions common during summer peak hours in Southern California.
What is the logistical transit timeline from your factory to delivery at facilities in Los Angeles?
Standard export orders leave our Shanghai manufacturing facility and ship directly via ocean freight to the Port of Los Angeles / Port of Long Beach with a marine transit duration of 14 to 18 days. Including customs documentation clearance, ISF filing, and door-to-door drayage to Los Angeles, Orange County, or San Bernardino industrial facilities, total transit time typically spans 22 to 28 calendar days. Air freight dispatch is available for urgent modular spare parts and vacuum airends with delivery in 3 to 5 business days via LAX.
Why is dry screw vacuum technology replacing oil-sealed rotary vane pumps in California clean manufacturing?
The transition is driven by three main factors: process purity, environmental compliance, and operating economics. Dry screw pumps compress gas without any oil lubricating or sealing the rotor pocket, eliminating the possibility of oil backstreaming into the process chamber. Environmentally, dry pumps emit zero oil mist exhaust, eliminating SCAQMD air permitting scrutiny and hazardous oil waste disposal costs. Economically, variable frequency permanent magnet drives adapt motor speed to real demand, cutting electricity consumption by up to 40% compared to legacy vane pumps.
How do your dry screw pumps handle corrosive gases and condensable vapors like solvent or steam?
Our vacuum pumps feature active jacket heating and automated thermostatic control loops. By maintaining an elevated operating temperature above the dew point of the gas stream, condensables pass cleanly through the compression cavity in vapor state without condensing into liquid droplets. Additionally, we apply proprietary anti-corrosion barrier coatings (including PEEK and specialized nickel alloys) to the rotor surfaces and pump chamber for aggressive chemical, pharmaceutical, or battery slurry processes.
What localized technical support and replacement parts availability are available in the United States?
We maintain regional warehousing partnerships and qualified technical field service relationships across Southern California to provide factory-spec spare kits—such as dynamic mechanical seals, PTFE lip seals, inlet filter cartridges, and synthetic timing gear oils. Every machine is equipped with an IoT-enabled PLC controller allowing real-time remote diagnostics, telemetry tracking, and software parameter adjustment directly between our factory engineering staff and your facility team.
Can your engineering team assist with complete vacuum system sizing and turn-key skid integration?
Yes. Our application engineering department works directly with your facility engineers or mechanical contractors. We calculate effective conductance losses, piping pressure drops, and pump-down volumes, sizing custom combination skids integrating dry screw roughing pumps, Roots mechanical boosters, vapor condensers, inlet dust traps, and automated manifold isolation valves tailored to your exact vacuum cycle requirements.
Complete Rotary Screw & Vacuum Extraction Catalog
From deep dry vacuum down to 0.005 mbar to high-volume water-lubricated Class 0 air compressors, explore our complete industrial portfolio.




Ready to Modernize Your Industrial Vacuum Operations?
Connect directly with our Shanghai application engineering team. We provide complete vacuum pumping speed sizing, gas compatibility analyses, electrical parameter matching (460V/480V 60Hz), and full DDP door-to-door freight quotes directly to your facility in Greater Los Angeles.
