
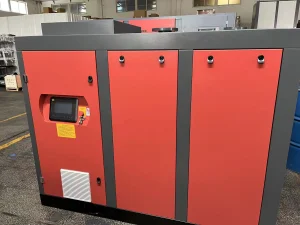
Boston Precision ODM Electrical Motor PM AC ASD Rotary Vacuum Compressor Unit
Direct-from-manufacturer rotary screw compressors and vacuum stations configured for continuous duty, tight contamination tolerances, and rapid dispatch across Greater Boston and New England.


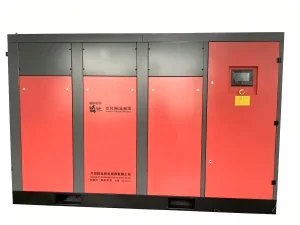
How Cambridge biopharma clusters, Route 128 precision engineering firms, and regional clean energy facilities demand specialized rotary screw pumping architecture.
Boston's biopharmaceutical infrastructure requires strict adherence to cGMP. Dry screw vacuum pumps eliminate oil back-streaming risk during delicate active pharmaceutical ingredient (API) freeze-drying, solvent recovery, and bio-reactor purging, guaranteeing zero hydrocarbon contamination.
Institutions operating near Route 128 and regional university spinouts utilize advanced physical vapor deposition (PVD), chemical vapor deposition (CVD), and electron microscopy. These setups demand deep ultimate vacuum thresholds (≤ 0.01 mbar) paired with vibration-free dynamic rotor balancing.
Commercial electricity rates in Massachusetts consistently rank well above the U.S. national average. Integrating high-flux permanent-magnet (IE4/IE5) variable speed drives allows regional facilities to slash base-load idle consumption by 20% to 40%, generating measurable payback within 18 months.
In high-throughput industrial and laboratory environments, legacy oil-sealed rotary vane pumps represent severe liabilities: thermal runaway, costly waste-oil disposal, frequent seal replacements, and hydrocarbon back-migration. Modern twin-screw vacuum systems utilize precision-machined, non-contacting variable-pitch helical screws that compress process gases progressively along the rotor axis.
Because there is zero metal-to-metal contact within the compression chamber, the system functions completely dry without internal lubrication. Our advanced perfluoropolyether (PFPE) sealing solutions prevent external lubricants from contacting aggressive chemical vapors or moist streams, ensuring continuous thermodynamic stability at high pressure ratios.
Request Technical Datasheet| Parametric Metric | Honest Dry Screw Vacuum | Standard Rotary Vane |
|---|---|---|
| Working Principle | Non-contact dual variable screw | Friction sliding vane with oil bath |
| Contamination Risk | 100% Zero (ISO 8573-1 Class 0) | High risk of oil back-diffusion |
| Solvent / Vapor Handling | Direct pass-through; corrosion resistant | Degrades pump oil, causes emulsification |
| Routine Maintenance | Annual gear oil check; 25,000h overhaul | Bi-monthly oil/filter changeouts |
| Motor Integration | High-Efficiency PM VFD (IE4/IE5) | Fixed-speed induction motor |
Tailoring screw vacuum systems with robust coatings, intelligent closed-loop cooling, and explosion-proof electrical systems for mission-critical installations worldwide.
For chemical and semiconductor duty, rotor and housing surfaces are treated with multi-layer PFA, nickel plating, or ultra-dense PTFE coatings. This guarantees chemical passivity against halogens, organic acids, aggressive solvent fumes, and humid gas loads common in Massachusetts research labs.
By transitioning from uniform pitch to variable pitch screw profiles, internal compression efficiency increases by over 30%. This lowers the exhaust gas discharge temperature, suppresses localized overheating, and minimizes thermal mechanical expansion of components under continuous 24/7 duty cycles.
When operating in chemical vapor synthesis or ethanol extraction environments, units can be specified with explosion-proof electric motors, anti-sparking brass rotor trims, ATEX Zone 1/Zone 2 conformity, and UL 508A compliant industrial control panels.
Integrating embedded telemetry, automated nitrogen purging, and magnetic levitation bearings to redefine operational efficiency and lifecycle predictability.
Every industrial vacuum skid is IoT-ready, transmitting high-frequency accelerometer and thermal imaging sensor data over Modbus-TCP / MQTT. Plant engineers monitor rotor clearance shifts in real time, preventing unexpected downtime before bearing fatigue can manifest.
Advanced gas ballast and automated nitrogen purging sequences modulate seal barrier pressures according to inlet gas concentration. This reduces expensive consumable nitrogen consumption by up to 60% across vacuum drying cycles while inhibiting explosive dust condensation.
Equipped with optional plate-frame liquid heat exchangers, our oil-free and micro-oil rotary systems capture up to 75% of dissipated motor heat to pre-heat facility wash water or cleanroom HVAC make-up air, lowering plant Scope 2 greenhouse gas footprints.
Deploying industrial machinery across New England requires strict alignment with municipal electrical codes, OSHA workplace sound constraints, and rigorous pressure equipment mandates. Honest Compressor delivers equipment designed specifically for international market integration:
Need custom inlet manifolds, variable speed retrofits, or a comprehensive vacuum pump audit for your facility?
Explore our complete portfolio of heavy-duty industrial twin-screw vacuum machines, oil-free high-efficiency blowers, and two-stage compressed air systems.
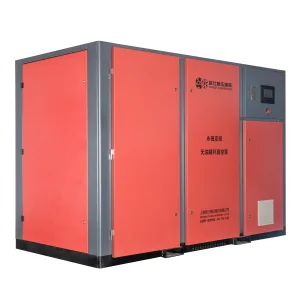
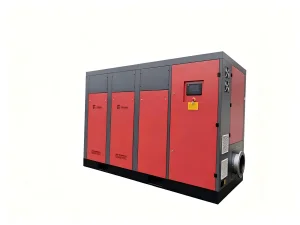

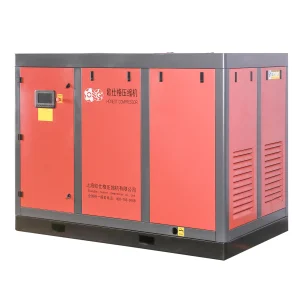

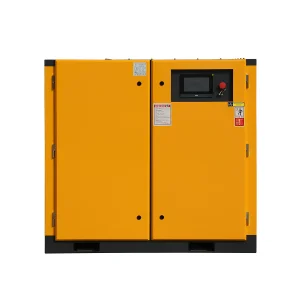
Detailed answers regarding sizing, cleanroom compliance, corrosion handling, and energy optimization for Boston facilities.
Oil-sealed rotary vane vacuum pumps rely heavily on an oil reservoir inside the compression chamber for lubricating and sealing. Under continuous roughing cycles, hydrocarbon vapors inherently back-migrate toward the vacuum inlet, introducing a devastating contamination risk to active pharmaceutical ingredients (APIs), lyophilizers, and semiconductor wafer substrates. Dry twin-screw vacuum pumps feature non-contacting rotors that operate completely without oil in the process chamber, achieving ISO 8573-1 Class 0 cleanliness, lowering operating expenditure by eliminating hazardous oil waste handling, and sustaining ultra-clean vacuum down to 0.01 mbar.
Massachusetts commercial industrial electricity tariffs are among the highest in North America. Traditional fixed-speed vacuum pumps run at a constant RPM regardless of actual pneumatic load, using an intake throttling valve or bypass during idle periods that still consumes up to 70% of full-load power. Our PM VFD systems continuously synchronize rotational velocity to actual process vacuum demand using rapid closed-loop PID control. This prevents mechanical idling, slashes base energy consumption by 20% to 40%, and reduces heat rejection into expensive facility HVAC cleanrooms.
For operations handling volatile chemicals, aggressive chlorines, or corrosive moisture, our screw pumps are custom-engineered with multi-stage chemical passivations. Options include multi-layer fluoropolymer (PTFE/PFA) rotor and stater coatings, electroless nickel plating, and internal Hastelloy or 316L stainless steel trims. In addition, an automated dry nitrogen purge system maintains a positive pressure differential across the lip seals, preventing corrosive vapor permeation into the mechanical synchronization gearboxes.
To accurately specify a unit, our application engineering team requires: (1) Target operational vacuum level (mbar, Torr, or Pa); (2) Required volumetric pumping speed (m³/h or CFM) at that target pressure; (3) Process gas chemical composition, moisture content, and particulate levels; (4) Local electrical power specifications (e.g., 460V, 480V, 380V, 60Hz 3-phase); and (5) Environmental factors including cleanroom classification, ambient temperature range, and site cooling method (air-cooled vs. closed-loop chilled water).
Yes. Our complete compressor and vacuum pump assemblies can be integrated to meet regional UL 508A control panel listing, NFPA 79 industrial electrical machinery safety guidelines, and relevant CE Directives. Surge separation tanks and inter-stage coolers are engineered in compliance with ASME Section VIII design criteria, allowing quick permitting and inspection approvals from municipal fire and building departments throughout Massachusetts.
Standard configured skid models are maintained in strategic buffer inventory for rapid oceanic or air-freight fulfillment, with average delivery times ranging from 2 to 4 weeks depending on customized voltage and control options. All essential consumables—such as intake HEPA filter elements, timing gear oil, mechanical seals, and dynamic sensor replacements—are fully documented with universal industrial cross-references and supported with rapid door-to-door courier dispatch directly into Greater Boston facilities.
Connect with our senior technical engineering team for equipment sizing, TCO payback models, or custom OEM manufacturing schedules tailored specifically for your application.
