
High-Efficiency Two-Stage Heavy Duty Compressors
Pre-configured for the Moscow Industrial District, featuring dual-stage rotor compression, PM VFD technology, and sub-zero winter start protection.
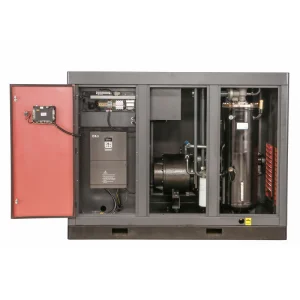



Moscow Industrial Ecosystem & Compressed Air Modernization
A deep-dive whitepaper analysis of localized mechanical manufacturing, import substitution, and thermal-efficiency requirements across Greater Moscow and Moscow Oblast.
Technopolis Moscow & SEZ Zones
The Special Economic Zone Technopolis Moscow (sites across Alabushevo, Micron, MIET, and Rudnevo) spearheads cutting-edge microelectronics, high-precision laser fabrication, and clean automation. These installations require continuous, pulsation-free air supplies with ISO 8573-1 Class 1 moisture and hydrocarbon standards to protect sensitive cleanroom tooling.
Electricity Tariffs & Baseload Optimization
Industrial commercial electricity pricing across the Central Federal District has incentivized plant managers to systematically audit pneumatic baseload power. Compressed air systems consume up to 25–40% of factory electric draws in metal-stamping, injection molding, and composite plants throughout Podolsk, Noginsk, and Kolomna.
Sanctions & Direct Eurasian Supply Lines
With legacy European compressors facing critical spare parts embargoes, Moscow plant engineers demand resilient, direct Sino-Russian supply continuity. Our factory-direct OEM engineering guarantees complete component backward compatibility, non-restricted Siemens/Inovance control stacks, and direct rail shipments via the Moscow Freight Hub (Vorsino).
Why Two-Stage Screw Compression Outclasses Single-Stage in Moscow Heavy Plants
In high-pressure continuous duty cycles (7.5 to 13.0 bar), single-stage compression suffers from elevated thermal expansion, excessive internal rotor slip, and bearing fatigue caused by high pressure differential ratios. Our dual-stage design decouples the overall compression ratio across two paired rotor sets:
- Isothermal Cooling Analogy: Oil mist injected between the first stage and second stage drastically cools compressed gas, lowering the polytropic compression exponent toward the ideal isothermal line.
- Reduced Volumetric Leakage: By maintaining a lower compression ratio per stage ($\pi_1 \approx 2.8$, $\pi_2 \approx 3.0$), internal rotor clearance leakage drops exponentially, boosting volumetric efficiency up to 93–96%.
- Extended Bearing Life: Symmetrical radial load distribution on high-precision SKF angular contact bearings extends mean time between overhauls (MTBO) to over 60,000 continuous hours.
| Performance Index | Single-Stage Machine | Two-Stage PM VFD (Our Unit) |
|---|---|---|
| Specific Power (8 bar) | 7.2 – 8.1 kW/(m³/min) | 5.9 – 6.4 kW/(m³/min) |
| Compression Ratio per Airend | High (approx. 8.0:1) | Balanced (approx. 2.8:1 each) |
| Rotor Discharge Temp | 90°C – 105°C | 68°C – 82°C (Low thermal stress) |
| Annual Energy (110kW / 8000h) | ~880,000 kWh | ~730,000 kWh (~17% saved) |
| Rotor Bearing Longevity | 30,000 – 40,000 hrs | > 60,000 hrs |
| Motor Efficiency | IE2 / IE3 Asynchronous | IE4 / IE5 Ultra-Premium PM |
Engineering for Moscow's Harsh Continental Winters
Uncompromising engineering adaptations preventing lubrication emulsion, valve crystallization, and line freeze in extreme cold seasons down to -35°C.
Pre-Heating & Thermostatic Oil Control
Low winter startup temperatures in unheated compressor enclosures cause oil thickening and severe hydrodynamic drag. Our Moscow-spec units integrate internal sump immersion heating cartridges and electronically modulated thermostatic valves that prevent circulation through oil coolers until the synthetic ISO VG 32/46 lubricant reaches optimal 65°C operating fluidity.
Anti-Condensate Freeze Defense
Condensate accumulation inside air-oil separators and moisture separators during winter load-unload cycling risks ice crystallization in pilot pneumatic valves. Integrated automatic heat-traced electronic zero-loss drain valves purge liquid condensation continuously, preventing line blockage and burst valves across cold workshop floors.
Heavy Particulate Multi-Stage Filtration
Industrial processing zones along the Moscow Ring Road (MKAD) and outer hubs feature high ambient dust from cement works, metallurgy, and highway transport. High-capacity nano-fiber suction filters capture 99.9% of dust particles above 2 microns, keeping the synthetic oil pristine and preserving rotor lobe micro-coatings.
Direct China-to-Moscow High-Speed Freight Corridor
Our smart assembly plants in Shanghai and Zhejiang leverage dedicated China-Europe Railway Express links. Standard consolidated container train sets depart regular terminals (Xi'an, Chengdu, Suzhou) directly to Vorsino Freight Terminal, Moscow Oblast or Bely Rast Logistics Center.
Transit times range from 12 to 16 calendar days, bypassing maritime bottleneck disruptions and guaranteeing on-schedule capital project commissioning for Russian contractors and manufacturing plant expansions.
Precision Rotor Grinding & In-House Manufacturing Depth
Unlike assembly-only aggregators, our factory utilizes German Klingelnberg and UK Holroyd precision rotor milling centers. Rotors undergo dynamic balance testing under ISO 1940 G1.0 standards, ensuring whisper-quiet running under 72 dB(A), minimal torsional vibration, and micro-gap tolerances.
Total Supply Chain Sovereignty & Spare Parts Stocking
Modern procurement demands complete independence from unstable foreign sub-tier suppliers. Our vertically integrated production model controls everything from grey-iron rotor housing casting, CNC five-axis milling, permanent magnet motor winding, through to pressure vessel certification.
For our Moscow partners, critical wear components—including replacement separator elements, synthetic lubricants, intake valves, minimum pressure check valves, and temperature sensors—are backed by warehouse buffer stocks, safeguarding Russian manufacturing lines from unforeseen stoppage.
Inquire About Direct Factory Delivery to MoscowCustoms Union (EAC) Certification & Russian Interface Engineering
Seamless commissioning under Technical Regulations of the Eurasian Customs Union (TR CU) with zero administrative friction.
TR CU 010/2011
Machinery SafetyComplete machine risk assessment documentation, dual-channel emergency stop architectures, mechanical interlocking, and structural rigidity verification conforming to Russian federation industrial standards.
TR CU 032/2013
Pressure EquipmentOil-air separation vessels and receiver vessels tested with ultrasonic weld inspection, hydrostatic pressure certification at 1.5x working pressure, and certified safety relief valves.
TR CU 004 & 020
LVD & EMC ResilienceInverters with built-in DC reactors and EMC filtering protect sensitive microelectronic equipment in Moscow laboratories from high-frequency harmonic grid distortion.
Russian Cyrillic HMI
SCADA & ModbusIntelligent multi-lingual touchscreen interface pre-configured in Russian and English. RS485 Modbus RTU enables seamless integration into local factory automation networks.
Integrated Waste Heat Recovery & Smart Industry 4.0 Telemetry
Convert compressor thermodynamic losses into facility heating for Moscow industrial plants through closed-loop heat recovery modules.
70°C–80°C District & Domestic Water Recovery
Over 90% of electrical energy consumed by a screw compressor is converted into heat. Our optional Moscow Heat Recovery Modules tap the hot oil loop via stainless steel plate heat exchangers, providing free hot water for boiler preheating, workshop radiant hydronic heating, or sanitary employee amenities during long Russian winter months.
IoT Remote Predictive Diagnostics
Real-time cellular 4G/NB-IoT telemetry links compressor operational parameters directly to Moscow plant maintenance dashboards. Live monitoring of vibration spectra, discharge temperature gradients, pressure drop across oil separator cartridges, and inverter bus voltage prevents catastrophic downtime through predictive maintenance.
Wide-Range Variable Frequency Inverters
By matching synchronous speed instantaneously with real-time pneumatic tool consumption, our vector VFD reduces idle load current to zero. The soft-start ramp ensures zero starting inrush current spikes, protecting factory transformers across aging municipal substation infrastructure in outer Moscow industrial rings.
Frequently Asked Technical Questions (Moscow Region)
Comprehensive engineering insights for procurement directors, chief power engineers, and operational leads.
Why is a two-stage compressor more economically viable than a single-stage unit in Moscow?
What measures prevent compressor oil emulsification during cold Russian winters?
Are Honest Compressor units certified under EAC TR CU regulations for the Russian Federation?
What logistics route is used for direct shipping from your factory to Moscow?
Can your controllers communicate with existing factory SCADA and Russian DCS architectures?
Complete Compressed Air Solutions for Moscow Industrial Sectors
Explore our specialized range of chemical, laser-cutting, oil-free, explosion-proof, and water-lubricated compressor equipment.




Equip Your Moscow Plant with Dual-Stage Energy Efficiency
Get direct technical proposals, dimension drawings, P&ID schematics, and CFR/DAP Moscow quotes within 12 hours from our dedicated Eurasian engineering desk.
