
Featured High-Efficiency Industrial Equipment
Explore flagship rotary screw air compressors, variable speed blowers, and industrial vacuum pumps manufactured under ISO 9001 and CE directives for critical industrial applications.

ODM Industrial Oil Free Vsd Screw air Blower Vacuum Pump with Plc Inverter Pm Motor Factories, Exporters
View Product Details
OEM Double screw air compressor with inverter and VSDPM motor for energy saving Manufacturer, Exporter
View Product Details
China 20bar pressure Screw Air Compressor for laser cutting machine Supplier, Suppliers
View Product Details
ODM IP55/54 55KW 75HP Factory Price Two Stage Industrial Screw Type Air Compressor Machine Factories, Exporters
View Product Details
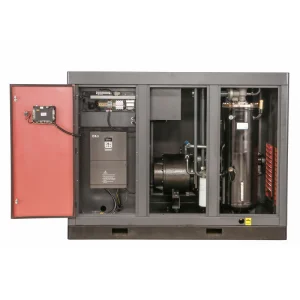
ODM Oil-cooled two-stage permanent magnet variable frequency screw air compressor Manufacturers, Suppliers
View Product Details
1. Macro Industry Solutions & Thermodynamic Efficiency Engineering
Compressed air is widely recognized as the fourth industrial utility, powering over 70% of global manufacturing systems. However, standard industrial audits confirm that up to 75% of a compressor's Total Cost of Ownership (TCO) over a 10-year lifecycle is consumed purely by electrical power expenditure.
Comparative Thermodynamic Analysis: Compression Technologies
| Compression Architecture | Specific Power (kW / m³/min) | ISO 8573-1 Air Purity | Thermal Efficiency Ratio | Optimal Industrial Deployment |
|---|---|---|---|---|
| Single-Stage Oil-Injected Rotary Screw | 6.2 - 6.8 kW/(m³/min) | Class 3 (Oil Content ≤ 5 mg/m³) | 72% - 76% | General pneumatic tools, mechanical workshops |
| Two-Stage PM VFD Oil-Injected Screw | 5.1 - 5.5 kW/(m³/min) | Class 2 (Oil Content ≤ 1 mg/m³) | 88% - 93% | 24/7 Heavy manufacturing, chemical plants, glass production |
| Water-Lubricated Oil-Free VSD Screw | 5.8 - 6.3 kW/(m³/min) | Class 0 (100% Oil-Free Certified) | 82% - 86% | Pharmaceutical cleanrooms, electronics, food processing |
| Dry-Type Oil-Free PM VFD Screw | 6.0 - 6.5 kW/(m³/min) | Class 0 (100% Oil-Free Certified) | 80% - 85% | High-temperature chemical synthesis, semiconductor manufacturing |
2. Global Industrial Supply Chain & Chinese Manufacturing Landscape
Over the past decade, the global industrial air compressor landscape has experienced a major structural shift toward the Yangtze River Delta manufacturing cluster in China, particularly centered around Shanghai and Zhejiang industrial bases.
Vertical Supply Chain Integration
Leading Chinese air compressor factories possess localized, end-to-end production capabilities—from precision casting of screw rotor housing blanks to high-precision rotor grinding using German KAPP CNC machines, IE4/IE5 permanent magnet motor production, and smart PLC assembly.
IE5 Ultra-Premium Motor Adoption
China leads global adoption of IE4 and IE5 Permanent Magnet synchronous motors (PMSM). Compared to standard IE3 induction motors, PMSM drives maintain high torque efficiency across 20% to 100% speed ranges without overheating or efficiency drop-off.
Rigorous ISO & CE Compliance
Top-tier exporters adhere strictly to European Machine Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, Pressure Equipment Directive (PED 2014/68/EU), and ISO 8573-1 air purity standards, matching tier-1 European manufacturers at a competitive capital expenditure.
3. Localized Application Scenarios & Industrial Matrix
Selecting the correct compressed air architecture requires alignment with localized operational constraints, environmental humidity, air purity tolerances, and continuous duty requirements.
Scenario A: Precision Fiber Laser Cutting
Technical Requirement: 16 to 20 bar high-pressure, ultra-dry, particle-free compressed air as assist gas for cutting stainless steel, carbon steel, and aluminum sheets.
Recommended Solution: China 20bar All-in-One Integrated Screw Air Compressor featuring dual refrigerated air dryers, multi-stage precision particulate oil-removal filters, and integrated air storage receivers.
Scenario B: Pharmaceutical & Food & Beverage Cleanrooms
Technical Requirement: Zero oil contamination tolerance. Any oil carry-over risks entire batch contamination, process downtime, and regulatory non-compliance.
Recommended Solution: Water-Lubricated or Dry-Type EOF Series 100% Oil-Free PM VFD Screw Air Compressor delivering ISO 8573-1 Class 0 certified air with low discharge temperatures.
Scenario C: Heavy Petrochemical & Explosive Gas Zones
Technical Requirement: Ex d IIB T4 / Ex d IIC T4 explosion-proof ratings for hazardous zone 1 or zone 2 installations with severe ambient humidity and dust levels.
Recommended Solution: Custom ODM Explosion-Proof PM VFD Integrated Air Compressors featuring IP55/IP65 protected enclosures, stainless steel piping, and flameproof control cabinets.
Scenario D: Municipal Wastewater Aeration & Pneumatic Conveying
Technical Requirement: Continuous low-pressure high-volume air supply (0.3 bar to 1.5 bar) with maximum energy savings under variable organic loads.
Recommended Solution: ODM PM&VSD Oil-Free Screw Blowers (EGV Series) offering non-contact rotor operation and up to 30% higher efficiency than traditional Roots blowers.
4. Global Electrical Compatibility, Compliance & Factory Testing
Deploying air compressors across international plants requires flexible electrical customization and rigorous pre-shipment quality verification protocols.
Worldwide Power Grid Adaptability
Factories engineer dual-frequency (50Hz / 60Hz) motors and custom voltage transformer options to accommodate diverse regional standards:
- North America: 230V / 460V / 575V 3-Phase 60Hz
- Europe & Asia: 380V / 400V / 415V 3-Phase 50Hz
- South America: 220V / 380V / 440V 3-Phase 60Hz
- Mining & Remote Sites: Up to 1000V heavy-duty mining specs
Factory Acceptance Testing (FAT)
Before dispatch, every machine undergoes a full load thermal and vibration test run on computerized test benches per ISO 1217 Annex C/E guidelines. Critical metrics evaluated include:
- Actual Free Air Delivery (FAD in m³/min)
- Specific Power Consumption (kW/m³/min)
- Bearing Vibration Spectrum Analysis
- Acoustic Pressure Sound Level dB(A)
OEM/ODM Customization Capabilities
OEM buyers can configure tailor-made solutions for regional market demands:
- Customized PLC interface supporting 10+ languages
- Variable color powder-coating enclosure options
- Skid-mounted containers for rugged outdoor sites
- Integrated IoT remote telemetry (4G/5G MODBUS TCP)
5. Technology Roadmap: Smart Compression & AIoT Integration
The future of Chinese industrial air compression lies in AI-driven predictive health monitoring, smart sequencing algorithms, and heat recovery integration.
AI Smart Master Controllers
Smart multi-compressor master controllers monitor real-time plant air consumption curves, dynamically starting, stopping, or trimming individual PM VFD compressors to keep line pressure fluctuations under ±0.1 bar while running each machine at its peak efficiency curve.
Predictive Health Telemetry
Embedded IoT sensors monitor rotor vibration frequencies, oil temperature differentials, motor winding thermistors, and air filter pressure drops in real time. Machine learning algorithms alert maintenance managers weeks before potential bearing degradation occurs.
Waste Heat Energy Recovery
Up to 94% of electrical energy input into an air compressor is converted into heat. Chinese manufacturers integrate thermal energy recovery exchangers directly into screw compressor oil circuits, supplying boiler feed water or facility heating up to 85°C at zero extra fuel cost.
Advanced Vacuum, Blower & Special Applications Portfolio
Explore secondary product categories including two-stage energy-saving air compressors, Class 0 dry screw compressors, water-lubricated units, and industrial vacuum pumps.
OEM Energy Saving Air Cooling Screw Compressor Two Stage Direct Driven Screw Air Compressor Manufacturers, Exporters
View Product Details
China Horizontal two-stage pressure screw air compressor Two Stage Screw Air Compressor Electric Screw Air Compressor Price Suppliers, Exporters
View Product Details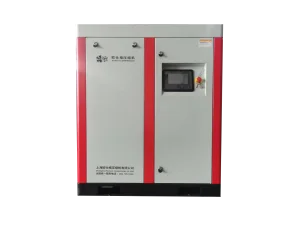
OEM 30kW Water Lubricated Oil Free VSD Screw Air Compressor 380V 400V 415V Industrial Air Compressor Suppliers, Factory
View Product Details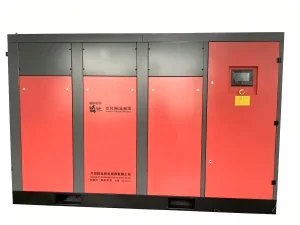
China EGV-132A-140 Oil-Free Permanent Magnet VFD Screw Blower Manufacturers, Exporters
View Product Details
China Honest Compressor -EOF series Oil-Free Dry Type Screw Compressor | 100% Oil-Free PM VFD Manufacturer, Exporter
View Product Details

OEM Industrial Screw Vacuum Pumps – Oil-Injected (0.35 mbar) & Oil-Free (20–80 kPa) Series, 5.5–110 kW Supplier, Exporter
View Product Details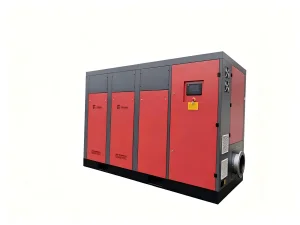
ODM Industrial Screw Vacuum Pump Oil Free High Efficiency Vacuum Pump for Semiconductor & Chemical Industry Manufacturer, Factories
View Product Details6. Technical Procurement Q&A (Frequently Asked Questions)
Expert answers addressing critical technical, energy, and operational evaluation criteria for industrial buyers and factory engineers.
How much electrical energy can a Permanent Magnet VFD compressor realistically save compared to fixed-speed units?
On industrial manufacturing sites featuring fluctuating air demand (30% to 85% load profiles), a Permanent Magnet Variable Frequency Drive (PM VFD) screw air compressor saves between 25% and 42% in electrical power costs. Fixed-speed units continue consuming approximately 30% to 45% of full-load power while running unloaded (idling). In contrast, PM VFD technology slows down the motor in direct proportion to real-time air consumption, eliminating unnecessary idling energy losses and maintaining a stable line pressure within ±0.1 bar.
What is the key engineering difference between Two-Stage compression and Single-Stage compression?
Two-Stage rotary screw air compressors divide the total pressure ratio between two distinct male/female rotor sets arranged in series. After the first stage of compression, an inter-stage cooling oil mist lowers air temperature before entering the second stage. Lower inlet temperature increases volumetric efficiency and decreases internal air leakage. Consequently, two-stage compressors require up to 15% less energy (kW) per m³/min of delivered air compared to equivalent single-stage units operating at 8 to 13 bar pressure.
When should a facility specify ISO 8573-1 Class 0 Oil-Free technology over Oil-Injected screw compressors with inline filters?
Specify 100% Oil-Free air compressors (Water-Lubricated or Dry-Type screw) whenever compressed air comes into direct or indirect contact with sensitive products—such as pharmaceuticals, food and beverage processing, semiconductor cleanrooms, electronics manufacturing, and high-tier automotive paint spraying. While oil-injected compressors equipped with coalescing filters can achieve low oil PPM, filter elements are subject to thermal degradation and sudden rupture, creating an inherent risk of catastrophic batch contamination. Class 0 guarantees absolute zero oil contamination risks.
How does water-lubricated oil-free screw compression operate without synthetic oil lubricants?
Water-lubricated oil-free screw compressors utilize purified water injected directly into the compression chamber. Water serves three crucial roles: sealing rotor clearances, lubricating ceramic/stainless steel bearings, and absorbing compression heat isothermally. Because water possesses a high specific heat capacity, air discharge temperatures remain extremely low (under 50°C), delivering 100% oil-free certified air at high thermodynamic efficiency.
What key technical parameters must be provided to Chinese factories for accurate compressor sizing?
To ensure optimal sizing, buyers should submit: 1) Required Free Air Delivery (FAD in m³/min or CFM); 2) Minimum required working pressure (bar or PSI); 3) Ambient operating temperature and installation altitude; 4) Site supply voltage, frequency, and phase (e.g., 400V/50Hz/3Ph); 5) Desired air purity class per ISO 8573-1; and 6) Plant duty cycle (24/7 continuous vs intermittent batch operation).
What is the typical maintenance schedule for an industrial PM VFD screw air compressor?
Standard preventative maintenance schedules include: Changing intake air filter elements every 2,000 to 3,000 hours; replacing oil filter elements and synthetic compressor coolant every 3,000 to 4,000 hours; replacing air/oil separator cartridges every 4,000 to 6,000 hours; and performing annual PLC firmware checks and cabinet electrical terminal tightening. Direct-drive permanent magnet motors eliminate belt replacements and shaft alignment routines.
How do Chinese compressor factories handle spare parts availability for overseas buyers?
Established Chinese exporters maintain standardized spare parts inventories across major international logistical hubs. Routine consumables (filters, oil separators, valves, sensor probes) feature universal ISO component dimensions and are routinely dispatched via express air freight within 48 hours. Moreover, OEM manufacturers utilize globally supported PLC controllers (such as Schneider, Siemens, or Inovance) ensuring local technician serviceability.
