

Primary Industrial Fleet
High-Efficiency Rotary Screw Machinery Catalog (Phase I)
Factory-direct industrial variable speed screw air compressors, vacuum pumps, and oil-free blowers engineered for minimum specific power consumption and extreme continuous duty.

OEM 4-in-1 Explosion-Proof Air Compressor | 7.5-22kW Permanent Magnet Integrated Unit Factory, Exporters
View Product Specs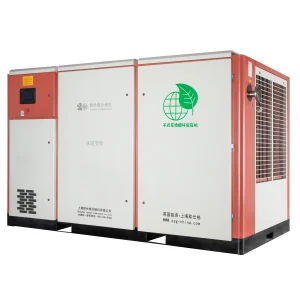
ODM EOF Oil-Free Dry Screw Compressor | 100% Oil-Free PM VFD Manufacturers, Factory
View Product Specs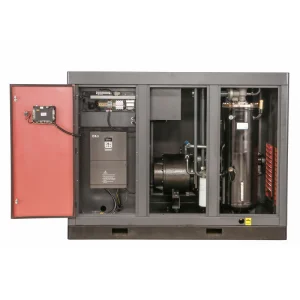
ODM Oil-cooled two-stage permanent magnet variable frequency screw air compressor Manufacturers, Suppliers
View Product Specs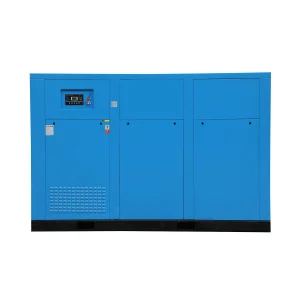
China 110Kw/150Hp Two-Stage Rotary Screw Air Compressor Permanent Magnetic Variable Frequency 380V Air Cooled Exporter, Exporters
View Product Specs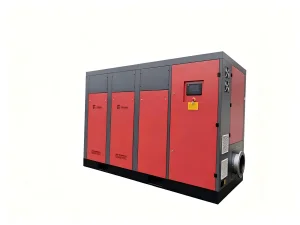
ODM Industrial Screw Vacuum Pump Oil Free High Efficiency Vacuum Pump for Semiconductor & Chemical Industry Manufacturer, Factories
View Product Specs
China 30kw Industrial Oil Free Vsd Screw Air Blower Vacuum Pump With Plc Inverter Pm Motor oil free screw blower Supplier, Suppliers
View Product Specs
ODM IP55/54 55KW 75HP Factory Price Two Stage Industrial Screw Type Air Compressor Machine Factories, Exporters
View Product Specs
Thermodynamic Optimization & System Science
Engineering Variable Speed Rotary Screw Air Compressors: The Science of Specific Energy
Compressed air is widely recognized across industrial engineering as the "fourth utility," frequently consuming up to 30% of a heavy manufacturing facility's total electricity footprint. However, conventional fixed-speed screw compressors operate using inefficient load/unload suction modulation, blowing off excess pressure or idling while still drawing 40% to 70% of full-load power without delivering productive airflow.
Dynamic Frequency Modulation
By pairing high-torque rare-earth permanent magnet synchronous motors (PMSM) with intelligent vector-control variable frequency drives (VFD), rotational rotor speed instantly syncs with real-time pneumatic demand. Pressure swings are compressed within an ultra-tight ±0.01 MPa band, completely abolishing idling blow-down waste.
Elimination of Unload Throttling
Traditional fixed-speed compressors exhaust stored pressurized air into the atmosphere during every unloading event to prevent motor burnout under continuous unloader resistance. A Variable Speed Rotary Screw Compressor soft-starts from 0 Hz and ramps fluidly between 25% and 100% capacity, retaining all compressed air within the header.
Zero Inrush Starting Current
Direct-on-line (DOL) and star-delta starters inflict brutal mechanical shocks and electrical current spikes exceeding 6 to 8 times the nominal full-load amp rating. Variable speed systems feature controlled ramp-ups with starting current consistently lower than 1.0× rated current, guarding transformer stability and extending bearing service intervals.
Industrial Hegemony & Cluster Efficiency
The China Factory Supply Chain Advantage: Shanghai Jiading Cluster
Headquartered in Malu Town, Jiading District, Shanghai, Shanghai Honest Compressor Co., Ltd. (founded in early 2004 as a premier British-owned enterprise) exemplifies the intersection of European fluid engineering and China's unmatched manufacturing supply chain scalability.
NdFeB Rare Earth Integration
China commands over 70% of global rare-earth extraction and refinement. Honest Compressor directly integrates Grade UH and SH Neodymium-Iron-Boron magnets capable of withstanding 180°C continuous rotor core temperatures without thermal demagnetization, ensuring sustained IE4/IE5 ultra-premium efficiency.
5-Axis Precision Rotor Machining
Utilizing high-rigidity CNC worm and screw rotor grinding centers from Germany (Kapp Niles) and Japan, our Shanghai facility manufactures proprietary 5:6 asymmetric helical screw profiles with inter-lobe clearances measured in single-digit microns (μm), drastically minimizing compressed air blow-hole leakage.
Cryogenic Casting & Stress Relief
Rotor housings and structural frames undergo artificial thermal aging, ultrasonic flaw detection, and computer-controlled cryogenic stabilization. This mitigates internal thermal warping across decades of non-stop 24/7 operating cycles under full industrial load.
Full Vertical Ecosystem Agility
With an annual output surpassing ¥100M+ and four specialized assembly lines, our 50,000 m² plant sources pressure vessels, cooling radiators, integrated inverters, and PLC control consoles within a 50 km radius in the Yangtze River Delta, dramatically shortening lead times for global projects.
Proprietary Machinery Architecture
Core Technological Breakthroughs in Screw Compression
Explore how our engineering teams optimize thermodynamic efficiency, seal integrity, and operational safety across diverse industrial operating environments.
1. Two-Stage Compression with Interstage Oil-Injection Cooling
By dividing the total compression ratio into two distinct steps (first-stage rotor feeding intermediate pressure into a second-stage rotor), the pressure ratio per stage drops from ~8:1 to approximately 2.8:1. Liquid atomized oil cooling between stages brings the compression process dramatically closer to ideal isothermal compression, slashing thermodynamic work by 12% to 15% compared to single-stage machines of identical flow rating.
2. Class 0 100% Oil-Free Dry Screw & Water-Lubricated Units
For high-purity sectors like semiconductor etching, bio-pharmaceuticals, and food processing, our EOF and EOWV series eliminate lubricating oil from the compression chambers entirely. Utilizing advanced food-grade Teflon polyetherketone coatings or purified water film lubrication, these compressors achieve ISO 8573-1 Class 0 validation without oil aerosols, liquid droplets, or toxic vapor carryover.
3. Oil-Cooled Permanent Magnet Integrated Inverter Systems
Rather than relying on noisy ambient air cooling fans that introduce airborne contaminants, our flagship PM motors feature an integrated internal oil-circulation cooling jacket. Even at extreme low-frequency operations (such as 15 Hz low-demand cycles), the motor remains thermally regulated, achieving IP55/IP65 ingress protection ratings and eliminating motor burnouts in dusty environments.
4. 4-in-1 Compact Explosion-Proof Skid Systems (Ex d IIB / IIC)
Engineered for hazardous oilfield gathering stations, underground mining, and offshore chemical processing, our integrated packages combine a flameproof PM motor, integrated air receiver, refrigerated desiccant dryer, and multi-stage coalescing filtration skid. The footprint is reduced by 50%, with sound pressure dampening down to 65 dB(A).
Procurement Engineering & TCO Modeling
Global Enterprise Sourcing Criteria & Life Cycle Costing
Procurement executives and plant engineers often mistakenly judge air compressors primarily by upfront purchase cost. Over a standard 10-year operating horizon, electrical energy bills account for up to 78% of the Total Cost of Ownership (TCO), with initial capital investment representing merely 10%.
| Model Series | Motor Power (kW/HP) | Discharge Pressure (MPa / Bar) | Free Air Delivery (m³/min) | Specific Power (kW/(m³/min)) | Drive / Motor Technology | Primary Industrial Application |
|---|---|---|---|---|---|---|
| PM-VFD 11 | 11 kW / 15 HP | 0.7 – 1.0 MPa (7–10 bar) | 1.65 – 1.30 m³/min | 6.67 kW/(m³/min) | PMSM Direct Coaxial | Precision Laser / Packaging |
| PM-VFD 30 | 30 kW / 40 HP | 0.7 – 1.3 MPa (7–13 bar) | 5.00 – 3.80 m³/min | 6.00 kW/(m³/min) | Oil-Cooled PM Inverter | Automotive / Metal Stamping |
| ETOV-55A (2-Stage) | 55 kW / 75 HP | 0.7 – 1.3 MPa (7–13 bar) | 11.2 – 8.90 m³/min | 5.45 kW/(m³/min) | Dual-Rotor Two-Stage VSD | Continuous Heavy Metallurgy |
| ETOV-110A (2-Stage) | 110 kW / 150 HP | 0.7 – 1.3 MPa (7–13 bar) | 23.0 – 18.5 m³/min | 5.15 kW/(m³/min) | Two-Stage Low-Temp VFD | Textile & Chemical Process |
| EOF-75W (Oil-Free) | 75 kW / 100 HP | 0.7 – 1.0 MPa (7–10 bar) | 12.5 – 10.2 m³/min | 6.10 kW/(m³/min) | Dry Screw Water-Cooled PM | Pharmaceutical / Cleanroom |
| ETOV-250A (Heavy) | 250 kW / 340 HP | 0.7 – 1.3 MPa (7–13 bar) | 55.0 – 43.0 m³/min | 4.98 kW/(m³/min) | Two-Stage Direct Drive | Petrochemical & Power Stations |
Real-World Deployment Topology
Engineered for High-Stress Industrial Operating Environments
Discover how variable speed screw compressor technology solves site-specific challenges across critical sectors with fluctuating air demand.
Automotive Manufacturing & Robotic Assembly
Automated spot-welding lines, stamping presses, and electrostatic paint finishing booths operate on rapidly swinging pneumatics. PM VFD compressors instantly ramp between shifts, preventing line pressure dips that can trip robotics while maintaining clean Class 1 oil aerosol control.
Semiconductor Cleanrooms & Electronics
Wafer fabrication, optical lithography sorting, and surface-mount technology (SMT) reject any trace of airborne hydrocarbons. Our EOF Dry-Type PM VFD series supplies continuous ISO Class 0 pure gas streams, protecting microchips against trace oil film contamination.
Biopharma & Sterile Fermentation
Continuous active pharmaceutical ingredient (API) synthesis and deep fermentation tanks require consistent airflow under sterile conditions. Combined with oil-free screw vacuum pumps and screw blowers, our machinery sustains continuous aeration and solvent vapor recovery without downtime.
Explosive & Corrosive Chemical Zones
Certified to Ex d IIB and Ex d IIC T4 ratings, our integrated explosion-proof compressors function reliably inside Zone 1/2 hazardous gas atmospheres and offshore drilling platforms. Copper-nickel coolers resist salt spray corrosion and sulfur atmospheric degradation.
Heavy Metallurgy, Mining & Fiber Laser Cutting
Operating laser cutters at 1.6 MPa to 3.0 MPa requires nitrogen or high-pressure dry air without oil residues that can fog optical lenses. Our two-stage oil-cooled compressors maintain steady pressure headers, guaranteeing burr-free stainless steel cutting edges.
Municipal Wastewater & Aeration Basins
Traditional Roots blowers generate heavy pulsations, ear-splitting noise, and rapid bearing wear. Honest Compressor screw blowers leverage continuous rotary displacement, cutting aeration power bills by 30% and maintaining quiet operation under 75 dB(A).
Quality Assurance & Field Assurance
International Regulatory Compliance & Inspection Protocols
Every compressor delivered from our Shanghai facility is backed by rigorous Factory Acceptance Testing (FAT) in accordance with ISO 1217:2009 Annex C and E, ensuring frictionless customs clearance and site operation worldwide.
TEST PHASE 01
Helium Mass Spectrometry
Every air receiver and refrigeration circuit undergoes vacuum helium testing to detect leakage rates smaller than 1×10⁻⁶ mbar·l/s, safeguarding pressure retention.
TEST PHASE 02
Harmonic & Vector Diagnostics
Inverter drives are tested under simulated line disturbances (±15% voltage sag, 47–63 Hz) to verify IEEE 519 harmonic distortion limits and eliminate grid interference.
TEST PHASE 03
Full-Load 4-Hour FAT Run-In
Units operate at 100% continuous rated discharge pressure while data loggers record bearing temperature rise, motor winding thermals, and mechanical vibration FFT spectrums.
TEST PHASE 04
Multi-Voltage Customization
Configured directly at the factory for overseas electrical supplies: 380V/50Hz, 400V/50Hz, 415V/50Hz, 220V/60Hz, 440V/60Hz, or 480V/60Hz with multi-lingual PLC firmware.
CE, ASME & International Standards Conformity
Compliance documentation accompanies every export container. Systems conform strictly to the European Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, and Pressure Equipment Directive (PED 2014/68/EU). Pressure vessels can be certified to ASME Section VIII Division 1 with the "U" stamp for North American and Middle Eastern markets.
Global Spare Parts Consignment & 1,000+ Field Nodes
With distribution partners across more than 50 export countries, maintenance wear items—such as synthetic lubricants, spin-on oil filters, air intake cartridges, and thermostatic valve kits—are distributed via local consignment warehouses, guaranteeing next-day replacement delivery.
Next-Gen Technology Roadmaps
Future Industry Trajectories: AI Telemetry & Waste Heat Recovery
The industrial rotary compressor landscape is advancing beyond simple mechanical compression into intelligent, connected energy ecosystems. We are pioneering this transition across three main domains:
IoT Digital Twin Cloud Telemetry
Modern Honest Compressor systems feature integrated edge-computing gateway modules connecting to central plant SCADA systems via Modbus RTU, Profinet, or Ethernet/IP. Cloud-based algorithms monitor lubricant viscosity degradation and vibration harmonics, predicting bearing service windows before an outage occurs.
Industrial Waste Heat Recovery (HRS)
Over 90% of electrical energy consumed by an air compressor is converted directly into heat. Our custom-engineered heat recovery modules capture rejected thermal energy from the oil cooler, producing hot water at up to 75°C for boiler feed, space heating, or sanitary washrooms without supplementary electrical or gas consumption.
IE6 Super-Ultra Efficiency Synchronous Drives
Looking toward future industrial decarbonization mandates, our Shanghai R&D center is currently field-testing next-generation Synchronous Reluctance (SynRM) and assisted PM drive configurations aimed at reducing motor electrical losses by an additional 15% under partial load duties.
Procurement & Technical Consultation
Frequently Asked Questions: Industrial Air Solutions
Detailed answers to the technical, operational, and electrical questions asked most often by factory procurement teams and plant engineers.
How much electrical energy can a Permanent Magnet (PM) VFD compressor realistically save?
On manufacturing sites with fluctuating compressed air demand (e.g., machining, automotive packaging, assembly lines), a PM VFD screw compressor consistently achieves 20% to 40% electricity savings compared to a conventional fixed-speed compressor using load/unload suction throttling. Because a fixed-speed unit continues to draw 40% to 70% of its rated electrical power while running completely unloaded (producing no useful air), variable speed units yield substantial savings by matching motor RPM directly to dynamic demand while eliminating unloader blow-off waste.
What is the exact thermodynamic advantage of Two-Stage compression over Single-Stage?
In single-stage compression delivering 0.8 MPa (8 bar), the pressure ratio across a single rotor set is approximately 8:1, resulting in high discharge air temperatures, significant thermal air expansion, and increased inter-lobe backflow leakage. Two-stage compression divides the compression process into two discrete stages (Stage 1 ~2.8:1, Stage 2 ~2.8:1) with atomized cooling oil injected between the stages. This interstage cooling lowers the inlet temperature of the air entering the second stage, bringing the total compression curve closer to an ideal isothermal cycle and cutting power consumption by 12% to 15% for identical volumetric output.
When is an ISO 8573-1 Class 0 Oil-Free compressor non-negotiable versus oil-injected?
ISO 8573-1 Class 0 oil-free air is legally required and process-critical whenever compressed air comes into direct or indirect contact with sensitive products—such as in pharmaceutical API manufacturing, aseptic food and beverage packaging, semiconductor wafer fabrication, continuous textile weaving, and high-end automotive paint spray lines. While oil-injected compressors equipped with coalescing filters and carbon adsorbers can achieve low ppm levels, filter cartridge rupture, high ambient heat, or deferred maintenance creates catastrophic risk of oil carry-over contamination into the production process.
How does Honest Compressor protect Permanent Magnet motors from thermal demagnetization?
We deploy high-coercivity NdFeB (Neodymium Iron Boron) magnets graded SH or UH, rated for continuous operational heat thresholds of 150°C and 180°C respectively. Additionally, our high-spec variable speed machines integrate an oil-cooled motor housing jacket rather than air-fan cooling. Circulating cooling oil directly absorbs heat from the stator and rotor even during sustained low-frequency (e.g., 15 Hz) operation, completely eliminating the thermal demagnetization risks common to low-cost air-cooled PM drives.
What electrical parameters and documentation are required to quote an export project?
To accurately configure and quote an industrial compressor, our application engineering team requires: (1) Free Air Delivery (FAD) requirement in m³/min or CFM; (2) Desired working discharge pressure in MPa, bar, or PSI; (3) Operating electrical parameters (e.g., 380V/50Hz/3P, 400V/50Hz, 415V/50Hz, 460V/60Hz, 480V/60Hz); (4) Ambient site conditions (ambient temperature range, relative humidity, installation altitude above sea level); (5) Air quality purity target per ISO 8573-1; and (6) Any specific explosion-proof certifications (e.g., ATEX, Ex d IIB T4).
Does Honest Compressor provide comprehensive OEM and ODM private labeling?
Yes. As a British-invested manufacturer operating a 50,000 m² smart facility in Shanghai, we provide extensive OEM and ODM customization for international compressor brands, industrial distributors, and turnkey engineering contractors. Customization options cover customized canopy aesthetics and RAL powder coating colors, custom sheet metal stamping, multi-lingual touchscreen PLC controllers, customized Skid-Mounted 4-in-1 layouts, custom pressure ranges, and third-party certified testing documentation.
How are variable frequency drives isolated from electrical harmonics that damage plant equipment?
Our variable speed rotary screw air compressors incorporate built-in DC bus link chokes or AC line input reactors alongside high-frequency EMI/RFI filter modules conforming to EN 61800-3 Category C2/C3 standards. This design mitigates total harmonic current distortion (THDi) to compliant levels, shielding sensitive factory PLCs, robotic controllers, and measurement instrumentation from high-frequency inverter feedback.
What maintenance routine is required to maintain the warranty on your screw air compressors?
Standard scheduled maintenance is straightforward: (1) Initial inspection and oil sampling at 500 operating hours; (2) Replacement of spin-on oil filter elements and high-efficiency air intake filter cartridges every 2,000 to 3,000 operating hours (dependent on dust loading); (3) Full synthetic lubricant replacement and air-oil separator element renewal every 4,000 to 6,000 hours; and (4) Motor bearing re-greasing or inspection at 20,000-hour intervals. Our front-hinged canopy design ensures full 360-degree maintenance access to all service points.
Precision Engineering Fleet
Specialized Industrial Machinery Catalog (Phase II)
Discover high-capacity, multi-stage, and application-specific rotary screw compressors and vacuum pumps built to world-class manufacturing standards.

China Permanent Magnet VFD Rotary Screw Compressor 11kW Manufacturer, Manufacturers
View Product Specs
OEM 18.5kW 25HP Industrial VFD PM Screw Air Compressor Factory, Exporter
View Product Specs
OEM 30kW 40HP Permanent Magnet VFD Air Compressor Manufacturers, Factories
View Product Specs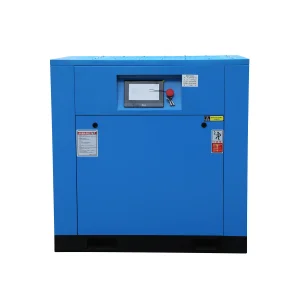
OEM Industrial 15kw/22kw/37kw/55kw/75kw Energy Saving Pm Motor VSD/VFD Rotary Screw Air Compressor Manufacturer, Exporters
View Product Specs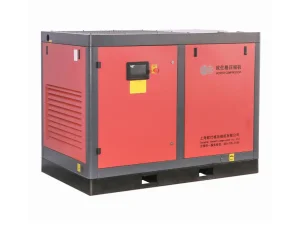
OEM Energy Saving Air Cooling Screw Compressor Two Stage Direct Driven Screw Air Compressor Manufacturers, Exporters
View Product Specs
China Honest Compressor -EOF series Oil-Free Dry Type Screw Compressor | 100% Oil-Free PM VFD Manufacturer, Exporter
View Product Specs
OEM 22kW 30HP Variable Speed Rotary Screw Compressor Factories, Exporter
View Product Specs
