
Featured Industrial Rotary Compressors & Systems
Engineered for low specific energy consumption, continuous 24/7 duty, and strict international standard conformity (ISO 1217 Annex C, CE, ASME, Class 0).
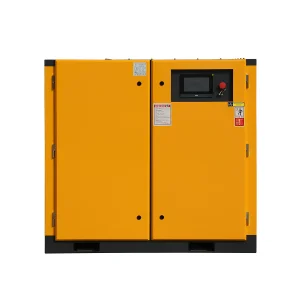
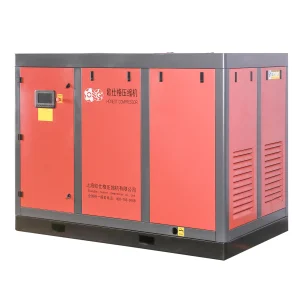


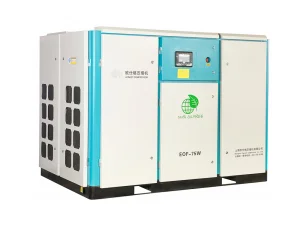
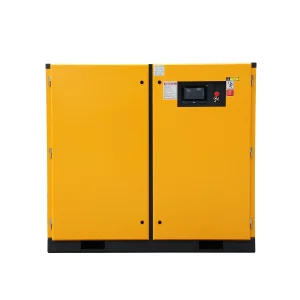

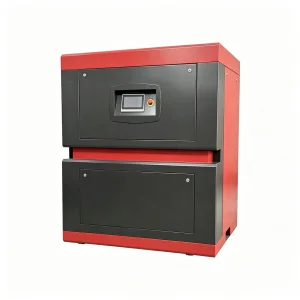
The Strategic Dominance of the 10 Hp (7.5 kW) Screw Compressor in Modern Manufacturing
How decentralized compressed air architectures, global decarbonization mandates, and high-frequency variable speed drive technologies have reshaped the benchmark for small-to-medium industrial powerplants.
Decentralization & Point-of-Use Resilience
Global industrial plants are pivoting away from massive, monolithic centralized compressor rooms toward agile, point-of-use installations. A centralized 250 kW plant suffers substantial transmission friction loss, distribution loop pressure drops (often losing 0.8–1.5 bar across long headers), and catastrophic downtime risks if the primary header fails. A precision-engineered 10 Hp rotary screw compressor (7.5 kW) delivers air delivery right at the machine cell—such as CNC machining centers, automated laser cutting cells, or packaging lines—drastically eliminating distribution pipeline drop, slashing pipework capital expenditure, and isolating operational line risk.
Piston-to-Rotary Screw Displacement Phase
The historical reliance on reciprocating (piston) compressors in the 7.5 kW category has collapsed under modern operating demands. Reciprocating units suffer from abrasive piston-ring friction, high vibration, unsupportable thermal spikes, and a maximum allowable duty cycle of roughly 50%–60% to avert thermal seizure. In contrast, twin-screw positive displacement machines run on a continuous 100% duty cycle. Utilizing precision asymmetric male-female helical rotors with hydrodynamic oil seals, rotary screw units maintain equilibrium temperatures under continuous full-load duty while reducing acoustic contamination from >85 dBA down to sub-65 dBA.
PM VFD Integration & Real-Time Load Tracking
Traditional fixed-speed compressors operate via inefficient "load/unload" suction throttling. When plant air demand drops, the motor continues drawing 40%–50% of full-load power while producing zero compressed air. Next-generation 10 Hp compressors manufactured with Permanent Magnet Variable Frequency Drives (PM VFD) continuously modulate motor rotational speed to synchronize precisely with real-time pneumatic demand. By maintaining pressure stability within ±0.01 MPa and eliminating unneeded idling, PM VFD technology drives electricity reductions between 25% and 42%.
Thermodynamic Insight: Why Specific Power (kW / m³/min) Dictates Profitability
In a 10 Hp compressor operating 6,000 annual hours, electricity costs dwarf the initial capital purchase cost within 14 months of commissioning. A sub-optimized 7.5 kW air compressor operating at a specific energy efficiency of 8.6 kW/(m³/min) consumes thousands of kilowatt-hours more per year than an optimized 5:6 asymmetric profile unit delivering 7.2 kW/(m³/min). When evaluating global suppliers, Free Air Delivery (FAD) per ISO 1217 Annex C must be the benchmark metric, not electrical nameplate rating alone.
Inside the ODM 10 Hp Screw Compressor: Advanced Componentry
Technical dissection of high-efficiency rotary airends, magnetic flux density, dual-stage acoustic dissipation, and thermodynamic fluid circuits designed for hostile operating environments.
5:6 Asymmetric Helical Rotor Airend
The core airend employs an asymmetric 5-lobe male and 6-flute female rotor configuration machined from forged carbon alloy steel. CNC ground on German gear-grinding machinery down to ±2 μm tolerances, this profile minimizes blow-hole leakage area and lowers internal back-flow pressure differentials, elevating volumetric efficiency above 95%.
IE4 / IE5 Ultra-Premium PM Motors
Featuring sintered NdFeB (Neodymium Iron Boron) permanent magnets capable of withstanding 180°C demagnetization thresholds. Direct-coupled without belt or gearbox friction losses, the motor runs at 96%+ electrical efficiency across an ultra-wide turndown frequency spectrum (15 Hz to 75 Hz) for maximum dynamic agility.
Triple-Stage Separation (< 2 ppm)
Centrifugal swirling separation, gravity sedimentation, and ultra-fine borosilicate fiber depth filtration work in synergy. The air-oil separator tank limits lubricant carry-over down to ≤ 2 ppm residual oil aerosol. Low carry-over extends downstream filter cartridge life, guards pneumatic solenoids, and lowers plant top-up oil costs.
Thermostatic Plate-Fin Heat Exchange
Oversized aluminum plate-fin cooling cores coupled with low-RPM, dynamic balanced centrifugal fans. Governed by mechanical thermostatic bypass valves to avert condensation emulsification in cold start states, ensuring continuous operation in ambient temperatures up to +46°C without thermal tripping.
| Performance Parameter | Fixed Speed 10 HP Standard | PM VFD 10 HP (Energy-Saver) | All-in-One 4-in-1 Laser Series | Class 0 Oil-Free 10 HP |
|---|---|---|---|---|
| Nominal Motor Power | 7.5 kW (10 HP) / IE3 | 7.5 kW (10 HP) / IE4 or IE5 | 7.5 kW (10 HP) / IE4 VFD | 7.5 kW (10 HP) / IE4 VFD |
| Working Pressure Range | 7.0 – 10.0 bar (0.7–1.0 MPa) | 6.0 – 13.0 bar (customized) | 13.0 – 16.0 bar (Laser assist) | 7.0 – 10.0 bar (0.7–1.0 MPa) |
| Free Air Delivery (FAD @ 8 bar) | 1.10 m³/min (38.8 CFM) | 0.32 – 1.15 m³/min (variable) | 0.85 – 0.95 m³/min (16 bar) | 0.98 – 1.05 m³/min (Dry) |
| Drive Coupling Method | Heavy-Duty Belt / Direct Gear | 1:1 Integrated Direct Drive | Direct Shaft Integrated | Direct Synchronized Gear |
| Noise Level (ISO 2151) | 68 ± 2 dB(A) | 64 ± 2 dB(A) | 65 ± 2 dB(A) | 66 ± 2 dB(A) |
| Compliance Certification | CE / ISO9001 | CE / Class 1 Energy | CE / ASME / Pressure Vessel | ISO 8573-1 Class 0 |
China Factory 4.0: Supply Chain Resilience & Export Advantage
How deep industrial clustering in Shanghai and the Yangtze River Delta delivers uncompromised component precision, agile ODM engineering turnaround, and robust global logistics guarantees.
Hyper-Integrated Component Supply Ecosystem
Within a 100-kilometer radius of our manufacturing plant in Jiading District, Shanghai, sits the world's most dense ecosystem of high-precision mechatronics suppliers. From specialized resin sand casting foundries producing Meehanite casting iron compressor housings to world-tier bearing distributors (SKF, NSK), our factory achieves unparalleled supply agility. Component supply lead times that take 12 to 18 weeks across European networks are procured and quality-inspected within 48 to 72 hours.
Rapid Prototype & Bespoke ODM Engineering
Unlike legacy manufacturers locked into rigid catalog SKUs, our engineering department provides end-to-end ODM adaptation within 15–20 business days. Whether an overseas private-label client requires dual-voltage electrical engineering (e.g., 208V/230V/460V 60Hz for North America; 380V/400V/415V 50Hz for Europe and Australia), customized PLC touchscreens with local language firmware, or specialty stainless steel piping for corrosive atmospheres, our CAD-to-production pipeline handles the iteration seamlessly.
Automated Testing & ISO 1217 Verification
Every 10 Hp compressor exiting the assembly station undergoes 100% full-load run-in testing on automated computer-controlled test benches. We log real-time vibration amplitude (< 1.8 mm/s), mechanical noise decibel curves, thermodynamic oil-air equilibrium temperatures, dielectric insulation resistance, and FAD volumetric flow rate verification complying with ISO 1217 Annex C standards. Clients receive traceable digital quality records with every export container.
Localized Application Scenarios: Where 10 HP Excels
From automotive spray booths in North America to precision laser fabricators in Central Europe, see how the 10 Hp screw compressor solves pneumatic bottlenecking across diverse industries.
Automotive Refinishing & Smart Body Shops
Spray booths require continuous, pulsation-free compressed air free of aerosolized lubricant mist. Pressure ripples caused by conventional piston compressors result in orange-peel imperfections and fisheyes on automotive clearcoats. The continuous helical discharge of a 10 Hp rotary compressor, paired with an integrated refrigerated dryer (+3°C pressure dewpoint) and coalescing filters, delivers zero-pulsation, Class 1-4-2 air quality that runs HVLP paint guns simultaneously without pressure drops.
1kW – 4kW Fiber Laser Assist Gas Cutting
Precision fiber sheet metal laser cutting requires high-pressure assist gas (up to 16 bar) to evacuate molten kerf cleanly. Utilizing liquid nitrogen or bottled oxygen induces immense consumable overhead. Our specialized 10 HP 16-bar all-in-one compressor station, tank-mounted with four-stage filtration down to 0.01 micron, generates on-demand high-pressure assist air at a small fraction of bottled gas costs, cutting burr-free stainless steel and aluminum.
Electronics Assembly & High-Speed SMT Lines
Surface Mount Technology (SMT) pick-and-place machines and pneumatic PCB test jigs demand low-vibration operation. A vibrating air compressor can send mechanical shockwaves through plant flooring, upsetting sub-millimeter component placement nozzles. With dynamic residual unbalance ratings within G2.5 and acoustic dampening cabinets maintaining sound levels below 65 dB(A), our 10 HP units sit safely right alongside sensitive automated electronics assembly lines.
Secondary Food Packaging & Bottling
Pneumatic box folding, capping cylinders, thermoforming blowers, and coding systems require stable, non-stop air supply during 16-to-24 hour packing shifts. Our 10 HP PM VSD air compressor responds in milliseconds to cycling pneumatic cylinders, eliminating the line starvation that stops automated cartoning lines, while optional food-grade synthetic polyol-ester (POE) lubricants guarantee complete peace of mind.
Textile Weaving & Industrial Garment Finishing
Textile mills present harsh ambient operating conditions characterized by airborne micro-lint, cotton dust, and high summertime temperatures. Conventional reciprocating compressors suffer early valve clogging and overheat. Our 10 Hp rotary units incorporate oversized pre-filtration louvers, large radiator fin spacing, and heavy-duty dust filters that resist lint blinding, ensuring continuous weaving productivity.
B2B Buyer Evaluation Matrix: Total Cost of Ownership (TCO)
Why professional equipment procurement managers evaluate specific power consumption, maintenance intervals, and duty ratings rather than raw purchase prices.
Capital Purchase Price (12% of Lifetime Cost)
The initial machinery invoice represents barely 10% to 15% of the total 10-year operational cost of a 10 Hp compressor. Opting for a low-grade machine with inefficient rotor tolerances may save $400 to $800 upfront, but will incur $2,500 to $4,500 in excess electricity penalties annually. As an established ODM supplier, our pricing strikes the balance: high-tier CNC-ground rotors and IE4 motors priced directly from our Shanghai manufacturing line.
Scheduled Maintenance (12% of Lifetime Cost)
Routine consumables (oil filters, air intake filters, oil-gas separator cartridges, synthetic polyalphaolefin PAO lubricant) require maintenance every 3,000 to 4,000 running hours. Our design utilizes spin-on filter architecture and hinged service doors, reducing routine servicing downtime to under 25 minutes without specialized tooling.
Electricity & Carbon Footprint (76% of Cost)
Power draw is the overwhelming financial driver. At an average industrial rate of $0.14 per kWh running 5,500 hours/year, a 7.5 kW motor draws roughly $5,775 in annual energy. Upgrading to our PM VSD architecture, which cuts un-loaded consumption and dynamically follows actual airflow needs, yields annual power reductions averaging $1,400 to $2,300—paying for the machine itself in under 3 years.
Bespoke ODM Engineering: Built for Your Brand and Market
We do not just produce compressors; we empower overseas distributors, brand houses, and system integrators with custom manufacturing tailored to local regional codes.
Worldwide Grid Adaptation
Custom windings and certified inverter drives configured for all global electrical grids: 220V/230V 60Hz 3-Phase (USA/Mexico), 460V/480V 60Hz (USA), 380V/400V/415V 50Hz (Europe/UK/Australia), and 575V 60Hz (Canada), complete with cULus, CE, and EAC control panel compliance.
Modular All-in-One Integration
Space-constrained facilities benefit from our fully integrated "4-in-1" package: 10 HP rotary screw compressor, 300-liter or 500-liter ASME/CE certified air receiver tank, cycling refrigerated air dryer, and 4-stage ultra-precision coalescing filter set on a compact, single forkliftable skid base.
Custom Controller & IoT Cloud Telemetry
Full-color 7-inch PLC touchscreen interfaces customized with your brand logo, corporate color theme, and native firmware in English, Spanish, Russian, French, German, or Portuguese. Built-in RS-485 Modbus-RTU, Ethernet, and optional 4G IoT cloud telemetry for predictive mobile maintenance alerts.
Turnkey Brand Packaging
From precision laser-cut sheet metal cabinet aesthetics finished in custom RAL electro-powder coat colors to silkscreen corporate badging, bespoke serial number identification plates, translated operator instruction manuals, and fumigated export wooden crating ready for immediate distribution.
Technical Q&A: Procurement & Engineering Guide
Answers to the most critical technical and operational questions posed by plant engineers, EPC consultants, and industrial equipment importers.
1. How does a 10 Hp (7.5 kW) rotary screw compressor compare to a reciprocating piston unit in continuous operation?
2. What is the real-world return on investment (ROI) when upgrading to a PM VSD 10 Hp model?
3. What Free Air Delivery (FAD) flow rate can I expect from a 10 Hp screw compressor at 8 bar vs 10 bar?
4. What are the key maintenance intervals and life expectancies for core components?
5. What ODM customization options are supported for overseas private-label distributors?
6. How do you prevent oil carry-over from contaminating sensitive pneumatic applications?
Expanded Industrial Range & Heavy-Duty Systems
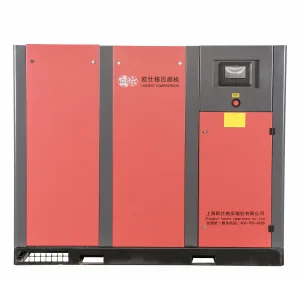
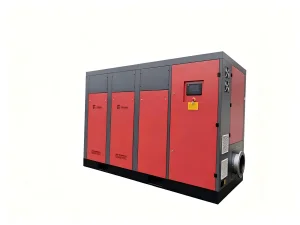
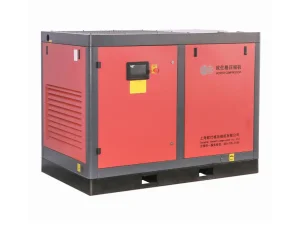
Browse our complementary portfolio of two-stage industrial rotary compressors, vacuum pumps, and high-efficiency permanent magnet air stations.




Global Delivery Assurance: Export Protocols for 50+ Countries
Ensuring sea freight integrity, seamless customs clearance, and verified mechanical readiness across ports in North America, Europe, the Middle East, Southeast Asia, and South America.
ISPM-15 Heat-Treated Packaging
All compressors are hermetically poly-wrapped with industrial desiccant packets, moisture-barrier vacuum sealed, and secured within reinforced fumigated ISPM-15 compliant wooden crates with heavy-duty structural steel skid forklift bases to eliminate ocean transit vibration and saline atmosphere corrosion.
International Document Compliance
Export documentation packages include verified Certificates of Origin (CO, Form E, Form F), official CE Declaration of Conformity documents, ASME/CRN pressure tank manufacturing data reports, and individualized factory ISO 1217 Annex C test run reports for immediate destination port customs clearance.
Continuous Spare Parts Guarantee
We maintain guaranteed global availability of consumable kits, airend rebuild components, thermostatic valves, and PLC motherboards, dispatched via air courier (DHL/FedEx express) within 24 hours of notification, minimizing plant disruption and reinforcing your brand reputation in your target market.
