
Standard & Custom Air Compression Systems
Explore our premier industrial systems engineered for continuous 24/7 duty. Designed with precision male-female rotor profiles, permanent-magnet variable-frequency drive control, and heavy-duty thermodynamic fluid cooling for demanding factory baseloads.
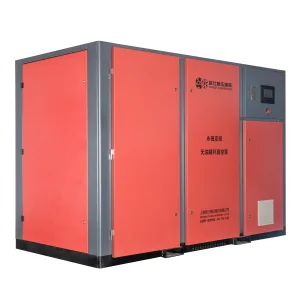
ODM PM VFD Dry Oil-Free Screw Vacuum Pump for Clean Vacuum
View Specifications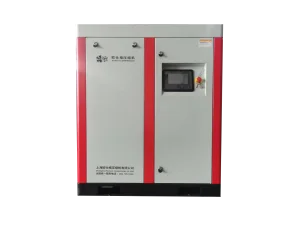
OEM 30kW Water Lubricated Oil Free VSD Screw Air Compressor
View Specifications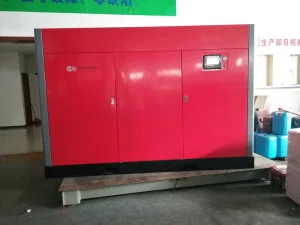
Smart Energy Saving Water Lubricating 100% Oil Free Compressor
View Specifications
OEM 18.5kW 25HP Industrial VFD PM Rotary Screw Air Compressor
View Specifications
OEM Screw Vacuum Pump PM Frequency Conversion Progressive Unit
View Specifications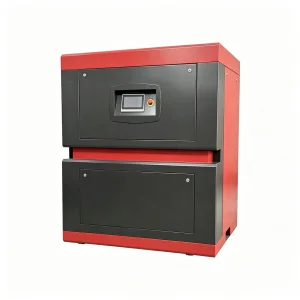
China Oil Cooled Screw Air Compressor 55kW 75HP Industrial Rotary
View Specifications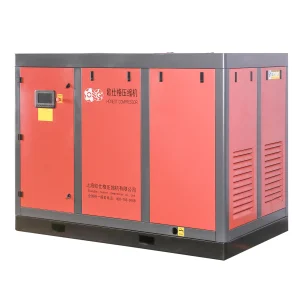
OEM Two-Stage Screw Air Compressor for Chemical Plant Duty
View Specifications
OEM 22kW 30HP Variable Speed Direct-Drive Rotary Screw Unit
View SpecificationsThe Mechanics of Lubricated Screw Compression: Near-Isothermal Efficiency
Oil-injected (lubricated) rotary twin-screw compressors represent the backbone of global industrial air power, accounting for over 78% of continuous plant installations worldwide. Understanding the thermodynamic role of dynamic fluid injection explains why these units dominate heavy manufacturing.
Thermodynamic Heat Absorption
Air compression inherently generates significant thermal energy governed by polytropic expansion. In an oil-injected airend, formulated synthetic or mineral lubricant is continuously atomized into the rotor flutes. The fluid acts as a massive thermal heat sink, absorbing the heat of compression immediately at generation, moving process curves closer to an ideal isothermal compression cycle and lowering specific power consumption (kW/m³/min).
Dynamic Hydrodynamic Sealing
Rotary screw compression relies on finite clearances between male and female helical rotors (typically 30–60 microns). The injected oil establishes a continuous hydrodynamic capillary barrier across radial and axial clearance gaps. This sealing action suppresses internal blow-hole leakage and backflow from the high-pressure discharge port to the suction intake, maximizing volumetric efficiency up to 96%.
Mechanical Rotor Drive & Bearing Cushion
Unlike dry oil-free units requiring complex external timing gears, lubricated male rotors directly drive the female rotors through an elastohydrodynamic oil film. This eliminates metal-to-metal contact, absorbs pulsation vibrations, and provides continuous pressurized lubrication to cylindrical roller and angular contact thrust bearings, extending nominal airend service life beyond 100,000 operational hours.
Global Commercial Dynamics & Lifetime TCO Analysis
Energy costs dictate more than 75% of an industrial air compressor's 10-year Total Cost of Ownership (TCO). In the modern regulatory climate—governed by EU Ecodesign, US Department of Energy (DOE) compliance, and corporate ISO 50001 energy targets—procuring optimized lubricated compressors is a top-priority financial decision.
Electricity: 76% of TCO
A standard 55 kW rotary compressor running 8,000 hours annually consumes electricity costs far eclipsing its initial purchase price in year one alone. Integrating IE4/IE5 permanent magnet motors with vector-controlled variable frequency drives eliminates idle running losses, dynamically tracking factory demand fluctuations.
Capital Capex: 12% of TCO
Initial procurement represents a fraction of plant expenditure. Selecting an experienced ODM manufacturing partner enables plant engineers and EPCs to deploy high-spec machinery—featuring dual-stage airends and integrated air handling—at sustainable direct-factory production economics.
Preventive Care: 12% of TCO
Unplanned downtime carries severe financial penalties. Modern oil-flooded compressor architecture features oversized spin-on filtration, centrifugal three-stage air-oil separation vessels, and synthetic lubricants with 4,000 to 8,000-hour replacement intervals, keeping recurring maintenance predictable.
Decarbonization Mandates
National net-zero roadmaps penalize plants operating outdated fixed-speed compressors. Upgrading to two-stage compression splits the overall pressure ratio across two distinct rotor stages, curbing specific energy consumption by 12–15% compared to legacy single-stage equivalents.
Original Design Manufacturer (ODM) Customization Matrix
Honest Compressor operates a 50,000 m² smart manufacturing plant in Jiading District, Shanghai. We engineer and deliver customized rotary screw packages designed around regional grid specifications, harsh ambient conditions, and proprietary brand guidelines for private-label distributors globally.
| Subsystem Architecture | Standard Production Specification | ODM Factory Customization Capabilities | Compliance / Standard |
|---|---|---|---|
| Compression Airend | Single-stage 5:6 asymmetric screw rotor profiles; precision ground finish | Two-stage inter-cooled airends; custom pressure ratios (0.5 to 1.6 MPa); specialized anti-corrosion rotor surface coatings | ISO 1217 Annex C |
| Drive Motor Topology | IE3 / IE4 three-phase asynchronous motors; IP54/IP55 protection | Ultra-efficient IE5 Permanent Magnet (PM) synchronous motors; liquid/oil-cooled motor enclosures; explosion-proof Ex d IIB / IIC ratings | IEC 60034-30-1 |
| Variable Frequency Drives | Integrated vector control frequency inverters; 25%–100% modulation range | Heavy-duty dual VFD configurations (main motor + cooling fan); multi-brand inverter sourcing (Inovance, Danfoss, ABB); EMC filter integration | CE / UL 508C |
| Thermal Cooling System | Oversized ambient air-cooled aluminum plate-fin heat exchangers | Marine-grade shell-and-tube water chillers; stainless steel cooling coils; dual-circuit heat recovery units capturing up to 90% thermal energy | ASME / PED Class |
| Separation & Air Quality | 3-stage centrifugal separation with wrap-around micro-glass separator; <3 ppm carryover | Ultra-clean <1 ppm deep-bed coalescing filtration; integrated refrigerated or desiccant air dryers; skid-mounted air receiver tanks | ISO 8573-1:2010 |
| Smart PLC & Telemetry | Multi-language color touchscreens with RS-485 Modbus interface | Cloud IoT gateways, real-time vibration/bearing temperature telemetry, 4G cellular remote diagnostics, custom branded UI firmwares | Industry 4.0 / OPC-UA |
Localized Electrical Engineering & Regulatory Compliance
Deploying compressor equipment internationally requires strict adherence to disparate electrical grids, regional safety certifications, and pressure vessel directives. Honest Compressor pre-engineers and factory-certifies equipment for swift installation and hassle-free customs clearance.
Worldwide Voltage & Frequency
Industrial power grids vary significantly by continent. We configure complete motor-inverter assemblies for 380V/50Hz (China, Europe), 400V/50Hz (UK, EU), 415V/50Hz (Australia, India, Southeast Asia), 460V/60Hz (North America), 220V/60Hz, and high-altitude derated applications with customized transformer windings.
Pressure Vessel Certifications
Air-oil separation tanks must satisfy rigorous boiler and pressure vessel codes. Our manufacturing facilities are audited and authorized to stamp vessels in compliance with the European Pressure Equipment Directive (PED 2014/68/EU), American ASME Section VIII Div. 1, MOM (Singapore), and DOSH (Malaysia).
Factory Traceability & Testing
Every machine undergoing export dispatch is subjected to automated dynamic load testing at our Shanghai facility. Free Air Delivery (FAD) is empirically verified according to ISO 1217 Annex C standards. Full quality documentation, material certificates, and test logs accompany each consignment.
Mission-Critical Field Scenarios for Lubricated Compressors
Oil-flooded screw compressors handle aggressive industrial operating environments where mechanical durability, continuous air availability, and high thermal resilience are paramount to production uptime.
Automotive & Heavy Stamping
Continuous robotic tooling, pneumatic clamping, and large-tonnage sheet metal stamping presses generate dramatic, cyclic air spikes. Lubricated VFD units dynamically adjust output within 0.1 bar of the target pressure setpoint, preventing pressure drops during shift changeovers.
Chemical Plants & Refineries
Hazardous processing zones demand explosion-proof electrical controls, ATEX certification, and continuous operation under high ambient temperatures. Two-stage lubricated units supply process gas conveyance, valve actuation, and nitrogen generation systems reliably.
Glass, Cement & Metallurgy
Cement clinker conveyance and glass bottle blow molding require enormous volumes of reliable, hot-shift compressed air. High-capacity water-cooled lubricated screw systems feature heavy-duty cyclonic air intake pre-filters to isolate airborne particulates.
Mining & Heavy Infrastructure
From tunnel boring and deep mine pneumatic ventilation to aggregate blasting, lubricated rotary packages provide shock-resistant structural skids, reinforced motor frames, and specialized extreme-duty synthetic oils resilient against temperature swings from -20°C to +50°C.
Specialized Heavy-Duty & Two-Stage Machinery
Broaden your facility's operational capabilities with our dedicated industrial equipment range. Covering two-stage high-efficiency air compressors, high-torque direct-driven systems, clean-screw blowers, and vacuum systems built to customer specifications.

China Permanent Magnet VFD Rotary Screw Compressor 11kW
View Specifications
China 55KW 75HP Two-Stage Direct Drive Screw Compressor with PM
View Specifications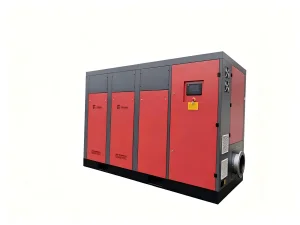
ODM Industrial Screw Vacuum Pump for Semiconductor & Chemical
View Specifications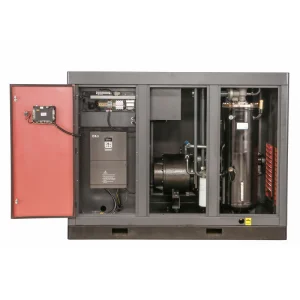
ODM Oil-Cooled Two-Stage Permanent Magnet Variable Frequency Unit
View Specifications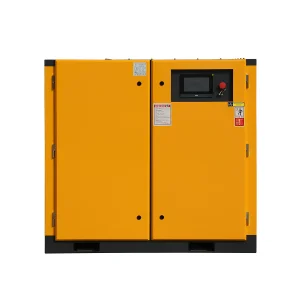
OEM Variable Frequency Drive Air Compressor 15kW Energy Saving
View Specifications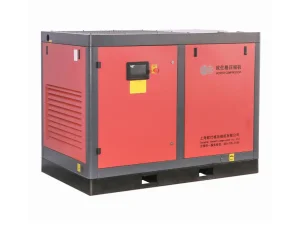
OEM Energy Saving Two Stage Direct Driven Air Cooling Compressor
View Specifications
China 30kW Industrial Oil Free VSD Screw Blower Vacuum Pump
View Specifications
ODM PM & VSD Oil-Free High Efficiency Industrial Screw Blower
View SpecificationsEngineering Roadmap: AI Telemetry & Heat Recovery Integration
The future of lubricated rotary screw systems lies in thermodynamic energy harvesting, autonomous algorithm-driven pressure matching, and synthetic lubrication formulations that minimize lifecycle carbon intensity.
AI Dynamic Pressure Matching
Conventional control architectures monitor static discharge pressure transducers. Next-generation controllers utilize edge-AI predictive models trained on plant consumption patterns. By anticipating air demand variations seconds before pneumatic equipment engages, the inverter speeds up proactively, eliminating pressure drops and wasteful over-pressurization.
94% Thermal Energy Recovery
Up to 94% of electrical energy consumed by a lubricated compressor is converted into heat absorbed by the cooling oil. Our factory-engineered heat recovery modules integrate food-grade plate heat exchangers directly into the oil circuit. This produces process hot water up to 85°C for boiler preheating, sanitation, or facility heating with zero additional fuel cost.
Predictive Bearing Health & IoT
Unplanned airend seizure is the ultimate catastrophic failure. Embedded high-frequency piezoelectric accelerometers continually monitor rotor FFT vibration spectra and bearing temperature curves. Real-time data streams via MQTT to secure cloud dashboards, flagging micro-spalling or lubricant breakdown hundreds of hours before physical failure occurs.
Technical & Procurement Inquiries
Clear, engineering-backed answers addressing rotor dynamics, specific power metrics, fluid maintenance protocols, and ODM supply agreements.
Why do lubricated screw compressors achieve superior specific power compared to single-stage dry oil-free units?
What technical criteria govern the choice between mineral, synthetic hydrocarbon (PAO), and polyol ester (POE) compressor lubricants?
How does two-stage screw compression mechanically achieve 12% to 15% energy savings over single-stage compression?
What is the actual residual oil carryover rate in modern lubricated systems, and can it satisfy ISO 8573-1 air purity standards?
What lead times, prototyping procedures, and MOQ policies apply to custom ODM/OEM compressor manufacturing contracts?
How do Permanent Magnet (PM) synchronous motors maintain high efficiency across fluctuating production loads compared to standard induction motors?
Initiate Your Custom ODM Compressor Project
Collaborate directly with Honest Compressor’s senior application engineers in Shanghai. We review site FAD demand, duty cycles, electrical parameters, and compliance mandates to formulate tailored, high-efficiency compressed air packages.
Manufacturing Headquarters
No. 355 Jiajian Branch Road, Malu Town, Jiading District, Shanghai, China.
Modern 50,000 m² machining, assembly & ISO 1217 testing center.
Direct Factory Communications
Telephone: +86 021 69177185
Technical Inquiry Email: [email protected]
Dedicated English-speaking technical sales & sizing support.
Global Engineering Response
Inquiries evaluated within 24 operational hours.
Comprehensive CAD engineering submittals, electrical schematics, and commercial quotes provided upon request.
