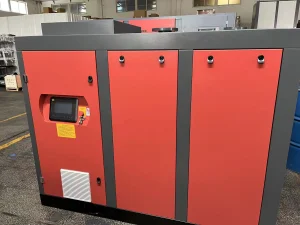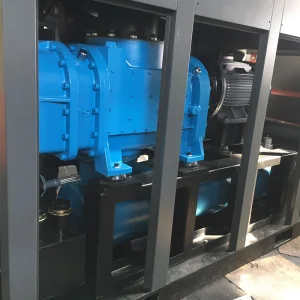
Explore precision rotary twin-screw compression machinery engineered with permanent magnet frequency conversion, water-lubricated oil-free airends, and process vacuum technology.
Strategic deployment of positive-displacement twin-screw gas compressors across energy transition corridors, petrochemical gas recycling, methane mitigation infrastructure, and sour gas wellhead booster operations.
The global shift toward non-fossil hydrocarbon streams has placed rotary screw compressors at the core of biomethane (RNG) injection systems. Raw anaerobic digester gas and landfill gas—rich in methane (50–65%) but saturated with water vapor and carbon dioxide—demand rugged twin-screw geometry capable of constant low-to-medium pressure ratio boosting (0.05 MPa to 1.6 MPa) without liquid droplet damage.
Under international climate frameworks (EU Methane Regulation, US EPA Quad Ob/Oc, and World Bank Zero Routine Flaring by 2030), upstream and downstream operators must eliminate venting and routine flaring. Rotary screw gas compressors serve as the industrial workhorse for Vapor Recovery Units (VRU) and Flare Gas Recovery Systems (FGRS), efficiently handling severe variations in molecular weight (MW 16 to 48) and flow volume.
Remote oilfields and mature coal seams face declining wellhead pressures. Conventional reciprocating compressors suffer from high valve failure rates caused by dirty, wet gas. Rotary screw compressors utilize oil-flooded or mechanical synthetic fluid barriers to scrub incoming particulate, dampen pressure pulsations, and operate continuously for 40,000+ hours between major overhauls.
| Compression Mechanism | Molecular Weight Sensitivity | Handling Wet / Dirty Gas | Turn-Down Capability | Maintenance MTBF (Hours) | Vibration & Pulsation |
|---|---|---|---|---|---|
| Twin-Screw Gas Compressor (Oil-Flooded) | Virtually Insensitive (MW 2–50) | Excellent (Liquid handled by oil circuit) | 15% – 100% (VFD + Internal Slide Valve) | 40,000 – 60,000 h | Negligible (Smooth rotary motion) |
| Reciprocating Piston Compressor | Low Sensitivity (Thermal ratio changes) | Poor (Liquid slugs shatter valves/liners) | Stepped / Clearance pocket limited | 8,000 – 12,000 h (Rings/Valves) | Severe (High pulsation dampers required) |
| Centrifugal Gas Compressor | Extremely Sensitive (Aerodynamic head collapse) | Very Poor (Blade erosion and stalling) | 70% – 100% (High surge vulnerability) | 30,000 – 45,000 h | Low unless near surge line |
| Dry-Type Screw Compressor (Oil-Free) | Moderate (Clearance leakage affects light gas) | Moderate (Requires dry gas pre-treatment) | 30% – 100% (Via variable inverter drive) | 25,000 – 35,000 h | Minimal (Synchronized timing gears) |
Customizing the rotary screw envelope for aggressive chemical matrices, sour hydrogen sulfide ($H_2S$) streams, variable built-in volume ratios ($V_i$), and complete barrier fluid containment.
Process gas compression differs radically from standard air compression. The thermodynamic behavior of hydrocarbon blends is governed by non-ideal real gas state equations ($P \cdot V = Z \cdot n \cdot R \cdot T$), where compressibility factors ($Z$) drift substantially as pressure ascends through the screw pitch.
In raw natural gas or flare streams containing propane, butane, and pentane ($C_3+$ fractions), lowering compression temperature prematurely induces condensation of heavy hydrocarbons inside the compression chamber. When liquid hydrocarbons condense into the lubricant, they dissolve synthetic polyalkylene glycol (PAG) or polyalphaolefin (PAO) oils, drastically reducing lubrication viscosity and accelerating bearing fatigue.
For sour field gas containing wet hydrogen sulfide, raw rotor blanks and casing alloys are manufactured strictly in accordance with NACE MR0175 / ISO 15156 standards to avert sulfide stress cracking (SSC) and hydrogen embrittlement:
Utilizes pressurized synthetic barrier fluid between inner and outer mechanical faces. The barrier fluid pressure is held 0.15–0.2 MPa above compressor internal suction pressure, ensuring zero process gas escapes into the environment. Ideal for toxic, combustible hydrocarbons and biogas boosting.
Engineered with spiral-grooved silicon carbide rotating rings and carbon stationary rings. Nitrogen purge buffer gas creates a micro-level hydrodynamic aerodynamic lift (2–3 μm), eliminating friction wear, delivering negligible parasitic power loss, and matching the rigorous expectations of critical refinery fuel gas systems.
Cost-effective, highly resilient configuration for low-to-medium differential pressure vacuum and vapor extraction processes. Constructed with filled PTFE sealing lips operating against ceramic-coated shaft sleeves with dedicated atmospheric oil quench cups to lubricate sealing edges continuously.
Key evolutionary trajectories transforming rotary screw process gas compression: Hydrogen blending, wide-bandgap silicon carbide inverters, AI-edge health analytics, and modular electrification.
With natural gas pipeline networks piloting 5% to 25% hydrogen admixture ($H_2$), gas density plunges dramatically. Honest Compressor is pioneering micro-clearance rotor machining (down to 15 μm) and specialized barrier gas loops to prevent blow-by leakage and mitigate hydrogen attack.
Replacing traditional induction drives with oil-cooled Neodymium (NdFeB) Permanent Magnet Synchronous Motors paired with Silicon Carbide (SiC) VFDs. Delivers unmatched efficiency across volatile wellhead pressures, slashing energy consumption by 20% to 40% compared to fixed-speed compression.
Integrated industrial IoT controllers run local Fast Fourier Transform (FFT) vibration algorithms. By sensing micro-cavitation, bearing raceway spalling, or lubricant oxidation trends before thermal spikes occur, our OEM skids provide true predictive reliability for unattended remote field stations.
Global oil and gas concessions are actively replacing gas-engine-driven recips with automated electric motor-driven rotary screw skids. This eliminates onsite tailpipe emissions, simplifies maintenance intervals, and leverages grid power or onsite solar-microgrid power sources.
Engineered packages built specifically for demanding process environments, aggressive chemical properties, and strict international site standards.
Challenge: Raw anaerobic biogas enters compressor at ambient pressure, saturated with 100% relative humidity, 40% carbon dioxide ($CO_2$), and up to 2,500 ppm of corrosive hydrogen sulfide ($H_2S$).
Honest ODM Solution: Custom 316L stainless-clad screw airend operating with fully synthetic PAG lube that refuses hydrocarbon solubility. Integrated water-separator coalescers on skid, followed by variable-speed PM motor tracking biological generation rates automatically.
Challenge: Storage crude oil tanks continuously flash volatile light hydrocarbons into the vapor space. Pressures fluctuate wildly between 20 mmAq vacuum to 15 kPa positive pressure, requiring immediate vapor suction to prevent venting.
Honest ODM Solution: Integrated explosion-proof (Ex d IIB T4) rotary screw package with high-frequency pressure transducer control. Responds in milliseconds from 15% idling up to rated capacity without tripping, compressing vapors directly into sales gathering lines.
Challenge: Syngas loops containing hydrogen ($H_2$), carbon monoxide ($CO$), and trace ammonia ($NH_3$) require ultra-tight internal clearances and zero risk of atmospheric gas escape.
Honest ODM Solution: Double mechanical shaft seal arrangement backed by automated nitrogen barrier consoles (API Plan 53C). Asymmetric precision-ground 5:6 rotor profile minimizing backflow of light hydrogen molecules, backed by water-cooled shell-and-tube heat exchangers.
Challenge: Lithium battery electrode slurry solvent recovery (NMP extraction) and pharmaceutical freeze drying mandate 100% hydrocarbon-free pumping chambers to eliminate batch cross-contamination.
Honest ODM Solution: Dry-running rotary screw vacuum pumps and water-lubricated ISO 8573-1 Class 0 oil-free screw machinery. Operates with non-contact synchronized timing gears, isothermal low-temperature rotor bodies, and completely dry compression cavities.
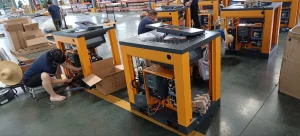
Inside our British-invested 50,000 square meter Jiading smart production complex: from high-precision rotor machining to full-load Factory Acceptance Testing (FAT).
Airend efficiency hinges on the tight tolerances of inter-lobe rotor meshes. Our Shanghai facility utilizes Klingelnberg and Holroyd precision screw grinding centers, maintaining profile tolerances within ±3 microns. This guarantees minimum gas back-leakage, especially critical when handling lightweight hydrogen or helium gases.
Every custom gas compressor skid undergoes comprehensive testing in our explosion-proof certified testing bays. Factory Acceptance Testing (FAT) records multi-point vibration spectra, sound pressure curves, lube oil particle counts, and power factor verifications across dynamic variable speed envelopes prior to export packing.
We supply skid-mounted architectures combining compressor airends, explosion-proof PM motors, heavy-duty suction scrubber vessels, coalescing gas filtration down to 0.01 ppm, air-cooled or water-cooled aftercoolers, and multi-language PLC microcontrollers (Siemens/Schneider/Allen-Bradley) into a single plug-and-play package.
In-depth technical answers addressing operational mechanics, custom gas configurations, certification compliance, and lifecycle optimization.
Reciprocating compressors utilize delicate suction and discharge valves that fail rapidly when exposed to liquid droplets, aerosol condensation, or dirt particles present in raw biogas and wellhead gas. Rotary screw compressors are positive displacement machines without internal valves. In oil-flooded configurations, incoming liquids are simply absorbed into the circulating oil stream and subsequently separated in the multi-stage separator vessel, resulting in vastly superior uptime and lower overall maintenance costs.
Hydrocarbon dilution occurs when the compression operating temperature drops below the hydrocarbon dew-point, causing gaseous $C_3+$ fractions to liquefy and dilute the lubricating oil. Our systems employ dynamic thermal management algorithms: smart electronic mixing valves continuously maintain the oil injection temperature at an optimal margin above the calculated hydrocarbon dew-point. Additionally, synthetic polyalkylene glycol (PAG) lubricants with low hydrocarbon solubility are specified to preserve film strength.
Yes. As an experienced ODM manufacturer, we design and certify electrical skid systems to match local explosion protection codes worldwide. This includes ATEX (Zone 1 / Zone 2), IECEx, and China GB3836 Ex d IIB T4 / Ex d IIC T4 ratings. Electric motors, variable frequency drives, solenoid valves, pressure switches, temperature transmitters, and PLC junction boxes are all fully encapsulated or intrinsically safe.
Wellhead pressures and biological digestion rates are rarely static. Fixed-speed machines waste massive amounts of power cycling through load/unload or bypass throttling modes. Permanent Magnet Synchronous Motors (PMSM) maintain exceptionally high electrical efficiency (IE4 / IE5) across 15% to 100% of their speed curve, allowing the compressor to modulate rotor RPM instantaneously to follow changing inlet gas volume while maintaining exact line pressure.
To deliver an optimal technical proposal and volumetric calculation, we require: (1) Gas chromatography / composition analysis ($CH_4, CO_2, H_2S, N_2,$ heavy hydrocarbons, etc.), (2) Suction pressure range (bar/MPa/psi), (3) Required discharge pressure, (4) Flow capacity in $Nm^3/h$ or SCFM, (5) Site ambient temperature boundaries and altitude, (6) Electrical utility voltage and frequency (e.g., 380V, 400V, 415V, 460V / 50Hz or 60Hz), and (7) Hazardous area classification.
Honest Compressor process gas packages are engineered for a design lifespan exceeding 20 years. By utilizing paired heavy-duty angular contact thrust bearings and cylindrical roller radial bearings bathed in filtered, thermally stabilized synthetic lubricants, the mechanical Mean Time Between Overhauls (MTBO) for bearing replacement is typically 40,000 to 50,000 continuous operating hours under rated operating parameters.
Industrial rotary screw vacuum packages, oil-free dry compression platforms, and variable-frequency single-phase compressors built for global distributors and EPC contractors.
Connect directly with Shanghai Honest Compressor's senior engineering team. Whether you need an explosion-proof flare gas recovery skid, sour biogas boosting units, or Class 0 dry vacuum packages, our factory provides complete sizing simulations, thermodynamic modeling, and global export compliance.