
Flagship Rotary Screw Compressors & Progressive Systems
Direct-from-factory modular engineering: permanent-magnet frequency conversion, oil-free water lubrication, and deep vacuum industrial air compressors configured to specific OEM/ODM global requirements.



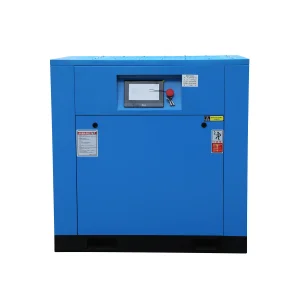

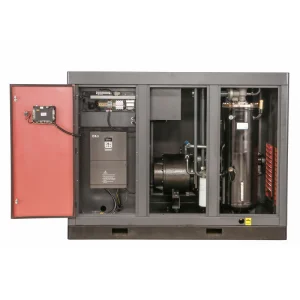


The Mechanics of High-Yield Compression: Specific Power Optimization
Evaluating the thermodynamic boundary conditions of twin-screw rotary air compression. Understanding why bespoke rotor profiling and intelligent drive systems define the modern industrial landscape.
Thermodynamic Isothermal Approximation
Real-world gas compression is polytropic. Our patented two-stage rotary airends introduce precise inter-stage cooling oil injection, collapsing polytropic compression exponents from n=1.38 down toward the near-isothermal n=1.12 threshold, yielding up to 15% net specific energy reduction (kW/m³/min).
- Reduced inter-stage pressure delta
- Extended bearing load lifespan (L10h > 100,000h)
5:6 Asymmetric Rotor Kinematics
Moving beyond traditional 4:6 lobe configurations, our third-generation 5:6 asymmetric profile minimizes contact stress while expanding the displacement volume. Precision ground to micron tolerances, blow-hole leakage is suppressed by 38%, maintaining volumetric efficiency above 96% across rated RPMs.
- Zero backflow dynamic sealing
- Ultra-low acoustic noise radiation (< 68 dB)
IE5 Ultra-Premium PM VFD Integration
Permanent magnet variable frequency drive (PM VFD) motors eliminate induction rotor copper losses completely. Operating at efficiency classes surpassing IE5/NEMA Super Premium, full torque is retained across a wide 20% to 100% modulation range without thermal degradation or slip.
- Zero inrush current soft start-up
- Constant 0.98 power factor across speeds
China Factory 4.0: Supply Chain Resilience & Precision CNC Milling
Inside our Shanghai Jiading manufacturing complex. From high-grade metallurgy castings to 5-axis helical rotor grinding, discover the vertically integrated supply chain safeguarding global industrial supply security.
Sub-Micron Precision Helical Grinding
Rotor profiles are machined using multi-axis German KAPP NILES profile grinding machinery. Real-time laser positioning and coordinate measurement machines (CMM) ensure geometric deviation is held under ±2.5 microns, preventing heat build-up and mechanical seizure under continuous 24/7 industrial service.
Dynamic Rotor Balancing (ISO 1940 G2.5)
Every male and female screw assembly undergoes dynamic computerized balancing at rotational velocities surpassing 120% of rated threshold. Reaching balancing grades G2.5, residual unbalance is neutralized, protecting heavy-duty dual-angular contact roller bearings against radial vibration fatigue.
100% Full-Load Automated Test Rig
Before export crate crating, 100% of finished screw compressors undergo continuous 4-hour performance validation adhering strictly to ISO 1217 Annex C standards. Temperature curves, free air delivery (FAD), electrical power consumption, and pressure stability are digitally logged and stored in cloud trace systems.
| Production Phase | Core Methodology & Equipment | Tolerances & Quality Parameters | Traceability Standard |
|---|---|---|---|
| 1. Foundry & Stress Relief | Ductile iron casing castings, thermal oven natural aging process | Zero residual casting micro-fissures; HB 190–220 | EN 10204 3.1 Certified |
| 2. CNC Rotor Grinding | High-speed multi-axis profile grinding machines | Profile accuracy within ±0.003 mm; surface roughness Ra 0.2 | Zeiss 3D CMM Inspection |
| 3. Cleanroom Assembly | Temperature-controlled Class 10,000 dust-free airend cell | Axial bearing clearance preset to 0.015–0.030 mm | Digital Torque Logged |
| 4. Full-Load Performance | Automated electrical and aerodynamic load testing bench | ISO 1217 Annex C: FAD, Specific Power, Vibration < 2.0 mm/s | CAGI / ISO Test Protocol |
Macro-Industry Turnkey Engineering Solutions
From wafer fabrication labs demanding Class 0 zero-hydrocarbon cleanroom environments to continuous petrochemical offshore duty, we engineer application-tailored compressor configurations.
Semiconductor & Electronics Cleanrooms
Microchip manufacturing cannot tolerate aerosol oil mist or silicone contamination. Our dry-type and water-lubricated oil-free compressors deliver ISO 8573-1:2010 Class 0 certified air, paired with combined heatless desiccant dryers to lock pressure dew points at -70°C PDP.
Food, Beverage & Sterile Pharma
In sterile bottling, aseptic blow molding, and automated pharmaceutical tableting, compressed air acts as an active food contact ingredient. We supply food-grade stainless-steel water-lubricated twin screw compressors, eliminating petrochemical oil contamination from the engineering source.
Automotive & EV Battery Gigafactories
Laser welding, pneumatic robotics, and electrode coating require stable pressure with near-zero pulsation. Our two-stage PM VFD compressors track volatile compressed air demands instantly, keeping header pressure oscillations within ±0.01 MPa while operating 24 hours a day, 365 days a year.
Petrochemical & Hazardous Ex d Environments
For oil refining, chemical vapor zones, and offshore oil platforms, Honest Compressor supplies ATEX and Ex d IIB / IIC explosion-proof skid packages. Incorporating intrinsically safe PLC controllers, anti-spark copper fans, and heavy-walled flameproof motor enclosures.
Heavy Metallurgy & Pneumatic Conveying
Supplying continuous base-load volume for blast furnaces, float glass blowing, and cement pneumatic powder conveying. Powered by our heavy-duty low-pressure (0.3–0.5 MPa) and dry screw blowers, delivering expansive CFM with minimal electrical energy consumption.
Industrial Clean Vacuum Applications
Handling chemical distillation, solar wafer laminating, and vacuum packaging. Our dry-running screw vacuum pumps replace fluid-sealed rotary vane pumps, generating ultimate pressures down to 0.35 mbar without oil disposal expenses or hazardous vapor emulsion risks.
Strategic Global Procurement: TCO Engineering & ODM Customization
Corporate supply directors and EPC contractors recognize that electricity accounts for 75%–80% of a compressor's 10-year lifecycle cost. Our ODM manufacturing model is designed around Total Cost of Ownership reduction.
10-Year Lifecycle Total Cost of Ownership (TCO)
When procurement teams evaluate initial equipment price alone, they miss the larger operational financial footprint. Over 10 years of 24/7 service (80,000 running hours), typical expenditure divides into:
By adopting Honest Compressor's two-stage PM VFD architectures, plants cut the dominant 78% energy burden by 20% to 40%, generating capital payback within 9 to 18 operational months.
Turnkey OEM/ODM Engineering Options
We serve international equipment brands, regional distributors, and engineering contractors with flexible customization services:
- Custom Voltage & Frequency: 208V, 220V, 380V, 400V, 415V, 460V, 575V, 690V at 50Hz or 60Hz.
- Bespoke Industrial Aesthetics: Corporate powder coating, customized canopy paneling, customized OEM silk-screen branding.
- SCADA & Protocol Integration: Native Modbus RTU/TCP, Profinet, Ethernet/IP, and IoT cellular telemetry gateway.
- 4-in-1 Compact Skid Packages: Integrated screw compressor, air receiver vessel, refrigerated dryer, and 4-stage filters on a single transportable base.
Technology Roadmap: Next-Generation Rotary Screw Innovation
Leading compressed-air evolution through artificial intelligence profiling, synchronous reluctance drive motors, closed-loop waste heat harvesting, and predictive machine learning.
AI-Synthesized Rotor Profiles
Deploying neural network generative design to optimize rotor cross-sections. Machine-learning algorithms simulate boundary layer turbulence and thermal deformation in real time, developing asymmetric geometry that achieves up to 4.2% higher specific flow rate per revolution.
Silicon Carbide (SiC) Inverters
Transitioning from standard silicon IGBT switches to wide-bandgap Silicon Carbide (SiC) semiconductors. SiC power stages operate at higher switching frequencies with 70% lower internal switching losses, sustaining 99.2% electrical inverter conversion efficiency even under heavy ambient conditions.
Thermodynamic Heat Recovery Skids
Up to 94% of the electrical energy supplied to a screw compressor converts directly into thermal heat within lubricating oil and cooling circuits. Our integrated heat recovery exchangers capture this energy, delivering water up to 85°C for boiler pre-heating, plant district heating, and sanitary uses.
Industrial IoT Edge Telematics
Edge processors run high-frequency FFT vibration analysis, exhaust temperature variance diagnostics, and oil differential monitoring on each unit. Maintenance alerts trigger predictively hundreds of hours ahead of scheduled maintenance, preventing unplanned plant downtime.
Ceramic Hybrid Airend Bearings
To accommodate higher rotational speeds and extreme temperature swings without degradation, our next-generation units implement silicon nitride (Si3N4) ceramic rolling elements. Friction coefficients drop by 45%, electrical current corrosion is eliminated, and bearing operational life extends beyond 150,000 hours.
Smart Grid Autonomous Shaving
Equipped with automated demand-response software, compressors sync directly with factory energy management systems (EMS). Units autonomously adjust working pressure bands based on spot electricity tariff rates, running higher storage buffers during off-peak windows to reduce power bills.
Worldwide Compliance, Localized Spares & Port Clearance
Operating across 50+ export jurisdictions requires stringent adherence to international safety, pressure vessel, and environmental protocols. We handle complete documentation sets for prompt customs clearance.
International Regulatory Approval
Fully compliant with the European Union CE Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, and Pressure Equipment Directive (PED 2014/68/EU). Certified under ISO 9001:2015, ISO 14001, and ISO 8573-1:2010 Class 0 by accredited inspection bodies.
Pressure Vessel Codes (ASME / MOM / DOSH)
Oil-air separation vessels and bulk receiver tanks are stamped in accordance with ASME Section VIII Div 1 for North America, MOM regulations for Singapore, and DOSH certifications for Malaysia. Full hydro-test dossiers, weld radiographs, and safety valve certs are supplied with each crate.
Standardized Global Consumables
To safeguard end-users against vendor lock-in, our filtration components use standard screw pitch and flange geometries compatible with major industrial filter providers worldwide. High-performance synthetic lubricants meet universal polyalphaolefin (PAO) grade standards.
Specialized Heavy-Duty & Two-Stage Compressors
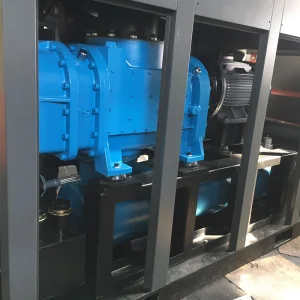
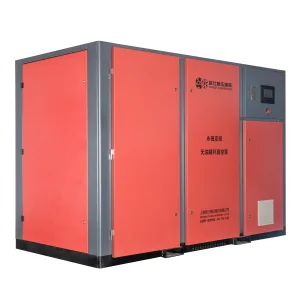
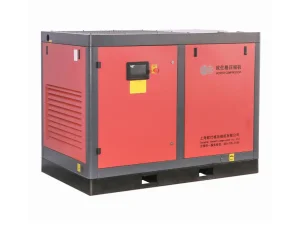
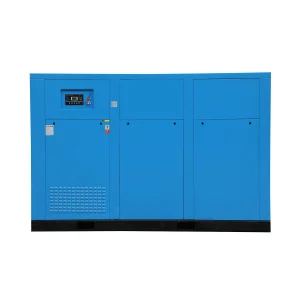
Expanding our manufacturing catalog with high-volume two-stage rotary screw configurations, heavy industrial vacuum systems, and multi-voltage water-lubricated units for heavy industrial manufacturing.


Frequently Answered Engineering & Procurement Queries
In-depth technical answers addressing rotor profile mechanics, efficiency boundaries, power conversions, and turnkey ODM manufacturing logistics.
