
Engineered 60 Hp & Heavy-Duty Compression Machinery
Browse our factory-direct industrial platforms optimized for 24/7 continuous duty cycles, unmatched specific power efficiency, and rigorous global grid adaptability.
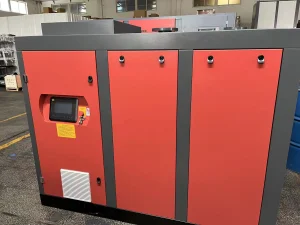
ODM electrical motor PM AC ASD rotary air vaccum pump compressor screw compressor Manufacturer, Manufacturers
View Product Specs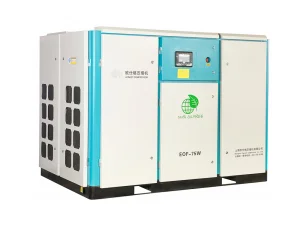
China 55kw to 315kw Oil free screw air compressor with dry type fixed speed or VSD PM type Suppliers, Exporters
View Product Specs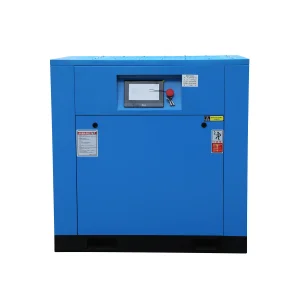
OEM Industrial 15kw/22kw/37kw/55kw/75kw Energy Saving Pm Motor VSD/VFD Rotary Screw Air Compressor Manufacturer, Exporters
View Product Specs
OEM Oil Free Water Lubricated Screw Air Compressor 37kW Supplier, Factories
View Product Specs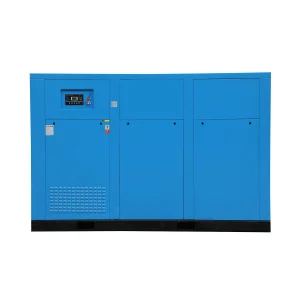
China 110Kw/150Hp Two-Stage Rotary Screw Air Compressor Permanent Magnetic Variable Frequency 380V Air Cooled Exporter, Exporters
View Product Specs
ODM IP55/54 55KW 75HP Factory Price Two Stage Industrial Screw Type Air Compressor Machine Factories, Exporters
View Product Specs
OEM Hot Sale China Factory High Quality Screw Vacuum Pump Permanent Magnet Frequency Conversion Progressive Pump Manufacturers, Factories
View Product Specs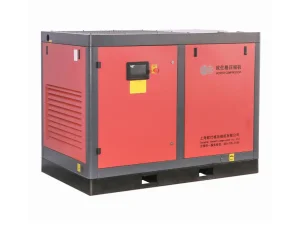
OEM Energy Saving Air Cooling Screw Compressor Two Stage Direct Driven Screw Air Compressor Manufacturers, Exporters
View Product SpecsThe Global Workhorse: Commercial Status of 60 Hp (45 kW) Air Systems
In modern thermodynamic engineering, the 60 Horsepower (45 Kilowatt) rotary screw compressor represents the foundational baseline for global mid-to-large-scale manufacturing infrastructure.
Baseline Operational Dominance
The 60 Hp category delivers between 7.0 and 8.2 m³/min (247–290 CFM) of Free Air Delivery (FAD) at typical working pressures ranging from 7.0 to 13.0 bar (100–188 PSI). Globally, this volumetric output directly satisfies approximately 42% of all automated discrete manufacturing plants, stamping lines, and pneumatic conveyance hubs, operating as either the sole plant compressor or a synchronized modular module.
Energy Decarbonization Mandates
With industrial electricity accounting for over 76% to 82% of a rotary screw compressor's Total Cost of Ownership (TCO) over a 10-year lifecycle, international regulatory frameworks (EU Ecodesign Lot 31, US DOE 10 CFR Part 431) have shifted global demand away from legacy fixed-speed modulating valves toward high-efficiency permanent magnet variable-frequency drives (PM VFD).
Industrial IIoT Telemetry Integration
Modern commercial purchasers no longer source standalone pneumatic mechanical pumps; they procure integrated cyber-physical nodes. Current OEM 60 Hp units integrate micro-differential transducers, predictive vibration monitoring on rotor bearings, Modbus RTU/TCP protocols, and automated condensate purge control to minimize unmetered downtime.
Why Global Brands Source 60 Hp Units from Chinese Industrial Hubs
Modern Chinese OEM rotary screw compressor factories—such as Honest Compressor's British-engineered 50,000 m² Jiading, Shanghai base founded in 2004—deliver a structural synergy of specialized clustering, robotic machining, and comprehensive international testing compliance.
Tier-1 Component Ecosystem
Within a 90-kilometer industrial corridor, our manufacturing lines access specialized rotor forging foundry works, precision CNC profile milling from Kapp Niles and Klingelnberg, high-grade silicon steel stator windings, and customized European-spec vector frequency inverters. This spatial concentration eliminates intermediate logistical friction, dropping prototype-to-production lead times to 15–20 working days.
Asymmetric 5:6 Screw Rotor Profiling
Chinese OEM engineering incorporates third-generation 5-lobe male and 6-flute female helical screw geometries. This asymmetric aerodynamic profile maximizes dynamic sealing line length, reduces internal blow-hole back-leakage, and maintains exceptional volumetric efficiency (>96%) at direct shaft coupling speeds without intermediary power-wasting gearboxes.
Multi-Jurisdictional Certification
Exporting to over 50 global economies requires exhaustive code compliance. High-tier Chinese facilities engineer pressure vessels directly compliant with ASME Boiler and Pressure Vessel Code Section VIII (Div 1), European Pressure Equipment Directive (PED 2014/68/EU), CE Machinery Directives, and UL/CSA dual-rated electrical controls.
Engineering Evolution: 60 Hp Core Technological Trends
Examine the shifts in thermodynamic cycles, magnetic materials, and air purity configurations redefining performance expectations in the 45 kW sector.
| Architecture Type | Motor Technology | Specific Power (kW/m³/min) | Thermal Distribution | Best Suited Application |
|---|---|---|---|---|
| 60 Hp Single-Stage Fixed Speed | IE3 Induction (TEFC) | 6.8 – 7.4 @ 8 Bar | High single-stage pressure ratio (8:1) | Continuous base load with 100% constant air demand. |
| 60 Hp Single-Stage PM VFD | IE4/IE5 Permanent Magnet (Oil-Cooled) | 5.9 – 6.5 @ 8 Bar | Modulated heat load via variable speed | Dynamic production schedules with fluctuating flow requirements. |
| 60 Hp Two-Stage Compression PM VFD | Dual IE5 Permanent Magnet Motors | 5.1 – 5.6 @ 8 Bar | Low stage ratios (~2.8:1) with inter-stage cooling | Heavy industrial 24/7 continuous duty seeking absolute lowest kWh/year. |
| 60 Hp Class 0 Oil-Free Dry Screw | IE4 VFD Synchronous Reluctance | 6.5 – 7.1 @ 8 Bar | High-temp dry chamber with thermal jacket | Critical pharmaceutical, semiconductor, and food packaging processes. |
| 60 Hp Water-Lubricated Oil-Free | IE4 Permanent Magnet Direct | 5.8 – 6.3 @ 8 Bar | Isothermal compression cooled by DI water injection | Ultra-clean electronic, medical air, and high-purity chemical plants. |
Rare-Earth Permanent Magnet Synchronous Motors
Unlike standard asynchronous induction induction drives that suffer steep rotor slip losses at partial loads, oil-cooled PMSM drives maintain >96.5% electrical-to-mechanical conversion efficiency across a wide 20% to 100% speed envelope. Their IP66/IP55 oil-cooled enclosures prevent dust ingress and demagnetization even at operating temperatures approaching 180°C.
Two-Stage Compression Advantage
By dividing the overall pressure ratio between two distinct rotor sets connected in series with an atomized oil inter-stage cooling curtain, the compression approach approaches the ideal isothermal thermodynamic cycle. Internal back-leakage across rotor tips drops by up to 50%, producing 12% to 18% higher volumetric CFM per input kilowatt compared to single-stage units.
Class 0 Certified Purity Architecture
Zero tolerance for hydrocarbons in lithium battery cathode lines, cleanroom automation, and parenteral drug formulation has catalyzed adoption of 60 Hp oil-free models. Certified strictly to ISO 8573-1:2010 Class 0, these machines utilize food-grade polyether ether ketone (PEEK) coatings or direct deionized water injection to guarantee pure, oil-free pneumatic power.
Localized Factory Applications for 60 Hp Platforms
A 60 Hp rotary screw compressor is configured precisely to the process medium, duty variation, and purity requirements of specific production environments.
1. High-Pressure Laser Cutting (16–25 Bar)
Equipped with a reinforced 60 Hp high-pressure airend or booster setup, delivering clean, dry, oil-free compressed air directly to fiber laser cutting heads (6 kW to 20 kW). Serving as an energy-efficient alternative to high-pressure bottled nitrogen assist gases, saving up to 70% in operating consumable costs when cutting stainless and carbon steels.
2. Automotive Assembly & Paint Robotics
Supplying steady 7.5 bar instrument air across robotic spot-welding pneumatic clamps, pneumatic transfer conveyors, and automated electrostatic spray finishing booths. Integrates with integrated refrigerant and desiccant dryers to eliminate paint surface cratering caused by aerosol moisture or trace lubricant vapor.
3. Semiconductor & Battery Gigafactories
Providing high-volume ultra-dry purge air (-40°C to -70°C pressure dew point) for cleanroom automated material handling systems (AMHS) and vacuum drying chambers in lithium-ion pouch cell manufacturing. PM VFD technology prevents line pressure swings from unsettling sensitive wafer staging systems.
4. Food & Beverage Packaging Automation
Deploying 60 Hp oil-free water-lubricated units for direct-contact bottle blowing (PET preform staging), vacuum pick-and-place packaging, clean-in-place (CIP) pneumatic valves, and nitrogen membrane generation for modified atmosphere packaging (MAP), preventing rancidity or contamination.
5. Textile Air-Jet Spinning & Weaving
Modern air-jet weaving looms consume enormous continuous volumes of compressed air at 5.5 to 7.0 bar. A 60 Hp two-stage screw platform running continuously 8,760 hours/year in high ambient heat and humidity delivers ultra-low specific energy, drastically lowering mill production overhead per meter of fabric.
6. Pharmaceutical Powder Conveying
Dense-phase pneumatic conveying of active pharmaceutical ingredients (APIs) and dry tablet compression requiring continuous positive displacement pressure. Configured with stainless steel internal piping, anti-microbial synthetic lubricants, and ISO 8573 Class 1 particulate filtration downstream.
B2B Sourcing Protocol: Total Cost of Ownership (TCO)
Strategic equipment procurement requires looking beyond initial machinery purchase price (CapEx). Compressed air is an ongoing operating expense (OpEx) governed by the 80/12/8 thermodynamic lifecycle formula.
The 80/12/8 Lifecycle Financial Model
Over a 5-year operating window (running 6,000 hours per annum), electricity accounts for roughly 80% of total lifecycle cost, initial factory acquisition cost represents only 12%, and routine maintenance (oil changes, air/oil separators, filters) totals 8%. Selecting a unit with 10% better specific power saves more money within 18 months than the compressor's entire initial purchase price.
Specific Power Auditing (kW / 100 CFM)
Demand documented factory test logs conducted under ISO 1217:2009 Annex C standards. Verify the true input electrical power across full-load and part-load operational steps. High-tier 60 Hp screw compressors should achieve a specific power rating under 6.2 kW per m³/min (approximately 17.5 kW/100 CFM) at 8.0 bar gauge working pressure.
Supply Chain Continuity & Spares
Evaluate factory support for universal replacement components. Honest Compressor guarantees global interchangeability on wear items: spin-on synthetic air/oil separator elements, micro-fiber intake filters, thermostatic mixing valves, and universal PLC touch controls with multi-language Modbus telemetry for third-party SCADA integration.
Factory Metrology: How We Build Reliability into Every Airend
At our 50,000 m² Shanghai facility, production relies on rigid physical inspection gates—from casting alloy analysis to dynamic balance testing—ensuring 24/7 reliability in demanding field conditions.
CMM Profile Metrology (±1.5 μm)
Every milled screw rotor is verified on Zeiss coordinate measuring machines (CMM) inside temperature-controlled metrology suites. Flute profiles, pitch angles, and tip clearances are held within sub-micron tolerances, ensuring minimal thermodynamic slip, zero casing interference, and extended airend lifespan.
ISO 1940 Grade G2.5 Balancing
Rotor shafts, cooling blowers, and flexible drive hubs undergo multi-plane dynamic balancing at speeds exceeding maximum rated RPM. Vibration is strictly maintained below 1.2 mm/s RMS, protecting SKF/FAG cylindrical roller bearings against premature spalling or thermal fatigue under continuous load.
Full-Load 4-Hour Thermal Run-In
Before crating and shipment, every completed 60 Hp compressor undergoes automated full-load bench testing. Flow velocity (nozzle method), electrical power factor, sound power levels, and operating oil temperature equilibrium are monitored continuously to guarantee out-of-the-box readiness.
Specialized OEM/ODM Pneumatic & Vacuum Assemblies
Explore our oil-free blowers, high-pressure laser systems, vacuum pumps, and specialized variable-frequency compression machinery manufactured for export worldwide.
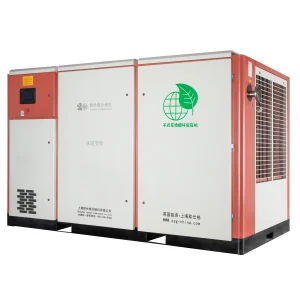
ODM EOF Oil-Free Dry Screw Compressor | 100% Oil-Free PM VFD Manufacturers, Factory
View Product Specs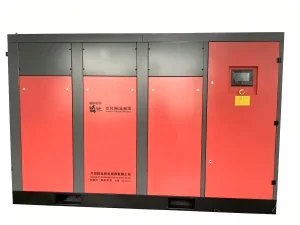
China EGV-132A-140 Oil-Free Permanent Magnet VFD Screw Blower Manufacturers, Exporters
View Product Specs
OEM Industrial Screw Vacuum Pumps – Oil-Injected (0.35 mbar) & Oil-Free (20–80 kPa) Series, 5.5–110 kW Supplier, Exporter
View Product Specs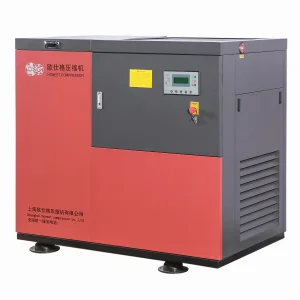
China 20bar pressure Screw Air Compressor for laser cutting machine Supplier, Suppliers
View Product Specs
ODM PM&VSD Oil‑Free Screw Blower Factories, Exporters
View Product Specs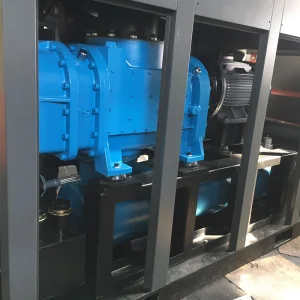
OEM Industrial Oil Free Vsd Screw Air Blower /Vacuum Pump With Inverter and Pm Motor Manufacturer, Exporter
View Product Specs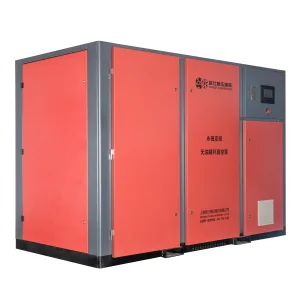
ODM PM VFD Dry Oil-Free Screw Vacuum Pump for Industrial Clean Vacuum Manufacturer, Suppliers
View Product Specs
OEM 30kW 40HP Permanent Magnet VFD Air Compressor Manufacturers, Factories
View Product SpecsFrequently Asked Questions: 60 Hp Compressor Engineering
Technical, thermodynamic, and procurement insights prepared by our chief application engineering team.
What is the expected CFM of a 60 Hp rotary screw compressor at various pressures?
Under ISO 1217 Annex C conditions, a 60 Hp (45 kW) single-stage oil-injected compressor yields approximately 280–290 CFM (7.9–8.2 m³/min) at 7.0–7.5 bar (100–110 PSI); 255–265 CFM (7.2–7.5 m³/min) at 8.5 bar (125 PSI); and 215–230 CFM (6.1–6.5 m³/min) at 10.0–10.5 bar (150 PSI). Two-stage variations increase output volume by roughly 12% to 15% across identical motor inputs.
How does an IE4/IE5 permanent magnet motor save energy compared to an induction motor?
Induction motors rely on electromagnetic induction from the stator to create rotor flux, creating rotor copper and slip losses that worsen significantly at partial loads. Permanent magnet synchronous motors (PMSM) use rare-earth NdFeB magnets that rotate synchronously with the stator field, eliminating slip losses and maintaining 96%+ efficiency even when operating down to 25% of rated full-load capacity.
When should a plant specify a Two-Stage 60 Hp compressor instead of a Single-Stage unit?
Specify a two-stage 60 Hp model if your facility operates more than 4,500 hours annually, uses steady continuous base-load volume, and pays over $0.09 per kWh for grid electricity. The two-stage architecture lowers the pressure ratio per stage (~2.8:1 instead of 8:1), cuts bearing thrust forces, and lowers specific power requirements, usually returning its capital premium within 12 to 18 months.
What is the difference between Class 0 Dry Screw and Water-Lubricated technologies?
Dry screw compressors compress air without any liquid in the compression chamber; the rotors run dry and rely on timing gears to prevent rotor contact. They operate at high speeds and discharge air at elevated temperatures. Water-lubricated screw units inject purified water directly into the chamber, which provides continuous lubrication and cooling, resulting in a near-isothermal compression process at lower rotor speeds.
Can Honest Compressor build OEM units with specific voltage and frequency requirements?
Yes. As a direct OEM factory, we customize drive systems for worldwide grid configurations: 380V/50Hz, 400V/50Hz, 415V/50Hz for Europe, Asia, and Oceania; and 208V/60Hz, 230V/60Hz, 460V/60Hz, 575V/60Hz for North American industrial networks. Inverters and control systems carry dual UL/CE electrical certification marks.
How does variable speed drive (VFD) prevent "blow-off" and motor idling losses?
Fixed-speed compressors switch to an idle state when plant air pressure reaches its upper limit. In idle, the intake valve closes, venting residual sump pressure, while the motor continues to draw 25% to 40% of its full-load power without delivering useful air. A PM VFD tracks system pressure fluctuations and alters rotor speed in real time, matching air delivery to demand and avoiding idle power waste entirely.
What size receiver tank is required for a 60 Hp rotary screw compressor?
A standard engineering guideline is 3 to 5 gallons of receiver capacity per rated CFM for fixed-speed compressors, requiring an 800 to 1,200 gallon (3,000–4,500 L) air tank to absorb rapid load swings. For a PM VFD 60 Hp compressor, because the machine modulates speed smoothly to meet demand, the receiver size can often be reduced to 1 to 2 gallons per CFM (300 to 500 gallons / 1,000–2,000 L) while still maintaining stable line pressure.
What routine maintenance intervals apply to an industrial 60 Hp screw compressor?
Routine service intervals for our 60 Hp oil-injected units include: air filter replacement every 2,000 to 3,000 operating hours; oil filter replacement every 2,000 hours; synthetic coolant replacement every 4,000 to 6,000 hours (depending on ambient temperatures); and spin-on air/oil separator replacement every 4,000 hours (or when differential pressure exceeds 0.8 bar).
Request an OEM Sizing Review & TCO Energy Audit
Evaluating an upgrade for existing manufacturing operations or specifying pneumatic generation packages for a greenfield facility? Submit your target volumetric flow (CFM or m³/min), working pressure (bar/PSI), supply voltage, and environmental conditions. Our Shanghai application engineering team will prepare a full ISO 1217 thermodynamic performance report and custom factory quote.
