
Precision OEM Industrial Compressors: Air-Cooled Solutions
Explore our foundational range of heavy-duty, high-efficiency twin-screw and oil-free compressors engineered for maximum uptime, thermal endurance, and verified energy savings.
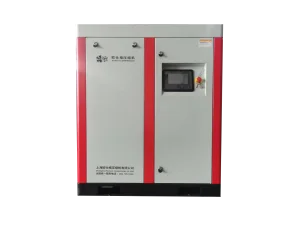


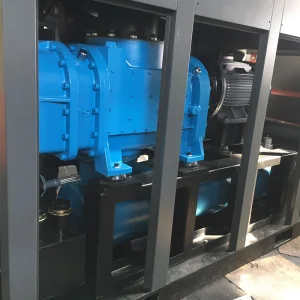
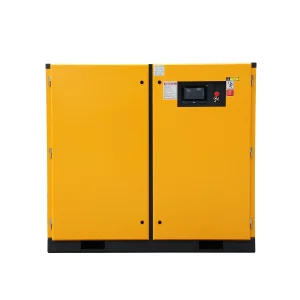


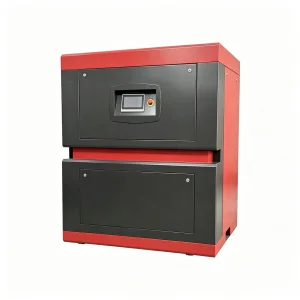
Engineering Excellence in Air-Cooled Compression Technology
Thermodynamic supremacy, mechanical durability, and total lifecycle optimization form the foundation of our British-engineered manufacturing facility in Jiading, Shanghai.
Elimination of Liquid Cooling Infrastructure
Traditional water-cooled installations demand massive ancillary investments: cooling towers, centrifugal circulation pumps, chemical biocide treatments, de-scaling maintenance, and freeze protection circuits. Our heavy-duty air-cooled rotary screw compressors bypass these CAPEX and OPEX sinks completely. Engineered with high-surface-area aluminum bar-plate heat exchangers, these machines dissipate thermodynamic heat directly into the ambient airflow with zero water consumption.
- Zero cooling water supply or discharge costs
- Eliminates shell-and-tube scaling & corrosion
- Plug-and-play installation for rapid plant rollout
Advanced Variable Aerodynamics & Fans
Conventional air compressors employ fixed-speed induction cooling fans that consume parasitic power continuously, irrespective of load conditions. Our OEM systems integrate aerodynamically optimized centrifugal cooling fans governed by internal thermostatic PID logic. The fan dynamically modulates RPM based on discharge oil temperature, maintaining the core lubricating fluid within the ideal viscosity envelope while preventing internal moisture condensation during low-load intervals.
- Centrifugal low-noise backward-curved impellers
- Dew-point protection prevents oil emulsification
- Parasitic fan power reductions up to 55%
Tropicalized Thermal Endurance (Up to 52°C)
Factory environments in the Middle East, Southeast Asia, and Central America frequently challenge ambient limits. Every Honest Compressor air-cooled chassis incorporates oversized oil coolers and aftercoolers with wide fin pitch to resist particulate clogging. Thermal modeling ensures that the compressed air discharge temperature does not exceed ambient +10°C, providing pre-conditioned, manageable intake air for downstream desiccant or refrigerated dryers.
- Wide-pitch fins prevent fibrous dust clogging
- Discharge approach temperature: Ambient +8°C to +12°C
- Rated for continuous 24/7 run under severe ambient heat
China Factory 4.0: Supply Chain Resilience & Quality Rigor
Operating from our 50,000 m² facility at No. 355 Jiajian Branch Road, Malu Town, Jiading District, Shanghai, we unite British mechanical design standards with China's rapid, fully vertically integrated industrial supply chain.
5:6 Asymmetric Rotor Precision Machining
The core of our rotary screw platform lies in proprietary rotor profiles ground on Klingelnberg and Holroyd CNC rotor grinding machines. Maintaining micron-level clearances between the male and female helical rotors guarantees minimal blow-hole leakage, exceptionally high volumetric efficiency, and an extended operational life exceeding 80,000 hours without airend rebuilds.
- Micron-tolerance grinding ensures maximum volumetric flow
- SKF / Timken high-precision bearing arrangements
Full-Load Aerodynamic & Thermal Testing Rigs
Every single compressor exiting our Shanghai production line undergoes full-load computerized testing before crating. Using calibrated ISO 1217 Annex C & Annex E flow nozzle nozzles, our engineers record Free Air Delivery (FAD), Specific Power Consumption (kW/m³/min), thermal dissipation curves, vibration FFT spectra, and electrical harmonics across the complete operating speed range.
- 100% factory run-in testing with verified data sheet
- Sound level acoustic chamber verification to ISO 2151
Localized Supply Clustering in Greater Shanghai
The Jiading industrial corridor provides unmatched logistics synergy. Over 85% of critical structural casting, high-grade forged steel, precision solenoid valves, electrical contactors, and pressure sensors are sourced within a 100-kilometer radius. This tight geographic integration buffers global OEM buyers against geopolitical supply shocks, shrinking standard production lead times to just 2 to 4 weeks.
- Resilient tier-1 component sourcing ecosystem
- Direct sea container loading from Port of Shanghai
Technological Roadmap & Future Innovation Outlook
The industrial compressed air sector is navigating a major generational transition toward ultra-premium efficiency, low-carbon footprints, and intelligent autonomous control.
| Architecture Subsystem | Legacy Industry Standard | Honest Compressor Generation 4.0 | Next-Gen R&D Roadmap (2026+) | Operational Value Proposition |
|---|---|---|---|---|
| Drive Motor Technology | IE2 / IE3 Asynchronous Induction | IE4 / IE5 Oil-Cooled Permanent Magnet (PMSM) | IE6 Ultra-Super-Premium Magnetless Reluctance | 6–9% Electrical Gain Across Full Speed Range |
| Compression Staging | Single-Stage Rotary Compression | Dual-Stage Direct-Driven Screw Pairs | Isothermal Multi-Stage Water Injection | Lowers Inter-Stage Pressure Ratio ($\sqrt{\Pi}$) |
| Lubrication Medium | Mineral & PAO Synthetic Oils | Food-Grade Synthetic / Water-Lubricated | Solid Polymeric Self-Lubricating Rotors | Zero Hydrocarbon Risk (ISO Class 0 Pure) |
| Air Cooling Dynamics | Fixed-Speed Direct Axial Fan | Thermostatic Centrifugal Variable Fan | Closed-Loop Phase Change Heat Recovery | Up to 80% Thermodynamic Heat Reusable |
| Control & Telemetry | Relay Logic / Basic Microcontroller | 7" Touch PLC with Modbus / Cloud IoT | Edge-AI Predictive Vibration FFT Algorithms | Zero Unscheduled Downtime via Bearing Telemetry |
IoT Edge Telemetry & Cloud Fleet Sync
Every Honest Compressor OEM chassis can be configured with an onboard IoT gateway communicating over 4G LTE, Ethernet, or RS485 Modbus. Operating parameters—including intake filter differential pressure, inter-stage temperature, motor winding resistance, and oil saturation—are monitored continuously. Cloud dashboards provide plant engineers with automated oil-change countdowns, anomaly alarms, and energy efficiency audit curves.
Dual-Stage Thermodynamic Compression
Splitting the total pressure ratio between two distinct male/female rotor pairs lowers the thermodynamic compression ratio of each stage. By integrating intermediate oil mist or air-cooling between stages, the thermodynamic compression cycle shifts significantly closer to the idealized isothermal baseline. This physical law translates into an immediate 15% to 20% reduction in specific energy compared to conventional single-stage compressors operating at 8 to 13 bar.
Direct-Driven Shaft-Integrated Architecture
By coupling the permanent magnet rotor directly onto the male rotor drive shaft, we eliminate intermediate gearbox friction losses, pulley slippage, and radial bearing stresses. The 1:1 direct drive mechanism operates with a mechanical transmission efficiency of 99.9%, drastically lowering acoustic emissions and guaranteeing that zero torque is squandered between the motor stator and the compression chamber.
Engineered Industry Solutions: Targeted Performance Metrics
No two manufacturing environments face the same air quality, pressure demand, or thermal stresses. We custom-engineer OEM packages tailored to specific sector requirements.
High-Precision Fiber Laser Cutting (16–30 Bar)
Modern high-wattage fiber laser cutting machines (12kW to 40kW) increasingly replace costly liquid nitrogen assist gas with dry, high-pressure compressed air. Our specialized booster and air-cooled 20-bar/30-bar screw platforms incorporate integrated refrigerated dryers and four-stage oil-removal coalescing filters. This ensures burr-free cuts on stainless steel, aluminum, and carbon steel without lens contamination.
- Solid particle retention down to 0.01 micron
- Residual oil content ≤ 0.003 mg/m³
- Immediate 70%+ savings versus bulk liquid nitrogen
Pharmaceuticals, Food & Beverage (ISO Class 0)
Where compressed air comes into direct contact with consumable packaging, active pharmaceutical ingredients (APIs), or sterile fermentation vessels, zero trace oil can be tolerated. Our water-lubricated single-screw and dry-type two-stage rotary screw compressors use pure water or PTFE/MoS2 synthetic coatings, guaranteeing certified Class 0 purity under ISO 8573-1 without risk of batch adulteration.
- Zero hydrocarbon carryover across all pressure bands
- Stainless steel rotor housing prevents biological biofilm
- Meets strict FDA, GMP, and EU pharmacopeia norms
Semiconductor, Electronics & Solar Photovoltaic
Cleanroom pneumatic actuators, wafer spin-dryers, and solar cell screen-printing systems require pressure dew points down to -40°C or -70°C, combined with continuous, micro-vibration-free compressed air. Our air-cooled packages are precision dynamically balanced to G1.0 balancing standards, isolated on rubber-damper chassis, and integrated with heatless or heated desiccant dryers.
- Ultra-low residual moisture dew points (-40°C to -70°C)
- Dynamic balance ISO 1940 Grade G1.0
- Suppresses line pressure ripples for micro-actuators
Explosion-Proof & Hazardous Petrochemical Sites
For chemical reactors, offshore platforms, and paint finishing workshops classified as Zone 1, Zone 2, Zone 21, or Zone 22, we engineer ATEX / IECEx / Ex d IIB T4 explosion-proof air-cooled compressors. Flameproof motor enclosures, intrinsically safe control panels, anti-static cooling fan impellers, and stainless-steel electrical conduit prevent spark or thermal ignition risks.
- Certified Ex d IIB / IIC T4 explosion-proof architecture
- Non-sparking brass and composite cooling fan blades
- Stainless steel electrical hardware & armored cables
Global Enterprise Procurement: Total Cost of Ownership Analysis
Experienced procurement officers evaluate compressed air systems through a 10-year lifecycle financial model, recognizing that the initial equipment purchase price represents only a fraction of overall costs.
The 10-Year Lifecycle Formula
Over a standard decade of operation (6,000 running hours/year), a 75kW compressor will consume over 4.5 million kWh of electricity. Total lifecycle expenditure breaks down into:
- 76% Electricity Costs: Direct grid power draw
- 12% CAPEX: Initial machine procurement & installation
- 12% Maintenance: Lubricants, filters, separators, labor
Procurement Takeaway: A machine priced 20% lower at purchase, but carrying a 10% higher specific power consumption (kW/m³/min), ends up costing vastly more within just 18 to 24 months of continuous operation.
Worldwide Power Customization (OEM/ODM)
Exporting to multi-national operations requires engineering versatility. Honest Compressor custom-winds and certifies drive motors and inverters across the full spectrum of global regional voltages:
- North America: 208V / 230V / 460V / 575V (60Hz)
- Europe / Asia / Africa: 380V / 400V / 415V (50Hz)
- Latin America / Japan: 220V / 440V (50/60Hz dual)
- PLC interface in English, Spanish, Russian, Arabic, French
OEM Private-Label & SKD Programs
For regional compressor distributors, engineering brands, and EPC contractors, we offer complete OEM private labeling programs. From custom-matched RAL industrial powder coatings and laser-cut branding fascias to specialized enclosure footprints, dual-source filtration cartridges, and Semi-Knocked-Down (SKD) containerized kits for localized assembly, we scale with your business model.
- Bespoke enclosure industrial design & RAL colors
- Custom branded PLC touchscreen human-machine interface
- Protected regional exclusivity arrangements available
Regulatory Compliance & Global Certification Standards
Ensuring frictionless import customs clearance, local occupational safety sign-offs, and compliance with statutory pressure vessel codes across major export destinations.
European Directives (CE & PED)
Full CE certification adhering to Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, and Electromagnetic Compatibility Directive 2014/30/EU. Air-oil separation vessels and air tanks conform strictly to Pressure Equipment Directive (PED 2014/68/EU) with third-party notified body inspection stamps.
North American ASME & UL/CSA Standards
Pressure vessels fabricated with ASME Section VIII Division 1 U-stamp documentation for deployment in the United States and Canada. Electrical cabinets wired with UL 508A certified components, NEMA-rated enclosures, and National Electrical Code (NEC) compliant wiring harnesses.
EAC (TR CU) & Middle East SASO / G-Mark
Verified conformity with Eurasian Customs Union technical regulations TR CU 010/2011 (Machinery Safety), TR CU 004/2011 (Low Voltage Equipment), and TR CU 020/2011 (EMC). Fast-track SASO Saber registration and Gulf Conformity (G-Mark) compliance for Gulf Cooperation Council markets.
ISO 9001, ISO 14001 & ISO 45001 Systems
Every compressor is manufactured under ISO 9001:2015 Quality Management, ISO 14001:2015 Environmental Management, and ISO 45001:2018 Occupational Health & Safety audited frameworks. Complete factory documentation includes traceable material test reports (MTRs), hydro-test certificates, and run-in logs.
Specialized Heavy Industrial Compressors & Vacuum Systems
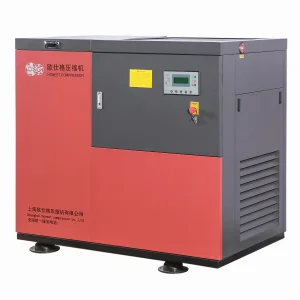
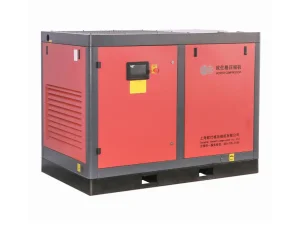
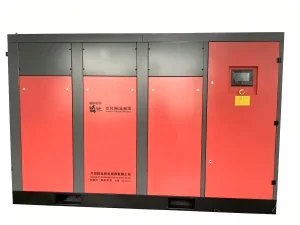
Explore high-pressure laser cutting packages, heavy-duty screw vacuum pumps, two-stage energy-saving platforms, and oil-free screw blowers tailored for specialized production lines.





Frequently Asked Questions: Engineering & Procurement Insights
Expert answers addressing the primary design, selection, sizing, and lifecycle operational considerations for global air-cooled rotary screw compressor installations.
How do air-cooled industrial screw compressors compare to water-cooled units regarding overall lifecycle efficiency and maintenance?
While water has a higher specific heat capacity than air, modern air-cooled screw compressors offer distinct total-cost advantages for the vast majority of industrial plants. Water-cooled systems require continuous raw water intake, water softening equipment, chemical anti-algae and corrosion inhibitors, periodic acid descaling of heat exchanger tubes, and winter freeze-drainage systems. In contrast, heavy-duty air-cooled compressors utilize oversized aluminum bar-plate heat exchangers that dissipate heat directly into the atmosphere. With zero water consumption, zero risk of thermal scale calcification, and maintenance limited to routine blowdown cleaning of cooler fins, air-cooled units provide a significantly lower 10-year Total Cost of Ownership (TCO) and rapid plug-and-play installation.
What specific energy savings can a Permanent Magnet Variable Frequency Drive (PM VFD) compressor achieve versus a fixed-speed load/unload machine?
In standard manufacturing plants, compressed air demand fluctuates significantly between shifts, batch runs, and tooling cycles. A conventional fixed-speed compressor accommodates fluctuating demand by cycling between "Load" and "Unload" modes. In "Unload" mode, the motor continues drawing between 40% and 70% of its full-load rated power while delivering zero useful compressed air—wasting massive amounts of electricity. Our Permanent Magnet VFD compressors continuously regulate motor RPM to match real-time system flow demand, keeping line pressure within a narrow ±0.01 MPa band. By eliminating idle blowing-off losses, transient motor starting inrush current, and excess pressure over-compression, our PM VFD platforms deliver verified electrical savings between 20% and 40%, with payback periods typically under 14 months.
What is the thermodynamic advantage of a two-stage rotary screw compressor over a single-stage machine?
Thermodynamic work is governed by the compression ratio ($P_2/P_1$). In a single-stage compressor operating at 8 bar (approx. 9 bar absolute), the entire compression occurs across one rotor pair, resulting in high internal pressure differentials, increased rotor blow-hole back-leakage, and elevated discharge temperatures approaching 95°C to 100°C. In a two-stage compressor, the compression is split into two sequential stages. The first stage compresses air to an intermediate pressure ($\approx 3$ bar), where oil mist inter-cooling cools the air before it enters the second stage. This inter-stage cooling shifts the compression path closer to the ideal isothermal compression curve, cutting thermodynamic compression work by 15% to 20%. Furthermore, because the pressure differential across each individual rotor pair is reduced, bearing radial loads decrease substantially, extending airend mechanical operating life beyond 100,000 hours.
How does Honest Compressor guarantee ISO 8573-1 Class 0 oil-free air purity in its water-lubricated models?
Our water-lubricated oil-free screw compressors utilize purified water as the internal lubricating, sealing, and cooling fluid within the compression chamber. Unlike oil-injected compressors that rely on coalescing separators to filter out mineral or synthetic lubricants, our water-lubricated chambers operate completely free of hydrocarbon compounds. Water is injected directly into the single-screw or twin-screw rotor meshing profile, creating a tight dynamic fluid seal at lower rotational speeds. Because water has a specific heat capacity more than double that of oil, the compression process remains near-isothermal, with operating discharge temperatures rarely exceeding 45°C to 50°C. The resulting compressed air is independently certified to ISO 8573-1 Class 0, ensuring zero risk of oil contamination in pharmaceutical cleanrooms, food processing plants, and optical fabrication lines.
What engineering modifications are incorporated to allow air-cooled units to run continuously in high-ambient environments up to 50°C?
Operating air-cooled equipment in desert climates or poorly ventilated compressor rooms requires specific engineering adaptations. Honest Compressor implements three key design parameters for tropicalized configurations: First, the surface area of both the aluminum oil cooler and compressed air aftercooler is oversized by 35% to 50% relative to standard European benchmarks, with wider fin pitch spacing to mitigate airborne dust clogging. Second, we integrate high-static-pressure centrifugal cooling blowers driven by dedicated variable-speed drives that maintain constant cooling air velocity even against dust filter backpressure. Third, the drive motor utilizes Class H electrical winding insulation (rated up to 180°C) with IP55 / IP65 enclosure protection, while high-temperature synthetic polyalphaolefin (PAO) lubricants with flash points exceeding 250°C prevent thermal fluid breakdown and varnish formation.
What is the standard procedure and lead time for OEM customization (voltage, color, controller, branding)?
Our OEM manufacturing workflow follows a structured engineering gateway process: Upon receipt of customer technical specifications (target flow, operating pressure, electrical supply voltage/frequency, ambient constraints, and compliance requirements), our application team generates an engineering submittal package within 48 hours. This includes 3D CAD step models, electrical schematic diagrams, and verified specific power curves. Following customer drawing sign-off, specialized component winding (e.g., 460V 60Hz or 415V 50Hz) and sheet metal laser cutting commence. Custom RAL powder coating, private-label silk-screen branding, and PLC multilingual firmware loading are executed in-house. Standard OEM production lead times at our Shanghai facility run from 2 to 4 weeks, with expedited 10-day turnaround available for standardized chassis variants.
How does an air-cooled screw compressor integrate with waste heat recovery systems to improve whole-plant energy efficiency?
Approximately 94% of the electrical energy supplied to an industrial air compressor is converted directly into thermodynamic heat during the compression process, with only about 6% remaining as potential energy in the compressed air stream. In our air-cooled OEM configurations, this thermal energy is concentrated primarily within the circulating oil circuit (approx. 72%) and aftercooler air stream (approx. 13%). By incorporating an optional internal heat exchanger module into the oil circuit before the air-cooling core, plants can capture hot water at 60°C to 80°C with zero degradation of compressor performance. This captured thermal energy can be piped directly to boiler preheating circuits, sanitary hot water loops, space heating radiators, or industrial cleaning baths—yielding overall plant energy recovery rates as high as 75% to 80% of total electrical draw.
What telemetry, cloud IoT, and Modbus capabilities are integrated into the control architecture?
All Honest Compressor modern industrial platforms feature our smart PLC control architecture with an integrated 7-inch color industrial touchscreen. The controller monitors and logs all vital operational metrics: individual phase voltages, motor currents, instantaneous power (kW), cumulative energy consumption (kWh), stage temperatures, oil pressure differentials, and maintenance countdown timers. Standard hardware interfaces include RS485 serial ports supporting native Modbus RTU/TCP protocols for seamless integration into enterprise SCADA or Distributed Control Systems (DCS). Additionally, optional cellular 4G LTE or Wi-Fi edge gateways enable cloud synchronization, allowing plant supervisors to monitor fleet health, receive automated SMS/email fault alerts, and download predictive vibration trend logs via our web portal or mobile applications.
