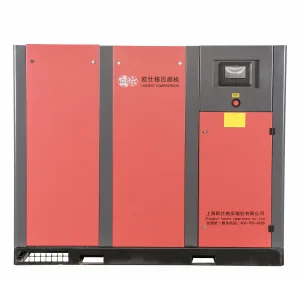
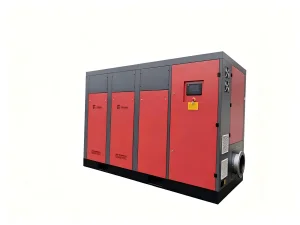
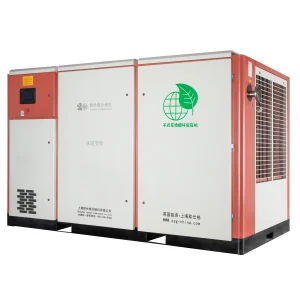
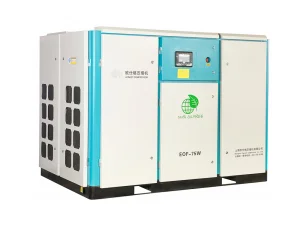
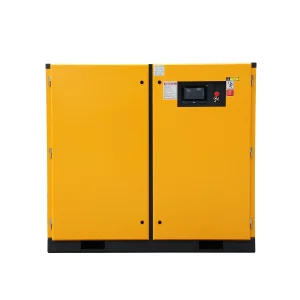
Featured OEM Air Cooled Screw Compressors
Precision-engineered rotary screw compressors designed for high volumetric yield, low operational dB(A), and zero-water consumption cooling.

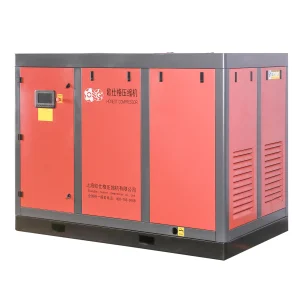


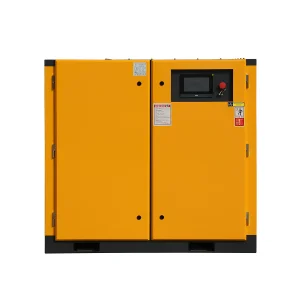
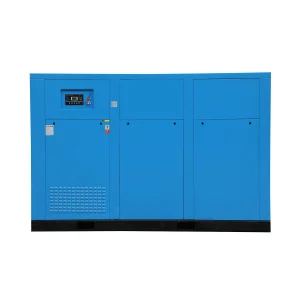
Global Commercial & Industrial Landscape of Air Cooled Screw Compressors
Analyzing macroeconomic energy mandates, thermal performance dynamics, and operational advantages driving global adoption.
The global market for industrial compressed air systems is undergoing a rapid paradigm shift. Historically viewed simply as utility hardware, air-cooled rotary screw air compressors are now evaluated as key strategic assets in corporate sustainability, decarbonization, and operational expenditure (OPEX) management. Across manufacturing hubs in North America, Europe, Southeast Asia, and the Middle East, the adoption of Air Cooled Screw Compressors has accelerated due to their zero-water footprint, installation versatility, and remarkable thermal dissipating capabilities.
1. Macro Energy Directives & Specific Energy Requirement (SER)
With industrial power costs climbing globally and stringent climate directives such as ISO 50001 (Energy Management) and EU Ecodesign mandates coming into force, factory procurement directors no longer focus purely on Capital Expenditure (CAPEX). Compressed air accounts for approximately 10% of total industrial electricity consumption globally. Over a 10-year lifespan, electricity accounts for nearly 75% to 80% of a screw air compressor's total cost of ownership (TCO).
Consequently, international demand has pivoted sharply toward high-efficiency Permanent Magnet Variable Frequency Drive (PM VFD) and Two-Stage Air Cooled Screw Compressors that minimize the Specific Energy Requirement (SER - measured in kW per m³/min). Air-cooled architectures eliminate the secondary electrical loads associated with water cooling loops, cooling towers, and water treatment pumps, yielding immediate overall system efficiency gains.
Engineering Insight: Isothermal vs. Adiabatic Efficiency
Compression generates significant heat. In an air-cooled screw compressor, efficient thermal removal via heavy-duty aluminum block heat exchangers and high-static-pressure axial fans brings the compression process closer to the ideal isothermal compression line. This drastically reduces the energy required to deliver each cubic meter of free air (FAD).
2. Strategic Comparison: Air-Cooled vs. Water-Cooled Systems
When selecting industrial compression architecture, engineering teams must weigh ambient environment parameters against infrastructure capabilities. Below is a whitepaper-level comparison detailing why modern air-cooled OEM units are overtaking water-cooled setups in mid-to-large industrial facilities:
| Evaluation Parameter | Air-Cooled Screw Compressor | Water-Cooled Screw Compressor |
|---|---|---|
| Water Infrastructure | Zero water required. Completely independent. | Requires cooling tower, circulation pumps, water piping & filtration. |
| Installation Complexity | Plug-and-play. Compact footprint, low civil setup cost. | High complexity. Extensive pipefitting and water quality treatment. |
| Maintenance & Scaling | Simple radiator surface blow-downs & air filter swaps. | Frequent descaling, tube bundle cleaning, chemical water treatment. |
| Operating Temperature Envelope | Engineered for ambient range: -20°C up to +50°C. | Dependent on cooling water inlet temperature (<32°C ideal). |
| Heat Recovery Potential | Direct ducting of hot exhaust air for facility space heating. | Water-to-water heat exchangers required for hot process water. |
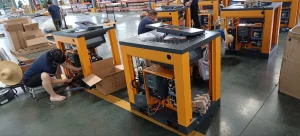
China OEM Manufacturing Efficiency & Production Capabilities
Inside the world's most advanced compressed-air manufacturing ecosystems: precision rotor grinding, automated testing, and supply chain synergy.
5-Axis Precision Rotor Machining
Utilizing SAPA and SKK asymmetric rotor profile technology manufactured on German dynamic CNC rotor grinders, ensuring inter-lobe blow-by clearance is held under 3 microns.
Strict ISO Quality Assurance
Every airend undergoes 100% full-load dynamic balance testing, thermographic hot-spot detection, and acoustic decibel verification before chassis mounting.
Vertical Supply Chain Density
Integrated manufacturing cluster covering foundry casting, oil-gas separator vessel fabrication, inverter coding, and automated export crating under one roof.
China's modern OEM air compressor factories have transformed from simple assembly lines into sophisticated, digitized Smart Manufacturing centers. By combining local industrial scale with European engineering protocols (such as British design legacies and German CNC machining precision), leading Chinese manufacturers export high-spec rotary screw units at cost structures that represent a 30% to 45% capital saving compared to Western European brand names without sacrificing operational reliability.
Key OEM custom capabilities available for global machinery buyers include:
- Multi-Voltage & Multi-Frequency Coils: Dual 220V/380V/400V/415V/440V/460V power configurations at both 50Hz and 60Hz to match global electrical grids seamlessly.
- Enclosure & Ingress Protection Customization: IP54, IP55, and IP65 dust/waterproof ratings, anti-corrosion marine-grade painting for coastal or offshore desert deployments.
- Multilingual Smart PLC Interfaces: 7-inch color touchscreen controllers integrated with English, Spanish, Russian, French, and Arabic microcode, supporting Modbus RTU/RS485 and IoT cloud telemetry.
Localized Application Scenarios & Engineering Case Studies
Tailored air solutions engineered for challenging industrial environments across the globe.
Chemical & Petrochemical Facilities
Challenge: Hazardous gas zones (Zone 1/2), high ambient dust, risk of thermal runaway.
Solution: OEM 4-in-1 Explosion-Proof Air Compressor featuring Ex d IIB T4 / Ex d IIC ratings, intrinsically safe PLC spark-proof enclosures, and heavy-duty flameproof motors.
Pharmaceutical & Beverage Bottling
Challenge: Contamination sensitivity where oil carryover compromises human safety and ruins end products.
Solution: ODM Dry-Type Oil-Free & Water-Lubricated Screw Compressors delivering certified ISO 8573-1 Class 0 oil-free air with stainless steel rotors and ceramic-coated housings.
Semiconductor & Electronics Fabrication
Challenge: Micro-fluctuations in air pressure disrupt high-precision automated pick-and-place robotics.
Solution: Permanent Magnet VFD Screw Compressors providing real-time pressure tracking within ±0.01 MPa tolerances, preventing costly line halts and scrap.
Industry Trends & Technological Innovations
The core technological shifts defining the next generation of industrial air compressors.
1. Permanent Magnet Motors (IE5 Efficiency)
Conventional induction motors suffer from electrical rotor losses and power factor drop-off during partial load. Next-gen OEM compressors utilize rare-earth Permanent Magnet Synchronous Motors (PMSM) achieving IE5 Ultra-Premium efficiency. The motor is directly coupled or oil-cooled on the same rotor shaft, eliminating v-belt and gear transmission energy losses completely.
2. Two-Stage Compression Architecture
By dividing total compression ratio across two sequential sets of rotors with an inter-stage cooling oil curtain, the internal pressure ratio of each stage is drastically reduced. This cuts internal air back-leakage, lowers bearing stress, and decreases power consumption by 15% to 25% compared to single-stage units operating at identical discharge pressures (0.7 to 1.3 MPa).
3. AI-Driven IoT Remote Diagnostics
Modern air-cooled units are now mobile-connected data nodes. Integrated microprocessors continuously monitor dew point, oil temperature, vibration spectral signatures, differential pressure across filters, and real-time kW consumption. Predictive algorithms automatically alert plant managers prior to bearing wear or filter saturation, eliminating catastrophic unscheduled downtime.
Global Enterprise Procurement Framework & Vendor Evaluation
A standardized technical audit roadmap for international machinery importers, EPC contractors, and factory procurement managers.
When auditing an OEM/ODM Air Cooled Screw Compressor factory in China, international buyers must establish a rigorous verification protocol beyond basic price negotiation. The following framework guarantees long-term product reliability and smooth import compliance:
Key Verification Vectors for OEM Sourcing Directors
- Airend Origin & Profile Design: Confirm whether the air end utilizes a 5:6 or 4:6 asymmetric profile. Check rotor dynamic balance reports and rotor surface hardness treatment.
- Motor Insulation & Duty Rating: Demand Class F or Class H insulation ratings with IP55 protection. Verify if permanent magnet motors use high-coercivity NdFeB magnets resistant to demagnetization up to 180°C.
- Electrical Compliance & Safety Marks: Ensure full CE compliance (MD & LVD directives), UL/CSA conformity options for North America, and ASME / CE-PED vessel stamping for air-oil separator tanks.
- Thermal Design Margin: Verify heat exchanger sizing. High-quality air-cooled factories design coolers with a 20% to 30% surface area safety margin to guarantee continuous operation at 45°C ambient temperatures without thermal tripping.
Frequently Asked Questions (Technical & Procurement Q&A)
In-depth technical answers addressing sizing, energy calculations, maintenance cycles, and OEM customization.
In typical industrial plants where compressed air demand fluctuates throughout the shift, a Permanent Magnet VFD compressor saves between 25% and 45% of total electricity. Fixed-speed compressors rely on load/unload control modes where the motor continues running at full RPM even when air demand drops, consuming roughly 30% power during idle. A PM VFD unit continuously adjusts motor RPM down to zero in direct proportion to real-time CFM consumption, eliminating unneeded idle power bleed completely.
Our industrial air-cooled screw air compressors are engineered with oversized heavy-duty aluminum block radiators and high-static axial cooling fans capable of continuous 24/7 duty in ambient environments up to +45°C (+113°F) to +50°C. Thermal shutdown protection triggers safely above +105°C oil discharge temperature, preventing machine damage.
Two-stage compression divides the overall pressure rise between two sets of rotors with inter-stage oil cooling. This lowers the pressure ratio across each individual rotor set, minimizing internal air slippage (backflow leakage) and reducing thermal stress. Two-stage machines deliver up to 15% to 20% higher Free Air Delivery (FAD) per kilowatt than single-stage compressors operating at 0.8–1.3 MPa pressures.
ISO 8573-1 Class 0 is the most stringent international air purity standard, certifying absolute zero oil contamination in the air stream. Oil-free screw compressors (dry-type or water-lubricated) are strictly mandatory in applications where oil contact ruins the final product or creates health hazards—specifically in pharmaceutical cleanrooms, food & beverage packaging, semiconductor chip processing, and precision automotive spray painting.
To accurately size your air system, engineering teams need: 1) Required Free Air Delivery (m³/min or CFM), 2) Minimum System Operating Pressure (bar or MPa), 3) Electrical Supply Voltage/Frequency, 4) Ambient Working Environment & Altitude, and 5) Air Purity Requirement (Class 0 Oil-Free vs. Standard Oil-Injected with downstream filters).
Standard OEM manufacturing lead time ranges from 15 to 25 days depending on motor voltage specs. Available OEM/ODM customizations include private-label branding, customized canopy color schemes, smart PLC language localization, integrated skid packaging (compressor + receiver tank + refrigerated dryer + 4-stage inline filters), and specialized IP55/explosion-proof electrical enclosures.
Advanced Industrial OEM/ODM Air Compressor & Vacuum Solutions
Explore our complete heavy-duty catalog including two-stage compression series, dry screw vacuum pumps, oil-free blowers, and PM VSD rotary units.