
High-Efficiency Rotary Screw Systems: Industrial Product Catalog
Explore our core rotary compressor and vacuum series developed in our British-invested 50,000 m² Shanghai facility, delivering verified specific energy efficiency and thermodynamic reliability.


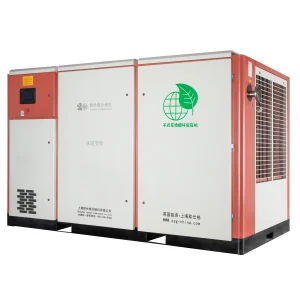


Macro Dynamics in Rotary Screw Compressor Engineering
Industrial compressed air systems consume approximately 10% of total electrical energy worldwide. As global carbon-neutrality mandates accelerate, modern OEM and ODM manufacturers are pivoting toward advanced rotor kinematics, thermodynamics, and intelligent edge control.
Asymmetrical 5:6 Rotor Kinematics
Traditional symmetrical profiles suffer from blow-hole leakage and elevated shear losses. Modern twin-screw compressor hosts leverage third-generation 5:6 tooth profiles, minimizing internal leakage line lengths and maximizing Free Air Delivery (FAD) per unit of shaft power.
IE4 / IE5 Permanent Magnet VFD
Fixed-speed machines incur substantial non-productive energy costs during idle states. Integrated PM Synchronous Motors (PMSM) maintain >96% efficiency across an ultra-wide turndown ratio (25% to 100%), precisely tracking real-time plant air demand without unload spikes.
Thermodynamic Two-Stage Compression
By dividing the overall pressure ratio into two intermediate stages with inter-stage atomized oil-mist cooling, the thermodynamic process closely approximates isothermal compression, driving down specific energy consumption (kW/m³/min) by 8% to 15% versus single-stage units.
Total Cost of Ownership (TCO) & Global Supply Procurement
In high-capacity manufacturing facilities, the initial equipment acquisition price accounts for less than 12% of the cumulative 5-year operating expenditure. Smart enterprise procurement focuses rigorously on isentropic efficiency, MTBF (Mean Time Between Failures), and lifecycle parts availability.
The 5-Year Compressor Lifecycle Cost Breakdown
Empirical audit data across European and North American manufacturing lines reveals that electricity consumption dominates system expenditure. Investing in high-efficiency rotary compressor hardware amortizes initial capital expenditure (CAPEX) within 9 to 14 operational months.
Core Procurement Decision Matrix
Global engineering procurement teams and EPC contractors systematically evaluate four fundamental engineering parameters when selecting rotary screw OEMs for export projects:
- Specific Power Rating (kW/m³/min): Strict compliance with GB19153-2019 Class 1 Energy Efficiency and ISO 1217 Annex C/E standards.
- Thermal Dissipation & Motor Protection: IP23/IP55 enclosures paired with oil-cooled PMSM drives capable of uninterrupted 46°C ambient operation.
- Electrical Grid Adaptation: Inverter hardware engineered for 380V, 400V, 415V, 440V, and 460V wide-frequency tolerances (50Hz / 60Hz).
- Harmonic Suppression: Integrated DC chokes and line reactors to maintain plant THD-i under 5%, preventing interference with factory PLCs.
| Compressor Technology Class | Thermodynamic Lubrication | ISO 8573-1 Air Purity | Optimal Specific Power | Target Industrial Application |
|---|---|---|---|---|
| PM VFD Single-Stage Rotary | Synthetic Fluid Lubricated | Class 2-3 (Particulates/Oil) | 6.2 – 6.8 kW/m³/min | CNC Machining, Automated Assembly, Metal Stamping |
| Two-Stage High-Pressure Screw | Synthetic Fluid Lubricated | Class 2-3 (Particulates/Oil) | 5.4 – 6.0 kW/m³/min | Laser Cutting (16-25 bar), Chemical Continuous Base Load |
| Dry-Type Oil-Free Twin Screw | Dry (Special PTFE/Polymer Coating) | Class 0 (100% Hydrocarbon Free) | 7.2 – 7.8 kW/m³/min | Pharmaceutical Synthesis, Microelectronics, Food Processing |
| Water-Lubricated Oil-Free Screw | Purified Deionized Water | Class 0 (Absolute Zero Oil Risk) | 6.1 – 6.6 kW/m³/min | Aseptic Beverage Bottling, Medical Gases, Semiconductor Cleanrooms |
Macro Industry Solutions Engineered for Severe Industrial Duty
From hazardous mining atmospheres to ISO Class 5 cleanrooms, our OEM rotary screw systems are tailor-packaged to mitigate process downtime, fluid carryover, and thermal tripping.
Laser Cutting & Sheet Metal
Delivers continuous 16 bar to 25 bar stabilized pressure with multi-stage oil coalescers, achieving pressure dew points below -40°C to prevent laser optics fouling and nozzle burring.
Chemical & Petrochemical
Explosion-proof Ex d IIB / IIC integrated packages featuring hermetic control enclosures, intrinsically safe sensors, anti-spark copper fans, and robust 24/7 continuous rated duty cycles.
Food & Pharmaceutical
Zero tolerance for lubricant migration. Class 0 water-lubricated and dry twin-screw architectures prevent batch adulteration, supporting strict FDA, GMP, and ISO 22000 audits.
Wastewater & Pneumatic Conveying
Low-pressure rotary screw blowers (0.3 to 1.5 bar) replacing obsolete Roots lobe blowers, slashing aeration basin power demands by up to 35% through positive displacement adiabatic gain.
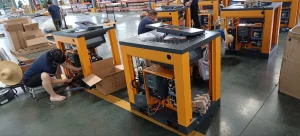
Inside Our Five-Stage Precision Manufacturing Architecture
Operating under ISO 9001:2015, ISO 14001:2015, and European Machinery Directives, every rotary screw host undergoing OEM fabrication is subjected to comprehensive coordinate measuring and full-load validation.
Precision Metallurgical Casting
HT250 / QT450 nodular cast iron housings undergo artificial thermal aging to eliminate internal stress, ensuring zero casing deflection under intense pressure.
Ultra-Precision Rotor Milling
German Klingelnberg & Holroyd five-axis rotor hobbing machinery maintains rotor profiles within ±0.005mm tolerances for micron-grade clearance sealing.
Dynamic Balancing & Bearings
High-speed rotors undergo ISO 1940 G2.5 precision balancing before installation into Swedish SKF Explorer or German FAG paired angular contact bearings.
Full-Load Run-In Testing
Every unit undergoes continuous 4 to 8 hours full-load factory testing under varied pressures to benchmark temperature curves, noise dB(A), and FAD volume.
Export Crating & Anti-Corrosion
Internal moisture purge, vapor-corrosion inhibiting wrapping, and ISPM 15 fumigated seaworthy wooden crating engineered for rough container journeys.
Technological Roadmap & Localized OEM Compliance
Sustainable industrial manufacturing demands proactive compliance alignment with European CE, North American ASME/UL, and evolving cyber-physical automation architectures.
Edge IoT & Predictive Maintenance
Integrated 4G/5G smart telematics modules continuously stream FFT vibration spectra, bearing temperatures, and pressure differentials directly to cloud dashboards, predicting component fatigue before failure occurs.
Waste Heat Recovery Systems
Over 80% of compressor electrical input is converted into thermal waste. Our direct liquid-liquid heat exchanger packages recover heated oil up to 75°C for boiler feed preheating or plant space heating.
Global Compliance Engineering
OEM customization spans custom cabinet powder coatings, dual-language Siemens or Schneider PLC touchscreens, multi-tap transformers, and full pressure vessel verification under PED 2014/68/EU.
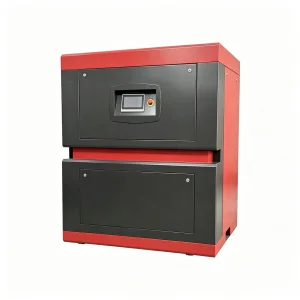
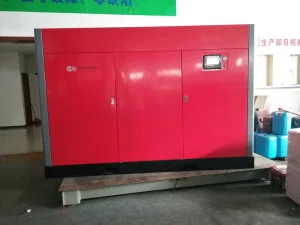
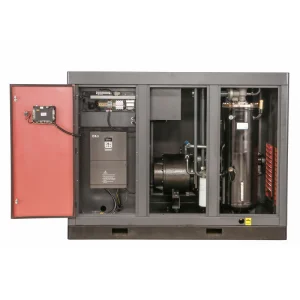
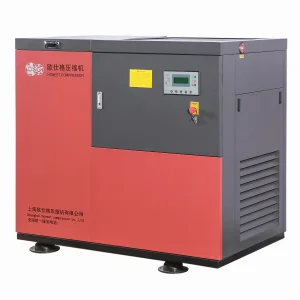
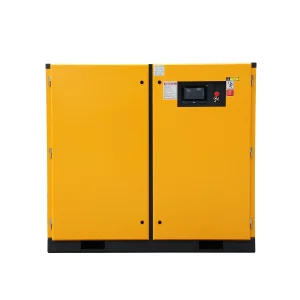
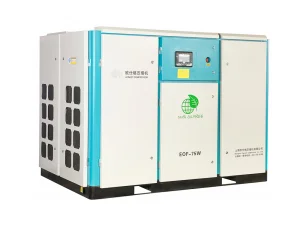
High-Capacity Industrial Compressors: Export Product Matrix
Review additional field-proven configurations tailored for laser profiling, heavy mining duty, energy-sensitive plant upgrades, and Class 0 sterile environments.




Engineering Questions: Rotary Screw Selection & OEM Sourcing
Authoritative answers compiled by our chief thermodynamic engineers to support plant engineers, procurement directors, and distributor networks.
How does PM VFD achieve 20% to 40% energy reduction over fixed-speed compressors?
Fixed-speed compressors operate via load/unload electro-pneumatic valves. When target pressure is reached, the motor continues spinning unloaded at roughly 40% full-load electrical draw without generating useful air. Honest Compressor PM VFD technology utilizes field-oriented magnetic vector control to continuously scale rotor RPM directly proportional to plant air consumption, maintaining a tight ±0.1 bar tolerance while eliminating unloaded kilowatt wastage entirely.
What is the fundamental engineering difference between Dry Oil-Free and Water-Lubricated screws?
Dry-type oil-free twin screw machines operate without any liquid in the compression chamber; rotors rely on micro-clearance timing gears and specialized poly-fluorocarbon coatings, requiring two stages with inter-coolers to manage heat. Water-lubricated units inject sterile, purified deionized water directly into the single-stage compression chamber, acting as a lubricant, dynamic sealant, and near-isothermal cooling medium. Both deliver certified ISO 8573-1 Class 0 air purity.
Why is Two-Stage Rotary Compression superior for high-pressure fiber laser cutting?
Achieving 16 bar to 20 bar in a single screw compression stage results in excessive internal leakage back to the suction port and extreme discharge temperatures that degrade lubricant longevity. Two-stage compression lowers the pressure ratio across each individual stage (e.g., stage 1 brings ambient air to 4.5 bar, stage 2 boosts from 4.5 to 20 bar). This reduces the pressure differential across rotor sealing lines, drastically cutting internal leakage and lowering specific power consumption by 15%.
What parameters must global procurement specify for an exact OEM turnkey quotation?
To accurately size an industrial rotary air system, our engineering division requires: (1) Free Air Delivery demand in m³/min or CFM; (2) Minimum working pressure at point-of-use (bar / psi); (3) Destination electrical parameters (Voltage, Phase, Frequency: 380V/50Hz, 460V/60Hz, etc.); (4) ISO 8573-1 purity requirements for oil and moisture; and (5) Environmental factors such as site altitude, ambient temperature extremes, or explosive zone classifications (ATEX/Ex).
What OEM/ODM customization capabilities are supported by Honest Compressor?
We provide full white-label and customized mechanical manufacturing: bespoke canopy sheet metal design, custom corporate color RAL powders, private labeled touch-panel HMI firmware with English/Spanish/Russian/Arabic languages, integrated skid packaging (compressor, vertical air receiver, refrigeration/desiccant dryer, line filters), and dedicated certifications (CE, ASME, EAC, CSA).
How does Honest Compressor support international parts supply and maintenance SLAs?
We maintain an extensive inventory of standardized consumable service kits (synthetic compressor fluids, 2000h/4000h/8000h filter and separator packs, solenoid rebuild kits, minimum pressure check valves). Stocked items are dispatched via express global air couriers within 24 to 48 hours to minimize unplanned plant downtime.
Initiate Your OEM/ODM Rotary Compressor Engineering Inquiry
Collaborate directly with Shanghai Honest Compressor Co., Ltd. (British-invested, founded 2004). Our Jiading plant engineering team is ready to analyze your pneumatic schematics, load profiles, and custom voltage requirements for complete system optimization.
