High-Efficiency Laser Cutting Compressors & Booster Units
Explore our premium factory-direct rotary screw air compressors, vacuum pumps, and oil-free blower systems engineered for reliable 24/7 continuous industrial duty cycles.
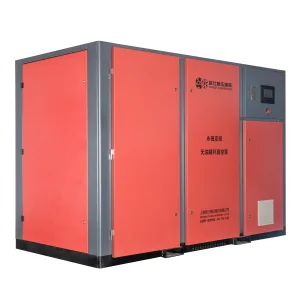
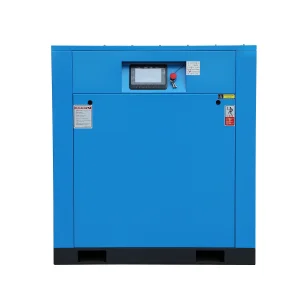

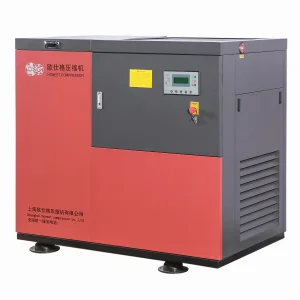



The Assist Gas Paradigm Shift: High-Pressure CDA vs. Liquid Nitrogen
How the rapid rise of 12kW–60kW ultra-high-power fiber laser cutting machines is revolutionizing industrial gas economics and shop-floor productivity.
In modern metal manufacturing, the cutting assist gas represents up to 45% to 60% of total machine operating hourly costs. Historically, fabricators relied on bulk Liquid Nitrogen (LN2) to attain oxide-free edge quality on stainless steel and aluminum, or Oxygen (O2) for exothermic cutting of thick mild carbon steel. However, with fiber laser power scaling exponentially from the standard 4kW/6kW thresholds toward 12kW, 20kW, 30kW, and up to 60kW, cutting mechanics have fundamentally transitioned from thermal melting reliant on exothermic reactions to high-speed kinetic expulsion.
High-pressure Compressed Dry Air (CDA), compressed to 16 bar, 20 bar, or 30 bar, has emerged as the premier operational solution. Because atmospheric air contains approximately 78% Nitrogen and 21% Oxygen, the focused kinetic energy of a high-pressure compressed air jet effectively clears the molten kerf at supersonic speeds, yielding clean, burr-free edges while cutting processing costs by up to 75% to 85% compared to bulk liquid nitrogen dewars.
Gas Economics & ROI Velocity
A continuous 20kW laser cutting 6mm stainless steel consumes roughly 45–60 m³/h of liquid nitrogen, generating monthly gas bills surpassing $6,000–$10,000. An integrated 20–30 bar rotary screw air compressor setup amortizes the entire capital equipment expenditure within 4 to 8 months.
Laser Optics Lens Preservation
Standard compressed shop air contains suspended liquid water, oil aerosols, and sub-micron particulates. If an uncertified compressor feeds the laser head, microscopic oil vapor coats the quartz protective window, absorbing laser energy and causing thermal fracture within operating hours.
Dynamic Kinetic Kerf Evacuation
At 20–30 bar pressures, assist air velocity at the nozzle tip reaches supersonic Mach 1.2–1.5. This immense kinetic shearing force violently sweeps viscous molten slag and oxides from the kerf, permitting cutting speeds 1.2x to 2x faster than pure nitrogen on thin to medium plate gauges.
High-Power Fiber Laser Assist Gas Operational Matrix
Empirical performance, hourly consumable analysis, and cut-edge quality comparison across varying structural metal gauges and assist gas media.
| Material Type & Thickness | Laser Power (kW) | Assist Gas Media | Required Pressure (Bar) | Cutting Velocity (m/min) | Hourly Gas / Energy Cost | Edge Quality / Dross Status |
|---|---|---|---|---|---|---|
| Mild Steel (Carbon) 3mm | 12 kW | Oxygen (O2) | 0.8 – 1.2 Bar | 3.8 – 4.5 m/min | $2.80 / hr | Dark Oxide Layer, Slag Free |
| Mild Steel (Carbon) 3mm | 12 kW | High-Pressure CDA | 16 – 20 Bar | 12.0 – 15.0 m/min | $0.85 / hr (Air Power) | Micro-Oxide, 3.2x Faster |
| Stainless Steel 304 6mm | 20 kW | Liquid Nitrogen (LN2) | 20 – 25 Bar | 7.5 – 9.0 m/min | $14.50 – $18.00 / hr | Silver White, Zero Dross |
| Stainless Steel 304 6mm | 20 kW | High-Pressure CDA | 25 – 30 Bar | 8.0 – 9.8 m/min | $1.40 / hr (Air Power) | Slightly Golden, Zero Dross |
| Aluminum Alloy 5052 10mm | 30 kW | Liquid Nitrogen (LN2) | 25 – 30 Bar | 4.0 – 5.2 m/min | $22.00 – $28.00 / hr | Bright Edge, Excellent Weldability |
| Aluminum Alloy 5052 10mm | 30 kW | High-Pressure CDA | 30 – 35 Bar | 4.5 – 5.8 m/min | $1.95 / hr (Air Power) | Clean Edge, Ready for Powder Coat |
Tailored Turnkey Compressed Air Integration for Heavy Fabrication
Custom-engineered compressed air packages meeting the rigorous 24/7 uptime specifications of global machine tool manufacturers and tier-one EPC contractors.
Automotive Stamping & BIW Profiling
Automotive body-in-white (BIW) lines utilizing 3D 5-axis robotic laser heads demand non-pulsating gas feeds. Dynamic pressure surges lead to kerf deviations and micro-cracking in high-strength boron steels. Our 4-in-1 integrated high-pressure systems incorporate 1,000L ASME/CE air receivers and dual desiccant dryers that hold pressure jitter within ±0.1 Bar.
Aerospace Superalloys & Titanium
Turbine exhaust ducts and heat shields fabricated from Inconel and titanium alloys require Class 0 oil-free air to prevent carbon embrittlement during laser cutting. Our water-lubricated and dry-type oil-free twin-screw platforms deliver ISO 8573-1 Class 0 certified air streams with total oil content <0.003 mg/m³.
Heavy Construction & Structural Steel
Profile cutting of thick 16mm–25mm baseplates and heavy architectural tubing demands steady 30 bar kinetic blow-off. Our dual-stage screw air compressors feature inter-stage water/air cooling to sustain peak continuous CFM flows under scorching 45°C ambient shop temperatures without thermal derating.
Precision Electronics & Enclosures
Fabrication of delicate server racks, aluminum battery enclosures, and telecommunication chassis requires burr-free edges directly powder-coatable without mechanical deburring. Our ultra-dry assist air packages ensure zero surface moisture to eliminate post-weld porosity and coating blister defects.
Agricultural & Yellow Goods OEM
High-volume cutting of 4mm–12mm hot-rolled pickling plates for tractor chassis, excavators, and agricultural implements. Switching from oxygen to 20 bar compressed air boosts piercing and cutting cycles by 220%, slashing overall cycle times and boosting daily tonnage through laser cutting cells.
Factory Certification, Quality Gates & Technical Roadmap
Built under British-founded manufacturing heritage in Shanghai since 2004, meeting stringent international pressure vessel directives, CE safety codes, and IoT telemetry architectures.
ASME & CE-PED Certified
Every air receiver tank and separator vessel complies with ASME Boiler & Pressure Vessel Code (Section VIII, Div 1) and European Pressure Equipment Directive 2014/68/EU (PED), backed by third-party hydrostatic burst test reports.
5-Stage Filtration System
Equipped with particulate pre-filters, high-efficiency oil coalescing filters, and deep-bed activated carbon vapor absorbers. Yields residual oil aerosol content under 0.003 mg/m³ and solid particles below 0.01 micron.
IoT Remote Telemetry
Standard Modbus RTU / Ethernet interfaces enable real-time bidirectional communication with laser CNC controllers (Beckhoff, CypCut, FANUC, Siemens). Automatically modulates compressor delivery based on active cutting cycles.
IE4 / IE5 PM Motors
Utilizing high-coercivity NdFeB permanent magnet synchronous motors delivering IE4/IE5 ultra-premium efficiency across 20% to 100% speed bands, eliminating unloading energy waste during laser sheet changeovers.
Technical Roadmap: Next-Generation Laser Assist Gas Innovations (2025–2030)
As laser powers scale toward 60kW–100kW, assist air engineering faces new physical boundaries. Our factory research and development facility in Shanghai is pursuing three pioneering technological avenues:
1. Synchronized Pulsed Boosters
Developing microsecond-response booster valves synchronized with CNC piercing routines, delivering instantaneous 40 bar pulse bursts for ultra-fast piercing without steady-state power waste.
2. Cryogenic Sub-Cooling Dryers
Integrated dual-refrigeration sub-cooling circuits reaching -70°C dew point under 35 bar continuous pressure without the purge air consumption penalties typical of heatless desiccant towers.
3. Maglev Oil-Free Turbos
High-pressure magnetic levitation centrifugal compression stages eliminating mechanical oil sumps entirely, targeting 100,000 running hours without maintenance interventions for mega-scale fabrication plants.
Laser Cutting Air Compressor Engineering FAQ
In-depth engineering answers to common procurement, sizing, and gas filtration questions asked by plant managers and mechanical engineers.
High-Power Two-Stage, Explosion-Proof & Oil-Free Industrial Systems
Explore our heavy-duty two-stage energy-saving air compressors, modular explosion-proof packages, and clean vacuum pump solutions built for global export.