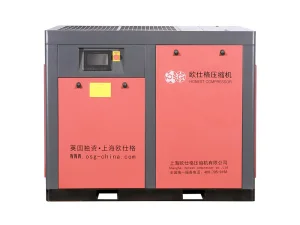
Featured Industrial Rotary Compressors & Vacuums
Explore our precision-machined rotary screw, oil-free, and high-efficiency permanent magnet variable frequency compressor models.
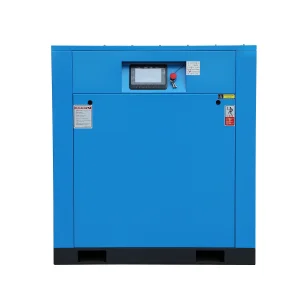
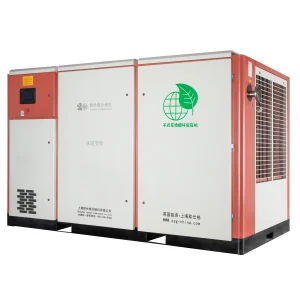


Engineering Optimization & Energy Dynamics of 7.5 kW Systems
A thorough evaluation of thermodynamic principles, rotor mesh aerodynamics, and why modern industrial manufacturing facilities are replacing legacy reciprocating piston machines with direct-drive rotary screw systems.
5:6 Asymmetric Rotor Kinematics
The heart of the 7.5 kW (10 HP) airend utilizes an advanced 5-lobe male rotor and 6-flute female rotor configuration. This geometric profile increases delivery volume by 12% over traditional 4:6 profiles while reducing blow-hole slippage and inter-lobe leakage. Rotors are finished on CNC grinding centers with micron-level tolerances, delivering an optimal adiabatic compression efficiency of up to 88%.
Intelligent PM VFD Frequency Modulation
Unlike fixed-speed compressors that consume 40% of rated electrical draw during off-load idle cycles, our 7.5 kW Permanent Magnet Variable Frequency Drive (PM VFD) dynamically throttles motor speed between 25% and 100%. Utilizing high-flux NdFeB magnets that maintain magnetic saturation at up to 180°C, the system holds discharge pressure steady within ±0.01 MPa, preventing unnecessary over-pressurization.
Direct-Coupled Coaxial Architecture
Belt slips and gear drive transmissions represent up to 4% mechanical drivetrain losses. Our 7.5 kW units feature a direct-coupled 1:1 drive mechanism where the PM motor rotor is integrated directly onto the compressor male rotor shaft. This eliminates bearings, couplings, and belt-tension maintenance, lowering vibration levels to under 1.5 mm/s and ensuring zero mechanical drivetrain degradation.
China Supply Chain Resilience & Cost-Engineering Architecture
How Shanghai's advanced manufacturing cluster combines vertical component integration, automated rotor milling, and rare-earth materials to deliver unparalleled cost-to-performance equity.
End-to-End Vertical Manufacturing in Shanghai
Operating across a 50,000 m² state-of-the-art manufacturing plant in Jiading District, Shanghai, Honest Compressor integrates high-precision ductile iron casting, multi-axis machining on German Klingelnberg and DMG MORI tooling centers, robotic shell welding, and localized automated assembly lines. Vertical manufacturing guarantees full quality transparency, eliminating subcontractor margin markups and lowering CapEx by 30% to 45% compared to European counterparts.
Rare-Earth NdFeB Motor Supply Security
China accounts for over 70% of global rare-earth mining and magnet refining. Our proximity to the domestic supply chain allows us to equip every 7.5 kW PM VFD compressor with grade 38UH/40UH Neodymium-Iron-Boron permanent magnets. These high-coercivity magnets offer zero demagnetization risk at elevated operating temperatures, providing superior flux density, exceptional low-speed torque control, and true IE4/IE5 operational efficiencies without global supply disruptions.
Standardized Global Spares Interoperability
To prevent vendor lock-in, our engineering team standardizes critical consumables and subcomponents. Spin-on oil filters, air intake cartridges, and thermostatic valve elements conform to worldwide metric threads and international envelope standards. Electronic controls utilize genuine Schneider and ABB contactors paired with standard Modbus RTU PLC platforms, ensuring plant maintenance crews can easily source replacement wear parts locally anywhere on earth.
Localized Compliance & Global Engineering Governance
Ensuring unhindered customs clearance, electrical grid compatibility, and pressure vessel certification across 50+ export jurisdictions.
CE & European Directives
Fully compliant with the European Machinery Directive 2006/42/EC, Low Voltage Directive (LVD) 2014/35/EU, and Electromagnetic Compatibility (EMC) 2014/30/EU. Ready for direct CE Declaration of Conformity audits.
ASME & PED Pressure Vessels
Air-oil separation tanks and optional receiver tanks are certified to ASME Boiler and Pressure Vessel Code Section VIII Div 1 (for North America) or the Simple Pressure Vessels Directive (SPVD 2014/29/EU) for Europe.
Universal Electrical Topology
Factory-configurable dual-frequency and custom multi-voltage drives: 220V/1Ph/50-60Hz, 380V/3Ph/50Hz, 400V/415V/3Ph/50Hz, and 460V/480V/3Ph/60Hz to seamlessly integrate with local industrial electrical feeds.
ISO 1217 Testing Rigor
Every 7.5 kW unit undergoes full-load flow testing on an ISO 1217:2009 Annex C (fixed speed) and Annex E (variable speed) automated test stand. Individual factory test reports documenting actual FAD and power draw accompany each machine.
7.5 kW (10 HP) Technical Specifications & Operating Parameters
Performance ratings measured in strict adherence to ISO 1217 Annex C/E standards at 20°C ambient, 1 bar(a) suction pressure, and 60% relative humidity.
| Model / Parameter | Working Pressure | Free Air Delivery (FAD) | Motor Drive Type | Cooling Mode | Noise Level | Air Outlet | Dimensions (L×W×H) | Dry Weight |
|---|---|---|---|---|---|---|---|---|
| OSG-10A (Standard) | 0.8 MPa (8.0 bar) | 1.15 m³/min (40.6 CFM) | IE3 Induction / Belt | Air-Cooled (Forced) | 68 ± 2 dB(A) | G 3/4" Female | 850 × 650 × 880 mm | 215 kg |
| OSG-10PM (VFD) | 0.7 - 1.0 MPa (7 - 10 bar) | 0.32 - 1.18 m³/min (11 - 42 CFM) | IE4 PM VFD Direct | Air-Cooled (Axial) | 64 ± 2 dB(A) | G 3/4" Female | 800 × 600 × 850 mm | 195 kg |
| OSG-10PM-HP (High Pres) | 1.25 MPa (12.5 bar) | 0.92 m³/min (32.5 CFM) | IE4 PM VFD Direct | Air-Cooled (Heavy Duty) | 66 ± 2 dB(A) | G 3/4" Female | 800 × 600 × 850 mm | 205 kg |
| OSG-10PM-4in1 Tank Mount | 0.8 - 1.0 MPa (8 - 10 bar) | 0.32 - 1.18 m³/min (11 - 42 CFM) | IE4 PM VFD + Tank/Dryer | Refrigerated Air Cooled | 65 ± 2 dB(A) | G 3/4" Female | 1500 × 750 × 1450 mm | 380 kg |
| EOWV-7.5 (Oil-Free Water) | 0.7 - 0.8 MPa (7 - 8 bar) | 1.05 m³/min (37.1 CFM) | Class 0 Water Lubricated | Internal Water Sealed | 62 ± 2 dB(A) | G 3/4" Stainless | 900 × 700 × 950 mm | 240 kg |
Localized Application Engineering & Duty Scenarios
Evaluating operational load profiles, air quality demands, and pneumatic uptime requirements across critical industrial use cases.
Precision CNC Machine Centers & Tool Purge
In automated vertical machining centers and turning lathes, pneumatic pressure actuates automatic tool changers (ATC), spindle air seals, and chuck clamps. Pressure fluctuations below 0.55 MPa cause spindle fault lockouts, stalling operations. The 7.5 kW PM VFD maintains a rigid 0.7 MPa header with immediate ramp-up response, while the sub-3 ppm oil filter ensures spindle labyrinth seals remain free of hydrocarbon varnishing.
Fiber Laser Cutting Workcells (1.0 to 1.6 MPa)
When processing thin sheet aluminum and mild steel, compressed shop air serves as an economical assist gas replacement for nitrogen. The OSG-10PM-HP high-pressure 7.5 kW variant delivers 0.92 m³/min at 1.25 to 1.6 MPa directly to the laser cutting nozzle. Integrated refrigerated drying produces a -40°C pressure dew point when paired with desiccant modules, preventing lens fogging and edge oxidation.
Surface Coating & Dust Extraction Pulse-Jet
Continuous electrostatic powder coating and wet spray painting require pulse-free airflow. Reciprocating compressors induce pressure ripple that generates orange-peel paint defects. A 7.5 kW rotary screw generates continuous non-pulsating displacement. Its triple filtration removes oil aerosols down to 0.01 micron, preventing fisheyes in Class A automotive refinishing and keeping reverse-pulse dust filters working reliably.
Total Cost of Ownership (TCO) & Lifecycle Economics
Compressed air accounts for roughly 10% of global industrial electricity consumption. Over a 5-year operating window, the initial machine purchase represents less than 15% of the total expenditure.
50,000-Hour Operating Cost Breakdown
Industrial accounting metrics prove that over a 50,000-hour lifecycle:
• Electricity Consumption: 76% of total life-cycle costs.
• Capital Equipment Purchase: 12% of total costs.
• Scheduled Maintenance & Lubrication: 8% of total costs.
• Unplanned Down-time: 4% of total costs.
Investing in an ultra-efficient PM VFD drive pays for its cost delta in power savings within 8 to 14 operating months.
Fixed-Speed vs. PM VFD Economic Model
Consider a typical plant operating 6,000 hours annually with a 65% average air demand profile at $0.14/kWh:
• Fixed-Speed 7.5 kW Unit: Draws roughly 3.0 kW during idle unloading. Annual power bill = $5,820 USD.
• 7.5 kW PM VFD Compressor: Slows down without idling, completely eliminating unloaded electrical waste. Annual power bill = $4,074 USD.
• Net Direct Cash Savings: $1,746 USD per year, yielding $8,730 USD saved over a 5-year operational lifecycle.
Predictive Maintenance vs. Reactive Rebuilds
Unplanned airend failure can shut down an entire manufacturing facility. Honest Compressor systems integrate high-precision NTC temperature probes and vibration telemetry monitoring directly within the micro-PLC. By providing early warnings for lubricant thermal degradation, bearing micro-spalling, or differential pressure drop across separator filters, repair costs shift from expensive emergency airend overhauls to economical standard filter swaps.
Technological Horizons in Screw Compression
Anticipating the technological shifts in decarbonization, telemetry, and small-envelope rotary machine performance over the next decade.
IoT 4.0 Telemetry Standard
Integrated 4G/Wi-Fi telemetry gateways link small 7.5 kW compressors to remote diagnostic dashboards, tracking specific energy consumption (kW/m³/min) and maintenance timers in real time from mobile or desktop terminals.
IE5 Ultra-Premium PM Motors
Adoption of synchronous reluctance permanent magnet (SynRM) motors delivering IE5 efficiency ratings. These units maintain over 96% motor efficiency even down to 25% part-load operation.
Class 0 Water-Lubricated Micro-Screw
Engineering precision ceramics and polymer-composite rotors that use purified water as the sealing lubricant. This makes certified ISO 8573-1 Class 0 air attainable in compact 7.5 kW packages for pharmaceutical and food production.
Low-GWP Refrigerated Dryers
Updating integrated 4-in-1 tank-mounted air compressors with eco-friendly R1234yf or R513A low Global Warming Potential refrigerants to satisfy upcoming European F-Gas regulations and US EPA SNAP requirements.
Global Procurement Checklist: Auditing a Chinese OEM Supplier
Critical technical indicators that international procurement departments, EPC contractors, and distributor networks must verify prior to signing supply contracts.
1. Verification of In-House Machining
Verify that the manufacturer owns and operates high-precision rotor milling and grinding equipment in-house (such as Klingelnberg, Holroyd, or Mitsui Seiki). Merely assembling off-the-shelf third-party generic airends in a warehouse leads to poor profile matching, high vibration, and unrepeatable FAD flow deliveries.
2. Factory Acceptance Testing (FAT) Rigor
Require documented flow nozzle calibration records according to ISO 1217 Annex C/E. High-quality Chinese manufacturers run every completed 7.5 kW unit at 100% full-load continuous pressure for at least 2 to 4 hours to verify steady-state thermal equilibrium, vibration velocity, and electrical amp draw before packing.
3. Electrical Component Provenance
Inspect the control cabinet schematic. Ensure high-voltage switchgear, thermal overload relays, and contactors are sourced from world-class brands like Schneider Electric, Siemens, or ABB, and that the VFD inverter incorporates integrated choke reactors to protect local plant circuitry from harmonic interference.
Frequently Asked Technical & Sizing Questions
Authoritative answers directly from our factory engineering department on sizing, electrical design, installation, and preventative maintenance for 7.5 kW rotary systems.
Two-Stage, Oil-Free & Vacuum System Solutions
Engineered for large chemical plants, food production lines, pharmaceutical cleanrooms, and automated packaging infrastructure.