
High-Efficiency Rotary Screw & Vacuum Equipment Portfolio
Direct from Shanghai Honest Compressor Co., Ltd. (Founded 2004, 50,000 m² state-of-the-art production plant). Precision engineered to eliminate parasitic system line loss, stabilize operating pressure, and reduce continuous specific power consumption.




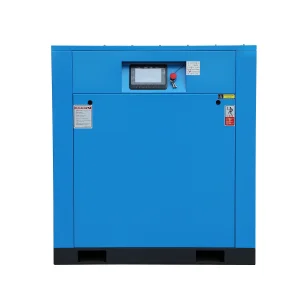
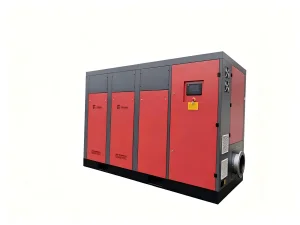
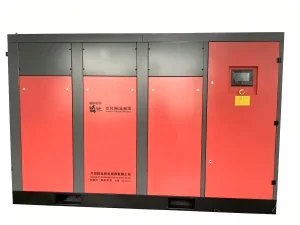
The 5-in-1 Integrated Architecture: Eliminating The Flaws of Legacy Decentralized Systems
In conventional manufacturing facilities, a compressed air system is assembled piecewise: a standalone rotary screw compressor connected via hundreds of feet of carbon steel piping to a loose receiver tank, a distinct refrigerated dryer, external filter bowls, and separate drainage valves. This archaic model introduces thermodynamic friction, pressure decay, multiple leak vectors, and excessive footprint. The ODM 5-in-1 design consolidates the entire thermodynamic cycle on a single precision vibration-damped skid.
1. PM VFD Twin-Screw Airend
The heart of the system incorporates an asymmetrical 5:6 tooth profile rotary screw mechanism driven by an ultra-efficient IE4/IE5 rare-earth NdFeB permanent magnet synchronous motor. The integrated vector inverter modulates motor RPM synchronously with downstream consumption in milliseconds.
- Zero idling energy waste (eliminates 20–40% unloaded draw)
- Soft-start avoids severe grid current peaks (0–100% ramp)
- Precision ground rotor tolerances down to 5 microns
2. High-Efficiency Refrigerated Dryer
Directly coupled via hard-piped non-corrosive stainless or copper manifold conduits, our integrated refrigerated air dryer utilizes an oversized aluminum plate-fin heat exchanger with environmentally compliant R410A/R134a refrigerants, holding consistent dew point control.
- Continuous Pressure Dew Point (PDP) suppression to +2°C ~ +5°C
- Zero moisture carryover prevents pneumatic valve seizing
- Anti-freezing automated hot gas bypass valve protection
3. ASME/CE Certified Pressure Buffer
Integrated horizontally beneath or vertically beside the compression module, the calibrated air storage vessel functions as a physical accumulator, dampening pulsation harmonics, cooling hot compressed air to drop bulk condensation, and stabilizing continuous demand surges.
- Certified to ASME Sec VIII Div 1 & EU PED 2014/68/EU standards
- Internal anti-corrosion epoxy lining for extended shell life
- Safety relief valves factory calibrated with test reports
4. Quad-Tier Coalescence Filtration
Equipped with a progressive 4 to 5-stage filtration bank (Pre-filter, Dust separator, Fine oil-mist coalescer, and Activated carbon stage), the 5-in-1 delivers ultra-clean technical air exceeding ISO 8573-1:2010 purity classes, protecting expensive downstream CNC and optical apparatus.
- Particulate retention down to 0.01 micron
- Residual oil carryover suppressed to ≤0.003 ppm
- Differential pressure indicators for timely cartridge servicing
5. Dual-VFD Central Intelligent PLC
Unlike segmented components that run asynchronous blind cycles, the 5-in-1 features a centralized high-speed PLC interface that monitors both the compressor airend and refrigerated dryer in real time, coordinating cooling fans, motor RPM, and zero-loss condensate evacuation.
- 7-inch color touchscreen supporting English, Spanish, Russian
- RS-485 Modbus-RTU & IoT 4G cloud remote connectivity
- Automated electronic zero-loss condensate drain management
The Net Hydraulic Result
By removing 10–20 meters of interconnected threaded pipe, flanges, and directional elbows, internal parasitic pressure loss drops from a typical 0.8–1.2 bar down to under 0.08 bar. This alone delivers an immediate 6%–8% net energy efficiency gain from day one.
The Global Shift: Decentralized Point-of-Use Compressed Air Stations
Across Europe, the Americas, and the Asia-Pacific region, soaring industrial kilowatt-hour electricity costs, strict carbon emission auditing (Scope 1 and Scope 2 GHG protocol), and the explosive proliferation of fiber laser metal cutting have triggered a historic transition away from monolithic central air houses.
The Demise of the Central Compressor Room
For decades, enterprise factories centralized 200kW–500kW compressors in distant utility outbuildings. Audits conducted by the U.S. Department of Energy (DOE) and Fraunhofer Institute confirm that between 20% to 35% of all compressed air energy generated in central plants is lost purely to piping leaks, header pressure drops, and dead-leg turbulence before reaching workstations. When production lines shut down for maintenance or changeover, the giant central machine still idles inefficiently.
By contrasting this with localized 5-in-1 skid-mounted modules positioned within 3 meters of specific work centers, distribution piping losses drop to absolute zero. Facilities can power down individual assembly lines without affecting the wider plant, eliminating thousands of lost MWh annually.
Electricity Inflation & Scope 2 Decarbonization Mandates
In standard manufacturing lifecycle accounting, electricity consumption accounts for 76% to 82% of a rotary screw compressor's total 10-year operating cost; capital equipment expenditure accounts for a mere 12%, with routine maintenance covering the balance. With electrical utility tariffs reaching historic peaks across Germany, the UK, Japan, and North America, purchasing a fixed-speed compressor is economically non-viable.
Our ODM 5-in-1 permanent magnet variable speed platforms dynamically lower running power during partial load scenarios, maintaining specific energy consumption (SEC) metrics as low as 5.8 to 6.2 kW per m³/min at 8 bar. This directly aligns with ISO 50001 energy auditing protocols and satisfies Corporate Sustainability Reporting Directive (CSRD) baselines.
Localized Engineering Deployments: Where 5-in-1 Systems Deliver Peak ROI
From modern high-density industrial parks to remote automated field sites, the 5-in-1 architecture solves distinct operational challenges across precision sectors.
High-Power Fiber Laser Cutting (16–25 Bar Assist Gas)
High-wattage fiber lasers (6kW to 30kW+) cutting stainless steel, carbon steel, and aluminum require continuous assist gas to evacuate molten slag. Historically, liquid nitrogen (LN2) bottles were required, incurring recurring logistics and evaporation losses. Our specialized 16 bar and 20 bar 5-in-1 units replace bulk nitrogen with dry, high-pressure filtered air, cutting assist gas overhead by up to 75%–85%.
- Pressure Dew Point ≤ +3°C prevents laser lens fogging
- 0.003 ppm residual oil eliminates optic surface pitting
Automotive Fabrication & Precision Robotic Stamping
Automated transfer tooling, pneumatic grippers, robotic spot-welders, and automotive paint booths cannot tolerate micro-pulsations or liquid condensate, which ruin pneumatic cylinders and cause costly assembly line stoppages. The 5-in-1 delivers rock-steady line pressure (±0.01 MPa precision) directly adjacent to the robotic cell without requiring civil foundation work.
- Low acoustic profile (<68 dBA) allows workshop placement
- Protects million-dollar pneumatic robotic valves
Semiconductor Cleanrooms & Medical Electronics
Surface-mount technology (SMT) pick-and-place nozzles, wafer dicing apparatus, and micro-electromechanical fabrication demand strict adherence to ISO 8573-1 Class 1:2:1 air purity. Oil aerosol contamination results in PCB dielectric failures. Our oil-free and fine-filtered PM screw units guarantee particle filtration down to 0.01 micron with zero hydrocarbon residues.
- Eliminates static micro-spark hazards in SMT assembly
- Continuous air purity validation for cleanroom audits
Pharmaceutical & Biotech Clean Packaging
Form-fill-seal blister packaging, pill de-dusting, and sterile laboratory dosing valves interact directly with final healthcare products. Water vapor inside air lines creates biological hazards and bacterial growth. The 5-in-1 integrated dryer and moisture separation prevents any water condensation inside pharmaceutical delivery piping.
- Microbiological barrier filtration compatible with FDA standards
- Anti-corrosive stainless steel terminal fittings
Modular Containerized Field Skids & Extreme Environments
For offshore rigs, remote mining exploration, tunneling projects, and rapid-deployment military/civil defense workshops, building brick-and-mortar air stations is impossible. Our robust 5-in-1 skid units fit cleanly inside standard ISO sea containers with external forklift pockets, handling harsh temperatures from -20°C up to +50°C without thermal de-rating.
- Forklift-ready base channels & heavy lifting eyelets
- Heavy-duty pre-filtration for dusty desert or mine sites
Craft Breweries, Beverage Canning & Distilleries
Keg washing, bottle purging, carbonation agitation, and air-actuated sanitary pinch valves demand continuous pneumatic reliability. Moisture in pneumatic cylinders can contaminate batch food products. The 5-in-1 package delivers food-grade oil and odor filtration within a compact, washdown-ready enclosure that fits alongside brewing vats.
- Washable enclosure paneling with IP54 electrical protection
- Direct connection to bottling line manifolds
China Supply Chain Resilience: How Shanghai Honest Delivers Global ODM Value
Shanghai Honest Compressor Co., Ltd. (established in 2004 as a British-invested enterprise) operates a premier 50,000 m² industrial campus in Malu Town, Jiading District, Shanghai. By anchoring production in the heart of the Yangtze River Delta industrial super-cluster, we deliver unmatched technical precision, component traceability, and rapid lead-time execution.
100km Full-Ecosystem Industrial Density
Within a 100-kilometer radius of our Jiading plant lies the world's dense supply chain for precision compressor mechanics: state-of-the-art ductile iron foundries, Kapp Niles rotor profile grinding hubs, rare-earth NdFeB permanent magnet motor fabricators, and certified pressure vessel testing labs. This geographic density eliminates intercontinental shipping delays for raw sub-assemblies, insulating our ODM clients from geopolitical logistics bottlenecks.
Agile ODM/OEM Customization Turnaround
European and North American legacy manufacturers frequently require 16 to 24 weeks of engineering lead time to modify standard schematics. Our dedicated in-house R&D engineering wing delivers complete OEM customization within 3 to 4 weeks. We support localized electrical grid configurations (208V/230V/380V/400V/415V/460V/480V across 50Hz and 60Hz), custom RAL powder coat finishes, client-branded touchscreen UI, and specialized footprint envelope adaptations.
Rigorous Factory Acceptance Testing (FAT)
Every single 5-in-1 unit that exits our assembly bays undergoes 100% full-load run-in testing in our digital test cells, adhering strictly to ISO 1217:2009 Annex C displacement verification standards. Test benches verify volumetric Free Air Delivery (FAD), shaft input power, specific energy consumption, motor thermal profiles via calibrated FLIR thermography, and tri-axial FFT dynamic vibration dampening before crating.
Technology Roadmap: The Next Decade of Autonomous Pneumatic Power
The industrial compressor sector is undergoing rapid digital and material evolution. Our engineering laboratories are actively driving three generational transitions to ensure long-term equipment relevance.
AI Predictive Telemetry & Cloud IoT
Transition from scheduled reactive servicing to real-time predictive health analytics. Integrated cellular IoT modems stream rotor vibration frequencies, bearing temperatures, motor phase current balance, and pressure differentials directly to cloud diagnostic centers.
- Algorithmic air leak detection on plant floor
- Automatic filter replacement alert triggers
- Remote firmware optimization and tuning
SynRM & Gallium Nitride (GaN) Power Stages
Adoption of Synchronous Reluctance Motors (SynRM) achieving IE5+ efficiency classes without reliance on heavy rare-earth elements, paired with next-generation GaN (Gallium Nitride) and SiC (Silicon Carbide) variable-speed inverters operating at ultra-high switching frequencies.
- Inverter electrical conversion efficiency reaches 98.8%
- Complete elimination of motor rotor thermal losses
- Radical reduction in inverter cabinet thermal heat
Zero-Carbon Cogeneration & Mag-Lev Rotors
Fully closed-loop pneumatic stations equipped with plug-and-play micro heat-recovery heat exchangers, recapturing up to 90% of electrical input energy as 70°C sanitary hot water for facility heating. Integrated magnetic levitation contactless airends will eliminate lubricants entirely.
- True friction-free magnetic levitation bearing systems
- Facility thermal cogeneration integration
- 100,000-hour maintenance-free operational life
Global Certification, Customs Expediency & Local Engineering Support
Exporting industrial pressure machinery across 50+ countries requires complete legal compliance with target jurisdiction safety codes. Shanghai Honest provides fully certified technical documentation packages with each shipment.
European Union (CE/PED)
Compliance with Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, EMC 2014/30/EU, and Pressure Equipment Directive (PED 2014/68/EU Module H/H1) for unimpeded customs entry across all EU member states.
North America (ASME / UL)
Air receiver tanks manufactured to ASME Boiler and Pressure Vessel Code (BPVC Section VIII Division 1) with official 'U' Stamp registration. Electrical panels built with UL 508A and CSA C22.2 compliant industrial switchgear.
Eurasian Customs Union
Certified to TR CU 010/2011 (Machinery Safety), TR CU 004/2011 (Low Voltage Equipment), and TR CU 032/2013 (Equipment Operating Under Excessive Pressure) for seamless entry into Russia, Belarus, and Kazakhstan.
Australia & Global Pacific
Pressure vessels designed and verified in full conformance with AS 1210 Hazard Level calculations. Electrical controllers comply with AS/NZS 3000 wiring standards, and inverters meet C-Tick electromagnetic emissions limits.
5-in-1 Standard Industrial Skid Engineering Matrix
| Model Series | Motor Power | Working Pressure | Free Air Delivery (FAD) | Integrated Receiver | Dew Point / Filtration | Sound Level |
|---|---|---|---|---|---|---|
| HNT-07V5 | 7.5 kW / 10 HP | 0.8 – 1.0 MPa | 1.10 – 1.25 m³/min | 300 L (ASME/CE) | +3°C / ≤0.01 μm, 0.003 ppm | 62 ± 2 dB(A) |
| HNT-11V5 | 11.0 kW / 15 HP | 0.8 – 1.25 MPa | 1.65 – 1.80 m³/min | 500 L (ASME/CE) | +3°C / ≤0.01 μm, 0.003 ppm | 64 ± 2 dB(A) |
| HNT-15V5 | 15.0 kW / 20 HP | 0.8 – 1.6 MPa | 2.20 – 2.45 m³/min | 500 L (ASME/CE) | +3°C / ≤0.01 μm, 0.003 ppm | 65 ± 2 dB(A) |
| HNT-22V5 | 22.0 kW / 30 HP | 0.8 – 2.0 MPa | 3.40 – 3.80 m³/min | 600 L (ASME/CE) | +3°C / ≤0.01 μm, 0.003 ppm | 67 ± 2 dB(A) |
| HNT-22L16 (Laser) | 22.0 kW / 30 HP | 1.6 – 2.5 MPa (High Pres) | 2.40 – 2.80 m³/min | 600 L (ASME High-P) | +2°C / ≤0.01 μm, 0.001 ppm | 68 ± 2 dB(A) |
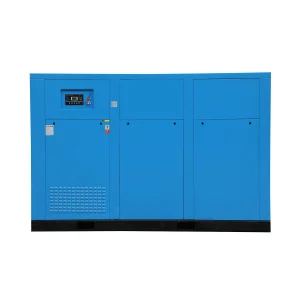
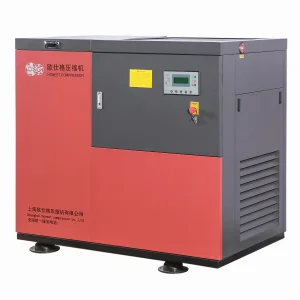
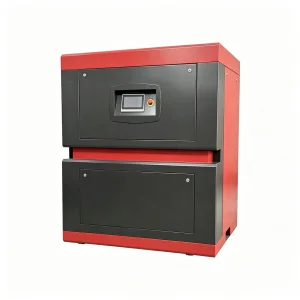
High-Pressure, Two-Stage & Oil-Free Compressor Series
Explore additional specialized models engineered by Shanghai Honest Compressor for continuous high-flow, chemical, metallurgical, and precision assist-gas applications.





Frequently Asked Engineering & Procurement Questions
In-depth responses covering thermodynamic efficiency calculations, assist-gas configuration, installation prerequisites, and long-term lifecycle maintenance.
What exact technical criteria define an authentic "5-in-1" integrated compressor station?
An authentic 5-in-1 pneumatic station is engineered as a unified thermodynamic skid comprising: (1) An asynchronous or permanent magnet rotary screw airend; (2) An integrated refrigerant air dryer utilizing a dedicated plate-fin heat exchanger; (3) An ASME/CE certified compressed air receiver tank designed as a structural and dynamic buffer; (4) A staged 4-tier to 5-tier micro-coalescent filtration battery (particulate, fine oil coalescing, and activated carbon vapor adsorption); and (5) A centralized micro-processor PLC supervisory controller that unifies the variable frequency drive, dew-point sensors, fan cycles, and electronic zero-loss condensate evacuation. Unlike makeshift field-coupled assemblies, an authentic 5-in-1 is factory-tested as a single hydraulic unit with certified specific energy consumption (SEC) and acoustic noise performance.
How does an integrated 5-in-1 PM VFD deliver 30% to 45% electricity savings compared to fixed-speed compressors?
Traditional fixed-speed compressors operate on a crude "load/unload" mechanical throttling regime. When plant air demand falls, the intake valve closes, but the electric motor continues spinning at 100% synchronous speed, drawing 40% to 60% of full-load power while producing zero air. In contrast, our Permanent Magnet Variable Frequency Drive (PM VFD) dynamically slows the motor RPM in direct linear proportion to CFM consumption. When air consumption drops by 50%, motor electrical draw drops by approximately 50%. Furthermore, by eliminating 10–20 meters of external interconnecting pipe fittings and elbows, internal hydraulic pressure drop is slashed from 0.8 bar down to under 0.08 bar. Because every 1 bar reduction in operating line pressure yields an approximate 7% drop in motor power draw, the cumulative energy savings routinely achieve 35% to 45% on variable-load production lines.
Can a 5-in-1 compressor replace liquid nitrogen for high-power fiber laser cutting?
Yes. In modern sheet metal fabrication, fiber lasers from 3kW up to 30kW frequently use assist gas to eject dross from cut kerfs. Liquid nitrogen provides excellent edge quality on stainless steel and aluminum, but carries enormous ongoing utility expenditures and continuous ambient evaporation losses. A specialized 16 bar to 20 bar 5-in-1 rotary screw station provides clean, oil-free, dry compressed air that cuts stainless up to 12mm and mild steel up to 20mm cleanly at roughly 15% to 25% of the cost of bottled or liquid nitrogen. To prevent damage to expensive protective optical lenses and cutting heads, the 5-in-1 must maintain a Pressure Dew Point (PDP) below +3°C, residual oil content below 0.003 mg/m³ (ISO 8573-1 Class 1), and particulate filtration down to 0.01 micron.
How does Shanghai Honest accommodate non-standard voltage and frequency grids globally?
Because we operate as a direct ODM/OEM manufacturer with fully integrated electrical and mechanical design teams, we engineer systems customized to any regional grid specification. We regularly deliver systems configured for: 380V/50Hz (China, Europe, Russia, MEA); 400V/50Hz (Europe, Australasia); 415V/50Hz (UK, Australia, India); 440V–480V/60Hz (USA, Canada, Mexico, Saudi Arabia industrial); and 208V–230V/60Hz (Americas commercial). Our variable frequency drives utilize dual-choke input line reactors complying with IEEE 519 harmonic distortion regulations to protect sensitive upstream CNC equipment from electrical noise.
What are the maintenance intervals and consumables required for a 5-in-1 screw compressor?
The 5-in-1 architecture utilizes standardized, easily accessible replacement modules that reduce scheduled downtime: (1) Air filter element: inspected monthly, replaced every 2,000 to 3,000 running hours; (2) Spin-on oil filter element: replaced initially at 500 hours (break-in), then every 3,000 hours; (3) Air/oil separator cartridge: replaced every 3,000 to 4,000 hours; (4) Synthetic PAO screw lubricant: 4,000 to 8,000 hours depending on operating ambient temperature; (5) Precision inline coalescing filter cartridges: replaced annually or when differential pressure gauge indicates >0.05 MPa pressure drop; (6) Refrigerant dryer condenser coil: air-blown clean monthly. Because components are organized compactly on a single skid, routine maintenance takes under 45 minutes.
How does the 5-in-1 prevent moisture condensation in unheated workshops during winter?
Condensation occurs when compressed air cools below its dew point temperature inside downstream distribution lines. The 5-in-1 eliminates this through a two-stage thermal separation mechanism. First, hot compressed air from the airend enters the air receiver tank, where radial swirl separation drops out up to 60% of bulk liquid water, which is instantly ejected via an automated zero-loss drain valve. Second, the air enters the integrated refrigerated dryer's pre-cooler and evaporator, rapidly chilling the compressed air stream to +3°C (37°F). This forces residual vapor to condense into liquid and separate. Before discharging from the machine, the cold dry air is reheated against incoming warm air inside the counter-flow plate-fin exchanger, lowering its relative humidity below 20%. As long as indoor ambient workshop temperatures remain above +3°C, zero condensation will ever form inside plant tools or piping.
