
Featured Industrial Compressors & Auxiliary Systems
Factory-direct rotary screw machinery designed for continuous duty cycles, high pneumatic pressure thresholds, and absolute moisture/oil aerosol filtration.
OEM 10A-PM Permanent Magnet Frequency Screw Air Compressor 220V 50Hz Single Phase
View Specifications
OEM 4-in-1 Explosion-Proof Air Compressor | 7.5-22kW Permanent Magnet Integrated Unit
View Specifications
OEM Industrial Screw Vacuum Pumps – Oil-Injected (0.35 mbar) & Oil-Free (20–80 kPa) Series
View Specifications
OEM Industrial 15kw–75kw Energy Saving PM Motor VSD/VFD Rotary Screw Air Compressor
View Specifications
ODM IP55/54 55KW 75HP High-Efficiency Two Stage Industrial Screw Type Compressor
View Specifications
China Oil-Free Water Lubricated Screw Air Compressor EOWV-45A/W Class 0 Standard
View Specifications
OEM 30kW Water Lubricated Oil Free VSD Screw Air Compressor 380V/400V/415V
View Specifications
China 110Kw/150Hp Two-Stage Rotary Screw Compressor Permanent Magnet Variable Frequency
View SpecificationsThe Paradigm Shift: High-Pressure Air vs. Liquid Nitrogen & Oxygen
Engineering analysis of assist gas thermodynamics, fiber laser cutting economics, and why high-pressure rotary screw compression is superseding bottled cryogenics across modern CNC machining facilities.
70% to 85% Assist Gas Cost Reduction
Traditional nitrogen (N₂) assist gas represents up to 60% of hourly operating costs on 12kW–30kW fiber lasers. Clean, high-pressure compressed air (composed of 78% Nitrogen and 21% Oxygen) provides the kinetic expulsion force needed to eject molten kerf at a fraction of liquid cryogenic gas delivery fees, eliminating tanker lease and boil-off losses.
Kerf Dynamics & Processing Speeds
The trace oxygen content in compressed air introduces an exothermic reaction when cutting mild carbon steels and thicker aluminum alloys, enhancing linear cut speeds by 15–30% compared to pure nitrogen. Simultaneously, continuous 16–25 bar kinetic purging prevents dross adhesion on lower plate edges, delivering burr-free parts ready for immediate robotic welding.
Optics & Protective Lens Integrity
High-power fiber laser cutting heads feature precision quartz protective windows valued at hundreds of dollars each. A single droplet of oil aerosol or moisture vapor under 20-bar stream will combust instantly upon crossing a 20kW laser beam, cracking the optic and ruining collimator assemblies. Our Class 0 ISO 8573-1 air trains eliminate this catastrophic failure vector.
| Evaluation Parameter | Liquid Nitrogen (Dewar/Tanker) | High-Pressure Oxygen (O₂) | Honest High-Pressure Screw Compressor |
|---|---|---|---|
| Direct Gas Cost / Hour (12kW Laser) | $18.00 – $32.00 / hr | $6.50 – $11.00 / hr | $1.80 – $3.20 / hr (Electrical Only) |
| Cut Surface Quality (Carbon Steel) | Bright silver, zero oxidation | Heavy black oxide layer, burred edges | Micro-oxidation, tight dross-free edge |
| Max Cutting Velocity (Mild Steel 3-8mm) | Baseline benchmark | Slow due to excess thermal burn | +15% to +25% Faster throughput |
| Logistics & Supply Reliability | Refill schedules, boil-off evaporation | High-pressure hazard bottles | 24/7/365 On-demand production |
| Payback Period on Equipment | N/A (Continuous operational cost) | N/A (Continuous operational cost) | 4.2 to 8.5 Months TCO amortization |
Global Procurement Specifications for Fiber Laser Facilities
What Tier-1 sheet metal fabricators, OEM laser builders, and EPC engineers mandate when specifying air compressor packages for 6kW to 60kW fiber lasers.
Pressure Dew Point (PDP) ≤ -40°C to -70°C
Standard refrigerated air dryers (producing +3°C PDP) are utterly insufficient for laser cutting. As high-pressure air expands rapidly across a supersonic laser nozzle orifice, ambient Joule-Thomson cooling induces instantaneous condensation. Our laser cutting skids combine deep refrigerated precoolers with regenerative desiccant adsorption beds, achieving deep sub-zero PDP that prevents internal beam distortion.
Five-Stage Filtration (0.001 mg/m³ Hydrocarbons)
Procurement audits require strict adherence to ISO 8573-1:2010 [Class 1:2:1] or Class 0 standards. Our dedicated laser packages integrate cyclonic bulk separators, dual high-efficiency particulate depth filters, ultra-fine coalescers, and a deep-bed activated carbon tower to strip residual oil vapor below 0.001 ppm, ensuring surgical-grade dry air arrives at the cutting head.
Continuous Flow Modulation & ±0.1 Bar Stability
Unlike intermittent stamping tools, a CNC laser cutting a nest of 25mm carbon steel demands continuous volumetric displacement with zero nozzle pressure droop. Our Permanent Magnet Variable Speed Drive (PM VFD) systems track fluctuating nozzle consumption dynamically from 25% to 100% capacity, stabilizing air line pressure within ±0.1 bar and eradicating cut line stutter.
Macro Industry Solutions: Precision Across Applications
From structural steel profiling to aerospace sheet fabrication, Shanghai Honest Compressor Co., Ltd. provides specialized high-pressure air configurations matched to material metallurgy.
Automotive Body-in-White (BIW) & Hydroformed Parts
High-throughput automotive suppliers processing ultra-high-strength steel (UHSS) and aluminum 6000-series stampings rely on our 16-bar integrated two-stage screw packages. The consistent kinetic air delivery strips micro-burrs along 3D contour lines, speeding up assembly robotic welding cells without manual grinding operations.
Electrical Enclosure & Server Rack Manufacturing
Processing galvannealed, galvanized, and stainless sheets from 0.8mm to 3.0mm demands extreme edge cleanliness for subsequent powder coating adhesion. Honest Compressor's water-lubricated oil-free and desiccant-dried air lines prevent cross-contamination, ensuring paint finishes never suffer from oil-induced blistering or pinholing.
Heavy Machinery, Shipbuilding & Yellow Goods
For cutting structural plates up to 30mm thick using 30kW–60kW ultra-high-power lasers, oxygen cutting produces excessive thermal heat distortion. Our 25–30 bar heavy-duty two-stage screw compressors deliver the immense pneumatic momentum required to sweep molten alloy through deep kerf depths while keeping part temperature controlled.
Localization Support, Regulatory Compliance & Export Logistics
Headquartered at No. 355 Jiajian Branch Road, Malu Town, Jiading District, Shanghai, our British-owned manufacturing operations maintain strict adherence to international electrical, mechanical, and pressure vessel directives.
ASME, CE-PED & Pressure Vessel Certifications
All buffer tanks, moisture separators, and heat exchange housings are engineered in compliance with EU Directive 2014/68/EU (PED) and American ASME Section VIII standards. We provide third-party certified hydro-test documentation and ultrasonic weld reports with every export consignment to guarantee immediate plant commissioning approval.
Multinational Electrical Architecture
We tailor electrical control switchgear to the destination grid: 380V/50Hz, 400V/50Hz, 415V/50Hz, 220V/60Hz, 440V/60Hz, and 460V/480V 60Hz. Controls feature Siemens or Schneider contactors, UL-compliant cabling, phase sequence monitoring, and PLC multi-language touch interfaces (English, Spanish, Russian, German, French, Portuguese, and Turkish).
Global Spare Parts Hubs & Rapid SLA
With established distributor networks across Europe, North America, Southeast Asia, and the Middle East, genuine consumable kits (rotor lubricant, precision micro-filter elements, desiccant beads, and check valve seals) are dispatched within 24 hours. Our Shanghai factory team provides direct remote tele-diagnostics and field engineering dispatch.
Engineering Roadmap: Next-Gen Laser Pneumatics
Anticipating the technological demands of 60kW+ fiber lasers, smart factory Industry 4.0 interconnectivity, and carbon-neutral green fabrication facilities.
Integrated 4-in-1 Compact Laser Skids
Mounting the rotary screw airend, 500L/1000L buffer vessel, refrigerated pre-cooler, and 5-stage filtration onto a single forkliftable vibration-damped structural base, cutting plant installation time to 30 minutes.
Dynamic Pressure-Tracking Cloud Telematics
IoT-connected inverter drives that communicate over Modbus-TCP and OPC-UA directly with CNC laser controllers (Bystronic, Trumpf, Amada, Han's, Bodor), adjusting compressor delivery pressure in real-time based on NC program piercing commands.
Ultra-High Pressure (35 Bar) Direct Injection
Developing dedicated booster screw stages capable of delivering 3.5 MPa (35 bar) for high-speed cutting of 40mm+ thick titanium, Hastelloy, and structural armor plate with zero bottom slag.
Zero-Loss Waste Heat Recovery (CHP)
Integrating closed-loop thermal recovery modules that capture up to 94% of electrical input energy from oil coolers and airend jackets to provide free preheated water for factory degreasing and powder coat curing lines.
Laser Cutting Compressed Air: Engineering FAQ
Detailed answers to critical sizing, metallurgical compatibility, and operational questions asked by plant managers and procurement teams.
What pressure and CFM flow rates are required for 6kW, 12kW, 20kW, and 30kW fiber lasers?
Air consumption depends primarily on nozzle diameter and operating cut pressure rather than laser wattage alone, although higher power units cut thicker materials using larger nozzles:
• 6kW Laser (1.5mm–2.5mm nozzle): Requires 16 bar (232 psi) working pressure at 1.2 to 1.8 m³/min (42–64 CFM). A 15kW to 22kW compressor is ideal.
• 12kW Laser (2.5mm–3.5mm nozzle): Requires 16–20 bar (232–290 psi) at 2.0 to 2.8 m³/min (70–99 CFM). Recommended compressor: 22kW to 30kW.
• 20kW–30kW Laser (3.5mm–5.0mm nozzle): Demands 20–25 bar (290–362 psi) delivering 3.2 to 4.8 m³/min (113–170 CFM). A 37kW to 55kW two-stage high-pressure screw compressor is specified.
How does microscopic oil carryover destroy protective laser optics and cutting heads?
When high-pressure air carries oil aerosols (even down to 0.1 mg/m³), the vapor settles onto the lower quartz protection window of the cutting head. As a 10kW+ laser beam focuses through this optic, the hydrocarbon molecules absorb optical energy exponentially, creating extreme localized thermal hot spots. This phenomenon, known as "thermal lensing," distorts the focal point, ruins cutting precision, and ultimately causes the window to shatter violently, allowing contamination into the upper collimator lenses and fiber optic termination crystal.
Can high-pressure compressed air completely replace nitrogen for stainless steel cutting?
For decorative architectural stainless steel or food/pharmaceutical sanitary tubing where 100% oxide-free silver reflective edges are mandatory, pure nitrogen remains necessary. However, for 80% of structural, industrial, and enclosure manufacturing where parts are subsequently powder-coated, painted, or welded, air cutting produces a remarkably clean edge with a faint, tight golden-yellow micro-oxide layer. Because this surface exhibits high paint adhesion without manual prep, major manufacturers have transitioned almost entirely to air cutting.
Why is two-stage compression superior to single-stage for 16 to 30 bar discharge?
Compressing atmospheric air directly to 20 bar in a single screw airend results in an excessive pressure ratio (~20:1), generating extreme internal heat, heavy bearing thrust loads, and increased rotor bypass leakage. A two-stage compressor splits this into two stages with inter-stage cooling: Stage 1 compresses from 1 to 5 bar, the air is cooled, and Stage 2 compresses from 5 to 20 bar. This reduces specific energy consumption by 15% to 25%, lowers operating temperatures by 30°C, and substantially extends bearing life beyond 60,000 service hours.
What size air storage tank is required to prevent pressure dips during rapid piercing cycles?
Laser piercing cycles require sudden bursts of maximum flow. To prevent upstream line pressure collapse, we recommend a high-pressure receiver tank sized at approximately 25% to 35% of the compressor's rated minute volumetric capacity. For example, for a 3.0 m³/min compressor, a 1000-liter (1.0 m³) air receiver rated at 20–30 bar acts as an energy buffer, stabilizing nozzle pressure and eliminating rapid compressor load/unload cycles.
What are the OEM/ODM branding and custom voltage capabilities from your Shanghai factory?
Shanghai Honest Compressor Co., Ltd. provides comprehensive OEM/ODM engineering. We can supply customized chassis colorways matching your laser machine aesthetics, private-label branding on PLC touchscreens, tailored skid dimensions for compact containerized laser cells, and customized motor windings for regional grids (such as 208V/230V/460V 60Hz for the Americas or 400V 50Hz for Europe). Complete documentation, exploded CAD drawings, and CE/ASME paperwork are included.
Continuous-Duty Rotary Screw & Specialty Compressors
Precision engineered for metal processing workshops, automated assembly lines, process aeration, and continuous vacuum handling.

China Permanent Magnet VFD Rotary Screw Compressor 11kW Manufacturer
View Specifications
ODM PM&VSD Oil‑Free Screw Blower Industrial Factories, Exporters
View Specifications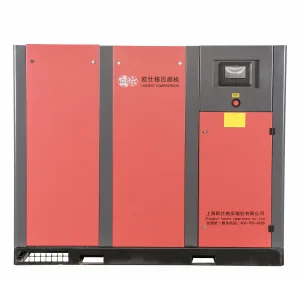
OEM Double Permanent Magnet Motor Integrated Two-Stage Compression Series
View Specifications
OEM 18.5kW 25HP Industrial VFD PM Screw Air Compressor Factory, Exporter
View Specifications
OEM 22kW 30HP Variable Speed Rotary Screw Compressor Factories, Exporter
View Specifications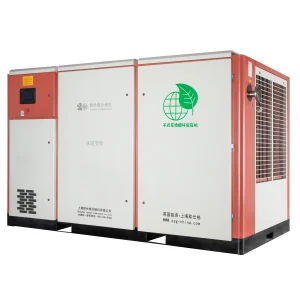
ODM EOF Oil-Free Dry Screw Compressor | 100% Oil-Free PM VFD Technology
View Specifications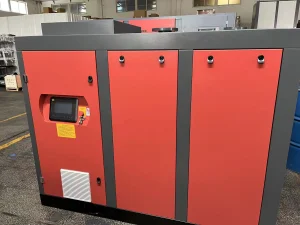
ODM Electrical Motor PM AC ASD Rotary Air Vacuum Pump Screw Compressor
View Specifications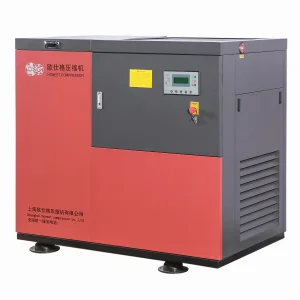
China 20bar Pressure Screw Air Compressor for Laser Cutting Machine Supplier
View SpecificationsRequest an Engineering Air Sizing Consultation
Supply your laser wattage, nozzle diameters, processed metal thicknesses, and site utility voltages. Our application engineering team in Shanghai will calculate your exact pneumatic CFM flow rate, storage volume buffer, and provide a comprehensive TCO ROI analysis.
