
High-Efficiency 75 HP Systems & Modular Airends
Configured for continuous 24/7 duty cycles across petrochemical, precision manufacturing, and process air applications. Compliant with international ISO 1217 standards.
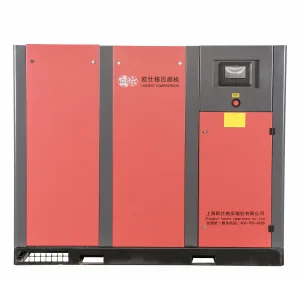
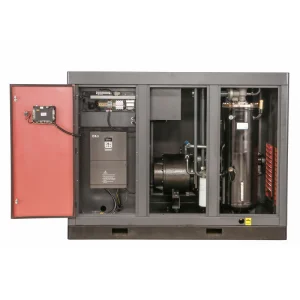

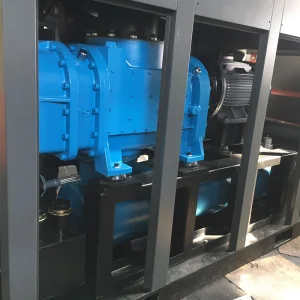


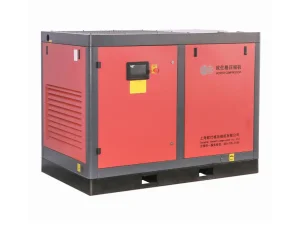
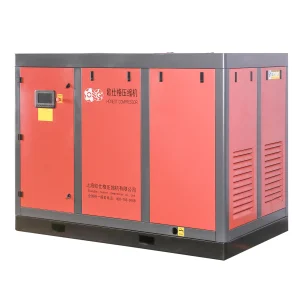
The Macro Landscape: 75 HP (55kW) as the Workhorse of Modern Industrial Utilities
In the contemporary industrial infrastructure landscape, compressed air is globally recognized as the "Fourth Utility," alongside electricity, natural gas, and water. Industrial facilities across North America, the European Union, Southeast Asia, and the Middle East deploy significant fractions of their total plant energy strictly to fuel compressed air generation. Within this matrix, the 75 HP (55kW) rotary screw compressor occupies the most critical volumetric niche. It represents the vital transitional threshold between decentralized light-manufacturing point-of-use units and centralized high-tonnage utility plant networks.
From a macroscopic commercial perspective, industrial plant operators no longer evaluate compressor procurement solely on the initial machine capital expenditure (CAPEX). Comprehensive life cycle cost (LCC) auditing reveals that over a standard 10-year operating horizon (operating 6,000 to 8,000 hours annually), capital purchase expenses account for merely 10% to 12% of overall lifecycle expense. Routine maintenance and filtration consumables represent approximately 11% to 13%, whereas electricity consumption absorbs an overwhelming 75% to 78% of total expenditure. Consequently, specifying an optimized OEM 75 HP compressor system with modern Permanent Magnet Variable Frequency Drive (PM VFD) and two-stage compression physics is no longer an incremental choice—it is a mandatory enterprise-level decarbonization strategy.
As global carbon boundary adjustment mechanisms (such as the EU CBAM) tighten and national energy intensity standards (such as China GB19153 Tier-1, US DOE electric motor efficiency standards, and European Ecodesign directives) elevate requirements, manufacturing plants are aggressively replacing antiquated fixed-speed load/unload units. A modern OEM 75 HP direct-drive rotary screw machine engineered by Honest Compressor matches precise real-time factory flow dynamics (Free Air Delivery: 1.20 to 10.8 m³/min across 7.0 to 13.0 bar variants), completely neutralizing no-load idling dissipation and delivering measurable specific power consumption reductions down to 5.4 to 6.2 kW/(m³/min).
Thermodynamic Excellence: Two-Stage vs. Single-Stage 75 HP
Discover how intermediate pressure intercooling and permanent-magnet rotor dynamics yield industry-leading volumetric efficiencies.
Two-Stage Quasi-Isothermal Physics
By splitting total compression ratio across two serial rotor pairs with intermediate oil-curtain intercooling, internal thermal expansion and back-leakage are suppressed. The compression process approaches the ideal theoretical isothermal baseline, saving 9% to 15% input kW compared to single-stage equivalents.
IE4/IE5 Ultra-Premium PM Motors
Utilizing high-coercivity NdFeB permanent magnets rated for 180°C demagnetization safety thresholds. Oil-cooled motor casing designs isolate heat away from the winding heads, sustaining motor efficiency exceeding 96.5% even during turndown ratios as wide as 25% to 100% capacity.
5:6 Helical Asymmetric Rotors
CNC rotor profiling cut with German Klingelnberg and Holroyd precision machinery. Dynamic mechanical tolerances held strictly below 5 microns ensure minimal blow-hole clearance, reducing internal bypass recirculation and ensuring sustained CFM flow delivery over 100,000 bearing operational hours.
| Performance Metrics (at 8.0 Bar Operating Pressure) | Standard Single-Stage 75 HP (Fixed Speed) | Honest PM VFD Single-Stage 75 HP | Honest Double PM Two-Stage 75 HP (Top Tier) |
|---|---|---|---|
| Rated Flow Capacity (FAD m³/min / CFM) | 9.10 m³/min (321 CFM) | 9.60 m³/min (339 CFM) | 10.85 m³/min (383 CFM) |
| Specific Power Input (kW / m³/min) | 6.95 kW/(m³/min) | 6.32 kW/(m³/min) | 5.68 kW/(m³/min) (Tier-1 Level) |
| Unload Energy Waste (% of Rated Power) | 35% – 45% Waste in idle mode | 0% (Motor decelerates & stops) | 0% (Instant dual motor speed match) |
| Rotor Bearing Mechanical Stress | High (Bearing load ratio 100%) | Moderate (Load modulated by VFD) | Low (≈ 40% bearing load per stage) |
| Operational Noise Level (dB(A) ± 2) | 76 – 78 dB(A) | 70 – 72 dB(A) | 65 – 68 dB(A) (Whisper Industrial) |
| Expected Bearing Overhaul Interval | 25,000 – 35,000 Hours | 40,000 – 50,000 Hours | 70,000 – 100,000 Hours |
Global OEM/ODM Customization & Export Readiness
Tailored engineering frameworks designed specifically for global brand distributors, EPC engineering firms, and high-volume compressed air machinery importers.
Brand Private Labeling
Full-scale enclosure customization, customized RAL color powder coating, laser-cut client logos, branded user interface touchscreens, and bespoke technical document asset kits.
Multi-Grid Electrics
Adaptable power architectures compliant with 3-phase 208V/220V, 380V, 400V, 415V, 460V, and 480V networks across both 50Hz and 60Hz grids with built-in harmonic reactor filtration.
Export Crating Rigor
Treated seaworthy fumigated ISPM-15 wooden packaging with internal vacuum vapor-barrier sealing, silica desiccant packs, and shock-sensor telemetry for transit via marine container transport.
Spare Parts Logistics
Fast-track consignment programs for air end rebuild kits, synthetic lubricants, micron-rated oil separator elements, and air filters with guaranteed 48-hour global air-freight dispatch.
Global Compliance Assurance: Certified for Market Entry
Navigating international regulatory frameworks with fully validated third-party testing, pressure boundary qualifications, and electrical safety certifications.
European Union: CE-PED & MD
Full alignment with Pressure Equipment Directive (PED 2014/68/EU Module H/H1), Machinery Directive 2006/42/EC, and Electromagnetic Compatibility (EMC Directive 2014/30/EU). Enclosed separators and safety release valves stamped with notified body approvals.
North America: ASME & UL/CSA
Oil-gas separator vessels manufactured in strict conformity with ASME Section VIII Division 1 requirements (stamped with 'U' or 'UM' indicators). Electrical control cubicles assembled with UL 508A and CSA C22.2 recognized industrial control components.
Air Purity: ISO 8573-1 Class 0
Validated by TÜV Rheinland for total hydrocarbon concentration below detectable analytical limits (≤ 0.003 mg/m³). Essential for pharmaceutical, cleanroom electronics, infant nutrition processing, and critical medical respiratory applications.
Targeted Heavy-Duty Application Profiles for 75 HP Systems
Discover how specific industrial verticals leverage the 55kW platform to maximize operating uptime, air purity, and process yields.
Fiber Laser Cutting (16–20 Bar)
High-pressure auxiliary cutting air. A 75 HP booster or dedicated high-pressure screw compressor provides clean, dry air as a cost-effective substitute for high-cost bottled nitrogen in mild steel and aluminum sheet processing.
Automotive & Assembly Robotics
Feeding high-speed stamping transfer lines, multi-axis pneumatic tooling, and electrodeposition spray painting booths. Wide PM VFD turndown handles erratic swing loads during shifts seamlessly.
Chemical & Pharmaceutical Plants
Fluidized bed aeration, powder pneumatic conveying, bioreactor gas blanketing, and sterile container bottle blowing. Deploying oil-free water-lubricated units prevents volatile hydrocarbon contamination.
Mining & Heavy Metallurgy
Harsh ambient desert and high-altitude quarry operations. Features oversized heavy-duty nano-synthetic air pre-filtration, cyclone water separation, and tropical ambient coolers rated up to 52°C.
Technological Roadmap: Next-Gen Compression (2026–2035)
Discover the vanguard of industrial compressed air engineering: edge-AI predictive algorithms, synchronous reluctance motors, and full thermodynamic thermal recovery.
AI-Driven IoT & Telemetry
Integrated micro-electro-mechanical (MEMS) vibration sensors and infrared oil viscosity telemetry. Onboard neural edge controllers calculate remaining bearing life and alert technicians prior to catastrophic failure.
IE6 Synchronous Reluctance
Moving beyond traditional permanent magnet alloys to ferrite-assisted synchronous reluctance motor (SynRM) designs, avoiding rare-earth price volatility while achieving hyper-efficiency ratings under partial loading.
94% Waste Heat Recovery
Integrated plate-type heat exchangers harness mechanical and compression friction heat, channeling 70°C water into district heating, boiler make-up feedwater, or municipal cleaning loops.
Carbon Nanotube Coatings
Applying diamond-like carbon (DLC) and fluoropolymer nanotube matrices directly to the rotor lobes, completely eliminating dry-screw friction wear and enabling elevated pressure ratios without oil lubricants.
Engineering Procurement FAQ: OEM 75 HP Sourcing
Addressing the most critical technical, commercial, and operational questions asked by plant engineers and overseas procurement directors.
A two-stage 75 HP (55kW) rotary screw compressor reduces the pressure ratio across each individual compression chamber by roughly 50%. This thermodynamic easing drops mechanical blow-by and discharge temperatures. In continuous 8,000-hour/year operations at $0.12/kWh, the 12% to 15% efficiency advantage generates direct annual savings between $6,300 and $7,900 USD, amortizing the initial equipment price differential in roughly 10 to 14 months.
Standard configurations operate reliably up to 45°C (113°F). However, for export shipments intended for the Middle East, North Africa, or equatorial Southeast Asia, Honest Compressor equips machines with high-ambient tropicalization packages: oversized aluminum-bar matrix heat exchangers, IP55-rated variable speed cooling fans, and synthetic ester or polyalphaolefin (PAO) lubricants rated to withstand 52°C (125°F) ambient thresholds.
Micro-oil lubricated screw compressors utilize triple-stage centrifugal and coalescing filtration, yielding residual oil carryover between 1 to 3 ppm (Class 1-2). This is fully adequate for mechanical tooling, metallurgy, and general automotive lines. However, when compressed air directly contacts food packaging, pharmaceutical formulations, semiconductors, or optical lens glass, an ISO 8573-1 Class 0 certified oil-free water-lubricated machine is non-negotiable to prevent total batch contamination liability.
All Honest 75 HP OEM units are built around modern PLC microcontrollers featuring multi-language 7-inch color touch displays. Native hardware includes RS-485 interfaces supporting Modbus RTU / Modbus TCP protocols. Optional modular expansion boards facilitate Profibus, CANopen, and Ethernet/IP protocols, allowing real-time parameter streaming (current, pressure, temperature, dew point, and filter differential pressure) directly into plant distributed control systems (DCS).
Every machine leaving our Shanghai manufacturing hub undergoes rigorous ISO 1217 Annex C full-load testing. Consignments are accompanied by factory calibration certificates, pressure vessel ASME/PED hydrostatic test certificates, electrical safety test logs (dielectric breakdown & ground continuity), complete wiring schematics, and exploded parts manuals in English.
Standard unbranded stock models can be dispatched within 7 to 10 working days. For full OEM customized orders (incorporating client branding, custom paint schemes, bespoke controller programming, and specific regional voltage combinations), the standard production lead time is 18 to 25 business days, with flexible MOQs starting at 1 unit for evaluation samples.
Specialized 75 HP, High-Pressure & Oil-Free Solutions
Explore additional specialized configurations: laser cutting high-pressure packages, industrial vacuum systems, explosion-proof units, and oil-free rotary architectures.





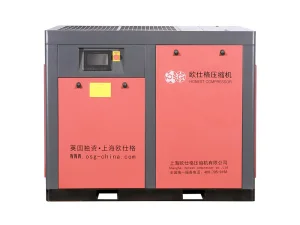
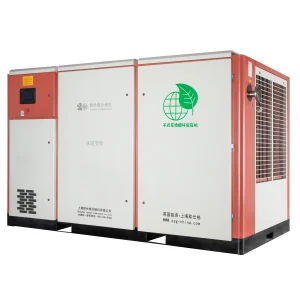
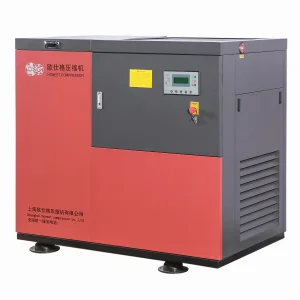
Global Engineering Sourcing Protocol: Honest Compressor Factory Direct
When selecting an overseas OEM manufacturing partner for 75 HP (55kW) rotary screw units, engineering teams must evaluate three fundamental non-negotiable vectors: Airend Precision Manufacturing, Motor-Inverter Synchronization Stability, and Total Process Testing Integrity. At our British-invested 50,000 square meter Shanghai production facility, every stage of production conforms strictly to ISO 9001 and ISO 14001 guidelines.
From initial cast iron structural stress-relieving and 5-axis CNC asymmetric screw rotor machining to static and dynamic balance testing (G2.5 balancing grade), our production workflows minimize rotational harmonics. Every completed 75 HP compressor undergoes an uninterrupted 4-hour full-load factory acceptance test (FAT) evaluating vibration velocity (≤ 2.8 mm/s), bearing operating thermal saturation (ΔT ≤ 45°C), specific energy consumption under ISO 1217 Annex C parameters, and automatic unloader safety cut-offs.
Partnering with Honest Compressor provides global distributors and machinery brand owners with an uncompromising balance of cutting-edge thermodynamic efficiency, comprehensive regulatory certification, and dedicated after-sales spare parts support across more than 50 export countries.
