
Featured Industrial Air Compression Units
Explore our OEM/ODM modular compressors engineered for extreme industrial duty, maximum fuel displacement efficiency, and Class 0 contamination resistance.

China Honest Compressor -EOF series Oil-Free Dry Type Screw Compressor | 100% Oil-Free PM VFD Manufacturer, Exporter
View Product Specs
ODM PM&VSD Oil‑Free Screw Blower Factories, Exporters
View Product Specs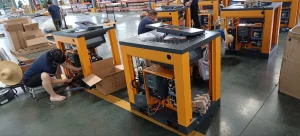
OEM 10A-PM permanent magnet frequency screw air compressor 220v 50hz single phase Suppliers, Exporters
View Product Specs
ODM IP55/54 55KW 75HP Factory Price Two Stage Industrial Screw Type Air Compressor Machine Factories, Exporters
View Product Specs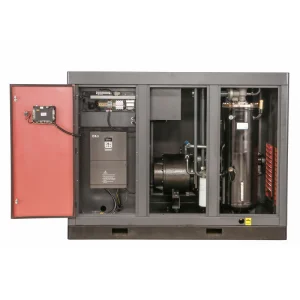
ODM Oil-cooled two-stage permanent magnet variable frequency screw air compressor Manufacturers, Suppliers
View Product Specs
OEM Oil Free Water Lubricated Screw Air Compressor 37kW Supplier, Factories
View Product Specs
OEM 18.5kW 25HP Industrial VFD PM Screw Air Compressor Factory, Exporter
View Product Specs
OEM High Precision Operational Safety Micro Oil Screw Vacuum Pump for Vacuum Industry Supplier, Exporters
View Product SpecsMacro Industry Solutions: Engineering Heavy-Duty Diesel-Powered Pneumatic Systems
In global industrial operations where utility electric grids are inaccessible, unstable, or financially unviable, diesel-powered rotary screw air compressors serve as the primary lifeblood of pneumatic energy. As a premier original equipment manufacturer (OEM) and international exporter, our manufacturing standard goes far beyond basic mechanical assembly. We engineer fully integrated thermodynamic systems tailored to survive the world’s most demanding industrial micro-environments.
From deep-pit open-cast mining operations in Western Australia to offshore oil platform decommissioning in the North Sea, off-grid pneumatic power demands relentless mechanical reliability. A drop in air delivery pressure or catastrophic engine thermal shutdown translates directly into substantial operational downtime costs. To mitigate these risks, modern OEM diesel compressor architectures merge heavy-duty internal combustion engines with high-efficiency twin-screw rotary air ends, regulated by intelligent electronic controller units (ECUs).
Optimal diesel compressor efficiency depends on precisely matching the engine's torque curve to the rotary screw's power demand across variable working pressures (7 bar to 35 bar). Our proprietary dynamic load control system modulates the intake throttle valve and engine RPM simultaneously, eliminating parasitic power loss during unloaded idling states.
Mining & Geotechnical Exploration
High-pressure diesel compressors (25–35 bar) power Down-The-Hole (DTH) hammer drilling rigs, reverse circulation sampling, and underground tunnel ventilation. Engineered with dual-stage heavy-duty air intake filters to process up to 99.9% of ambient silica dust particles before air reaches internal compression rotors.
Infrastructure & Heavy Construction
Supplying reliable pneumatic volume (15–30 m³/min) for shotcreting, pneumatic jackhammers, foundation piling, and bridge surface preparation. Designed with compact towable skids, low center of gravity, and heavy-duty leaf-spring axles for high-speed highway trailering across rough terrain.
Energy & Pipeline Maintenance
Essential for oil & gas pipeline pigging, pressure testing, nitrogen purging preparation, and abrasive sandblasting prior to anti-corrosion coating application. Integrated with certified spark arrestors and emergency automatic overspeed shut-off valves (Chalwyn valves) for safe operation in hazardous Zone 2 environments.
Global Commercial & Industrial Landscape: Market Dynamics & TCO Analysis
The global market for diesel-driven air compressors is undergoing a structural transition driven by stringent environmental regulations, escalating fuel prices, and the requirement for integrated remote telemetry. International buyers—ranging from regional equipment rental fleets to multinational EPC (Engineering, Procurement, and Construction) conglomerates—evaluate supplier partnerships based on Total Cost of Ownership (TCO) rather than upfront capital expenditure (CAPEX).
Over a typical 10,000-hour operational lifecycle of a diesel air compressor, initial purchase cost accounts for only 15% to 20% of total expenditure. Diesel fuel consumption represents approximately 65% to 70%, with routine maintenance and spare parts comprising the remaining fraction. Consequently, our OEM engineering team focuses on maximizing specific fuel efficiency (measured in liters of diesel consumed per cubic meter of air delivered, L/m³).
| Performance Metrics | Standard OEM Tier 2 Engine Baseline | Advanced Stage V / Tier 4F OEM Package | Operational Value Impact |
|---|---|---|---|
| Specific Fuel Consumption (SFC) | 215 – 225 g/kWh | 190 – 198 g/kWh | 12% to 15% Reduction in Annual Fuel Spend |
| Emissions Standard Compliance | High PM & NOx Output | DPF + SCR Aftertreatment (Zero Smoke) | Unrestricted Access to EU/US Urban Construction Zones |
| Airend Rotor Profile Efficiency | Standard 5:6 Asymmetric Profile | Optimized 5:6 / 4:6 Rotor Geometry | Higher Free Air Delivery (FAD) per kW input |
| Maintenance Service Interval | 250 Hours (Engine Oil/Filters) | 500 Hours (Synthetic Lubricants + HD Filtration) | 50% Reduction in Planned Operational Downtime |
| Asset Resale Value (5-Year Horizon) | 30% – 35% of Purchase Price | 55% – 60% of Purchase Price | Substantially Lower Fleet Amortization Costs |
Regional Regulatory Alignment & Global Trade Compliance
Exporting heavy industrial machinery requires comprehensive knowledge of localized market regulations. As an established global exporter, our OEM manufacturing lines maintain dual-track production pathways:
- Regulated Markets (North America, European Union, Japan, South Korea): Units are integrated with Tier 4 Final / Stage V ultra-clean diesel powerplants (CUMMINS, DEUTZ, CAT, PERKINS) featuring Diesel Particulate Filters (DPF) and Selective Catalytic Reduction (SCR) with DEF injection systems.
- Lesser-Regulated Markets (LATAM, Southeast Asia, Middle East, Africa): Units are equipped with rugged Tier 2 / Tier 3 mechanically governed or simplified common-rail engines designed to handle high-sulfur diesel fuel (up to 5,000 ppm) without fuel injector failure.
Technical Engineering & Modular OEM Customization
Standard off-the-shelf air compressors often fail when subjected to localized operational extremes. True OEM flexibility requires engineering modular components that can be customized to match precise site specifications, ambient temperatures, and air quality mandates.
Custom Air-End Rotor Design
Our precision twin-screw rotors are machined using high-accuracy German CNC grinder technology. Featuring advanced SAP (Symmetric Asymmetric Profile) tooth geometry, these rotors maintain high volumetric efficiency with minimal internal blow-by leakage, achieving direct air delivery up to 40 m³/min per single unit.
Extreme Thermal Management
Engineered for environmental conditions ranging from -40°C arctic freezes to +55°C desert ambient heat. Packages include oversized aluminum matrix oil coolers, independent thermostatically controlled electric fans, engine coolant pre-heaters (Webasto system), and anti-recirculation baffle plates.
Intelligent Microprocessor Controllers
Features color graphical IP65 digital control panels supporting multi-language interfaces (English, Spanish, Russian, French, Arabic). Displays real-time parameters including engine torque load, compressor discharge temperature, oil pressure, fuel consumption rate, and DPF soot accumulation level.
Acoustic & Environmental Canopy Options
Heavy-gauge galvannealed steel enclosures coated with outdoor-grade electrostatic powder paint provide superior corrosion resistance. Sound-dampening flame-retardant foam lining reduces operational noise levels down to 68 dBA @ 7 meters, satisfying urban noise regulations.
Localized Field Applications & Real-World Operating Scenarios
Deploying diesel air compressors successfully requires accommodating localized environmental conditions. Below are detailed operational scenarios demonstrating how optimized OEM configurations resolve field challenges:
High-Altitude Mining (4,000m+ Andes Region)
Challenge: Rarefied air reduces atmospheric air density, causing severe diesel engine power derating and reduced compressor volumetric efficiency.
OEM Solution: Turbocharged intercooled engines matched with oversized displacement airends. Customized ECU calibration adjusts fuel injection timing and boost pressure dynamically, restoring up to 92% of nominal rated air delivery at high elevation.
Offshore Platform Drilling (Humid & Saline)
Challenge: Salt spray causes rapid galvanic corrosion of aluminum coolers, steel enclosures, and electrical wiring harnesses.
OEM Solution: DNV 2.7-1 certified lifting frames, 316L stainless steel hardware, C5-M marine-grade multi-layer epoxy coating, offshore-spec copper-tube aluminum-fin coolers, and IP67 sealed wiring systems.
Urban Tunnel Boring & Shotcreting
Challenge: Strict low-noise limits in residential zones combined with confined space emissions compliance.
OEM Solution: Ultra-silent canopy design with multi-stage baffled air intake and discharge louvers. Tier 4 Final / Stage V aftertreatment eliminates visible particulate emissions and odorous hydrocarbon compounds.
Localized Support, Quality Compliance & Global Export Infrastructure
Exporting heavy equipment requires more than just building robust machinery; it requires an infrastructure built for global support. As a dedicated exporter, our factory provides complete supply chain transparency, international certifications, and long-term aftermarket parts support.
Quality Certification & Factory Acceptance Testing (FAT)
Every custom diesel compressor manufactured at our plant undergoes rigorous Factory Acceptance Testing (FAT) prior to crating. Tests follow ISO 1217 Annex C/E standards for Free Air Delivery (FAD) measurement, sound pressure testing according to ISO 2151, and full electrical/hydraulic pressure safety checks under CE-PED standards.
• ISO 9001:2015 Quality Management System Certificate
• CE Certificate of Conformity (Pressure Equipment Directive 2014/68/EU)
• ISO 1217 Performance Test Guarantee Report
• Engine Manufacturer Global Warranty Certificate
Spare Parts Staging & Logistics Security
We maintain an inventory of fast-moving maintenance consumables (oil filters, air filter elements, separator cartridges, compressor lubricant, engine drive belts) ready for air freight dispatch within 24 hours. For long-term fleet deployments, we provide customized "500-Hour / 2000-Hour Maintenance Kits" packaged in heavy-duty export crates alongside the machinery.
All export units feature reinforced lifting lugs, integrated fork pockets, and heavy-duty tie-down points engineered for container shipping (20GP/40HQ) or flat-rack transport.
Technology Roadmap: Next-Gen Off-Grid Compression (2025–2035)
As global industries aim to cut net carbon emissions, diesel compressor technology is advancing rapidly. Our R&D division is focused on three key technological areas to maintain long-term competitive advantage:
1. Hybrid Diesel-Electric Dual Drives
Developing hybrid air compressors that combine a high-efficiency Stage V diesel engine with a Permanent Magnet Electric Motor (PM-VFD). When on-site utility electricity is available, the unit operates silently on electric power; when working off-grid, the diesel engine engages automatically.
2. AI Telematics & Predictive Health Monitoring
Integrating 4G/5G IoT telematics modules with CAN-bus controllers. Proprietary cloud algorithms monitor vibration signatures, thermal dynamics, and filter differential pressures in real-time, predicting component failure weeks before field breakdown occurs.
3. Hydrogen-Diesel Dual Fuel & Bio-Diesel (HVO)
Engineered engine intake manifolds capable of burning Hydrotreated Vegetable Oil (HVO100) bio-diesel, cutting net CO2 emissions by up to 90%. Active development of co-injection systems utilizing green hydrogen fuel blend ratios.
Frequently Asked Questions (FAQ) & Engineering Selection Guide
Additional OEM/ODM Compressed Air Solutions
Browse our complete export product line designed for continuous duty industrial applications, vacuum processes, and specialized high-pressure air demand.

China Horizontal two-stage pressure screw air compressor Two Stage Screw Air Compressor Electric Screw Air Compressor Price Suppliers, Exporters
View Product Specs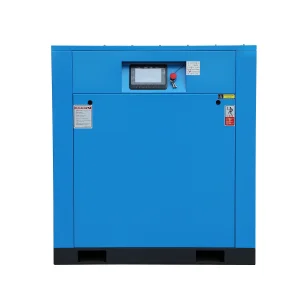
OEM VFD screw air compressor 0.7-1.25mpa Energy Saving up to 30% Manufacturers, Exporter
View Product Specs
OEM 22kW 30HP Variable Speed Rotary Screw Compressor Factories, Exporter
View Product Specs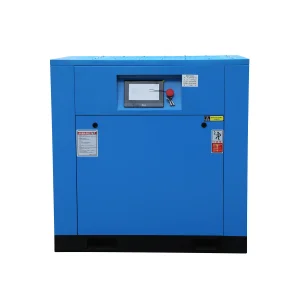
OEM Industrial 15kw/22kw/37kw/55kw/75kw Energy Saving Pm Motor VSD/VFD Rotary Screw Air Compressor Manufacturer, Exporters
View Product Specs
China 110Kw/150Hp Two-Stage Rotary Screw Air Compressor Permanent Magnetic Variable Frequency 380V Air Cooled Exporter, Exporters
View Product Specs
China Permanent Magnet VFD Rotary Screw Compressor 11kW Manufacturer, Manufacturers
View Product Specs
China 55KW 75HP 7-13bar air compressor two stage screw air compressor Direct Drive Screw Type Compressors with VSD PM motor and Inverter Factory, Factories
View Product Specs
