Specialized High-Pressure & Variable Frequency Systems
Continuous duty 24/7 air compressors, variable-frequency permanent magnet units, and process vacuum systems engineered for mission-critical industrial manufacturing.
China 20bar pressure Screw Air Compressor for laser cutting machine Supplier, Suppliers
View Product Specs
OEM High Precision Operational Safety Micro Oil Screw Vacuum Pump for Vacuum Industry Supplier, Exporters
View Product Specs
OEM 18.5kW 25HP Industrial VFD PM Screw Air Compressor Factory, Exporter
View Product Specs
China Low Noise Industrial High Efficiency 10HP 15HP 20HP 30HP 100HP Rotary Pm VSD Screw Type Air Compressor Factory, Exporter
View Product Specs
China 110Kw/150Hp Two-Stage Rotary Screw Air Compressor Permanent Magnetic Variable Frequency 380V Air Cooled Exporter, Exporters
View Product Specs
China Permanent Magnet VFD Rotary Screw Compressor 11kW Manufacturer, Manufacturers
View Product Specs
China Oil-Free Water Lubricated Screw Air Compressor EOWV-45A/W Suppliers, Exporter
View Product Specs
China Honest Compressor -EOF series Oil-Free Dry Type Screw Compressor | 100% Oil-Free PM VFD Manufacturer, Exporter
View Product SpecsMacro-Industry Paradigm Shift: Gas Aerodynamics & The Economics of High-Pressure Assist Air
In the contemporary thermal cutting sector, industrial laser processing has experienced an exponential escalation in output power. While 2kW to 4kW CO₂ and early fiber oscillators once dictated fabrication schedules, the modern manufacturing standard has pivoted decisively to 12kW, 20kW, 30kW, and ultra-high-power 60kW fiber laser engines. At these intense energy densities, cutting velocity is no longer constrained solely by photonic flux absorption; rather, the fundamental rate-determining step has shifted to hydrodynamic melt ejection within the narrow kerf slot.
Historically, fabrication facilities relied upon liquid nitrogen ($LN_2$) or oxygen ($O_2$) as assist gases. Oxygen relies on an exothermic iron-oxygen combustion reaction, which introduces thermal runaways, excessive edge heat-affected zones (HAZ), and heavy oxide scaling unsuitable for immediate welding or e-coating. Liquid nitrogen provides an inert mechanical blowout mechanism preventing oxidation; however, the recurring operational expenditure (OPEX) associated with bulk cryogenic tank vaporization, logistics deliveries, boil-off evaporation losses, and regional distribution tariffs imposes a severe financial penalty on contract fabricators.
This is where High-Pressure Compressed Dry Air (CDA) between 16 and 30 bar (232 to 435 psi) has emerged as the definitive industrial disruptor. Composed of approximately 78% Nitrogen and 21% Oxygen, high-pressure compressed air delivers high kinetic momentum at the nozzle throat while introducing a tightly controlled, localized minor exothermic burst. This hybrid thermodynamic action melts and expels dross at velocities exceeding pure Nitrogen in thin-to-medium sheet metals (1mm to 12mm), while yielding an astounding 70% to 85% reduction in recurring assist gas expenditures.
| Evaluation Parameter | High-Pressure CDA (16–30 Bar System) | Cryogenic Bulk Liquid Nitrogen ($LN_2$) | High-Pressure Bottled Oxygen ($O_2$) |
|---|---|---|---|
| Primary Removal Mechanism | Kinetic momentum impulse + Controlled micro-oxidation | Pure mechanical viscous shear & kinetic ejection | Exothermic chemical combustion + Iron-oxide slag run |
| Direct Energy Cost / m³ | $0.02 – $0.05 / Nm³ (Electrical only) | $0.35 – $0.85 / Nm³ (Supply chain indexed) | $0.25 – $0.55 / Nm³ (Cylinder transport) |
| Cutting Velocity (1–6mm SS/CS) | 115% – 140% baseline speed | 100% baseline speed (Standard benchmark) | 40% – 60% baseline speed (Thermal limit) |
| Post-Cut Edge Condition | Micro-oxide layer (Easily adheres powder coats) | Pure metallic silver (Zero oxidation layer) | Heavy black oxide scale (Requires mechanical de-burr) |
| Supply Reliability & Logistics | Continuous on-site generation; zero downtime | Subject to cryogenic transport delays & boil-off loss | Dangerous high-pressure manifold swapping & handling |
| ISO 8573-1 Purity Requirement | Class 1:2:1 (Residual oil <0.003mg/m³, Dew Pt -40°C) | Standard industrial vaporization purity | Standard welding-grade oxygen purity |
When assist air exits the conical laser cutting nozzle at 20 to 25 bar pressure, it operates in a regime of underexpanded supersonic flow. Without strict pneumatic pressure regulation within ±0.1 bar, oblique shock waves and Mach disks form between the nozzle tip and the workpiece. These shock diamonds deflect the gas stream, decoupling the assist jet from the optical kerf, creating localized turbulent eddies, molten spatter splashback onto the optical protective window, and severe bottom-edge dross adhesion. Honest Compressor's OEM Laser Series integrates dual-stage high-response pneumatic balancing reservoirs to guarantee non-pulsating laminar core gas streams.
Global Industrial Fiber Laser Expansion & Regional CDA Penetration
Analysis of international adoption trends reveals an unprecedented migration toward integrated high-pressure air systems across tier-1 manufacturing economies.
Fabricators replacing liquid N2 storage in 10kW–30kW workshops worldwide.
Based on two-shift job shop cutting 2mm–8mm structural carbon steel.
Fully certified machines operating in DACH, NAFTA, ASEAN, and Gulf regions.
Strict ISO 8573-1:2010 residual hydrocarbon ceiling safeguarding lenses.
European Union & DACH Industrial Zone
Surging electricity tariffs and severe industrial carbon taxation (EU ETS) in Germany, Austria, and northern Italy have compelled precision job shops to eliminate cryogenic gas logistics. Focus is centered on CE-certified, low-decibel (≤68 dB) enclosed 4-in-1 compressed air centers featuring integrated refrigeration and high-adsorption desiccant dryers.
- Strict adherence to EN 1012-1 safety norms
- High requirement for heat recovery integration
North American Contract Metal Fabrication
In the US Rust Belt, Texas, and Mexico, job shops running 20kW+ machines on heavy 1/4" to 1/2" plate are aggressively adopting 20-30 bar CDA systems to counteract high cryogenic bulk gas haulage surcharges and recurring monthly cylinder telemetry rental fees.
- ASME Section VIII Div 1 pressure vessels
- 460V/480V 60Hz UL-508A compliant electricals
Asia-Pacific High-Speed Production Hubs
Led by automotive sheet supply chains, electronic enclosure manufacturers, and shipbuilding yards across China, Vietnam, Thailand, and India. Massive production volumes make gas cost the single largest variable cost after raw sheet stock, pushing 24/7 continuous duty cycles.
- High-ambient tropical cooling design (up to 46°C)
- Permanent magnet VFD variable loading efficiency
Thermodynamic Architecture & The Strict ISO 8573-1:2010 Purity Barrier
The absolute bottleneck preventing contract fabricators from successfully deploying standard shop air onto modern fiber laser heads is sub-micron contamination. A fiber laser focusing optic or quartz protective cover slide operates under catastrophic laser power intensities exceeding megawatts per square centimeter. If an assist gas stream carries microscopic oil vapor droplets, liquid aerosol droplets, or moisture particulates, these substances instantly absorb photonic energy at the 1064nm to 1080nm wavelength.
This localized absorption induces rapid thermal lensing, focal shift, beam wave-front distortion, and ultimately explosive thermal fracturing of the quartz protective slide. A single blown protective lens can contaminate the internal collimation assembly, incurring tens of thousands of dollars in optical head replacement fees and catastrophic machine downtime.
To eliminate this vulnerability, Honest Compressor's OEM Laser Series adheres strictly to an unyielding purification benchmark: ISO 8573-1:2010 [Class 1:2:1] or Class 0 Oil-Free Purity:
Pressure Dew Point: -40°C Class 2 Moisture
Standard refrigerated dryers merely condense vapor down to a pressure dew point of +3°C. In high-pressure expansion nozzles, this results in immediate sub-cooling condensation at the nozzle throat. Honest Compressor couples an oversized refrigeration precooler with a twin-tower micro-heat desiccant adsorption system to maintain an absolute -40°C to -70°C dew point, guaranteeing zero liquid condensation inside the cutting chamber.
Total Residual Hydrocarbons: ≤0.003 mg/m³
Our multi-stage filtration train utilizes advanced multi-layer borosilicate nanofiber coalescence filters followed by an oversized active carbon adsorption vessel. By leveraging packed-bed activated carbon tower dynamics, hydrocarbon vapor molecules are irreversibly bound, driving oil carryover below 0.003 mg/m³—rendering the air stream completely optical-grade safe.
Particulate Filtration: Class 1 (≤0.01 μm)
Even sub-micron rust or desiccant dust particles can scatter laser energy and induce beam distortion. We integrate terminal stainless-steel sintered mesh post-filters that catch 99.999% of solids down to 0.01 micrometers. The output air stream delivers cleaner particulate metrics than the surrounding cleanroom ambient air.
Compressing atmospheric air straight to 20 or 30 bar in a single screw airend yields an excessive compression ratio (ε > 20:1), resulting in severe thermal degradation of lubricating oil, extreme rotor volumetric back-leakage, and shortened bearing lifespan. Honest Compressor utilizes Two-Stage Series Compression Technology with an optimized 5:6 asymmetric rotor profile. By cooling the gas between the low-pressure and high-pressure stages, compression approaches isothermal efficiency, reducing overall electrical motor consumption by 15% to 22% while drastically limiting thermal strain on all mechanical seals.
Localized Application Scenarios & Cutting Performance Profiles
Field-proven data parameters illustrating kerf edge quality, speed gains, and structural metallurgical characteristics across primary alloy categories.
Carbon Steel & Mild Steel (1mm – 16mm)
Cutting mild steel with high-pressure air at 16–22 bar leverages the controlled micro-combustion of the 21% atmospheric oxygen to boost cutting velocities by 30% to 50% compared to pure nitrogen. Striation patterns remain exceptionally uniform without dross beading on the lower lip. The resultant ultra-thin micro-oxide layer acts as an ideal bonding primer for automated powder coating without requiring secondary pickling or acid-wash operations.
Austenitic Stainless Steel (304 / 316)
When cutting thin-gauge stainless steel (0.8mm to 6mm) for kitchen equipment, architectural facades, or HVAC ducts, 20 bar high-pressure assist air achieves cutting rates matching or exceeding pure Nitrogen. While a light champagne-gold tint develops on the cut surface due to surface oxidation, for non-sanitary structural parts, this trade-off saves tens of thousands of dollars per month in liquid Nitrogen invoices with completely burr-free bottom edges.
Aluminum Alloys (5052 / 6061) & Galvanized
Aluminum's high thermal conductivity and low melting point make molten dross highly prone to clinging to the lower kerf corner. The high mass density and kinetic impulse of 22 to 25 bar compressed dry air rapidly shears molten aluminum and zinc layers away from the cutting front before oxide-metal intermetallic phases can freeze. This produces razor-sharp, dross-free edge geometries even on challenging galvanized zinc-coated coil stock.
Baseline Installation: Two 15kW fiber laser systems operating 16 hours/day cutting 3mm structural mild steel and 2mm stainless brackets. Utilizing bulk liquid nitrogen with ambient vaporizers, monthly assist gas expenditures averaged €8,420 (including delivery, tank leasing, and boil-off).
Retrofit Solution: Installation of one Honest Compressor 22kW Two-Stage PM VFD 25-bar Laser Integrated Compressor Skid with built-in desiccant dryer. Monthly incremental electrical consumption: €1,140. Monthly net savings: €7,280. Total capital expenditure payback achieved in exactly 4.8 months with zero optical lens failures recorded over 3,800 operational hours.
Localized Support, Engineering Customization & Global Regulatory Compliance
As an internationally oriented OEM/ODM exporter with British engineering roots established in Shanghai in 2004, Shanghai Honest Compressor Co., Ltd. operates a vertically integrated 50,000 m² smart manufacturing plant. We understand that deploying high-pressure equipment into international jurisdictions requires far more than basic functionality; it demands complete alignment with localized pressure equipment directives, electrical safety codes, and site-specific operational protocols.
Pressure Vessel Certification (PED & ASME)
All internal air receivers, oil separator tanks, and desiccant columns are certified under the European Pressure Equipment Directive (PED 2014/68/EU) with CE marking, or manufactured to ASME Boiler and Pressure Vessel Code Section VIII Division 1 with U-stamp registration for the United States, Canada (CRN), and Latin America.
Multi-Voltage Grid Adaptability & UL Standards
We provide bespoke factory electrical configurations matching international power distribution: 380V/400V/415V/50Hz (Europe, Australia, Asia) and 208V/230V/460V/480V/60Hz (North America). Electrical control cabinets feature UL/CSA certified contactors, Siemens or Schneider switchgear, and dual-language HMI touchscreens.
Turnkey OEM/ODM Skid Packaging
For laser machine integrators and overseas distributors, we design compact "4-in-1" all-in-one skid platforms incorporating the rotary compressor, high-pressure storage tank, desiccant dryer, and four-stage filtration array into a single fork-liftable base frame with custom brand colors and OEM badging.
Technology Roadmap (2026–2035): The Next Decade of Assist Gas
Pioneering research vectors in ultra-high-pressure dynamics, membrane nitrogen enrichment, and dynamic AIoT closed-loop pressure vectoring.
20–25 Bar Integrated PM VFD Skids
Wide implementation of IE4/IE5 permanent magnet variable speed screw systems equipped with micro-channel refrigeration and active carbon hydrocarbon traps. Full remote telemetry integration via 4G/5G Modbus IoT.
30–35 Bar Ultra-Pressure Mechanics
Development of specialized ultra-high-pressure dual-stage screw airends designed specifically for 30kW–60kW cutting heads processing 25mm to 40mm thick structural steel plates with zero bottom dross.
Membrane N₂ Purity Modulation
Integration of inline hollow-fiber polymer membranes within the compressor frame, enabling the CNC operator to dial in assist gas composition dynamically: from 78% CDA up to 99.5% semi-inert Nitrogen on demand.
AI Closed-Loop Kerf Pressure Tracking
Direct real-time neural linkage between laser CNC cutting path feed rates and the compressor inverter, micro-modulating assist gas pressure instantaneously across piercing, corner deceleration, and high-speed linear cuts.
Frequently Asked Engineering & Procurement Questions
Detailed technical answers addressing pressure sizing, optical lens protection, air purity validation, and financial payback metrics.
Why is standard 8-bar workshop compressed air strictly unacceptable for modern fiber laser cutting?
How does cutting edge quality with 20-bar CDA compare to pure cryogenic Nitrogen?
What is the typical financial return on investment (ROI) timeframe for a 20-bar laser compressor?
Why does Honest Compressor recommend Two-Stage compression over Single-Stage for 20-bar applications?
How often must the filtration train and activated carbon beds be serviced to guarantee zero optical risk?
Can Honest Compressor configure machines for foreign voltages and regional electrical grids?
Engineered Industrial Vacuum & Energy-Optimized Screw Systems
Explore our complete OEM/ODM production fleet including water-lubricated oil-free compressors, intelligent variable speed drives, and robust industrial screw vacuum pumps.
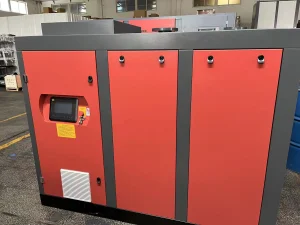
ODM electrical motor PM AC ASD rotary air vaccum pump compressor screw compressor Manufacturer, Manufacturers
View Product Specs
OEM Industrial Screw Vacuum Pumps – Oil-Injected (0.35 mbar) & Oil-Free (20–80 kPa) Series, 5.5–110 kW Supplier, Exporter
View Product Specs
OEM 30kW Water Lubricated Oil Free VSD Screw Air Compressor 380V 400V 415V Industrial Air Compressor Suppliers, Factory
View Product Specs
OEM Variable Frequency Drive Air Compressor 15kW Energy Saving Manufacturers, Exporters
View Product Specs
China Smart energy saving water lubricating 100% oil free screw air compressor with fixed speed or VSDPM Manufacturers, Exporter
View Product Specs
China Oil Cooled Screw Air Compressor 55kw 75hp Industrial Air Compressor Rotary Air Compressor Supplier, Exporter
View Product Specs
OEM 22kW 30HP Variable Speed Rotary Screw Compressor Factories, Exporter
View Product Specs