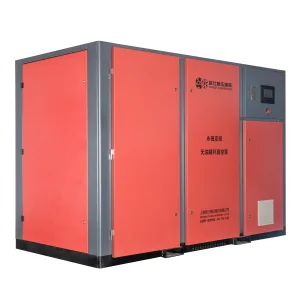
Flagship OEM Plant Air Compressor Systems
Explore high-performance rotary screw solutions engineered to deliver uninterrupted volumetric flow, low specific energy consumption, and high operational uptime across diverse industrial plant sectors.
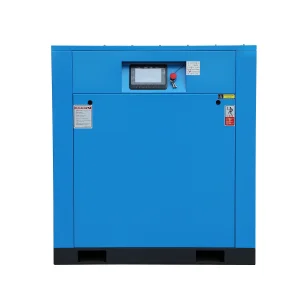
OEM VFD Screw Air Compressor 0.7-1.25MPa
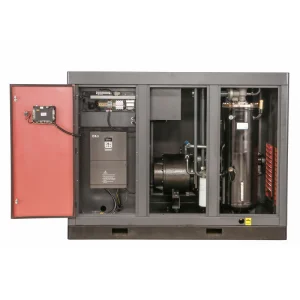
ODM Oil-Cooled Two-Stage PM VFD Screw Compressor

Permanent Magnet VFD Rotary Screw Compressor 11kW

EOF Series Oil-Free Dry Screw Compressor PM VFD
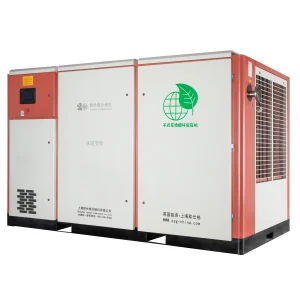
ODM EOF 100% Oil-Free Dry Screw Compressor
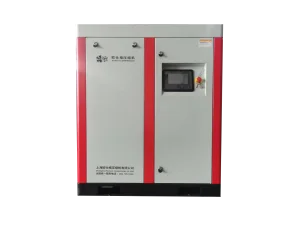
30kW Water Lubricated Oil-Free VSD Screw Compressor
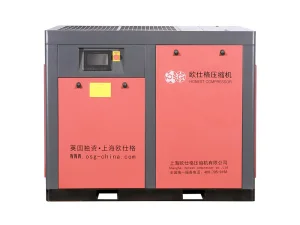
Double Screw Air Compressor with VSD PM Motor

55kW 75HP Two-Stage Direct Drive Screw Compressor
Industrial Plant Compressed Air Solutions: The "Fourth Utility"
In modern industrial facilities, compressed air is universally recognized as the fourth utility alongside electricity, natural gas, and water. However, it is fundamentally the most energy-intensive.
Over a standard 10-year lifecycle for a continuous-duty industrial plant air compressor system, electrical consumption accounts for approximately 75% to 78% of the Total Cost of Ownership (TCO). Capital expenditure (Capex) represents a modest 12%, while scheduled routine maintenance, filter consumables, and lubrication represent the remaining 10% to 13%.
As a veteran British-owned OEM manufacturer established in 2004 in Jiading District, Shanghai, Honest Compressor engineers complete utility room packages designed to drive down the specific energy requirement (kW per m³/min) across varying load cycles. Our holistic approach encompasses not only the air-end compression mechanics but also intake aerodynamics, variable speed drive synchronization, waste heat recovery systems, and distribution network design.
Generation: Two-Stage & PM VFD
By splitting the total pressure ratio across two distinct pairs of precision 5:6 asymmetrical screw rotors with intermediate cooling, interstage thermodynamic loss is minimized. Combined with IE4/IE5 permanent magnet motors, internal back-leakage is suppressed and electrical demand tracks actual plant CFM consumption without wasteful blow-off or unload idling.
Purification & Dew Point Stability
Industrial pneumatic air must be stripped of liquid condensate, aerosol mists, and particulates. Our OEM plant installations integrate refrigerated dryers achieving a stable +3°C PDP or modular desiccant adsorption systems reaching -40°C to -70°C PDP. Multi-grade coalescing filtration guarantees particulate retention down to 0.01 micron.
Network Ring & Buffer Storage
Dead-end branch piping suffers severe pressure drop and condensation settling. We assist EPC contractors and factory planners in engineering closed-loop ring main headers using calibrated smooth-bore aluminum piping, correctly sized wet and dry receiver vessels, and zero-loss electronic condensate discharge traps.
Global Commercial & Industrial Realities
Across European, North American, Southeast Asian, and Middle Eastern manufacturing ecosystems, energy costs, environmental reporting, and carbon border adjustment mechanisms are transforming capital expenditure strategies.
The Demise of Fixed-Speed Idling
Historically, legacy facilities operated fixed-speed rotary screw compressors that modulated delivery via suction throttling or standard load/unload cycling. During unloaded conditions, an idling motor still consumes 25% to 45% of its full-load rated power while delivering zero useful air volume. In continuous 8,000-hour annual factory schedules, this mechanical idling translates to tens of thousands of dollars in unrecoverable energy loss. Leading global manufacturers have initiated mandatory plant upgrades to PM VFD compressors that dynamically throttle rotor rotational speed from 100% down to 25%, maintaining system header pressure within a tight ±0.01 MPa tolerance band.
Stricter Product Purity Mandates (ISO 8573-1)
Product contamination scandals and strict regulatory governance (such as FDA FSMA in the United States and EU Regulation (EC) 1935/2004) have effectively eliminated the use of oil-injected compressors in high-risk manufacturing nodes. In clean manufacturing, even 0.01 mg/m³ of residual lubricant can foul automated pneumatic cylinders, contaminate biopharmaceutical fermentation batches, or ruin microelectronics semiconductor yields. The industrial market is aggressively migrating toward dry-running or water-lubricated oil-free screw compression systems certified to Class 0 standards, removing chemical hydrocarbon risk entirely from the compressed supply stream.
| Compressor System Architecture | Specific Power (kW / m³/min) | Turndown / Modulation | Oil Carry-over Purity | Relative Capex | 10-Year Lifecycle TCO |
|---|---|---|---|---|---|
| Standard Fixed-Speed Single-Stage | 7.2 – 8.1 @ 0.8 MPa | None (Load/Unload, 30% Idle draw) | ≤ 3 ppm (with coalescing) | Baseline (1.0x) | Highest (High kWh waste) |
| PM VFD Single-Stage Direct-Drive | 6.4 – 7.1 @ 0.8 MPa | Dynamic 25% – 100% Stepless | ≤ 2 ppm (with coalescing) | 1.35x | 20% – 30% Lower than Baseline |
| Two-Stage PM VFD Intercooled | 5.6 – 6.2 @ 0.8 MPa | Dynamic 20% – 100% Stepless | ≤ 1-2 ppm (with coalescing) | 1.75x | Lowest Overall TCO in Heavy Plants |
| Water-Lubricated Oil-Free VSD | 6.1 – 6.8 @ 0.8 MPa | Dynamic 30% – 100% Stepless | 0.00 ppm (ISO 8573-1 Class 0) | 1.80x | Low Opex, Zero Oil Reclamation |
| Dry-Type Two-Stage Oil-Free Screw | 6.5 – 7.4 @ 0.8 MPa | Dynamic 30% – 100% Stepless | 0.00 ppm (ISO 8573-1 Class 0) | 2.40x | Critical Process Security Standard |
Localized Engineering, Electrical Compatibility & Regulatory Compliance
Deploying OEM plant air compressor skids globally requires comprehensive compliance with local mechanical safety codes, electrical supply grids, and high-ambient environmental conditions.
Multi-Grid Voltage Engineering
Plant utilities must interface with regional voltages without costly step-up/down transformers. We custom engineer control enclosures and windings for 380V/50Hz (APAC & Europe), 400V/50Hz (Middle East), 415V/50Hz (UK & Commonwealth), 460V-480V/60Hz (North America), and 220V/380V/60Hz (Philippines/South Korea), fitted with dual-frequency variable frequency inverters and multi-tap auxiliary control transformers.
Pressure Vessel Certifications
Oil separator sumps, air receiver tanks, and heat exchangers are certified strictly per destination market regulations. Honest Compressor builds skids compliant with ASME Boiler and Pressure Vessel Code (Section VIII Div 1 with U-Stamp), European Pressure Equipment Directive (PED 2014/68/EU with CE marking), EAC TR CU for Russia/CIS, MOM for Singapore, and DOSH for Malaysia.
Severe Ambient Robustness (50°C / Coastal)
Industrial facilities in the Gulf region, North Africa, and Southeast Asia face ambient temperatures exceeding 46°C and high airborne saline or particulate concentrations. Our engineering incorporates oversized aluminum-plate bar fin coolers, high-static variable speed centrifugal fans, IP55/IP65 electrical enclosures with synthetic pre-filtration mats, and anti-corrosive marine C5-M coatings.
Plant-Floor Application Scenarios & Tailored Case Deployments
A plant air compressor system cannot be sized with a "one-size-fits-all" mentality. Different manufacturing verticals require dedicated aerodynamic sizing, acoustic engineering, and dew-point stabilization.
Automotive Body & Stamping Lines
Large automotive assembly plants operate hundreds of high-speed pneumatic spot-welders, robotic clamps, and laser cutting heads simultaneously. The air demand profile is erratic, marked by deep instantaneous draw-downs. Honest Compressor engineers modular two-stage PM VFD systems paired with dedicated primary high-volume wet tanks. This absorbs pressure dips while maintaining line header stability within 0.1 bar, preventing robotic line shut-downs due to pneumatic low-pressure interlocks.
Semiconductor & Electronics Cleanrooms
Lithography stations, wafer drying nozzles, and SMD component pick-and-place units require ISO 8573-1 Class 1.2.1 air purity. Hydrocarbon aerosols cannot exceed 0.01 mg/m³, with particulate filtration reaching down to sub-micron thresholds. We supply turnkey OEM skids featuring water-lubricated oil-free screw air compressors paired with heatless desiccant air dryers and zero-particle stainless-steel piping conduits, ensuring yield rates remain uncompromised.
Hazardous Chemical & Explosive Zones
Petrochemical processing plants, solvent extraction units, and resin reaction vessels operate in volatile environments containing hydrocarbon vapors. Our 4-in-1 explosion-proof PM VFD air compressors are engineered with flameproof Ex d IIB T4 / Ex d IIC T4 electric motors, intrinsically safe PLC control barriers, copper anti-sparking fans, and Ex-rated instrumentation, permitting safe co-location inside Zone 1 or Zone 2 hazardous areas.
Food Packaging, Bottling & Pharmaceuticals
Pneumatic blow molding for PET bottles, active pharmaceutical powder transport, and aseptic pill pouching demand zero possibility of mineral oil mist. By deploying Honest Compressor's EOF dry-type or EOWV water-lubricated units, food processors eliminate product recalls, streamline HACCP/GMP facility audits, and lower long-term operating costs by bypassing disposable downstream activated carbon absorption beds.
Technology Roadmap: Smart IoT, AI Diagnostics & Waste Heat Recovery
The convergence of industrial automation, industrial Internet of Things (IIoT), and thermal co-generation is reshaping plant utility room performance metrics.
Integrated Edge-Computing Compressor Master Control
Single-compressor load tracking is insufficient for large plants running multiple units. Honest Compressor incorporates centralized smart sequencing controllers capable of managing up to 16 networked compressors via Modbus TCP/IP, Profinet, or BACnet interfaces. The algorithm monitors system line pressure decay rates and schedules the optimum combination of base-load two-stage compressors and modulating PM VFD trim units, eliminating unnecessary pressure over-generation.
- Predictive AI bearing vibration and spectrum trend tracking
- Automated artificial pressure reduction (0.1 MPa cut = 7% kWh saved)
- Cloud-based remote telemetry with real-time specific power logging
- Dynamic oil thermal bypass control preventing sump moisture condensation
- Factory waste heat recovery yielding industrial hot water at 70°C–85°C
- Smart auto-sequencing equalizing total operating running hours
Frequently Asked Questions: Plant Air Engineering & OEM Sizing
Critical mechanical, electrical, and procurement guidelines for plant engineering managers and OEM system integrators.
Why does a two-stage rotary screw compressor deliver higher thermodynamic efficiency than a single-stage machine? +
During single-stage compression, air is compressed from atmospheric pressure (0.1 MPa) directly to discharge pressure (e.g., 0.8 MPa), representing a pressure ratio of 8:1. This rapid compression generates elevated thermal rise, increasing internal rotor clearances and thermal back-leakage. In a two-stage compressor, the compression is split: the first stage compresses the gas from 0.1 MPa to approximately 0.28 MPa (ratio ~2.8:1). The air then passes through an intermediate oil-curtain or intercooler chamber that quenches the temperature before the second stage raises the pressure to 0.8 MPa (ratio ~2.8:1). By cooling between stages, the thermodynamic compression cycle moves significantly closer to the ideal isothermal compression line, yielding an energy reduction of 10% to 15% for identical volumetric output.
What is the primary difference between Dry-Type Oil-Free and Water-Lubricated Oil-Free screw compressors? +
Dry-type oil-free compressors utilize timing gears and specialized rotor barrier coatings (such as PTFE or molybdenum disulphide) to ensure the intermeshing male and female rotors never physically touch. Because air is dry-compressed without an internal fluid coolant, discharge temperatures are high (frequently exceeding 180°C), requiring dual-stage compression even for standard 0.7 MPa working pressures. In contrast, water-lubricated oil-free compressors inject purified reverse-osmosis (RO) water directly into the compression cavity. The water acts simultaneously as a lubricant, an airtight rotor seal, and a thermodynamic heat sink. This enables true single-stage compression with discharge temperatures below 50°C, providing exceptional isothermal efficiency and lower replacement part overhead.
How does an OEM manufacturer ensure voltage and frequency stability for international factory installations? +
At Honest Compressor's Shanghai plant, our engineering division designs custom power electronics architecture for every export order. For 60Hz markets (USA, Canada, Mexico, Saudi Arabia, parts of the Philippines), motors are wound with high-grade electrical steel laminations rated for corresponding magnetic flux saturation, preventing overheating. Variable frequency drives are programmed with firmware configured for wide input voltage tolerances (±10%) and fitted with heavy-duty DC chokes, AC line reactors, and EMC filters (Class C2/C3) to prevent electromagnetic interference from bleeding back into sensitive plant supervisory networks.
What critical technical metrics should be provided when requesting a customized plant air system sizing quotation? +
To accurately calculate the correct compressor airend displacement, motor horsepower, receiver buffer volume, and downstream dryer capacity, our application engineering team requires: (1) Total normal and peak volumetric flow rate in m³/min or CFM; (2) Minimum required working pressure at the furthest point-of-use tool in bar or MPa; (3) Load variability profile (e.g., constant 24/7 base load vs. high peak cycling); (4) ISO 8573-1 air purity targets for solid particles, water dew point, and total oil concentration; (5) Site environmental parameters, specifically maximum ambient summer temperature, relative humidity, and plant altitude above sea level; and (6) Available cooling media (cooling tower water vs. ducted ambient air cooling).
Can Honest Compressor build turnkey containerized or skid-mounted compressed air systems? +
Yes. For remote manufacturing facilities, mining camps, petrochemical skids, and infrastructure construction projects where erecting a dedicated masonry compressor utility building is cost-prohibitive, we build ISO containerized air compressor stations (20-foot and 40-foot configurations). These modular plug-and-play skids come pre-engineered with internal acoustic insulation, intake/exhaust motorized louvers, full electrical distribution switchgear, air receivers, pre-piped refrigerated or desiccant dryers, condensate handling systems, and internal overhead hoist cranes for easy maintenance access.
How does a plant recover waste heat from an oil-injected rotary screw air compressor? +
Approximately 94% of the electrical energy supplied to an air compressor motor is converted directly into thermal heat (via mechanical friction and the gas compression process itself). By integrating our factory-installed heat recovery modules, the superheated oil circulating from the airend is intercepted before it reaches the air-cooling radiator. It passes through a counter-flow 316L stainless steel plate heat exchanger, safely transferring thermal energy to process water without contamination risk. This process allows facilities to generate pressurized hot water at 70°C to 85°C suitable for plant boiler make-up preheating, space heating, chemical cleaning baths, or domestic sanitary use, drastically reducing natural gas or boiler utility costs.
OEM Blowers, Clean Vacuum & Specialized Rotary Utilities
Complete your facility's utility envelope with precision-engineered low-pressure screw blowers and oil-free dry rotary vacuum systems built to the same exacting British engineering standards.

Industrial Oil-Free VSD Screw Blower Vacuum Pump
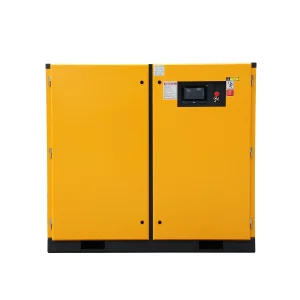
Low Noise High-Efficiency Rotary PM VSD Compressor
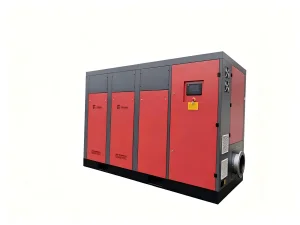
Oil-Free Screw Vacuum Pump for Semiconductor & Chemical

Oil-Free Water Lubricated Screw Compressor EOWV-45A/W

Permanent Magnet Frequency Conversion Screw Vacuum Pump
EGV-132A-140 Oil-Free PM VFD Screw Blower

22kW 30HP Variable Speed Rotary Screw Compressor