
Specialized ODM Screw Air Compressors for High-Speed Laser Cutting
Precision-manufactured air power systems engineered for continuous, heavy-duty duty cycles in precision sheet metal fabrication, automotive stamping lines, and structural laser machining centers.
China Smart energy saving water lubricating 100% oil free screw air compressor with fixed speed or VSDPM Manufacturers, Exporter
View Product Details
ODM IP55/54 55KW 75HP Factory Price Two Stage Industrial Screw Type Air Compressor Machine Factories, Exporters
View Product Details
China Oil-Free Water Lubricated Screw Air Compressor EOWV-45A/W Suppliers, Exporter
View Product Details
OEM Variable Frequency Drive Air Compressor 15kW Energy Saving Manufacturers, Exporters
View Product Details
OEM Energy Saving Air Cooling Screw Compressor Two Stage Direct Driven Screw Air Compressor Manufacturers, Exporters
View Product Details
OEM 4-in-1 Explosion-Proof Air Compressor | 7.5-22kW Permanent Magnet Integrated Unit Factory, Exporters
View Product Details
OEM Double permanent magnet motor integrated two-stage compression series Supplier, Factory
View Product Details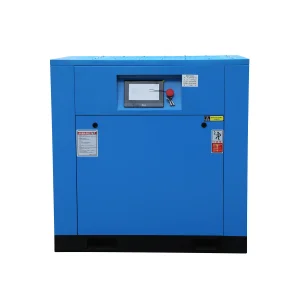
OEM Industrial 15kw/22kw/37kw/55kw/75kw Energy Saving Pm Motor VSD/VFD Rotary Screw Air Compressor Manufacturer, Exporters
View Product DetailsThe Paradigm Shift in Laser Assist Gases: Compressed Air vs. Cryogenic Nitrogen
Over the past five years, the global fiber laser cutting arena has undergone a tectonic shift. As laser sources scaled from 4kW–8kW to 20kW, 30kW, and up to 60kW+, gas consumption economics replaced machine depreciation as the single largest operational cost factor.
Exponential Opex Reduction
Liquid nitrogen (LN₂) storage Dewars or bulk cryogenic tanks carry substantial vapor loss, recurring logistics charges, and volatile regional spot prices. A dedicated high-pressure (16–25 bar) rotary screw compressor system replaces recurring gas bills with predictable electrical power consumption, slashing hourly cutting gas expenditures by up to 85%.
- Payback timeline typically achieved in 4–8 months
- Elimination of cylinder handling hazards & delivery delays
- Zero evaporation loss during off-shift factory downtime
High-Power Fiber Synergy (12kW–60kW)
Early-generation fiber lasers lacked the raw power density to cut cleanly with air due to oxidation cooling effects. With modern 15kW+ optical engines, high-pressure compressed air (78% Nitrogen, 21% Oxygen) produces an exothermic reaction that actually increases cutting speeds by 20–40% on carbon steel and aluminum compared to pure inert nitrogen cutting.
- Higher feed rates on medium-gauge mild steel plate
- Sufficient kinetic purge velocity to expel molten dross
- Superior beam penetration dynamics through thin kerfs
Supply Chain Independence
Remote industrial fabrication hubs, shipyards, and emerging manufacturing clusters in Southeast Asia, the Middle East, Eastern Europe, and Latin America frequently suffer from fractured industrial gas infrastructure. On-site assist air generation establishes absolute operational sovereignty for high-throughput job shops.
- Guaranteed 24/7/365 uninterrupted production uptime
- Insulation from commodity energy price fluctuations
- Ideal for decentralized OEM export machinery deployments
| Evaluation Parameter | Liquid Nitrogen (LN₂) Bulk Dewar | Standard Shop Air (7–8 Bar) | Dedicated ODM High-Pressure Air (16–25 Bar) |
|---|---|---|---|
| Direct Gas / Power Cost / Hr | $18.00 – $42.00 / hour (volume dependent) | $1.20 / hour (inadequate pressure) | $2.80 – $4.50 / hour (Electricity inclusive) |
| Operating Pressure at Nozzle | 18.0 – 25.0 Bar | 4.5 – 6.0 Bar (High dross formation) | 16.0 – 25.0 Bar (Smooth kerf ejection) |
| Cut Edge Metallurgy | Completely oxide-free (Silver finish) | Heavy oxide layer, excessive micro-burrs | Semi-gloss, minor micro-oxidation (weldable) |
| Cutting Speed (12kW, 6mm MS) | Baseline (100% feed rate) | Uncuttable or unstable arc blowout | 120% – 135% (Exothermic assist boost) |
| Logistical Burden | Continuous cryogenic trucking & tank boil-off | Zero external supply needed | Autonomous closed-loop utility skid |
Why Standard Compressed Air Destroys Laser Cutting Optics: The ISO 8573-1 Mandate
In high-power laser processing, the beam passes through ultra-pure fused silica lenses and quartz protective windows where power densities exceed gigawatts per square centimeter. A single aerosolized oil droplet or microscopic water molecule will instantly vaporize, thermal-shocking the optical substrate and causing catastrophic lens implosion.
Zero Oil Carryover (≤0.003 mg/m³)
Mineral or synthetic compressor lubricant vapors, when exposed to 1070nm laser radiation, absorb electromagnetic energy, leading to thermal blooming, focal shift, and beam deflection. Our systems employ multi-stage activated carbon adsorbers alongside high-efficiency coalescing filters to achieve ISO 8573-1 Class 0/1 residual oil purity.
- Guarantees optical protective lens lifespan > 1,200 hours
- Dual water-lubricated or deep-filtration dry technologies
- Prevents internal collimating chamber soot buildup
Sub-Zero Dew Point Control (-40°C PDP)
Moisture entering the cutting head at 20 bar pressure undergoes Joule-Thomson expansion cooling at the nozzle orifice, instantly generating liquid water mist. Combined combined refrigerated and modular desiccant adsorption drying systems suppress pressure dew point down to -40°C or -70°C (ISO Class 1:2:1).
- Prevents micro-droplet condensation inside fiber connector
- Eliminates thermal gradient cracking on focusing optics
- Stabilizes gas density across high-speed dynamic tracking
Sub-Micron Particulate Capture (0.01 μm)
Dust particles circulating in ambient workshop air, if concentrated under high compression, become destructive abrasive projectiles inside laser cutting heads. Integrated five-stage micro-filtration with stainless-steel internal housings arrests 99.999% of solids down to 0.01 micron.
- Protects proportional throttle and solenoid valves
- Prevents nozzle bore erosion and asymmetric gas curtains
- Certified compliance with Precitec, Raytools, and WSX specs
Localized Application Scenarios: Where High-Pressure Assist Air Excels
Engineered for diverse global manufacturing ecosystems, high-pressure assist air systems handle specific metallurgical compositions and dimensional profiles with exceptional repeatability and speed.
Carbon & Mild Steel Processing
From 1.0mm up to 20mm structural plates, air cutting delivers high feed rates. The slight exothermic reaction of atmospheric oxygen provides extra cutting energy, while high pressure expels molten iron oxide instantly.
- Agricultural equipment & chassis brackets
- Storage racking, logistics shelving & trailers
- Clean cutting without corner burning on thick plate
Stainless Steel Fabrication
When cutting kitchen equipment, ventilation ductwork, or industrial machinery brackets where slight edge yellowing is acceptable or subjected to subsequent powder coating, high-pressure air completely replaces costly nitrogen.
- Commercial kitchen sinks & food prep counters
- HVAC air handling units & architectural grilles
- Zero-burr, smooth mechanical joinery profiles
Aluminum & Light Alloys
Aluminum alloys have high thermal conductivity and low melt viscosity. At 18–22 bar pressure, clean compressed air flushes dross with extreme velocity, avoiding typical weld-back and stubborn lower-edge burrs.
- Electric vehicle battery enclosures & trays
- Architectural cladding & solar mounting brackets
- 30% faster feed rates versus pure nitrogen cuts
Heavy Machinery & Yellow Goods
Earthmoving, mining, and shipbuilding components require heavy beveling and profile cuts in 12mm–25mm high-tensile steels. High-pressure air provides the momentum necessary to blow out heavy slag across extended throat depths.
- Excavator booms, crane arms & bucket sideplates
- Heavy structural gussets & baseplates
- Continuous piercing stability without blowback spatter
Architectural Roadmap: The Evolution of Laser-Dedicated Compression Skids
From piecemeal, multi-box compressor rooms to integrated, intelligent, cyber-physical power generation units designed specifically for seamless CNC laser machine tool integration.
Two-Stage Compression
Splitting high compression ratios (up to 25–30 bar) across two separate rotor pairs lowers the pressure differential per stage. This slashes internal leakage by 35%, lowers rotor thermal stress, and extends bearing L10h life beyond 60,000 continuous hours.
IE4/IE5 PMSM + Dual VFD
Oil-cooled permanent magnet synchronous motors directly coupled without gears or belts eliminate mechanical transmission losses. Dual-inverter control regulates airend motor speed and cooling fan speed simultaneously, preventing off-load energy waste.
5-in-1 Compact Skids
Integrating the two-stage compressor, 30-bar ASME/CE air receiver, refrigerated dryer, desiccant deep dryer, and precision 5-stage filtration onto a single anti-vibration structural footprint reduces factory installation footprint by 50%.
AIoT & CNC Handshake
Industrial RS-485 / Modbus-RTU / Profinet fieldbus connectivity interfaces directly with the laser CNC controller (CypCut, Beckhoff, Siemens). Instant gas demand prediction eliminates pressure drops during rapid high-pressure piercing cycles.
System Engineering: Centralized Ring-Main vs. Dedicated Point-of-Use
Optimizing factory-wide compressed air networks requires tailored pneumatic topologies based on total installed laser wattage, shift concurrency, and duty profiles.
Point-of-Use Integrated Skids (1:1 Topology)
A single dedicated 4-in-1 or 5-in-1 compressor package placed immediately adjacent to each individual laser cutting table. This layout offers the highest flexibility for job shops operating mismatched machine capacities or independent shift schedules.
- Zero distribution pipe friction loss; maintains instant 25 bar dynamic pressure
- Modular scaling: Add compressor units only when purchasing new laser tables
- Zero factory-wide downtime if a single system undergoes routine service
- Simplified plug-and-play installation with integrated electrical disconnects
Centralized High-Pressure Ring Network (N+1 Utility)
For high-throughput factories operating 3 to 10+ laser cutting machines simultaneously, a centralized utility plant equipped with lead-lag sequencing master controllers, large-volume 30-bar storage receivers, and stainless loop piping guarantees optimal specific power efficiency.
- Lowest combined specific energy (kW/m³/min) via intelligent load balancing
- N+1 redundancy allows uninterrupted filter changes and oil service
- Noise, heat, and vibration completely isolated from precision cutting areas
- Integrated waste heat recovery systems capture up to 80% thermal energy for plant heating
Engineering Q&A: High-Pressure Laser Cutting Air Systems
Authoritative answers to the most critical technical, metallurgical, and pneumatic sizing questions asked by mechanical engineers, factory managers, and OEM exporters.
What is the minimum pressure and flow rate required for a 20kW fiber laser?
For a 20kW fiber laser cutting up to 16mm stainless steel or carbon steel with high-pressure air, the machine tool typically requires a stabilized nozzle dynamic pressure of 16 to 22 bar. Volumetric air consumption at the nozzle generally ranges from 1.8 to 2.8 m³/min (64 to 99 CFM), depending on nozzle aperture (e.g., 2.0mm to 3.5mm double-layer supersonic nozzles). We recommend specifying a 22kW to 30kW compressor producing at least 2.5–3.2 m³/min at 20–25 bar to account for pipe friction and dynamic piercing surges.
Why is a standard 8-bar workshop air compressor insufficient for laser cutting?
Standard 7–8 bar workshop compressors fail for two major reasons: dynamics and purity. First, 7 bar provides inadequate kinetic force at the cutting head nozzle; after passing through valves and internal bore passages, dynamic pressure drops below 4–5 bar, leaving molten slag unable to exit the kerf, resulting in massive bottom burrs. Second, standard plant air contains excessive liquid water, oil vapors, and particulates that instantly fog, burn, and crack expensive optical lenses within hours.
How does compressed air cutting affect edge quality compared to pure nitrogen?
Pure nitrogen cutting is chemically inert; it produces a bright, clean, completely unoxidized silver edge suitable for instant high-spec medical or aerospace welding. Compressed air consists of 78% nitrogen and 21% oxygen. The oxygen content causes microscopic surface oxidation, creating a slight straw/yellowish tint. For structural fabrication, architectural sheet metal, bracketry, and parts intended for powder coating or painting, air-cut edge adhesion is equal or superior, while the operational cost is up to 85% lower.
Why is a combined Refrigerated + Desiccant dryer system essential for high-pressure air?
At 20–25 bar, air holds significantly more moisture per unit volume than at atmospheric pressure. A refrigerated dryer alone can only lower the pressure dew point to approximately +3°C. When this air discharges through the laser nozzle, supersonic expansion causes instantaneous temperature drops down into the negative range, instantly turning residual moisture into aerosolized ice/water mist. A dual refrigerated plus modular desiccant adsorption drying train depresses the dew point to -40°C or -70°C, guaranteeing bone-dry air under any ambient humidity.
Can an oil-injected screw compressor reliably achieve ISO 8573-1 Class 0 air?
Yes, provided it is engineered with an advanced multi-stage purification train. High-pressure two-stage oil-cooled screw compressors utilize high-efficiency spin-on separator cartridges to lower bulk oil below 2 ppm, followed by secondary micro-coalescing filtration stages (0.01 ppm) and an active catalytic converter or activated carbon tower adsorber that chemically bonds hydrocarbon vapors, achieving residual oil content ≤0.003 ppm (Class 0 standard). Alternatively, our 100% oil-free water-lubricated screw series completely eliminates hydrocarbon lubricants from the compression chamber.
What customization options are supported for global OEM / ODM exporters?
As an experienced ODM manufacturer exporter, we support comprehensive mechanical and electrical tailoring: custom voltage and frequency configurations (200V, 220V, 380V, 400V, 415V, 440V, 480V at 50Hz/60Hz); certified pressure vessels conforming to ASME Section VIII, CE/PED, AS1210, and DOSH standards; PLC touch-screen multi-language firmware (English, Spanish, Russian, Turkish, Arabic, German); private-label custom enclosure paint (RAL color matching); and skid layout adaptations to slide inside standardized containerized field-laser packages.
Industrial Screw Compressors, High-Pressure Modules & Vacuum Systems
Explore our complementary range of energy-saving PM VFD rotary screw compressors, oil-free vacuum solutions, and high-pressure air systems engineered for the highest global factory standards.
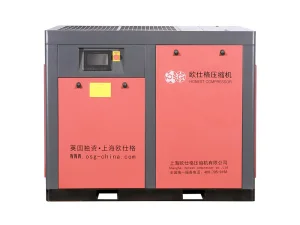
OEM Double screw air compressor with inverter and VSDPM motor for energy saving Manufacturer, Exporter
View Product Details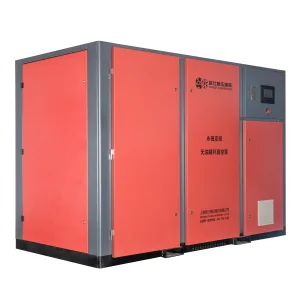
ODM PM VFD Dry Oil-Free Screw Vacuum Pump for Industrial Clean Vacuum Manufacturer, Suppliers
View Product Details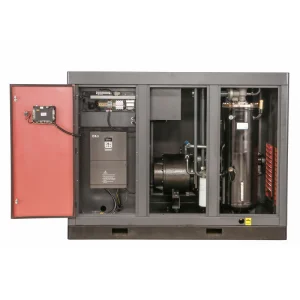
ODM Oil-cooled two-stage permanent magnet variable frequency screw air compressor Manufacturers, Suppliers
View Product Details
OEM Industrial Screw Vacuum Pumps – Oil-Injected (0.35 mbar) & Oil-Free (20–80 kPa) Series, 5.5–110 kW Supplier, Exporter
View Product Details
OEM 30kW 40HP Permanent Magnet VFD Air Compressor Manufacturers, Factories
View Product Details
China 30kw Industrial Oil Free Vsd Screw Air Blower Vacuum Pump With Plc Inverter Pm Motor oil free screw blower Supplier, Suppliers
View Product Details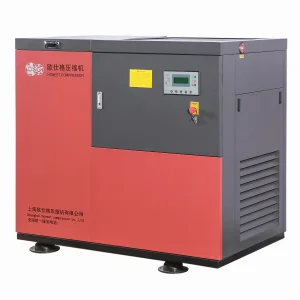
China 20bar pressure Screw Air Compressor for laser cutting machine Supplier, Suppliers
View Product Details
OEM High Precision Operational Safety Micro Oil Screw Vacuum Pump for Vacuum Industry Supplier, Exporters
View Product Details