
Precision OEM Industrial Compressors & Vacuum Assemblies
Direct manufacturer supply from our 50,000 m² Shanghai smart manufacturing plant. Standard-equipped with ultra-efficient PM motors, heavy-duty cooling matrices, and intelligent telemetry.

OEM High Precision Operational Safety Micro Oil Screw Vacuum Pump for Vacuum Industry
Configure Model
OEM 22kW 30HP Variable Speed Rotary Screw Compressor Factories, Exporter
Configure Model
OEM 18.5kW 25HP Industrial VFD PM Screw Air Compressor Factory, Exporter
Configure Model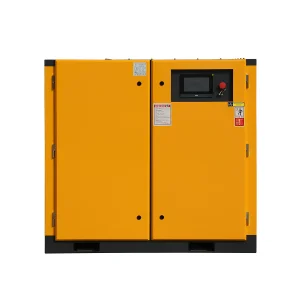
OEM Variable Frequency Drive Air Compressor 15kW Energy Saving Manufacturers
Configure Model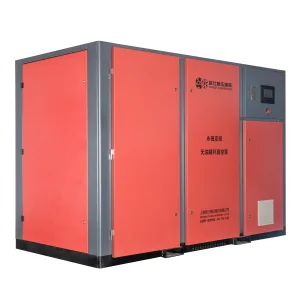
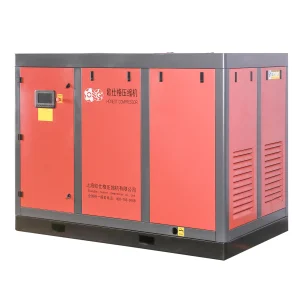
OEM Two-stage Screw Air Compressor Chemical Factory Air Equipment Manufacturer
Configure Model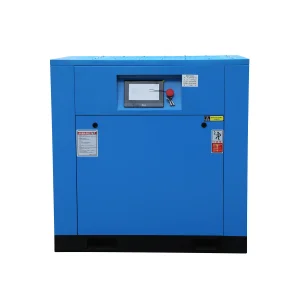
OEM Industrial 15kw/22kw/37kw/55kw/75kw Energy Saving PM Motor VSD/VFD Compressor
Configure Model
OEM Oil Free Water Lubricated Screw Air Compressor 37kW Supplier, Factories
Configure ModelTechnological Paradigms in 100 HP Air-Cooled Compression
The industrial compressed air landscape is experiencing a structural migration toward variable frequency drives, dual-stage compression efficiency, and self-contained forced air-cooling heat exchangers.
Permanent Magnet IE4/IE5 Electrification
Traditional induction motors incur significant rotor slip and magnetic excitation losses. Modern 100 HP (75 kW) compressors leverage Neodymium-Iron-Boron (NdFeB) permanent magnet synchronous motors (PMSM) maintaining >96.5% electrical-to-mechanical conversion efficiency across the entire 25%–100% operational frequency curve.
IE5 Ultra-Premium No Rotor I²R LossTwo-Stage Isothermal Compression
By dividing the total compression ratio of a 100 HP machine (typically 8:1 to 10:1) into two distinct steps with intermediate oil-curtain intercooling, internal re-expansion leakage is slashed. The compression cycle approaches the ideal thermodynamic isothermal curve, saving up to 15% specific energy (kW/m³/min) over single-stage designs.
Interstage Cooling 5.6 kW/(m³/min)IoT Edge Telemetry & AI Failure Prediction
Microprocessor integration has transcended simple start-stop sequencing. Contemporary OEM controllers continuously sample multi-channel vibration spectrographs, high-frequency pressure ripples, bearing skin temperatures, and lubricant dielectric breakdown, predicting consumable replacements 300 hours prior to degradation.
Modbus RTU / Profinet Cloud DiagnosticsThermodynamic Authority Note: In continuous baseline duty (8,000 operational hours/year), a 100 HP (75 kW) air compressor consumes approximately $72,000 USD in electricity at $0.12/kWh. Enhancing specific energy performance from 7.2 kW/(m³/min) to 5.9 kW/(m³/min) through two-stage PM VFD technology yields annual net savings exceeding $13,000 USD, amortizing capital expenditure within 18 months.
Enterprise Sourcing Matrix: Single-Source OEM Evaluation
Procuring industrial compressed air infrastructure demands an exhaustive audit of lifecycle costs, structural tolerance standards, thermal dynamics, and mechanical harmonic isolation.
| Evaluation Parameter | Standard Commercial Tier (Generic) | Honest Compressor Heavy-Duty OEM Tier | Procurement Advantage & Impact |
|---|---|---|---|
| Motor Architecture | IE2 / IE3 Asynchronous Induction (Belt/Gear) | IE4 / IE5 Permanent Magnet Synchronous (Direct C-Flange) | Eliminates transmission slip losses (2-4%); reduces electrical bill by up to 35% on variable demand. |
| Thermodynamic Cycle | Single-Stage (Compression ratio up to 11:1) | Two-Stage Dual Rotor Pairs with Intermediate Injection | Lowers thermal stress on bearings, stabilizes discharge at <8°C over ambient, cuts specific power. |
| Airend Bearing Array | Standard Ball Bearings (Rated 30,000 hrs) | Heavy-Duty Paired SKF/FAG Angular Tapered Rollers (100,000+ hrs) | Absorbs radial and axial rotor thrust, prevents clearance gap drift, extends overhaul intervals. |
| Air Cooling Geometry | Compact combi-cooler, stamped fan blade | Oversized Aluminum Bar-Plate Matrix, Variable Inverter Centrifugal Fan | Guarantees continuous 100% duty cycle in 46°C (115°F) ambient environments without thermal trip. |
| Residual Oil Content | 3 – 5 ppm w/ standard spin-on separator | < 2 ppm w/ 3-Stage Pleated Coalescing Filtration | Reduces downstream air-dryer desiccant fouling and pneumatic tool contamination. |
| Customization Rigidity | Fixed catalogue configurations | Complete OEM/ODM customization (Dual voltage, skid layout, custom paint, Ex-proof) | Tailored for EPC system integration, private label machinery manufacturers, and local grid compliance. |
The 77% Electricity Reality in 100 HP Sourcing
Across a typical 10-year lifecycle operating 6,000 hours per year, initial machinery acquisition represents merely 12% of the total cost of ownership (TCO). Routine maintenance, consumable lubricant, and air/oil filter elements account for approximately 11%. Electrical energy consumed directly accounts for the remaining 77%. OEM selection criteria that prioritize purchase price over isentropic specific power (kW/m³/min) inevitably compromise enterprise profitability.
Macro-Industry Air Solutions Engineered for Scale
Deploying 100 HP air-cooled rotary screw systems requires targeted engineering packages adapted to industry-specific atmospheric contaminants, dynamic demand fluctuations, and environmental hazards.
Automotive Stamping & Paint Shop
Requires instantaneous flow delivery from 12.5 to 15.8 m³/min without pressure dips that compromise robotics. Configured with dual-stage VFD damping and silicon-free paint-grade particulate post-filtration.
Chemical & Petrochem Plants
Engineered for hazardous atmospheres utilizing Ex d IIB T4 explosion-proof enclosures, anti-static V-belts/direct couplings, NEMA 4X / IP65 electrical enclosures, and ASME Sec VIII coded pressure vessels.
Textile & Air-Jet Looms
Characterized by extreme ambient airborne lint and sustained continuous 24/7 full-load requirements. Features heavy-duty pre-filtration cyclone housings, self-cleaning air panels, and high CFM low-dB blowers.
Pharma & Clean Food Processing
For applications demanding sterile air contact, our water-lubricated oil-free screw line delivers 100% Class 0 certified air (ISO 8573-1), eliminating mechanical oil entirely from the compression chamber.
Regulatory Compliance & Multi-Territory Interfacing
Global original equipment manufacturing necessitates strict adherence to destination-market electrical safety standards, pressure directive codes, and electromagnetic compatibility regulations.
Pressure Vessel Directives (PED / ASME)
All air/oil separation sumps and post-cooling vessels manufactured in our facility undergo 100% radiographic weld testing and hydrostatic proof-pressure qualification up to 1.5x working rating, meeting ASME Section VIII Div 1, CE-PED 2014/68/EU, and MOM certifications.
Multi-Voltage Electrical Engineering
Global deployment requires custom winding configurations: 208V/230V/460V 60Hz for North America (UL 508A compliant control cabinetry), 380V/400V 50Hz for Europe (CE LVD/EMC compliant), and 415V/440V for Southeast Asia and mining complexes.
Acoustic & Vibration Ergonomics
Equipped with tuned acoustic internal sound-dampening labyrinth panels, flexible stainless steel braided discharge conduits, and heavy elastomeric vibration mounts, keeping continuous 100 HP sound emission within an operator-safe 68–72 dB(A).
Decarbonization Roadmap & Technology Roadmap (2026–2035)
The next decade of industrial compressed air design converges on waste heat reclamation, ultra-high-efficiency synchronous reluctance mechanics, and autonomous AI-driven air network balancing.
Integrated Waste Heat Recovery (WHR)
Over 85% of input electrical power in a 100 HP compressor is transformed directly into thermal energy in the cooling fluid. Next-generation OEM units feature pre-plumbed shell-and-tube or plate heat exchangers, extracting water at 70°C for boiler pre-heating, plant district heating, or CIP wash processes without burning additional gas.
Synchronous Reluctance (SynRM) Drive Trains
Mitigating the geopolitical supply volatility of rare-earth permanent magnet elements, SynRM architectures deliver IE5 efficiency classes purely through geometric rotor magnetic anisotropy. This yields uncompromised torque characteristics and zero risk of high-temperature demagnetization under severe ambient factory loads.
Autonomous Multi-Machine Orchestration
Eliminating static cascade sequencing, AI micro-controllers monitor pressure drop velocity ($dP/dt$) throughout the header distribution loop. The system predicts pneumatic surge cycles and modulates between 100 HP base-load two-stage machines and auxiliary trimming PM units with millibar precision.
Engineered Systems: Blowers, Two-Stage & Dry Oil-Free Units
Expand your industrial pneumatic line with heavy-duty air-cooled rotary compressors, high-vacuum pumps, and specialized industrial blowers engineered to international standards.
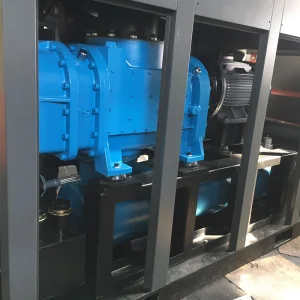
OEM Industrial Oil Free Vsd Screw Air Blower / Vacuum Pump With Inverter and PM Motor
Configure Model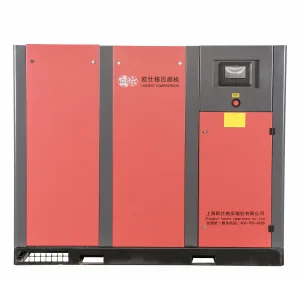
OEM Double Permanent Magnet Motor Integrated Two-Stage Compression Series
Configure Model
China 55KW 75HP 7-13bar Two Stage Screw Air Compressor Direct Drive With VSD PM Motor
Configure Model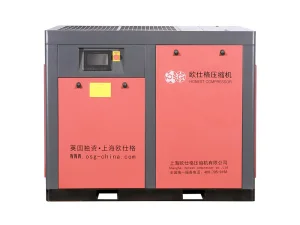
OEM Double Screw Air Compressor With Inverter and VSD PM Motor for Energy Saving
Configure Model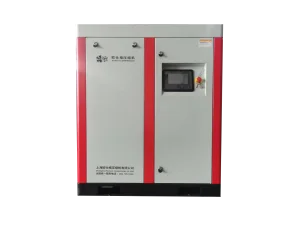
OEM 30kW Water Lubricated Oil Free VSD Screw Air Compressor 380V 400V 415V
Configure Model
OEM Screw Vacuum Pump Permanent Magnet Frequency Conversion Progressive Pump
Configure Model
ODM IP55/54 55KW 75HP Two Stage Industrial Screw Type Air Compressor Machine
Configure Model
EOF Series Oil-Free Dry Type Screw Compressor | 100% Oil-Free PM VFD Manufacturer
Configure ModelFrequently Asked Questions: 100 HP OEM Air-Cooled Systems
Authoritative technical guidance compiled by senior rotary mechanical engineers to assist plant engineers, EPC consultants, and equipment procurement managers.
What is the actual Free Air Delivery (FAD) of a 100 HP air-cooled compressor?
Under ISO 1217 Annex C conditions (20°C, 1 bar absolute), a high-performance 100 HP (75 kW) rotary screw compressor delivers approximately 14.5 to 15.2 m³/min (512 to 536 CFM) at 8.0 bar working pressure, and 12.8 to 13.5 m³/min (452 to 476 CFM) at 10.0 bar. Two-stage airends yield up to 8% higher volumetric delivery per kilowatt consumed compared to single-stage units.
Why choose air-cooled over water-cooled for 100 HP (75 kW) industrial setups?
Air-cooled architectures eliminate the substantial capital expenditure and maintenance overhead associated with external cooling towers, chemical biocides, scaling descaling treatments, and frozen pipe risk in cold seasons. Modern oversized bar-plate air-cooled heat exchangers maintain safe thermal margins in ambients up to 46°C (115°F).
How does permanent magnet variable speed (PM VFD) prevent motor overheating at low RPM?
Our OEM PM motors are engineered with separate forced-air cooling blowers or self-contained oil-cooling jackets whose heat removal rate is completely decoupled from the main rotor rotation speed. This allows indefinite operation at 20% to 25% minimum speed turns without stator or rotor thermal accumulation.
What OEM and white-label customization options are available for distributors?
As a British-invested primary manufacturer founded in 2004, Shanghai Honest Compressor offers full OEM/ODM branding: custom sheet metal fabrication, RAL color powder-coating matching corporate identity, localized multi-language touch screen PLC software (English, Spanish, French, Russian, Arabic), and specialized power cabinet certifications (UL, CSA, CE).
What is the recommended maintenance schedule to safeguard the 100,000-hour airend life?
Initial run-in oil filter and fluid change occurs at 500 hours. Subsequent routine maintenance intervals are established at every 3,000 hours for air filter elements and spin-on oil filters, and every 4,000 to 6,000 hours for synthetic polyalphaolefin (PAO) lubricant and coalescing air/oil separator cartridges, depending on operating atmospheric dust loads.
How does altitude derating affect 100 HP air-cooled rotary compressors?
At elevations exceeding 1,000 meters above sea level, thinner atmospheric density reduces mass intake airflow and diminishes the convective cooling efficiency of air coolers. Our engineering team calculates specific rotor speed adjustments and specifies oversized cooling matrices to maintain full rated discharge pressure and thermal stability at high-altitude mine installations.
