
Featured Industrial Rotary Compressors & Systems
Factory-direct OEM solutions featuring precision-ground asymmetric rotor profiles, permanent-magnet VFD controllers, two-stage energy conservation, and robust continuous operation.
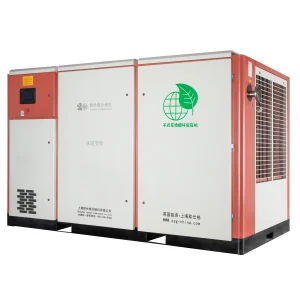
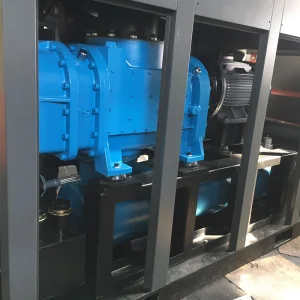
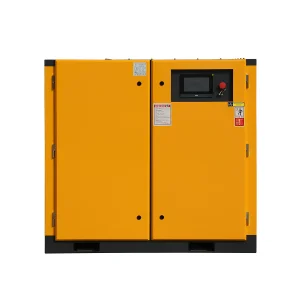
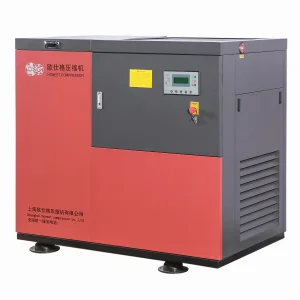


The Engineering Paradigm of Oil-Flooded Rotary Screw Air Compressors
In modern industrial infrastructure, compressed air represents the "fourth utility." For high-duty, 24/7 continuous manufacturing environments, oil-flooded (oil-injected) twin-screw compressors deliver the thermodynamic pinnacle of balance, volumetric efficiency, and operational lifespan.
Unlike intermittent reciprocating units or dynamic centrifugal systems configured for massive static flows, an oil-flooded rotary twin-screw compressor accomplishes continuous positive displacement compression via the precise intermeshing of helical male and female rotors. The thermodynamic ingenuity of the oil-flooded architecture rests on three critical functions performed by the synthetic coolant injected directly into the compression chamber:
Thermodynamic Isothermal Shift
During dry adiabatic compression, air temperature escalates exponentially, degrading density and wasting immense mechanical energy. Injected oil absorbs thermal energy at the point of compression, pushing the process closer to an efficient isothermal curve and restricting discharge temperatures below 95°C.
Dynamic Seal Clearances
Helical rotors require finite micro-tolerances (typically 15 to 30 microns) to prevent metal-to-metal galling. Injected lubricant creates dynamic fluid film seals across rotor intermesh lines and housing bores, arresting blow-hole blowby and boosting volumetric efficiency above 95%.
Direct Rotor Drive & Bearing Life
Because the injected fluid establishes an elastohydrodynamic lubrication film between contacting profiles, the male driving rotor transfers torque directly to the female rotor without requiring complex, wear-prone external timing gears, extending bearing L10h life beyond 100,000 running hours.
As a premier British-owned manufacturer situated in Jiading District, Shanghai, Shanghai Honest Compressor Co., Ltd. (operating as Honest / OSG Compressor since early 2004) manufactures over 12,000 specialized airend units annually across our 50,000 m² production site. By mastering precision 5:6 asymmetrical tooth profiles on world-class Gleason and Klingelnberg multi-axis CNC rotor milling platforms, our OEM compressors achieve specific power consumption ratings up to 18% lower than national Tier-1 energy efficiency benchmarks (GB 19153 / ISO 1217 Annex C).
| Compression Architecture | Specific Power (kW/m³/min @ 8 bar) | Capital Cost Index | Continuous Duty Cycle | Overhaul Interval (Airend) | Best Fit Applications |
|---|---|---|---|---|---|
| Oil-Flooded Single-Stage PM VFD | 6.1 – 6.6 kW/(m³/min) | Optimal (1.0x) | 100% 24/7/365 | 40,000 – 60,000 hrs | Automotive, general manufacturing, machining, packaging |
| Oil-Flooded Two-Stage PM VFD | 5.3 – 5.8 kW/(m³/min) | 1.3x – 1.5x | 100% Extreme Industrial | 80,000 – 100,000 hrs | Heavy chemical, metal refining, continuous 500+ CFM baseload |
| Oil-Free Dry Screw (Two-Stage) | 7.0 – 7.8 kW/(m³/min) | 2.2x – 2.8x | 100% Continuous | 25,000 – 40,000 hrs | Pharmaceutical cleanrooms, semiconductor fabs, food contact |
| High-Pressure Booster / Laser Cut (20-30 Bar) | 6.8 – 7.4 kW/(m³/min) | 1.2x – 1.4x | 100% Continuous Duty | 40,000 – 50,000 hrs | Fiber laser assist gas, nitrogen generation, PET blow molding |
Navigating Global Procurement Requirements for Industrial Air Systems
B2B procurement leaders, EPC engineering executives, and international distributors operate in a complex matrix of regulatory compliance, operational voltage variability, and strict Total Cost of Ownership (TCO) constraints.
Multi-Region Electrical & Grid Adaptation
Industrial manufacturing hubs present divergent grid configurations. Honest Compressor designs and exports OEM compressors configured for 380V/50Hz (China, Europe, Southeast Asia), 400V/50Hz, 415V/50Hz (UK, Australia, India), 460V/60Hz, 480V/60Hz (North America), and 220V/380V dual-voltage systems. Our integrated variable-frequency drives include internal harmonic filters, line reactors, and EMC Class C2/C3 conformance to mitigate phase imbalances and dirty power.
Harsh Environment & Ambient Tolerance Engineering
For installations spanning Middle Eastern desert oilfields (operating in +50°C ambient temperatures) to high-altitude Andean mining operations, factory standard units suffer from derating, oil foaming, and premature thermal trips. Our OEM customisation packages incorporate oversized aluminum plate-fin oil coolers, centrifugal pre-filtration cyclone separators, nano-treated intake media, and Class H insulated motors rated IP55/IP66.
Pressure Vessel Certifications & Regional Compliance
Import clearance depends on strict pressure vessel and electrical enclosure conformity. As a veteran Shanghai exporter with 20+ years of pedigree, our oil-gas separation reservoirs, aftercoolers, and moisture separators carry traceable certifications including CE-PED (Pressure Equipment Directive 2014/68/EU), ASME Section VIII Div. 1 (U-Stamp optional), EAC for the Eurasian Customs Union, and DOSH/MOM approvals for Southeast Asian jurisdictions.
Integrated 4-in-1 Compact Skid Assemblies
Factory floor space commands a high capital premium. For decentralized operations, laser fabricators, and remote workshops, Honest Compressor fabricates integrated 4-in-1 skid packages containing the oil-flooded screw compressor, vertical air receiver, refrigerated desiccant dryer, and 4-stage inline oil-mist filters on a single vibration-isolated baseframe, cutting installation time by 80% and footprint by 50%.
Macro-Industry Solutions Powered by Rotary Screw Technology
Different manufacturing and processing verticals exhibit vastly diverse demand cycles, pressure thresholds, and contamination sensitivities. Explore how our engineered oil-flooded compressor range is tailored to demanding industrial applications:
Automotive Stamping & Robotic Assembly
High-speed pneumatic presses, robotic spot welders, and conveyor transfer lines demand stable pressure devoid of surging. Our permanent-magnet variable-frequency drive (PM VFD) systems dynamically match motor rotational speed to fluctuating line demands in milliseconds, preserving line pressure within ±0.01 MPa and eliminating costly pressure drops that trip sensitive automation robotics.
High-Precision Fiber Laser Cutting (16-30 Bar)
Modern 10kW to 30kW fiber laser cutters utilize high-pressure dry air as an economical cutting assist gas for stainless steel, carbon steel, and aluminum plates. Our specialized 20 bar high-pressure oil-flooded rotary screw compressors feature multi-stage centrifugal separation and sub-micron particulate filtration to deliver residual oil concentrations below 0.001 ppm, preventing laser lens contamination.
Chemical Processing & Corrosive Environments
Continuous-process chemical refineries require uninterrupted 8,760 hours/year baseline availability. Our 55kW to 315kW two-stage oil-flooded rotary units feature cast meehanite iron casings, synthetic PAO or POE thermal fluids resistant to oxidative breakdown, explosion-proof Ex d IIB/IIC control enclosures, and stainless steel pipework configurations to resist chemical attack.
Mining, Mineral Slurry & Cement Works
Airborne silica, clinker dust, and extreme temperature fluctuations choke standard air compressor intakes. Honest Compressor equips mining-spec models with two-stage cyclonic heavy-duty air intake filters with nano-fiber media (filtering 99.9% of particles down to 1 micron) alongside low-face-velocity coolers to prevent core fouling in cement batching and mineral processing.
Textile Spunlacing & Air-Jet Looms
Textile mills operate hundreds of pneumatic air-jet looms concurrently under high ambient humidity. Any pressure fluctuation causes yarn breakage and machine stoppage. Our large two-stage permanent magnet compressors maintain extreme specific efficiency at full volumetric flow, reducing plant-wide electrical overhead while integrating zero-loss electronic condensate drains.
Centralized Smart Air Station Projects (EPC / BOO)
Engineering procurement contractors executing Build-Own-Operate (BOO) utility contracts prioritize long-term efficiency and remote telematics. Honest Compressor supplies master-slave sequenced networks via IoT gateways, orchestrating up to 16 compressors simultaneously to eliminate wasteful unload idling and balance cumulative runtime across assets.
Technology Roadmap: The Future of High-Efficiency Rotary Compression
The industrial screw compressor market is experiencing rapid technological evolution driven by strict carbon neutrality mandates, synthetic lubrication advances, and AI-enabled edge telemetry. Here is how Honest Compressor's engineering division is leading this transition:
Transition to IE5 Ultra-Premium PM Motors
While industry standard compressors still feature standard IE3 induction motors connected through elastic couplings or belts, Honest Compressor has standardized on liquid-cooled and oil-cooled IE4 and IE5 Permanent Magnet Synchronous Motors (PMSM). By embedding rare-earth NdFeB magnets directly into the rotor shaft without rotor slip or copper excitation losses, motor electrical efficiency remains consistently between 96.5% and 97.8%, even down to 25% turndown speeds.
Dual-Stage Pressure Ratio Division
In single-stage compression operating from 1 bar absolute to 8 bar gauge, the high pressure ratio (9:1) generates substantial heat and internal backflow leakage across rotor tips. Our two-stage compression splits the overall ratio across two discrete pairs of rotors (Stage 1: 1 bar to 3 bar; Stage 2: 3 bar to 8 bar). By spraying oil between stages to achieve intercooling, the specific compression work decreases by 12% to 18%, drastically reducing kilowatt consumption per cubic meter of air delivered.
Predictive IoT & Edge Condition Monitoring
Every Honest export unit can be configured with integrated 4G/5G edge telematics supporting MQTT and Modbus TCP protocols. Real-time data streams monitor vibration spectral FFT analysis, oil filter differential pressure, separator carryover resistance, and discharge temperature curves. Cloud-based machine learning models detect anomalous bearing raceway fatigue and lubricant breakdown hundreds of hours before physical failure, preventing catastrophic unscheduled shutdowns.
Factory Heat Recovery Systems (HRS)
In a standard industrial air compressor, approximately 94% of the electrical energy consumed is converted directly into heat absorbed by the cooling oil and air discharge stream. Honest Compressor integrates custom stainless-steel plate heat exchangers directly into the oil circuit. This allows facility operators to recover 75% to 85% of total shaft power as hot water at 70°C – 85°C for boiler pre-heating, sanitary plant showers, or district heating, cutting overall plant carbon footprints.
Total Cost of Ownership (TCO) & Lifecycle Decarbonization
For decades, procurement tenders disproportionately focused on capital equipment acquisition cost. However, comprehensive ISO 1217 lifecycle analyses reveal the hidden realities of compressed air operational finance:
The 5-Year Lifecycle TCO Breakdown
For an industrial 75kW (100HP) screw compressor operating 6,000 hours per year over a 5-year lifecycle horizon:
The Strategic Cost of Low-Efficiency Systems
A "budget" fixed-speed compressor with an inefficient rotor profile might save $3,000 during initial procurement, but will consume an excess of $15,000 to $25,000 in additional electrical power each calendar year. In contrast, investing in an Honest Compressor Two-Stage PM VFD unit amortizes the initial machinery investment within 9 to 14 months of commissioning.
Under tightening global emission controls—including the EU Carbon Border Adjustment Mechanism (CBAM) and corporate ESG Scope 2 decarbonization targets—audited Specific Power improvements directly contribute to lower carbon accounting across export manufacturing supply chains.
| Compressor Specification | Motor Power | Avg. Turndown Load | Annual kWh Consumed (6000h) | Annual Power Cost (@$0.14/kWh) | 5-Year Power Expenditure |
|---|---|---|---|---|---|
| Standard Fixed-Speed (Induction IE2) | 75 kW | 70% Load / 30% Idle | 427,500 kWh | $59,850 USD | $299,250 USD |
| Standard Single-Stage VFD (IE3 Motor) | 75 kW | 70% Modulated Speed | 330,750 kWh | $46,305 USD | $231,525 USD |
| Honest Two-Stage PM VFD (IE5 Motor) | 75 kW | 70% Modulated Speed | 264,600 kWh | $37,044 USD | $185,220 USD |
Global Compliance & Stringent Factory Testing Protocols
Every rotary screw compressor leaving our Shanghai manufacturing plant undergoes exhaustive mechanical, electrical, and thermodynamic validation before ocean export packaging.
Rotor CMM Verification
Helical male/female rotor pairs are inspected on ultra-precise Leitz Coordinate Measuring Machines (CMM) to ensure pitch, profile, and lead tolerances reside within ±3 microns of CAD specifications.
Dynamic Dynamic Balancing
Assembled rotor shafts and motor armatures are dynamically balanced to ISO 1940 Grade G2.5 standards, eliminating baseline harmonic vibrations that induce premature mechanical bearing wear.
Calorimeter Full-Load Run
Every complete machine undergoes a documented 4-hour full-load factory acceptance test (FAT) measuring Free Air Delivery (FAD), shaft input power, vibration velocity, and sound pressure levels.
Export Seaworthy Packaging
Compressors are hermetically vacuum-bagged with vapor corrosion inhibitors (VCI), enclosed in ISPM-15 fumigated solid timber crates, and reinforced with internal steel bracing for transoceanic transit.
Frequently Asked Engineering & Procurement Questions
Detailed technical clarifications regarding specific power calculations, air filtration, two-stage thermodynamics, and OEM supply parameters.
How is Specific Power calculated, and why is it superior to motor horsepower for evaluation?
Specific Power (expressed in kW/m³/min or kW/100 CFM) defines the true electrical energy required to deliver a standardized unit of compressed air at a specific rated pressure, measured strictly in accordance with ISO 1217:2009 Annex C or Annex E. Nominal motor horsepower or kilowatt ratings do not account for mechanical transmission losses, blower fan electrical draws, aftercooler pressure drops, or internal rotor profile efficiencies.
Two compressors with identical 75kW motors can exhibit widely disparate specific power metrics: an inferior unit may consume 7.2 kW/(m³/min), while an Honest two-stage PM VFD unit achieves 5.4 kW/(m³/min). Over 6,000 operating hours, that differential translates to tens of thousands of dollars in wasted electrical overhead.
What mechanical mechanism keeps residual oil carry-over below 3 ppm in oil-flooded compressors?
Although oil is injected directly into the twin-screw compression cavity, air delivered to the plant contains minimal trace lubricant (typically <2 to 3 mg/m³ or ppm) thanks to a three-tier separation process:
1. Primary Mechanical Cyclonic Impingement: The compressed oil-gas mixture enters the separation vessel tangentially at high velocity. Centrifugal forces fling up to 98% of liquid oil droplets against the tank walls, returning directly to the reservoir.
2. Gravity Coalescence: The slowed airstream passes through internal baffling where droplet momentum forces coalesce remaining liquid into the sump.
3. Deep-Bed Borosilicate Separator Cartridge: The air finally traverses a multi-layer micro-glass fiber separator element. Sub-micron aerosols coalesce into droplets drawn away by an internal scavenging line (oil return tube with sight-glass check valve), leaving clean, dry instrument-ready air.
Why does two-stage rotary screw compression consume significantly less energy than single-stage compression?
The thermodynamic efficiency of two-stage compression derives from reducing the compression ratio across each individual stage. In a single-stage machine elevating ambient air to 8 bar gauge (~9 bar absolute), the compression ratio is 9:1. This steep pressure differential increases internal rotor blowby leakage and elevates discharge air temperatures, driving the process toward inefficient adiabatic work.
In a two-stage compressor, Stage 1 compresses from 1 bar to approximately 3 bar absolute (ratio of 3:1). The air-oil mixture is cooled via intermediate oil mist injection before entering Stage 2, which compresses from 3 bar to 9 bar (ratio of 3:1). Dividing the ratio lowers interstage gas temperature, decreases bearing radial thrust loads by over 40%, restricts internal clearance leakage, and brings overall compression work substantially closer to the ideal isothermal compression line.
What synthetic lubricant formulations are recommended for high-ambient export installations?
For demanding export environments where ambient temperatures exceed 40°C, mineral-based oils suffer thermal cracking, varnish deposition on rotor surfaces, and premature viscosity breakdown. Honest Compressor mandates premium synthetic polyalphaolefin (PAO) or ester-based synthetic rotary compressor lubricants with a high Viscosity Index (>140) and flash points exceeding 230°C.
These synthetic lubricants offer 8,000-hour fluid service lifespans, superior demulsibility (rapid separation of atmospheric moisture condensate in humid tropical regions), and excellent hydrodynamic film tenacity under heavy bearing loads.
Can Honest Compressor engineer custom OEM/ODM designs for overseas private-label distributors?
Yes. As a dedicated OEM/ODM manufacturer with 20+ years of British-managed operational history in Shanghai, approximately 65% of our annual production output is custom-branded for major machinery brands and industrial distributor networks worldwide.
Our turnkey OEM capabilities include custom structural enclosure sheet metal design, bespoke PLC touch-screen firmware in 12+ international languages (English, Spanish, Russian, Arabic, French, German, Portuguese, etc.), tailored sheet metal powder-coat RAL colorways, specialized dual-voltage electrical engineering, and integrated private-label spare parts kits (oil filters, air filters, separator elements, synthetic lubricants).
What is the standard production lead time and maritime freight packaging standard for full container loads?
Standard lead times for standard 380V/400V 50Hz and 460V 60Hz units range from 15 to 25 business days from order confirmation. Fully customized OEM skids or explosion-proof custom systems typically require 35 to 45 business days including engineering sign-off.
Export packaging complies rigorously with international shipping regulations: machines are strapped to reinforced hardwood forklift skids, enveloped in heavy gauge polyethylene moisture barriers with desiccant packs, and enclosed within fully framed, fumigated ISPM-15 export plywood crates engineered for multi-tier ocean container stacking.
Heavy-Duty Rotary Air Compressors & Vacuum Technology
Explore additional precision-engineered twin-screw systems, variable-speed industrial air solutions, and heavy-duty rotary vacuum systems available for global OEM partnership.



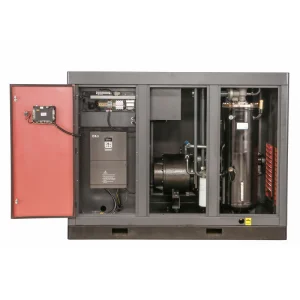


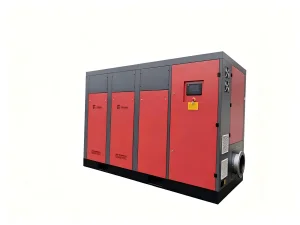
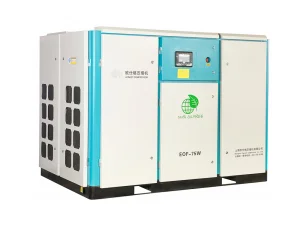
Connect Directly With Our Shanghai Engineering Division
Whether you require custom electrical enclosures (380V/400V/460V), private-label OEM manufacturing, or an authoritative plant-wide FAD specific power audit, our senior application engineers provide complete technical drawings, PID schematics, and commercial quotes within 24 hours.
